pewag conveyor chains and components
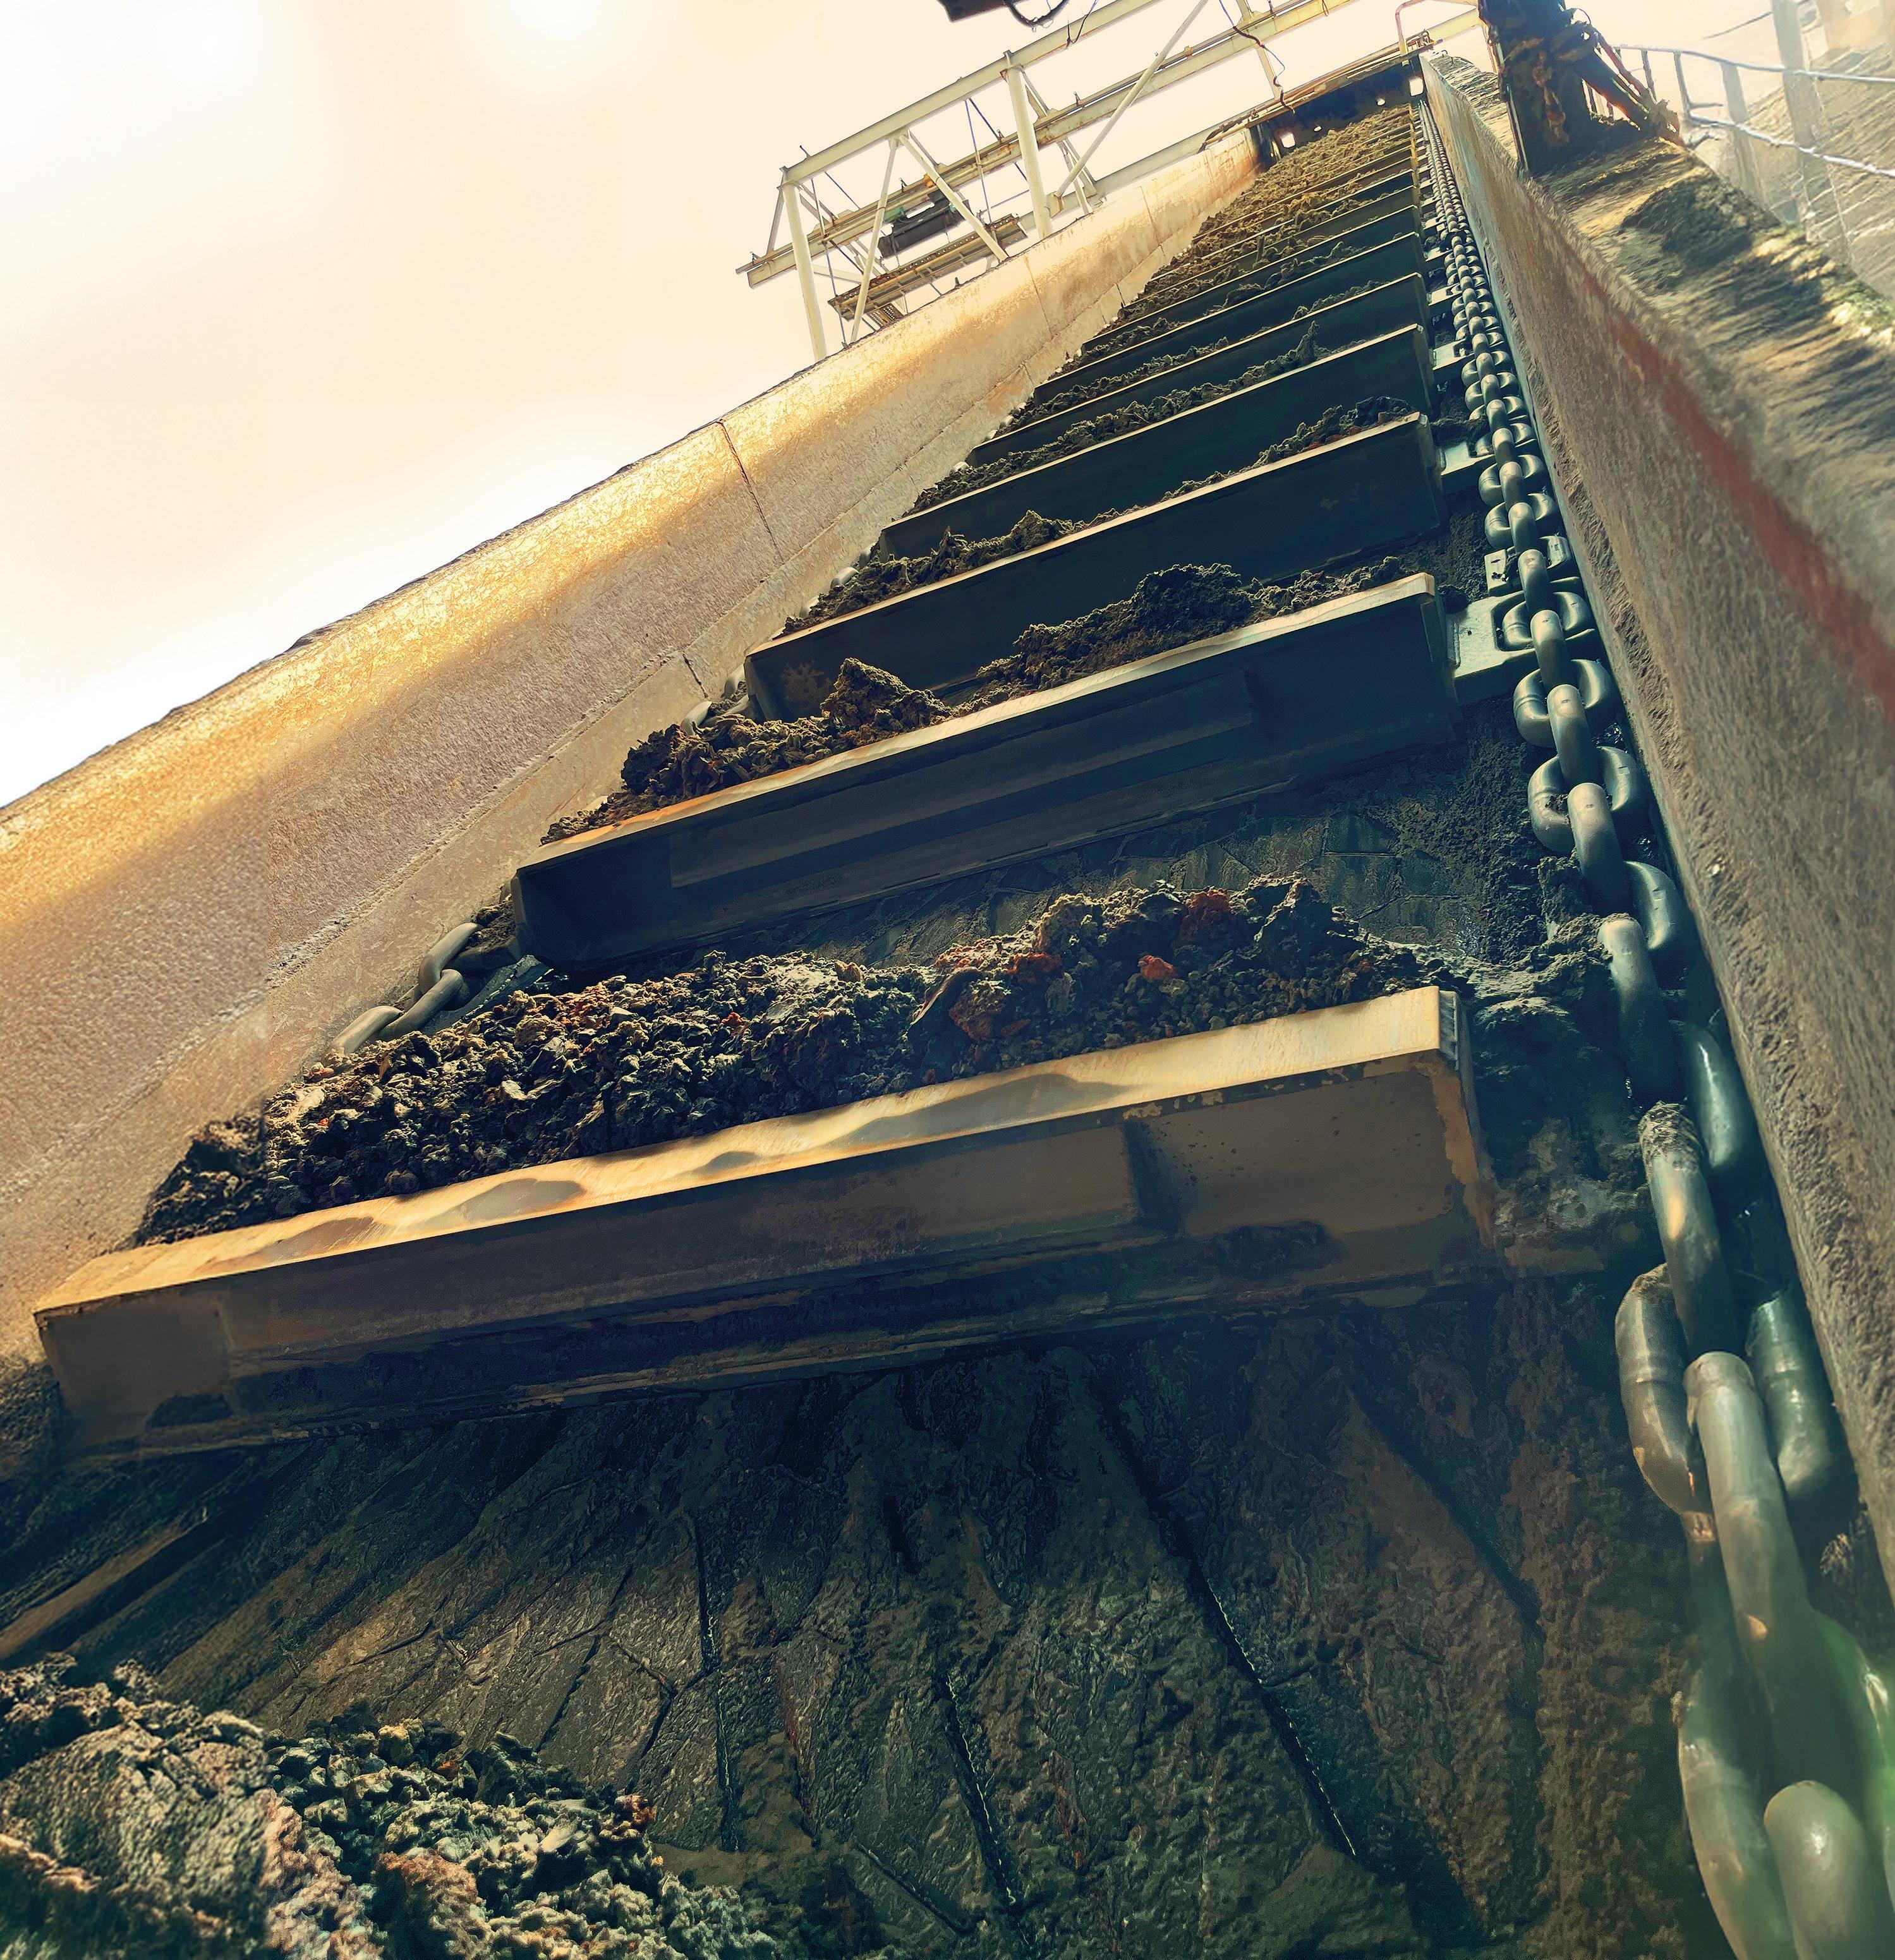
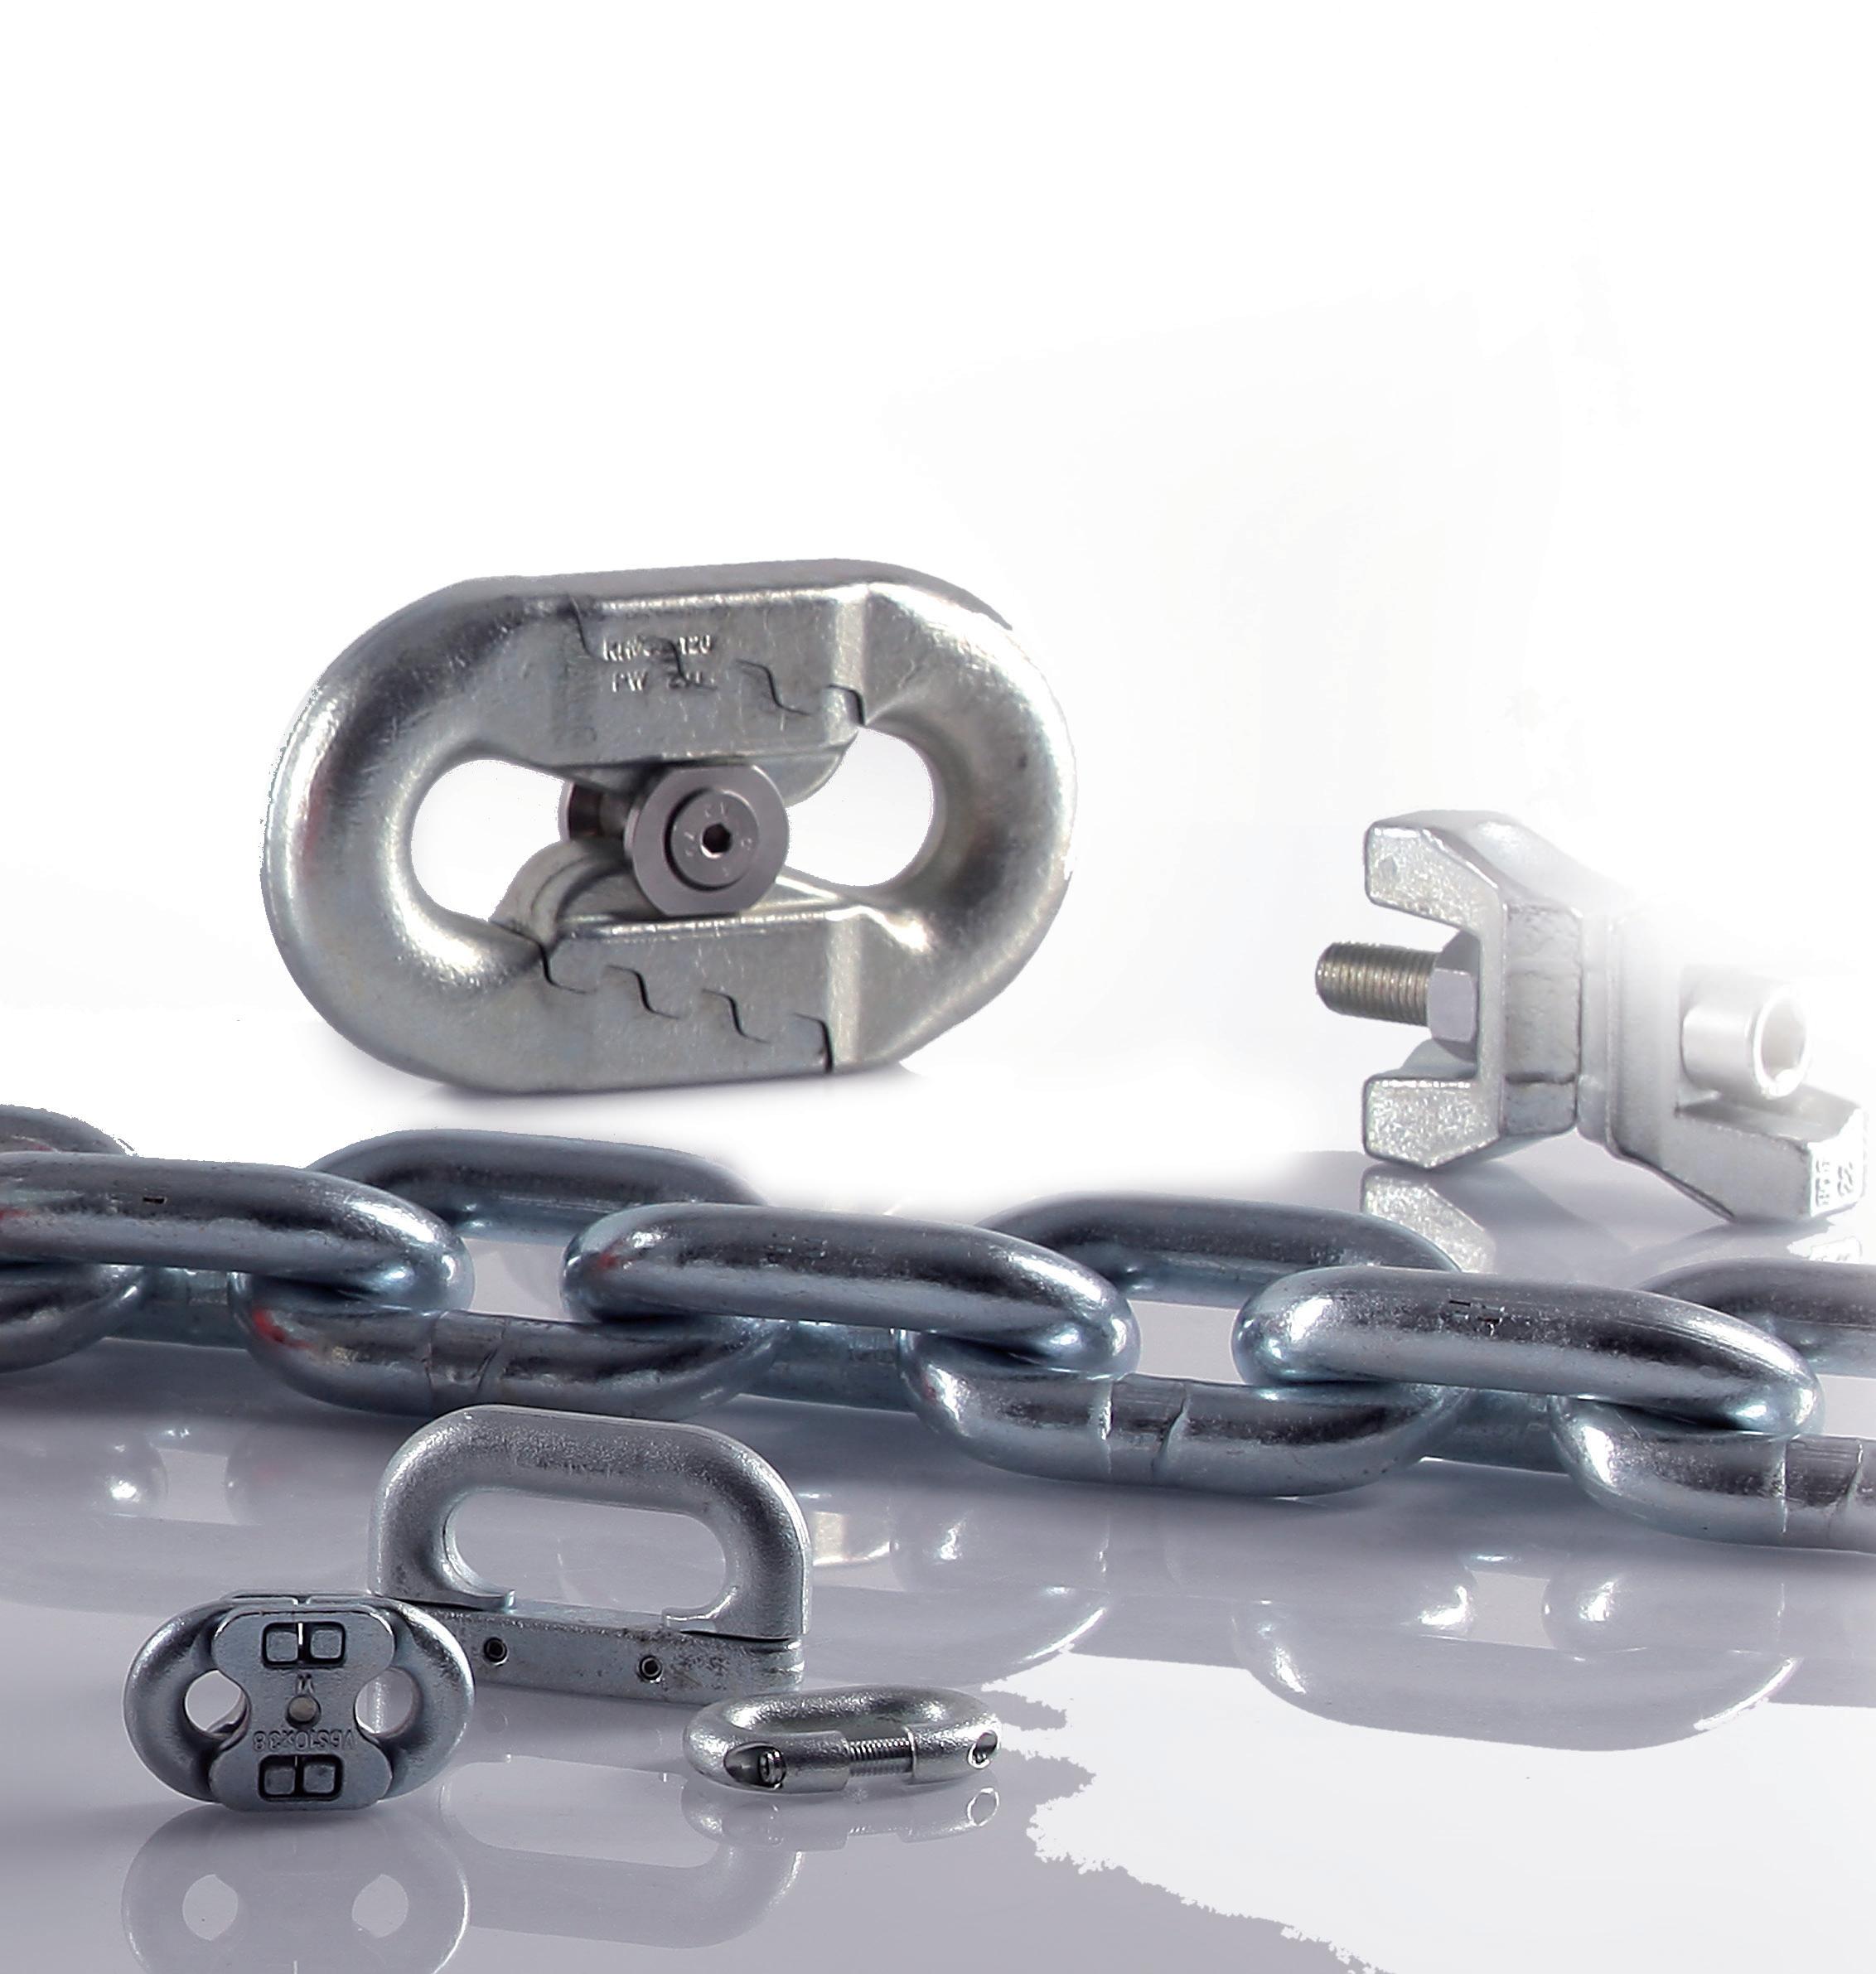
pewag conveyor technique is part of

pewag conveyor technique is part of
Through our entrepreneurial spirit - shaped by the joy of innovation - we strive to offer the best solutions for the market. Today and in the future.
The high quality of our brands, products and services, as well as the passionate commitment of our employees are our most valuable assets to exceed customer expectations and to live up to our corporate responsibility towards people and environment.
striving for excellence in QUALITY
The values of the pewag group brands are demonstrated by our first-class quality and continuous innovation. You can rely on us.
striving for excellence in RESPONSIBILITY
Our goal is CO2 neutral production by 2030. We live sustainable and fair partnerships and an open way of working together. We take on social as well as environmental responsibility.
striving for excellence in ENTREPRENEURSHIP
Through the specific expertise of each individual and decentralized responsibilities, we ensure healthy growth and a sustainably successful future.
striving for excellence in TECHNOLOGY
We ensure our technological strength by striving for quality, continuous improvement and innovation of our products and production processes.
The corporate ethics of the pewag group are based on our clear commitment to universal human rights. As a globally active group of companies, we bear a social and corporative responsibility. This applies in particular to our employees. Their occupational safety and health protection are our top priority. We promote their personal and professional development and foster a culture of open, honest, non-discriminatory and team-oriented exchange based on transparent communication. We apply the same standards in our dealings with customers, suppliers and other business partners.
We are committed to a careful and sustainable approach to the environment. This applies to all areas and activities of our group of companies. For us, it is a matter of course to use resources as efficiently as possible and to ensure this also in the future through new environmentally friendly and efficient processes. We are continuously working to optimize the durability and recyclability of our products. In this context, one of our core concerns is to continuously improve our energy efficiency and thus reduce energy consumption in the long term. The energy we use comes from renewable energy sources and is already partly generated by ourselves.
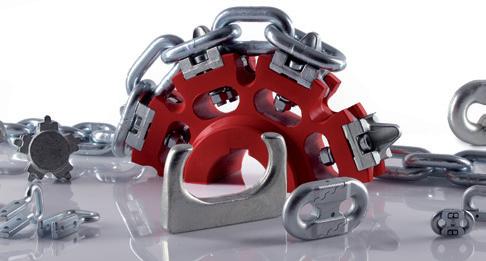
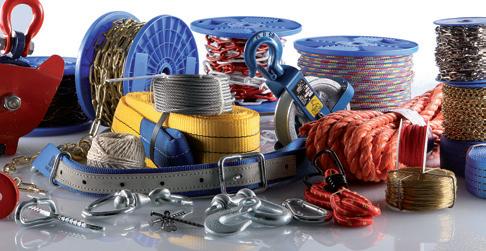
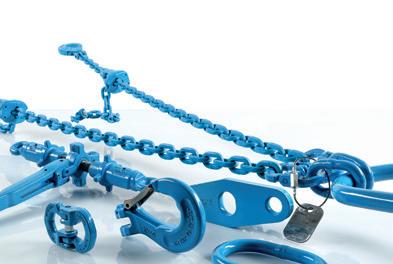
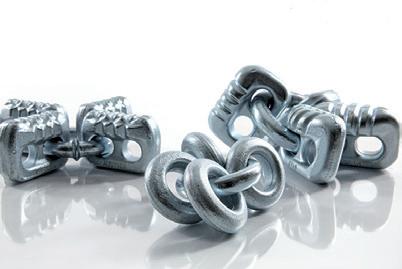
Our international brands have an extensive and diverse range of products and services.
The portfolio ranges from traction chains for tires, tire protection chains for mining vehicles over a wide range of technical chains and innovative lifting solutions up to products for the do-it-yourself area as well as forming technology.
With over 50 locations on five continents, the pewag group forms a global platform of product specialists, partners and suppliers.
This community is strengthened by a large network of external experts from science, research and development and a wide range of brands and companies within the group.
Based on centuries of experience, genuine craftsmanship and innovative technologies we process the highest quality materials with the claim to offer the best solutions on the market.
What unites us as people within the pewag group is the strong ambition for continuous development.
Discover cutting-edge products and the advanced technologies that drive their performance, quality, and durability! At pewag academy, we equip customers, partners, and employees with expert knowledge on installation, safety inspections, and maintenance. We offer valuable insights into key topics like sustainability, cybersecurity, and more. Join us to explore how these innovations are shaping the future and elevate your expertise!
pewag academy offers a wide range of exciting courses available in both e-learning and blended learning formats. Our experts use a dynamic mix of multimedia teaching methods and innovative didactics to create a truly lasting learning experience. From e-learning to immersive virtual reality, our courses deliver specialized knowledge in an engaging and interactive way. Ready to explore and learn more?
We ensure the highest quality of teaching materials, validated through our ISO 29993 certification for learning services outside formal education. This certification guarantees that our courses meet international standards for excellence and effectiveness. You can trust that our programs are designed to provide valuable, practical knowledge that enhances both professional and personal development.
Contact us for more information: academy@pewag.com
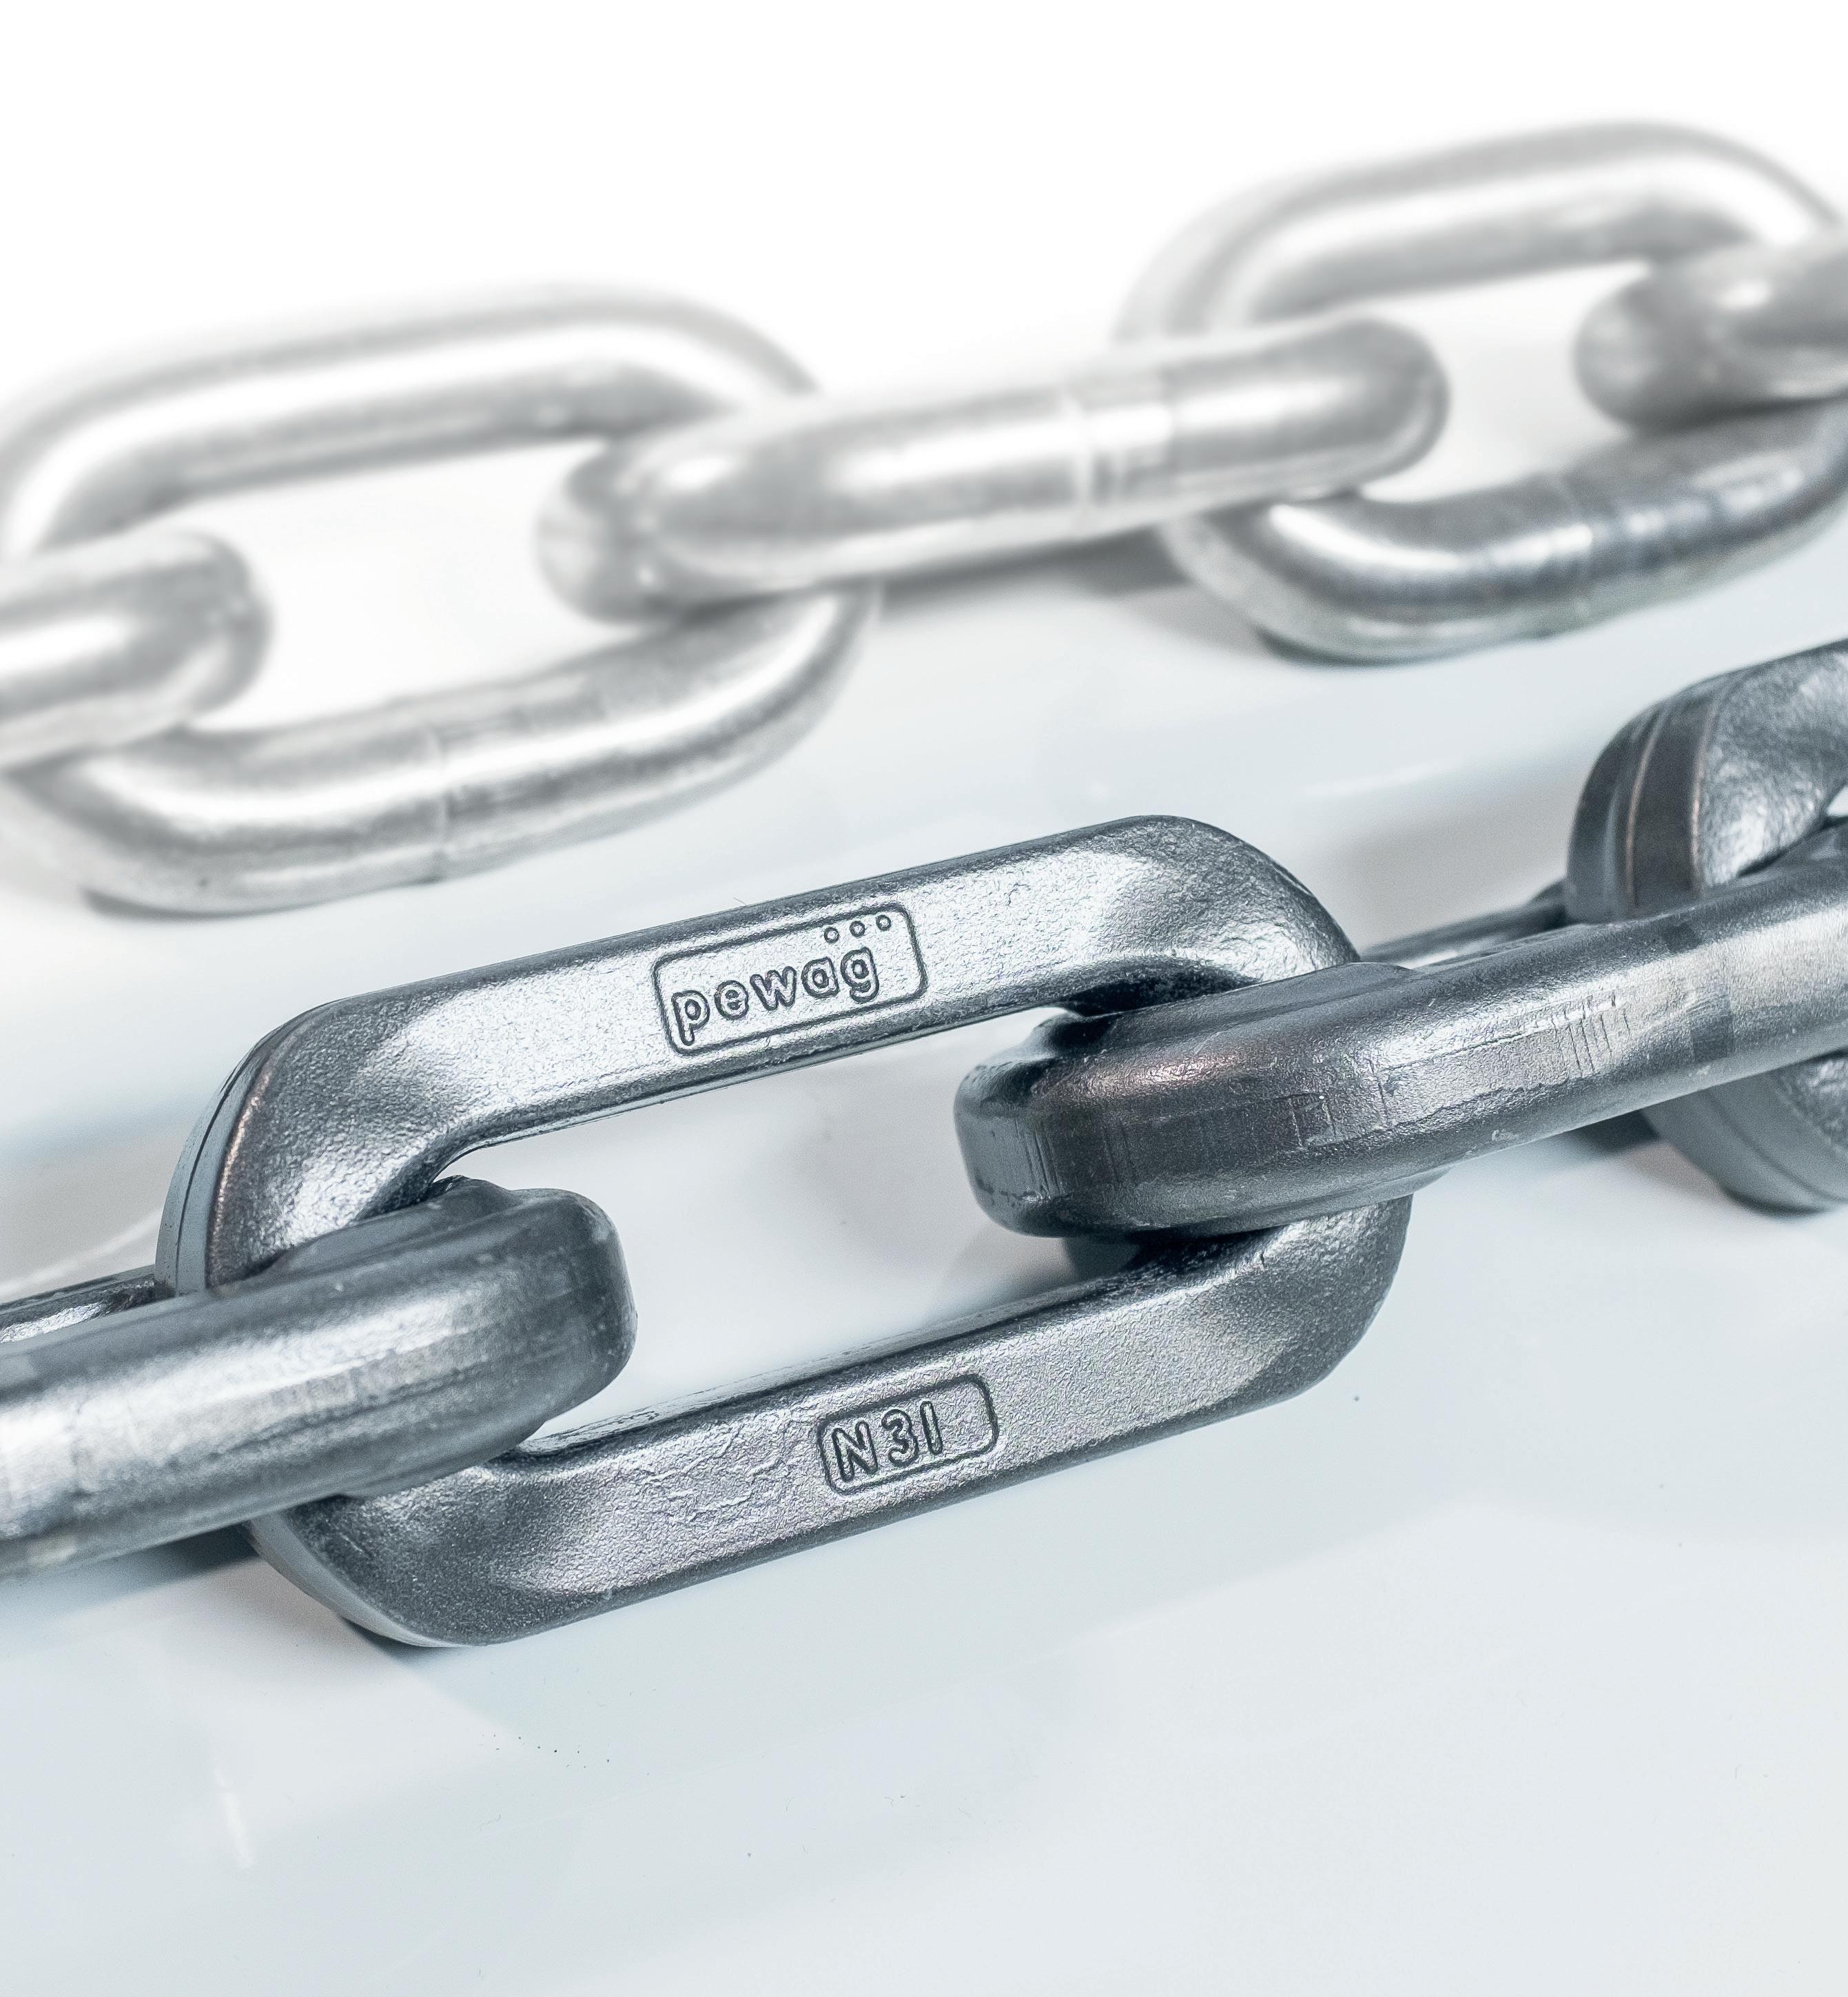
Manufactured on state-of-the-art chain production machines, our chains achieve high dimensional accuracy and tight tolerances, ensuring smooth operation in demanding chain drive applications. An environmentally friendly continuous heat
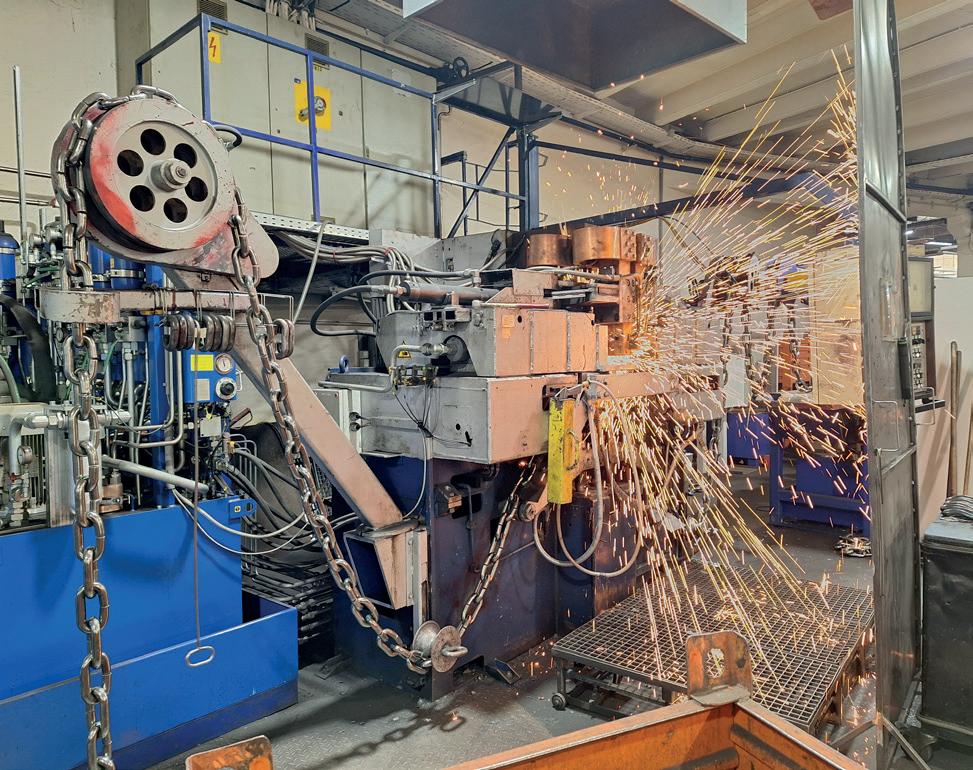
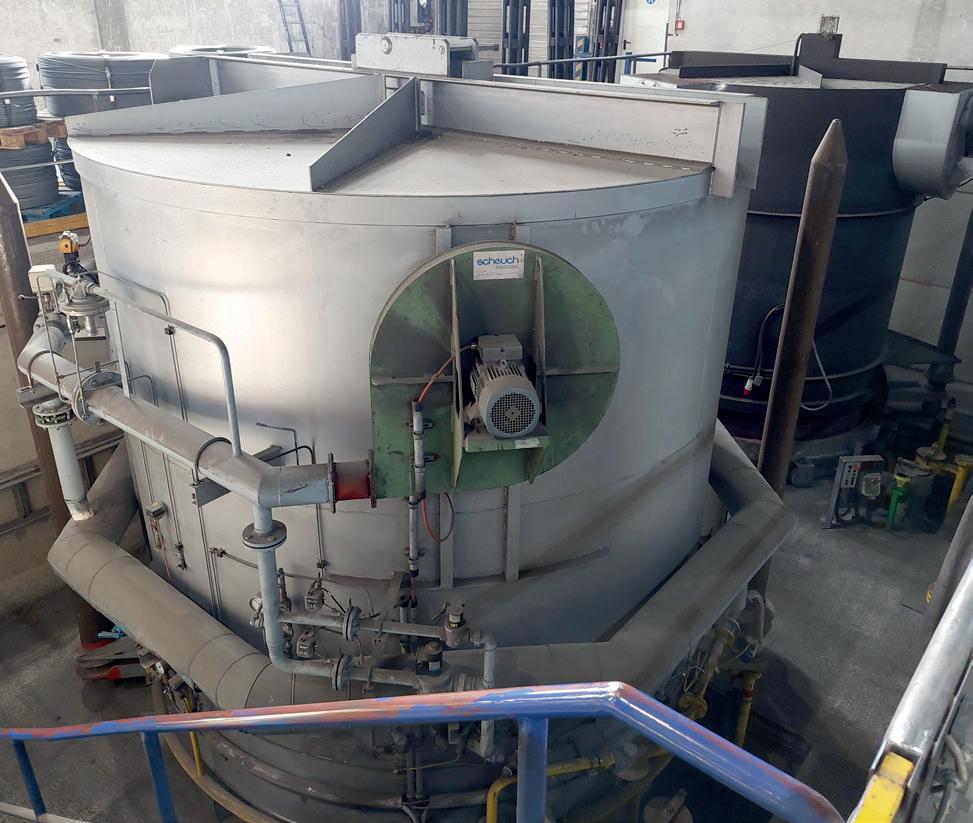
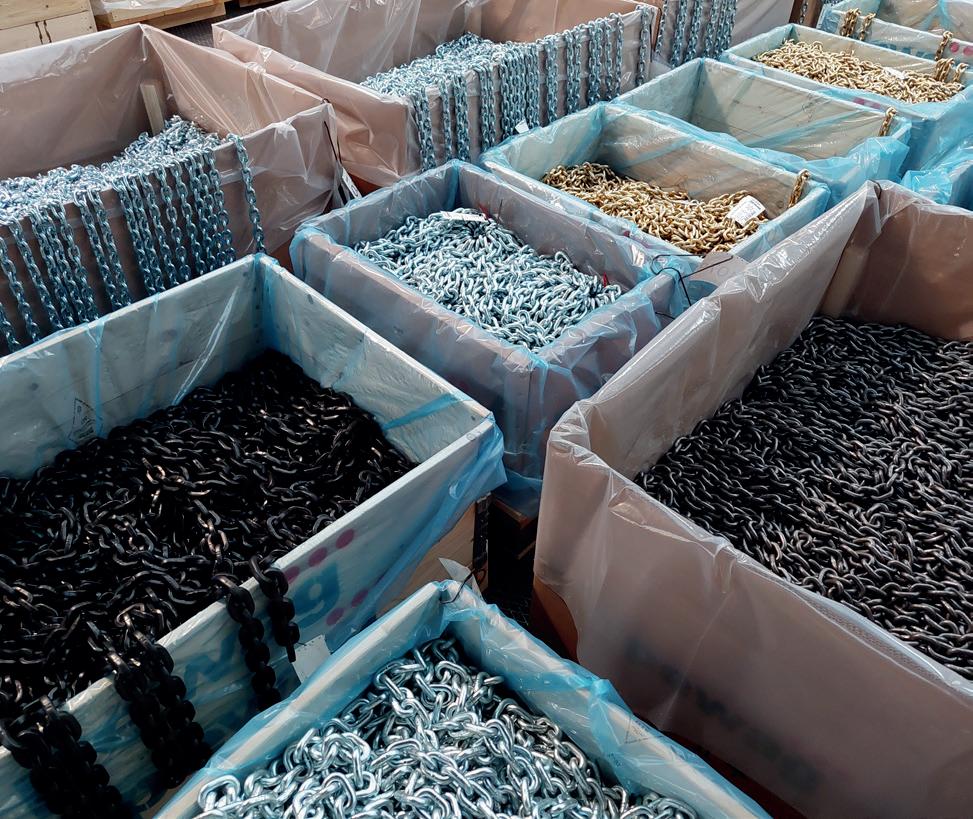
treatment provides uniform hardness and strength for every link. Comprehensive testing and development capabilities, supported by numerous test benches and inspection systems, guarantee consistent performance and long service life.
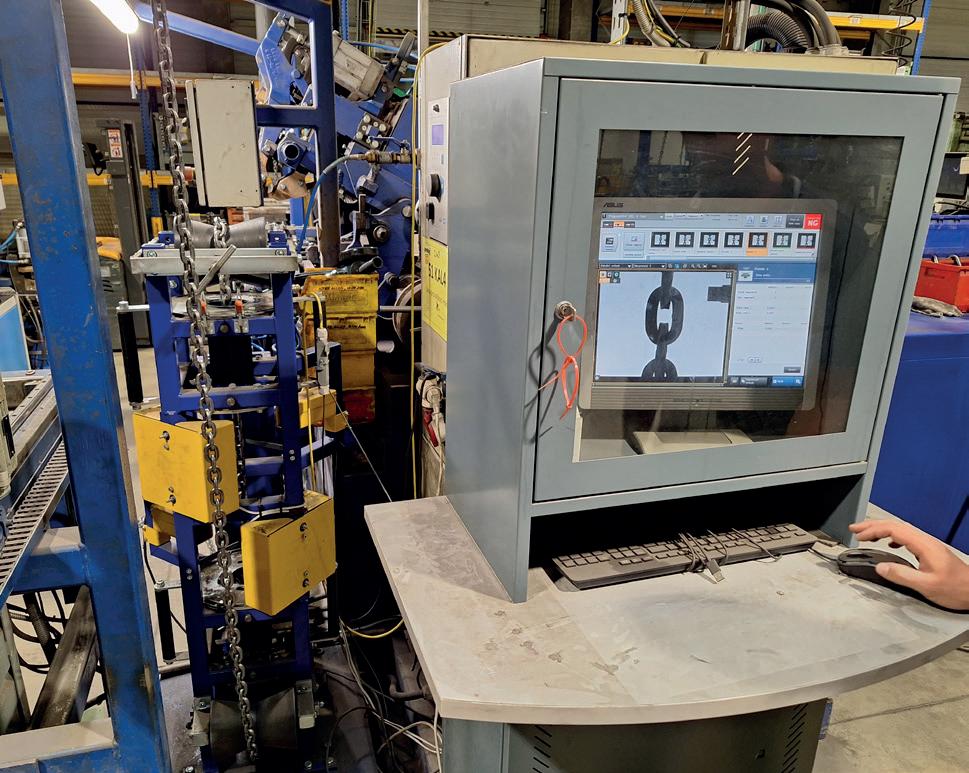
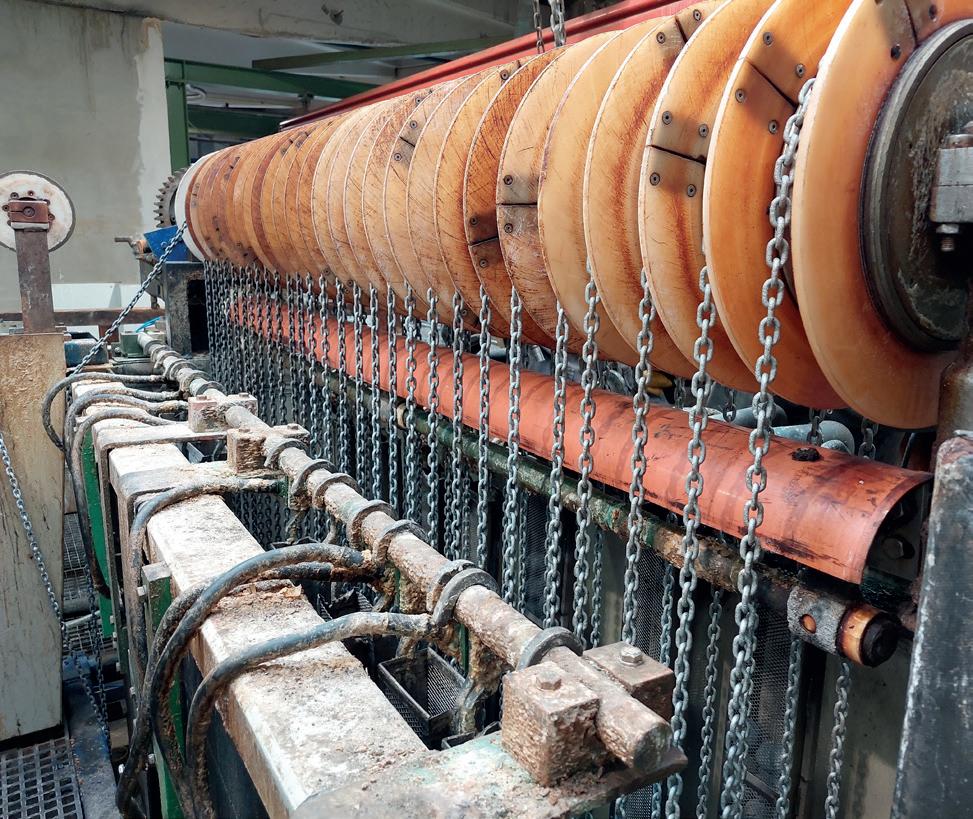
For decades, chains have been produced using the same method: by cutting wire rod or rod steel, bending the round steel to the desired link shape and welding the links together using energy-intensive processes like resistance or flash-butt welding.
The limiting factors of this conventional technology are the shape of the chain links (round) as well as the weldability of the steel grade, which very much depends upon the carbon content and alloying elements.
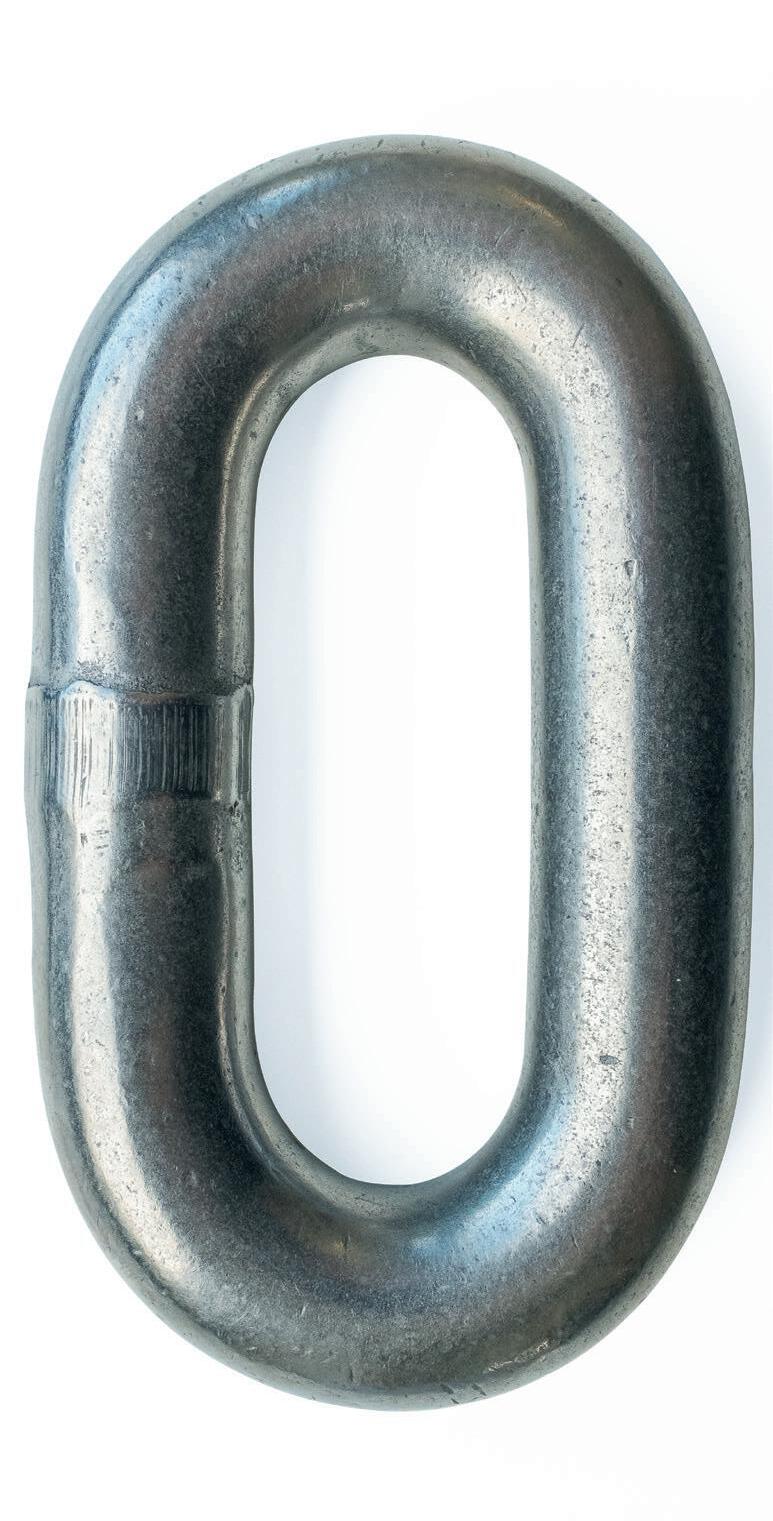
pewag hero, an innovative friction-welded chain, goes beyond these limits and opens the door to a new world of chains.
Friction welding is a well-established “joining technology” which has been used by aviation and automotive industries for decades. pewag is the first chain producer to apply and refine the friction welding process for the production of the next generation of chains.
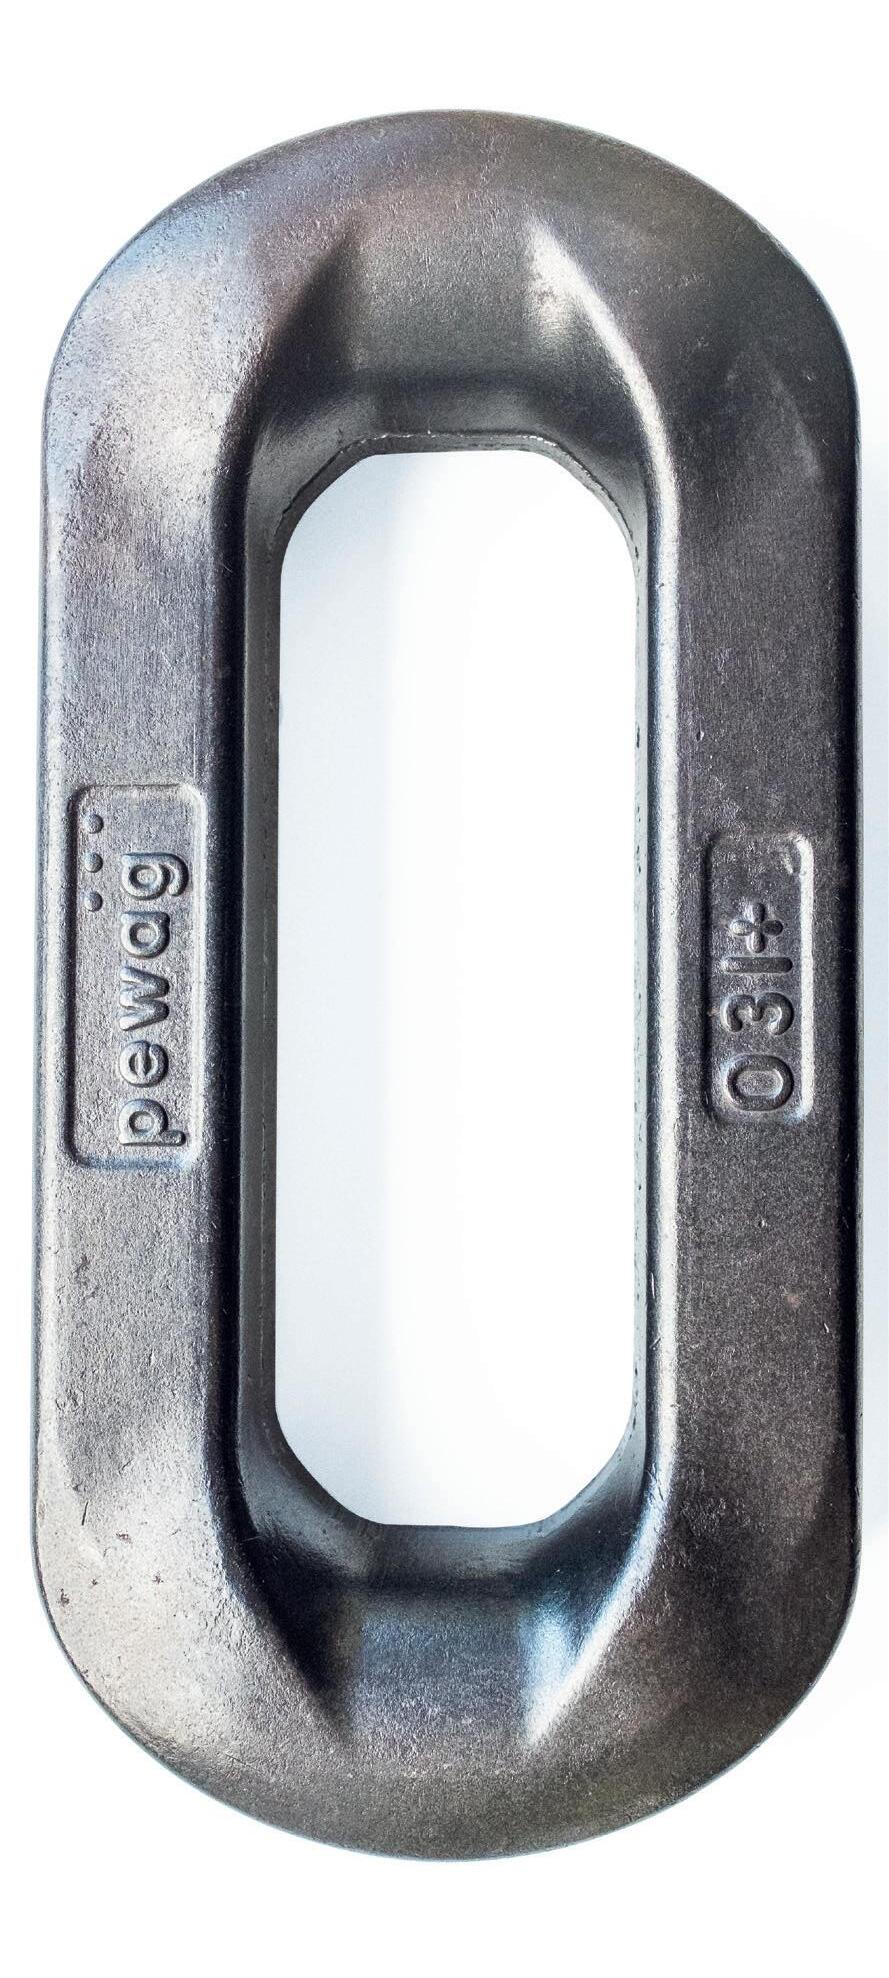
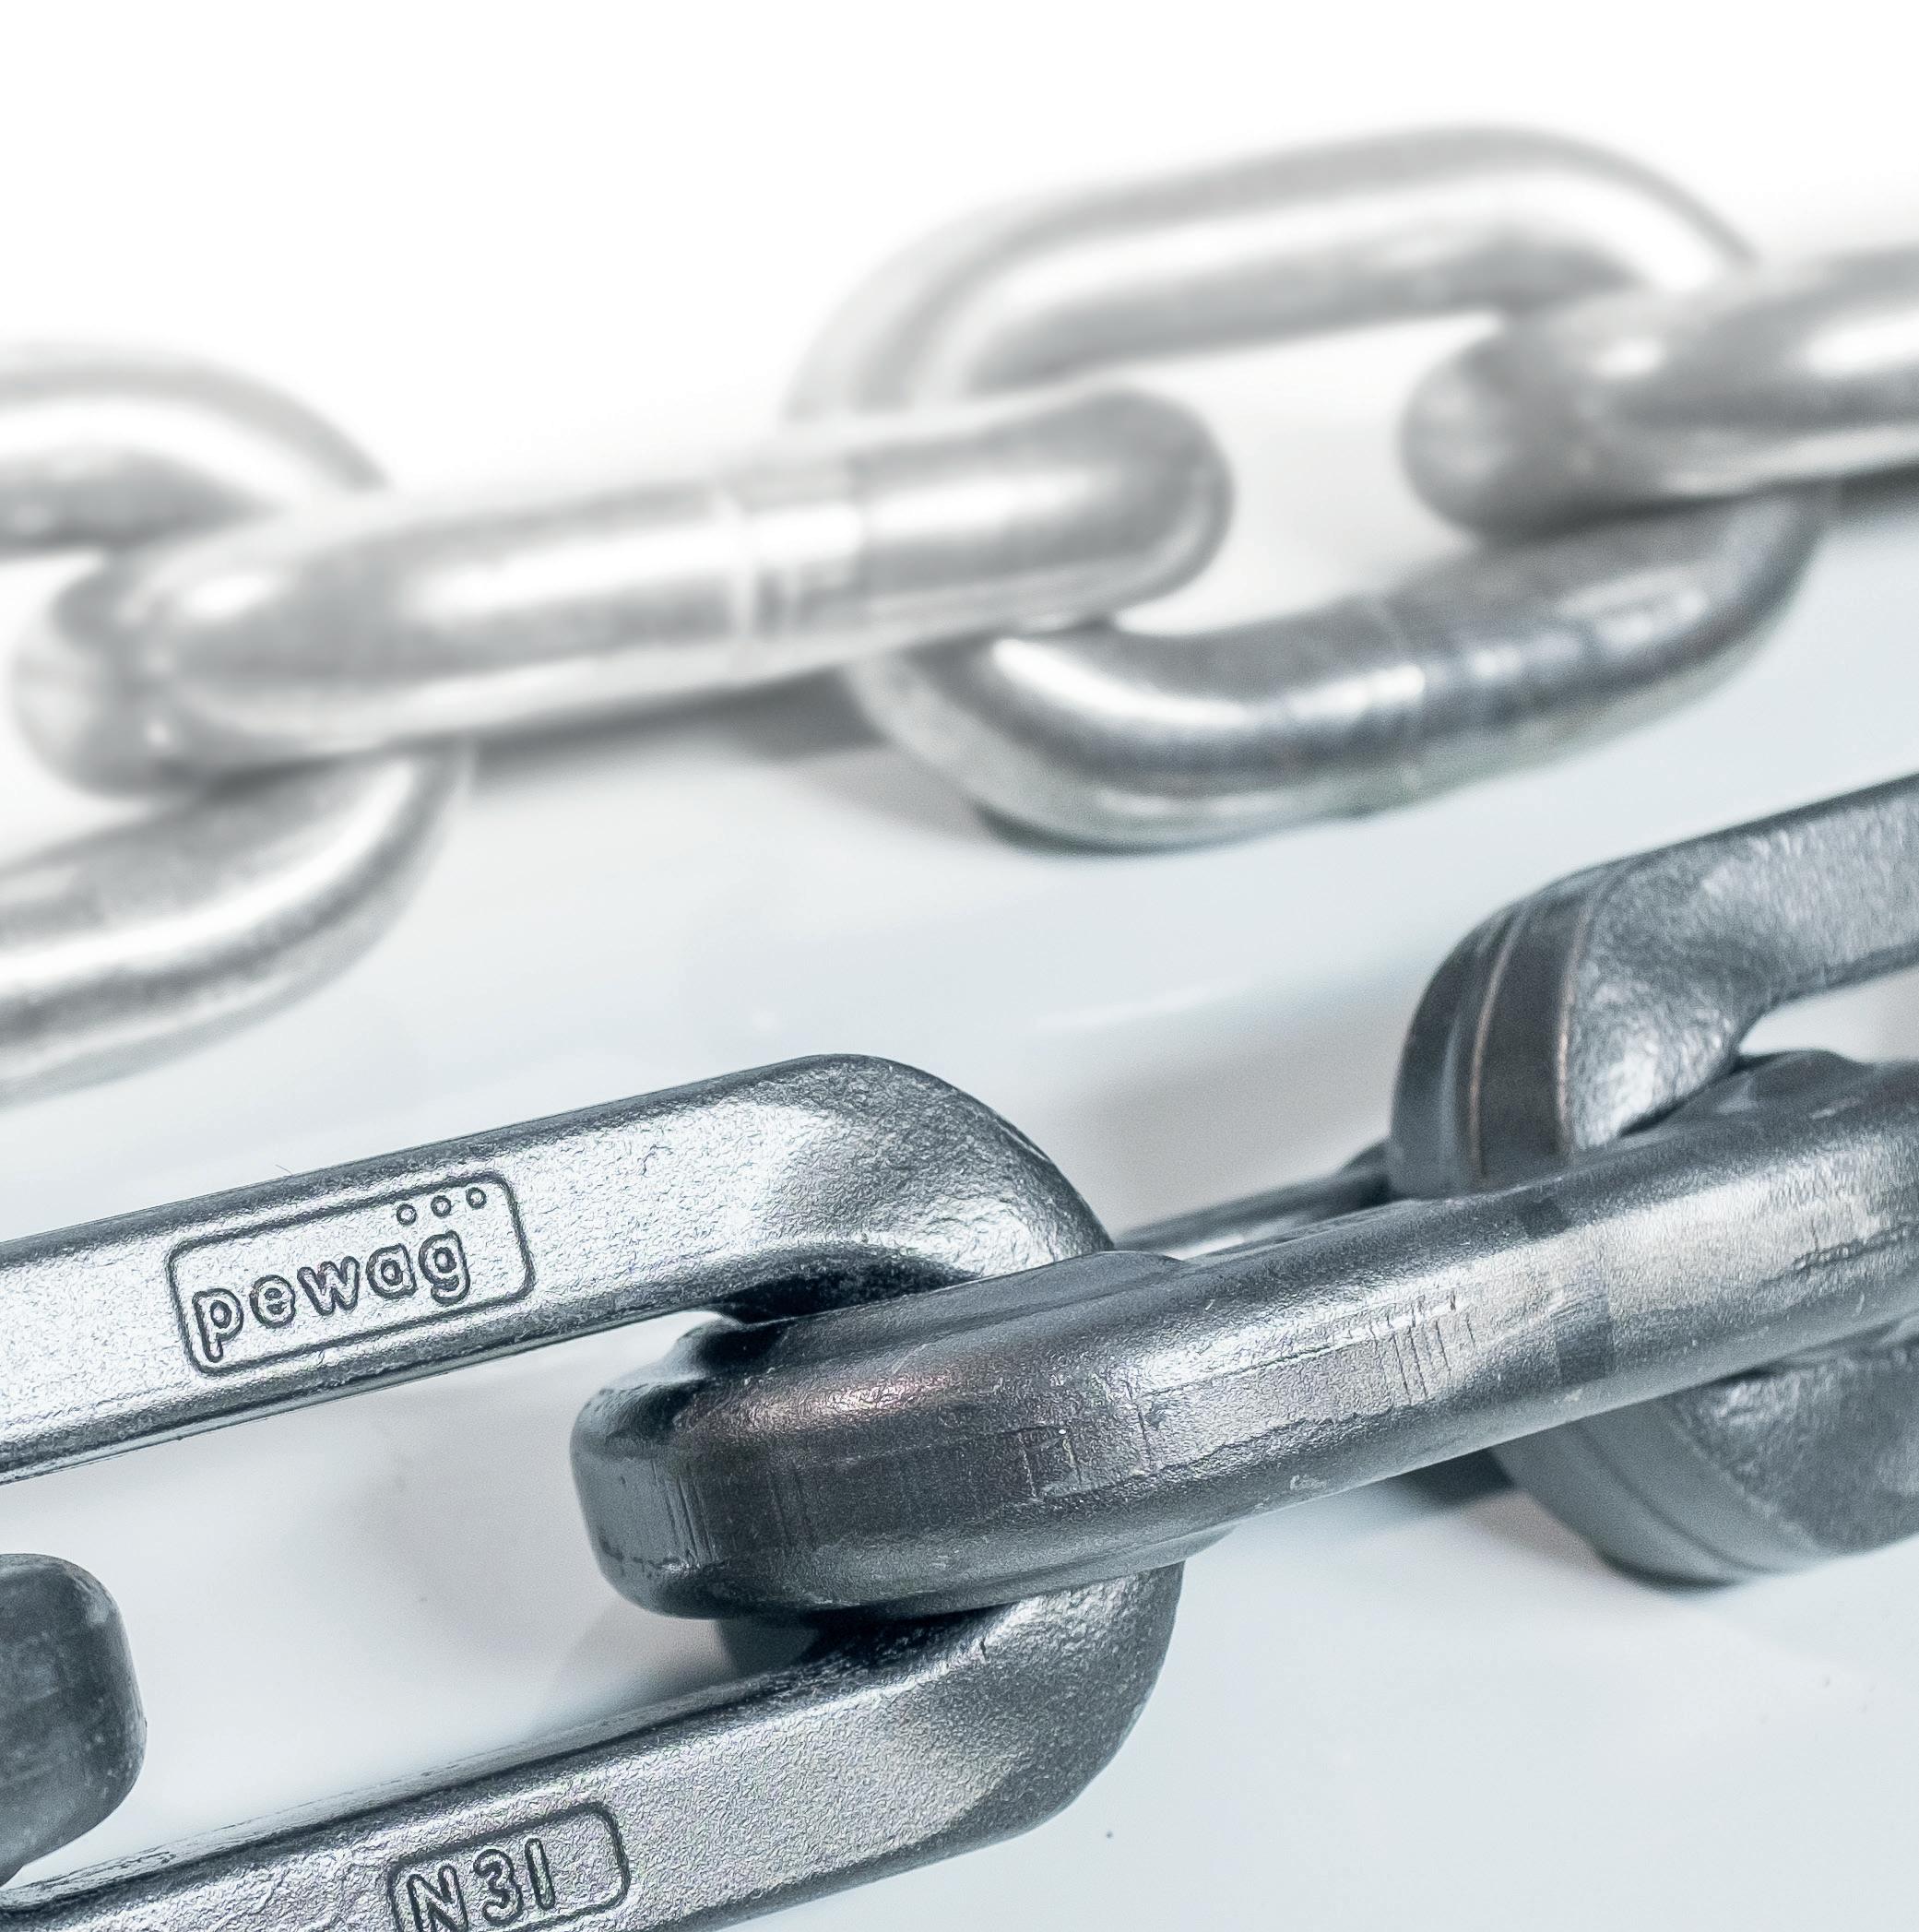
Friction-welded chains are produced from forged steel components, unlike round steel chains that start from drawn steel wire or rolled bars. The use of forged components offers the ability to increase the section modulus in areas of high stress or wear and eliminates the risk of tension cracks, which can occur during the bending process of round steel chains.
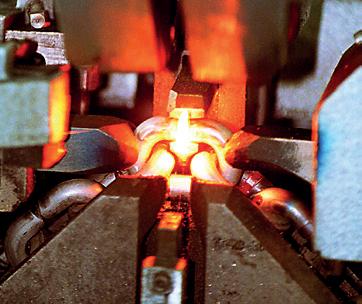
Friction welding is not a welding process in the traditional sense. Heat is generated through mechanical friction between the chain link components until the material plasticises. Lateral force is applied to exactly fuse the components to a whole chain link.
Melt-free technique
• no grain-growth
• very small heat-affected zone (near zero residual stresses)
Clean joining
• impurities between the contact surfaces are removed by the plasticised working mass and are forced out during the joining of the forged components.
No material limits
• even conventionally non-weldable steel grades, for example a 50 CrV4 steel which offers excellent wear resistance, can be joined
No shape limits
• every chain application has its special demands – the use of forged components can address critical factors like adding wear volume in the interlink section or legs of the link to drastically improve wear life of the chain
No pairing process needed
• due to the high production quality every strand has the same length with a very small tolerance.
• each strand with the same number of links can be installed parallel to each other.
• production tolerance of 0.05 % for matched chains.
Longer chain strands are possible
• because of the friction welding process, the pewag hero chain can be delivered with longer chain strands compared to conventional round link chains. For example, the standard length of pewag hero chain is double the standard length of round link chains.
Longer lifespan & easy change
• case hardened and in many different dimensions, the pewag hero is running over all different types of toothed and plain wheels, which are also used for round links chains. This has the advantage that changing from roundsteel chain to pewag hero chain – for example at existing installations – is quite easy and also cost effective.
• the bigger wear volume leads to a significantly longer lifespan compared to round steel chains.
• this results in: lower maintenance costs, lower operating cycles and lower downtime costs.
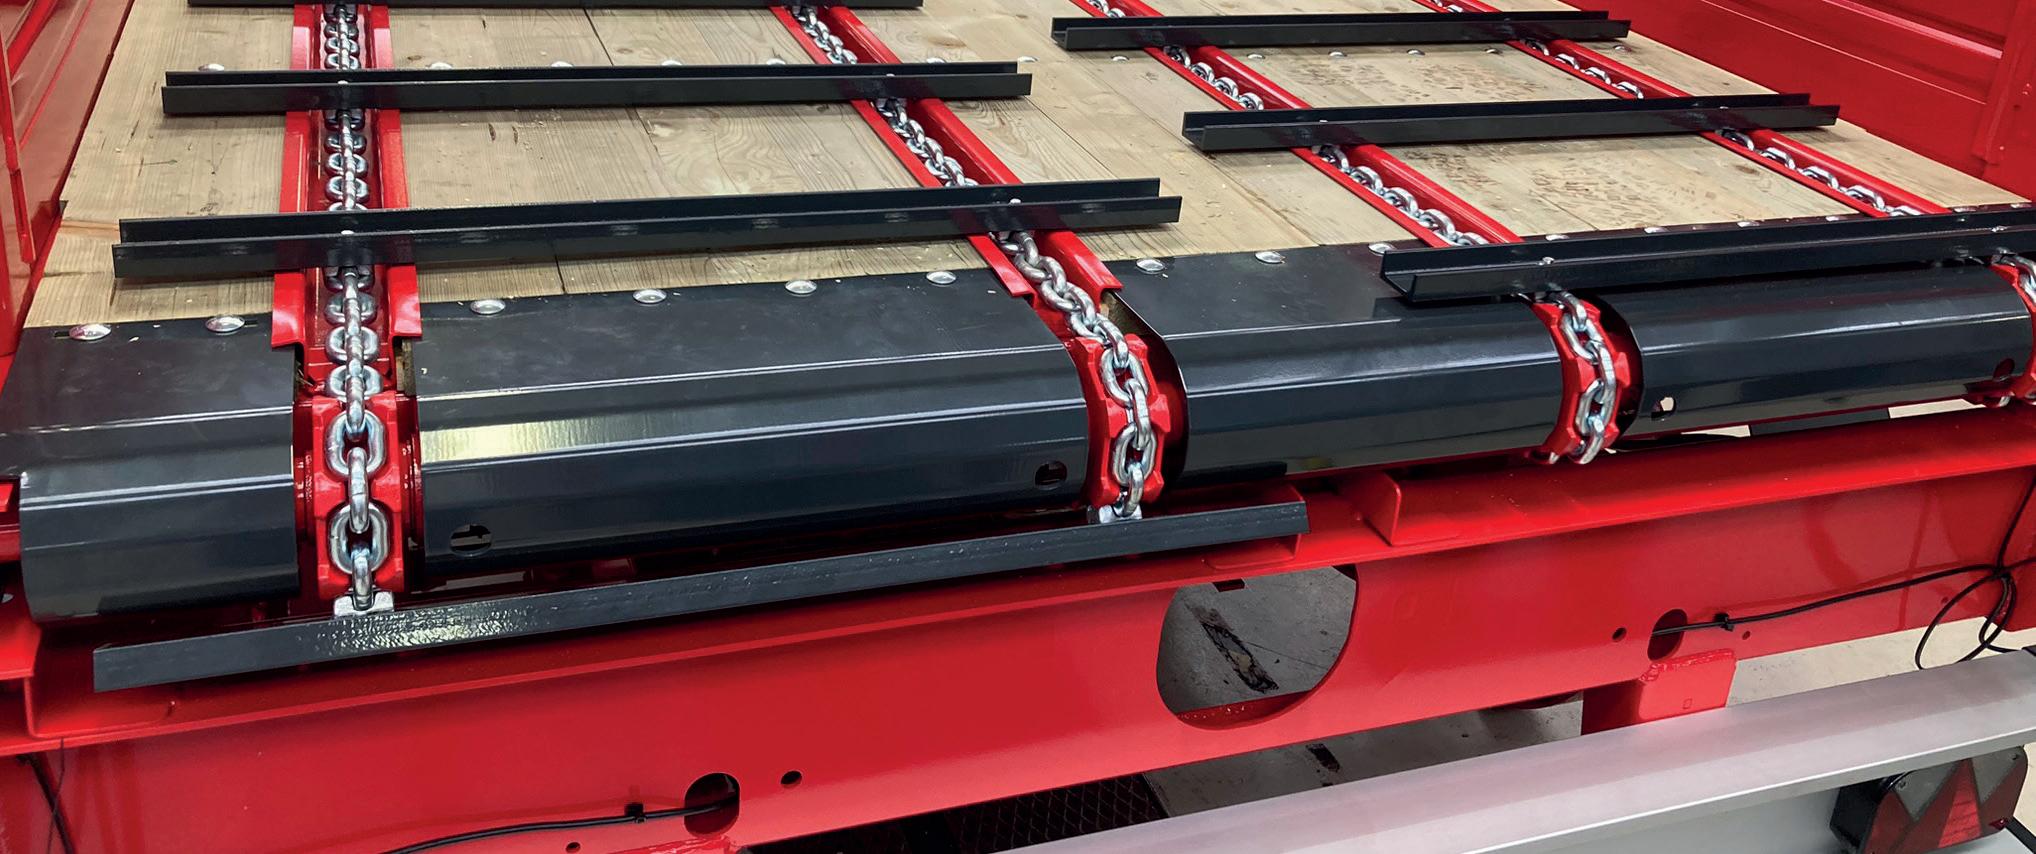
The friction welded pewag hero chain can be used for different applications such as conveyors or bucket elevators.
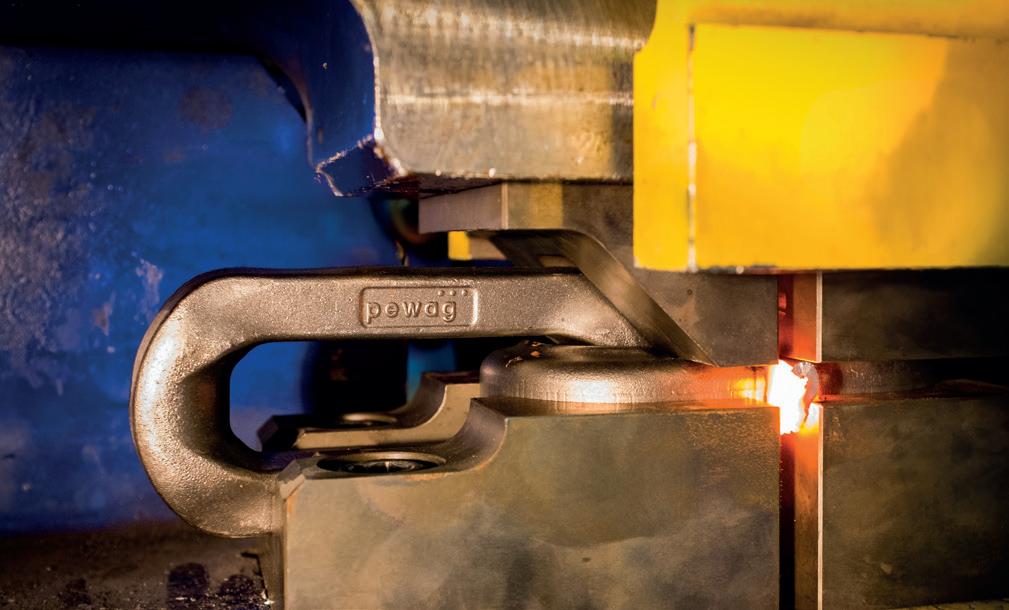
Friction welding is a tried-and-tested ‘joining technology’ that has been used by the aviation and automotive industries for decades. The method also allows for the joining of lightweight construction materials such as aluminium with high- strength steels.
With conventional welding techniques, the joining of materials with highly different welding points is not possible, which is why mechanical joining methods have to be applied to achieve this goal. With friction welding, such materials can be joined without any problems and without having to compromise when it comes to weld stability or having to accept a higher weight.
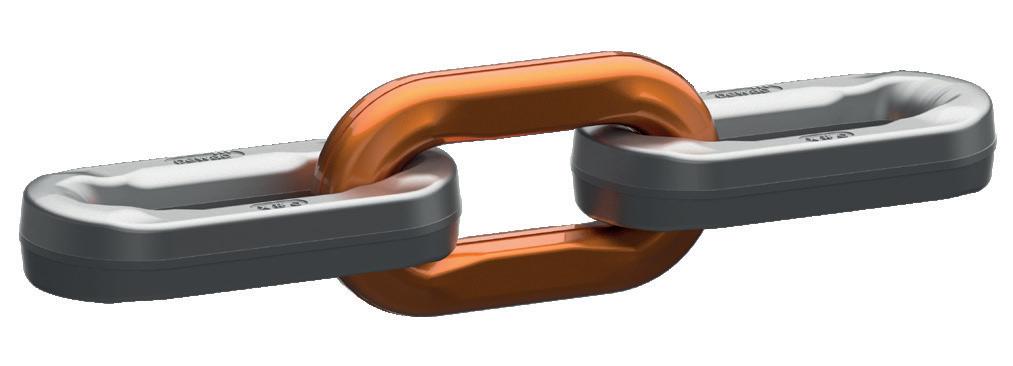
pewag is the first chain manufacturer worldwide to have taken up the innovative technology of friction welding and refined it for the manufacture of the next generation of chains. Unlike conventional round steel chains, the friction-welded chain does not start out as wire rod or rod steel, but consists exclusively of forged parts. By using forged components, the risk of tension cracks, which are a typical byproduct of the cold-bending process of round steel chains, is eliminated. As such, friction welding is not a conventional welding technique. In friction welding, heat is generated through mechanical friction between the links to be joined, which causes the material to plasticise.
A defined lateral force is applied to fuse the components to a whole chain link with precise pitch and strand lengths therefore the pairing operation is no longer required.
Compared to round steel chains, the pewag hero chains offer the following advantages thanks to their design.
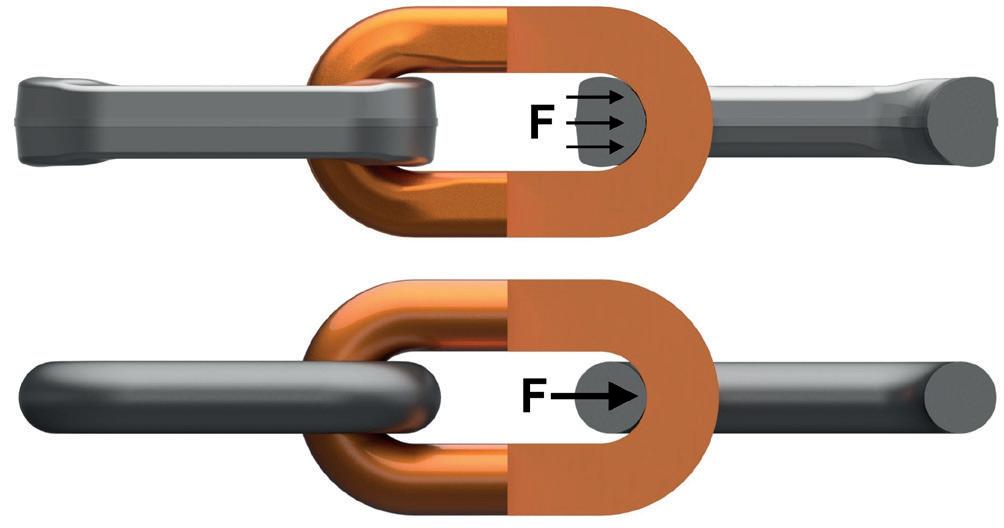
The load-specific geometry of the pewag hero chain has an increased interlink contact area and more than twice the wear volume of a conventional chain. This leads to significantly reduced contact and maximum stress, better performance and an approximately 30 % longer lifespan.
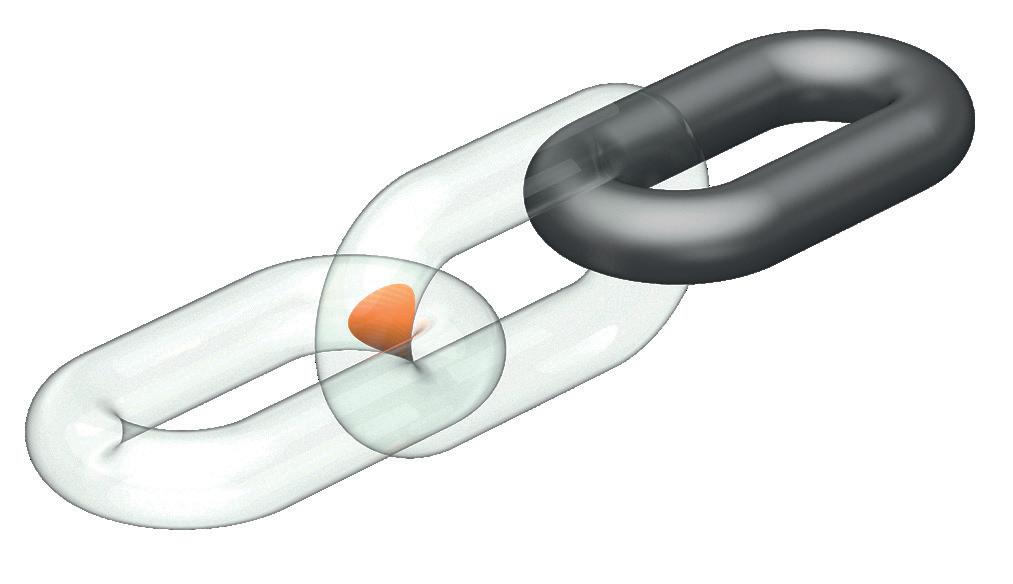
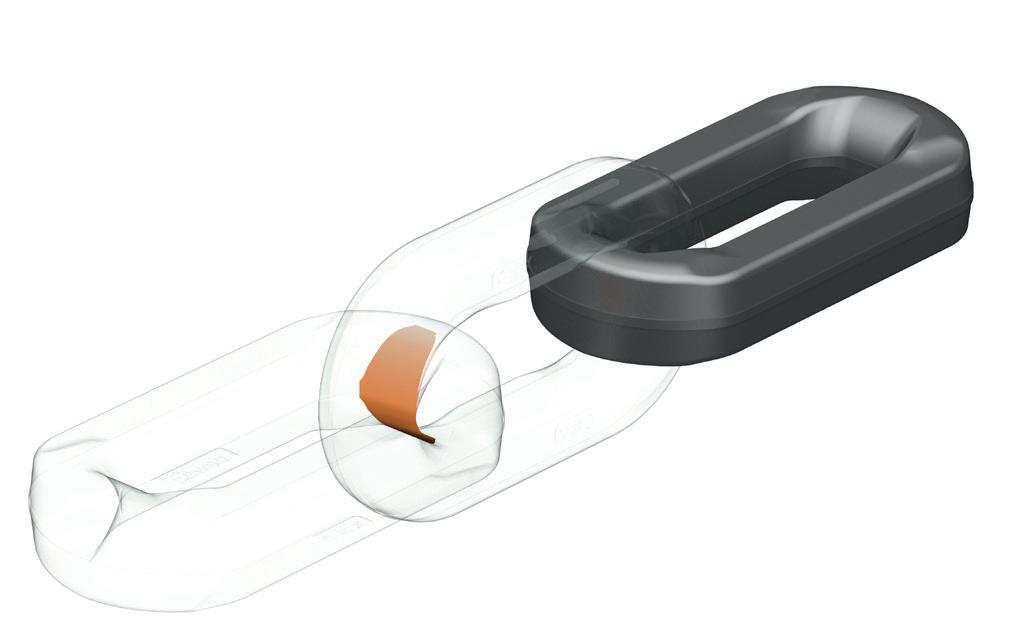
The geometry of traditional round steel chains provides a small interlink contact area and subsequent high stresses
• evenly distributed force
• less force per mm2
• lower maintenance cost • longer operating cycles
• lower downtime cost
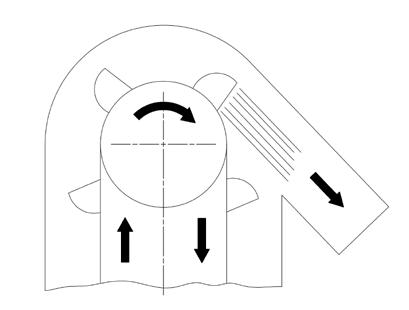
Our bucket elevator configurator supports you in selecting the ideal system for your individual conveying requirements. Depending on the discharge method, bucket elevators can be configured for centrifugal or gravity discharge applications. Gravity discharge systems are designed for lower operating speeds and feature laterally mounted buckets, while centrifugal discharge systems offer greater flexibility in bucket mounting options.
A range of chain system solutions is available to suit different operating conditions. Customers can select between chain strand or chain end designs as well as suitable sprocket and bucket attachments configurations, ensuring reliable operation, efficient power transmission, and durable performance for a wide variety of bulk material handling applications.
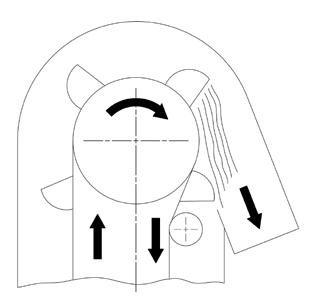
Bucket elevators are the backbone of vertical conveying. They operate under high tensile loads while ensuring smooth bucket guidance and accurate discharge at every cycle. Chain performance directly influences plant availability and maintenance intervals.
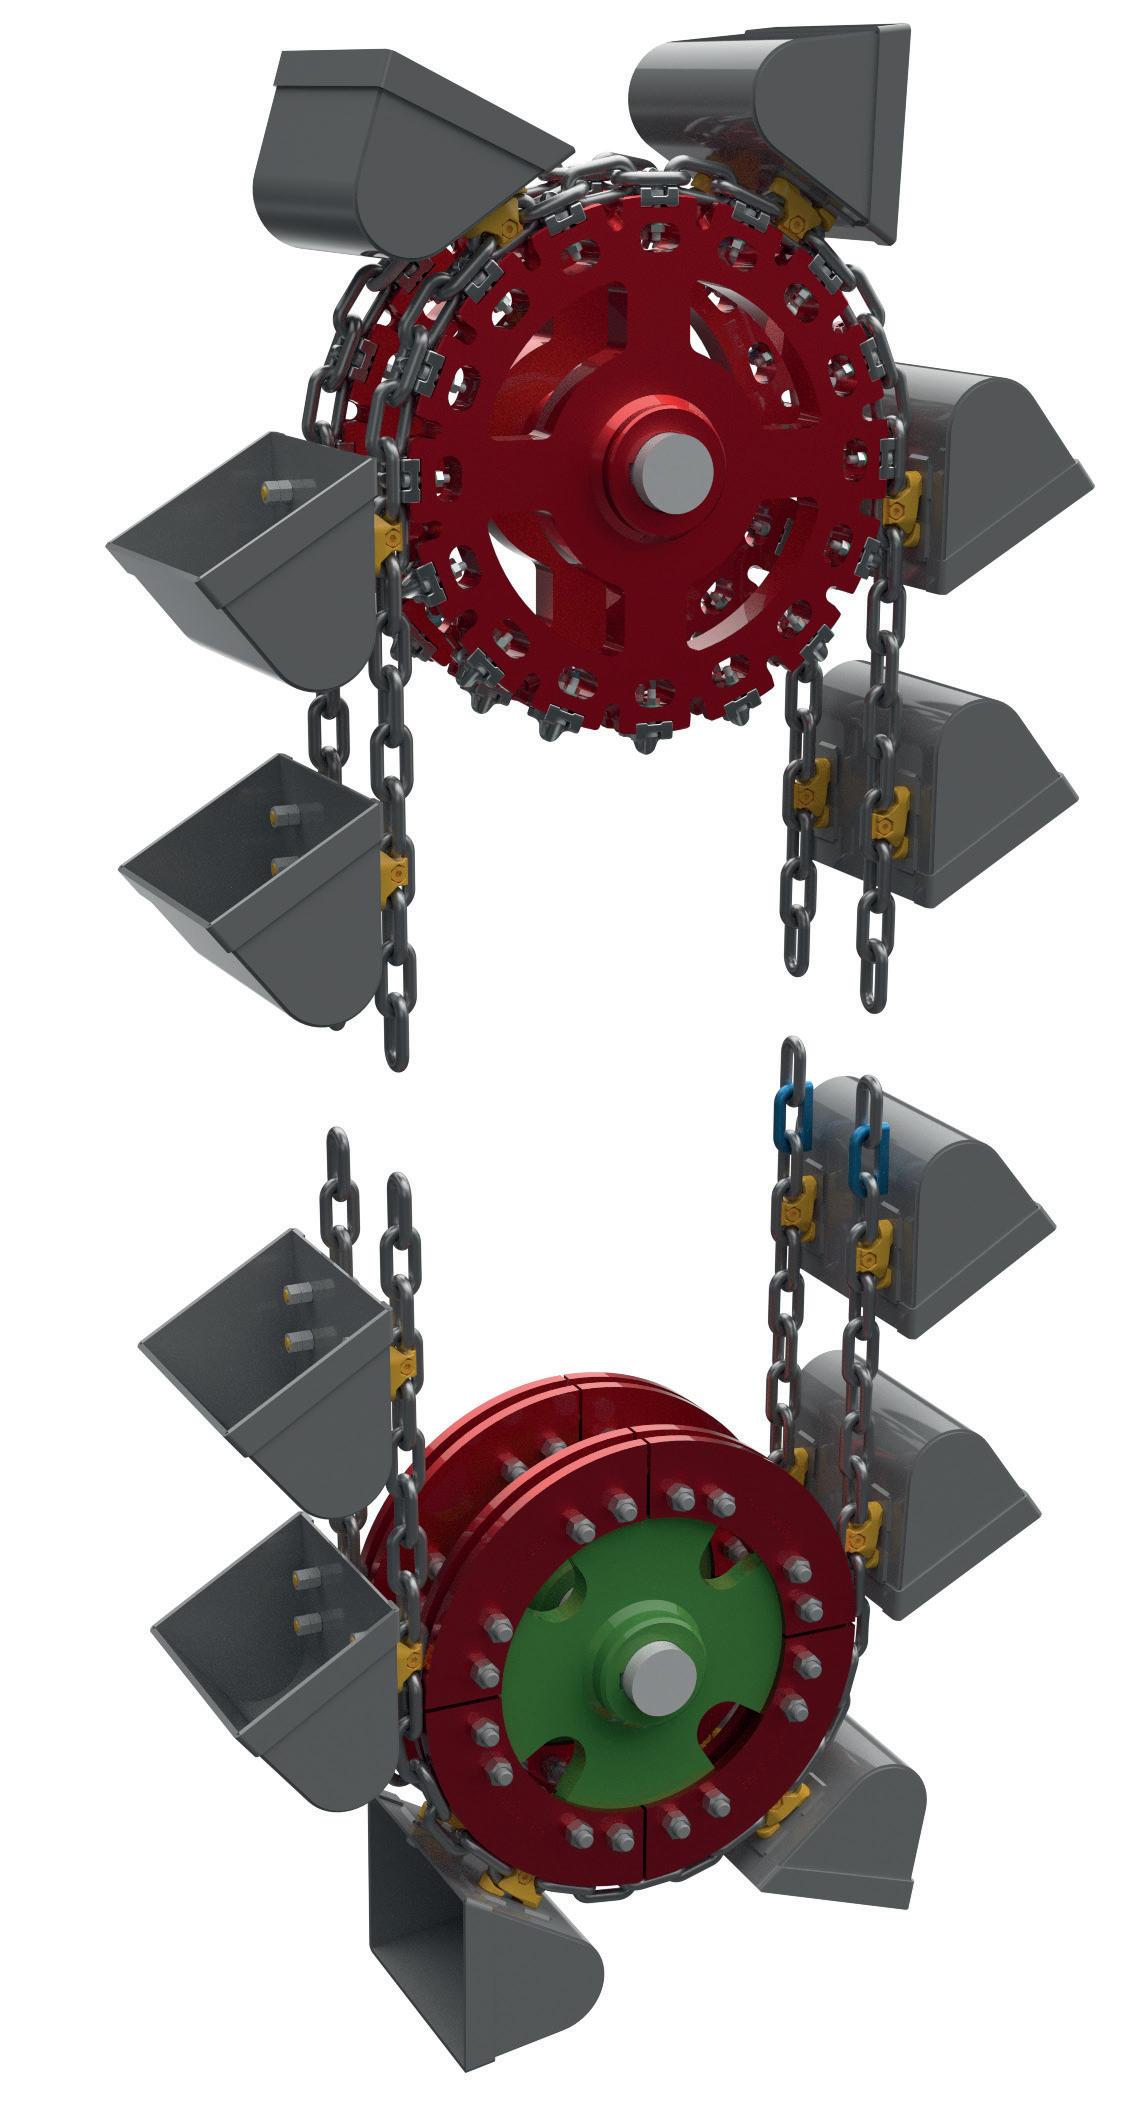
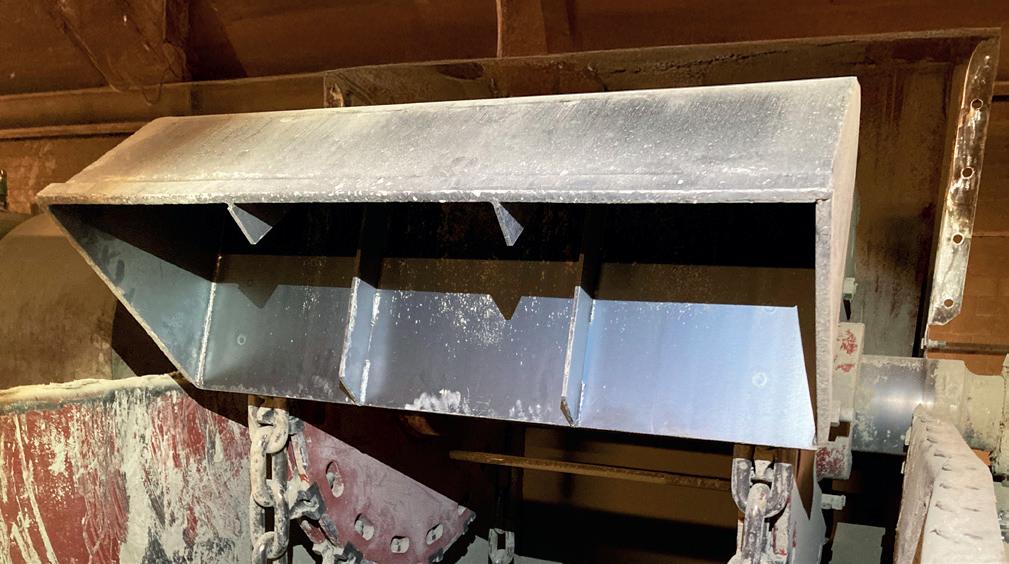
Pewag offers a complete portfolio of chain solutions for bucket elevators, including precision-manufactured friction welded and round steel chains built for strength, dimensional accuracy, and extended lifetime. Our systems prove themselves every day in heavy-duty environments such as cement, fertilizer, and plaster.
From individual components to coordinated chain assemblies, we provide everything required for reliable, continuous vertical transport.
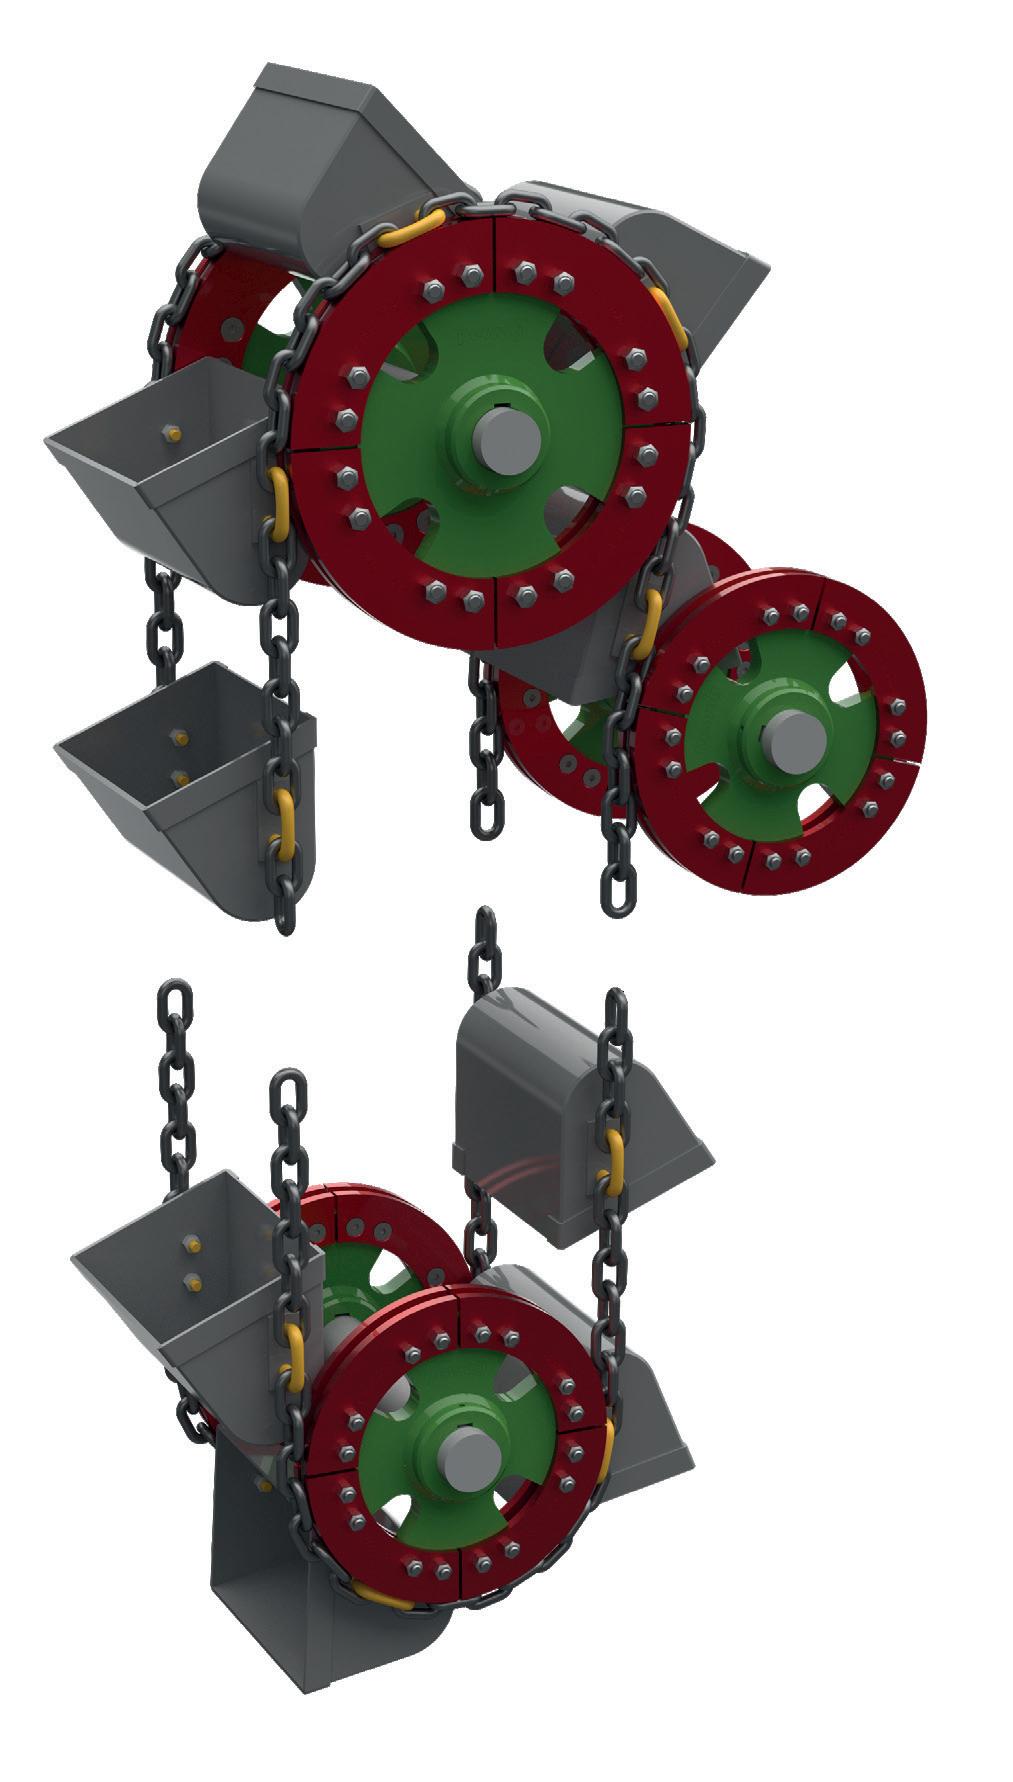
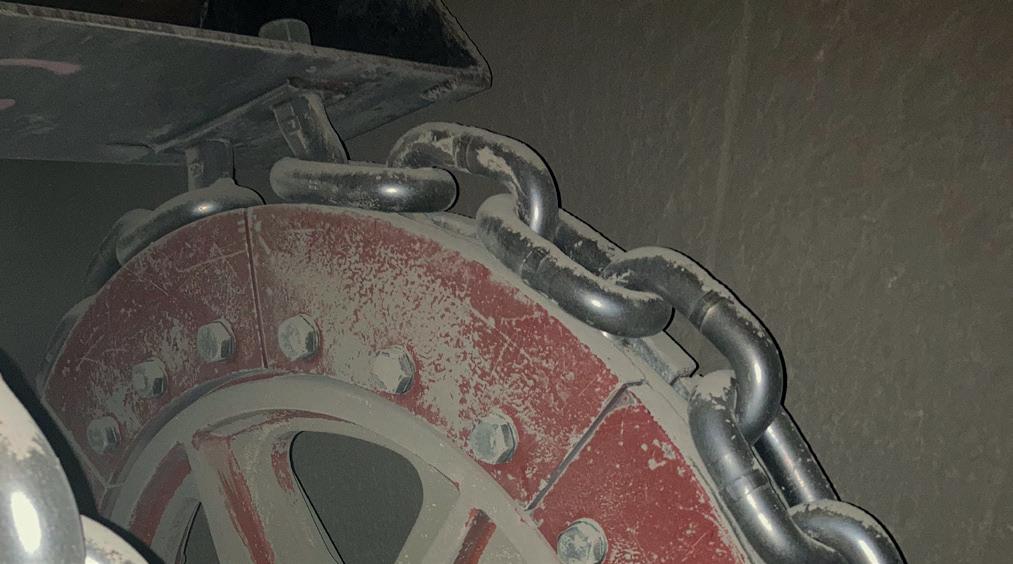
In scraper conveyors, bulk material is moved continuously over long horizontal or slightly inclined distances. The chain is permanently exposed to abrasive fines, high drag forces, and demanding operating conditions – reliability is crucial to prevent unplanned downtime.
pewag supplies robust conveyor chains and components specifically developed for scraper applications. Our friction welded and round steel chains provide high wear resistance, excellent fatigue strength, and long service life in industries such as mining, agriculture and power generation. Whether you require replacement parts or a perfectly matched system, we deliver solutions that keep your material moving efficiently.
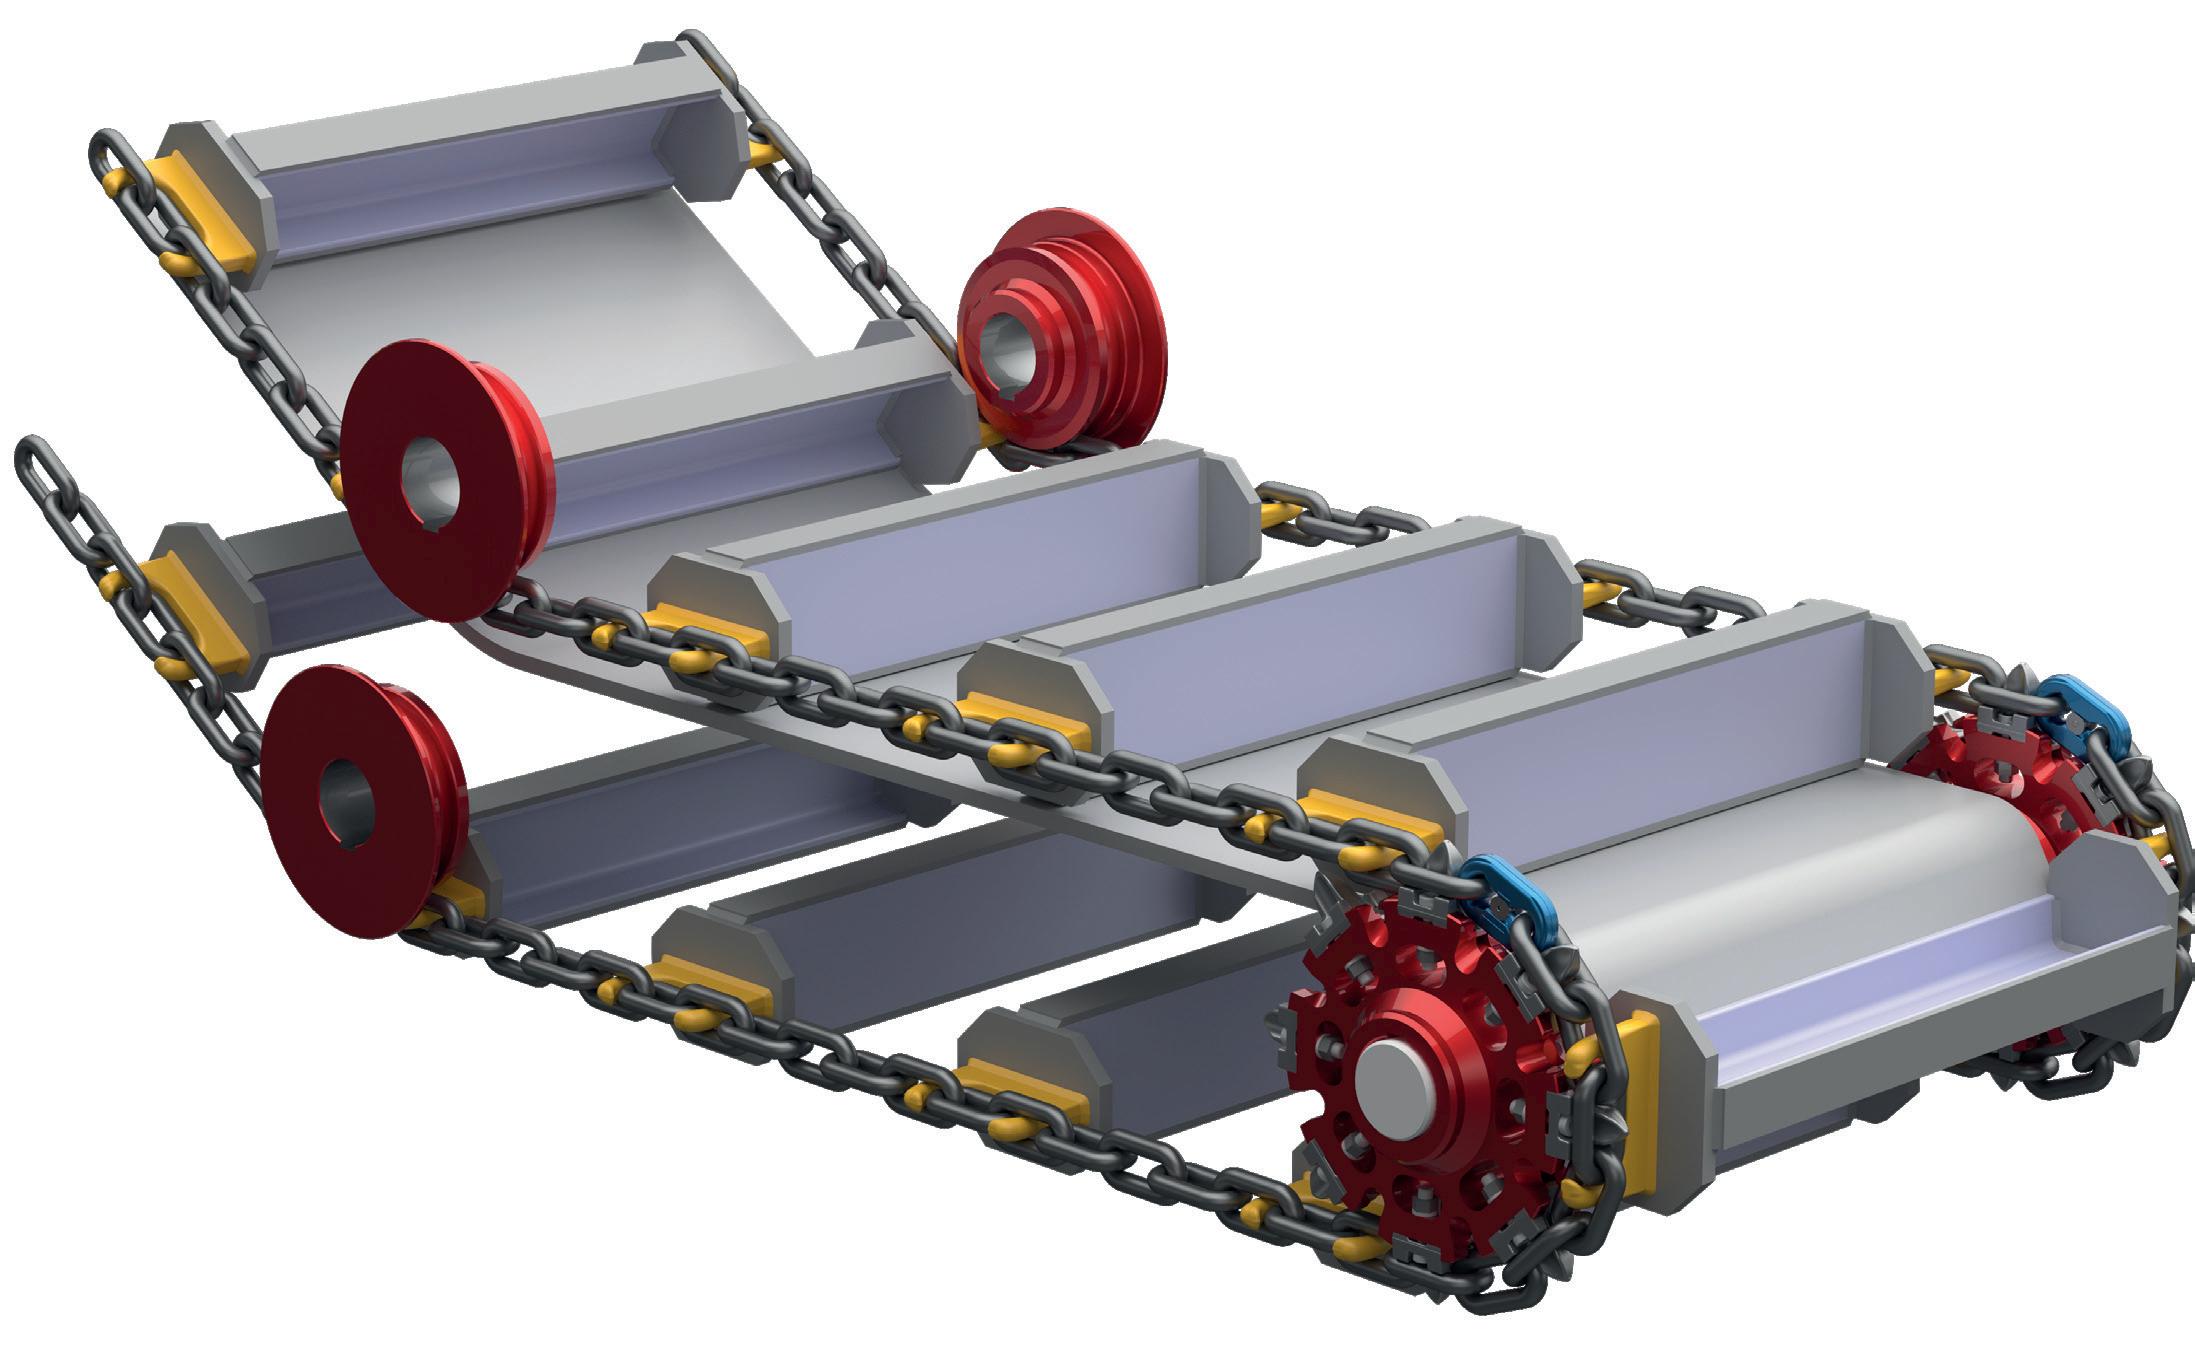
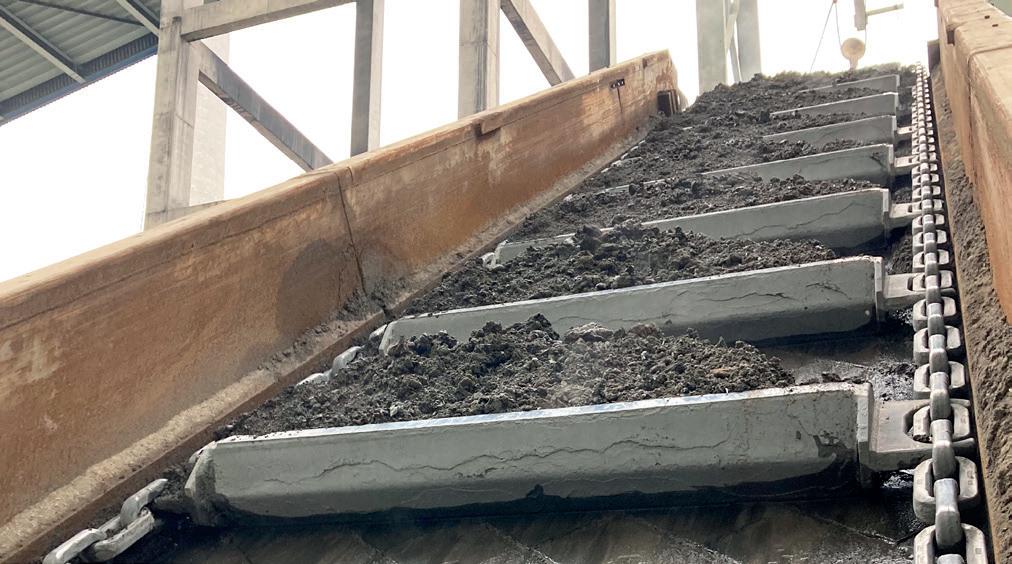
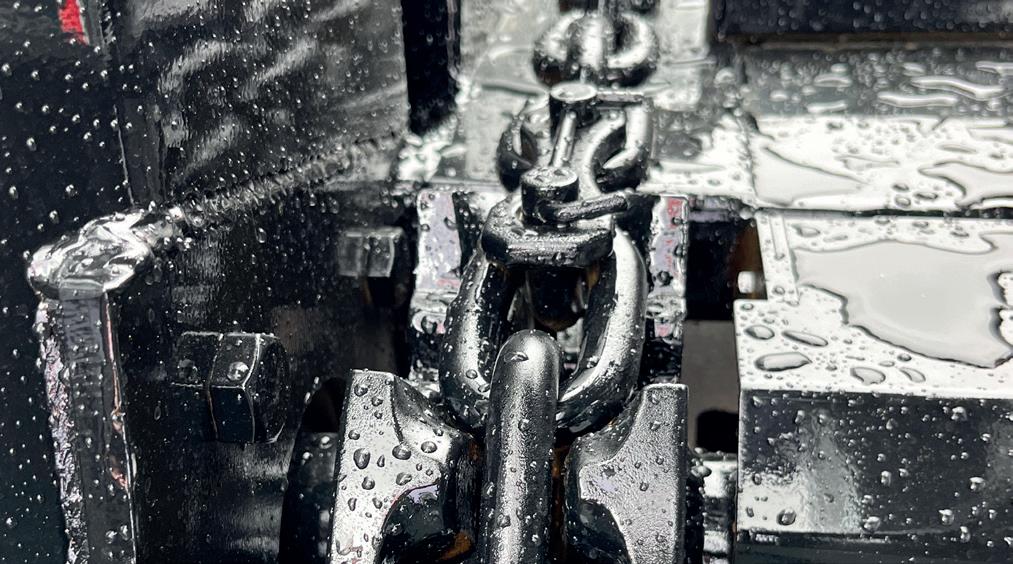
pewag conveyor chains are made from fine-grained, nonageing special CrNi-, CrNiMo-, MnCr-alloyed steel. By ensuring optimum heat treatment pewag maintains high quality standards.
pewag conveyor chains have consistently high core quality which gives resistance to shock loadings and ensures maximum breaking loads and excellent fatigue strength can be achieved.
Case hardened conveyor chains can be used for operating temperatures of up to 200 °C (392 °F) without loss of surface hardness.
The chains are manufactured with very close production tolerances to ensure a smooth, parallel run over the sprockets. All round steel chains and components are matched in terms of strength and uniform hardness, to minimize the wear and provide the greatest possible wear life and maximum chain life, to guarantee a long lasting chain system.
An extensive range of pewag conveyor chains up to 38 mm, chain connecting links, chain sprockets, guide wheels, flight bars with flight attachments provide the optimum design for bucket and scraper conveyors in the bulk industry.
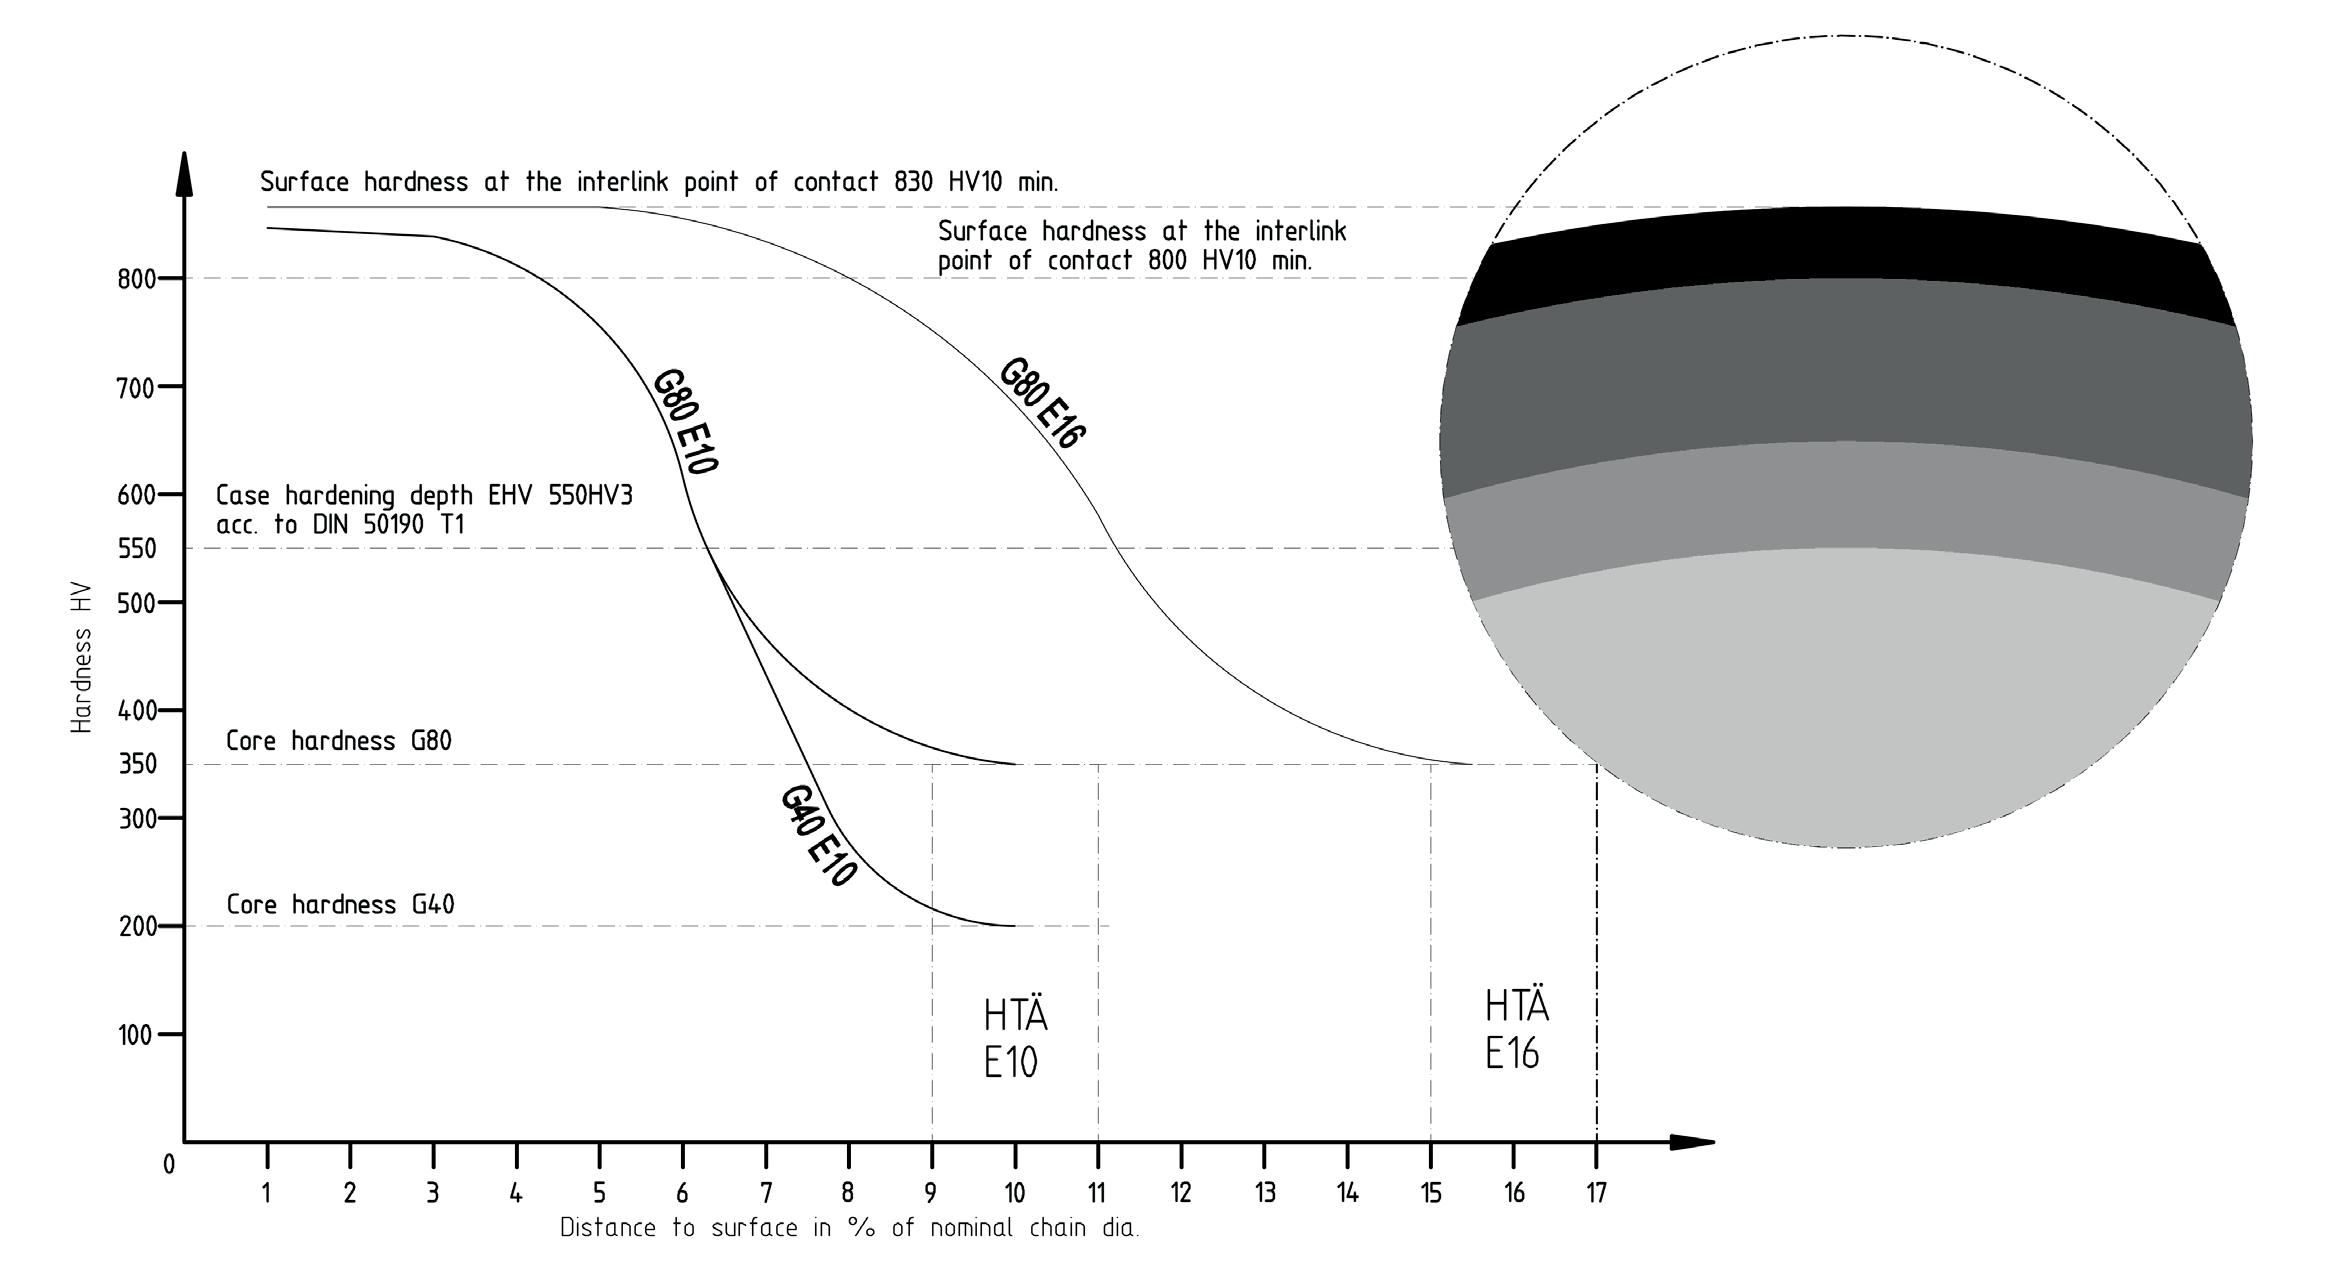
Quality grade G80 E10
Carburizing depth E10
Quality grade G80 E16
Carburizing depth E16 = 0,10 x chain diameter = 0,16 x chain diameter
*All standard components (except for SDS and SDD) and chain wheels are compatible with hero and round steel chains. Upon request, we offer special versions of SDS and SDD attachments for hero chains.
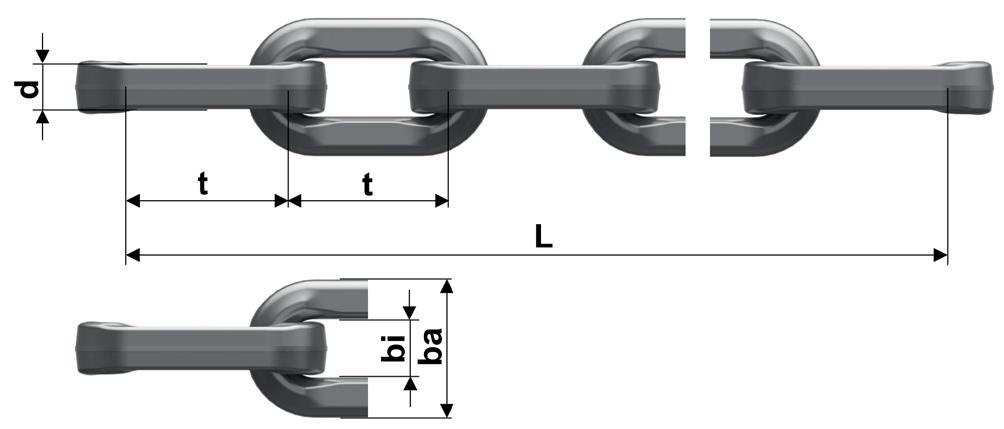
pewag hero – chains are made from CrNiMo-special alloyed steel and are suitable for high-capacity bucket elevators and scraper conveyors with high dynamic and static loads. The combination of increased wear volume and reduced surface pressure results in a significant increase of the chain life of approx. 30 %. The pewag hero chain fits on conventional wheels and sprockets. Pairing is not required due to the high manufacturing precision.
26
Technical data
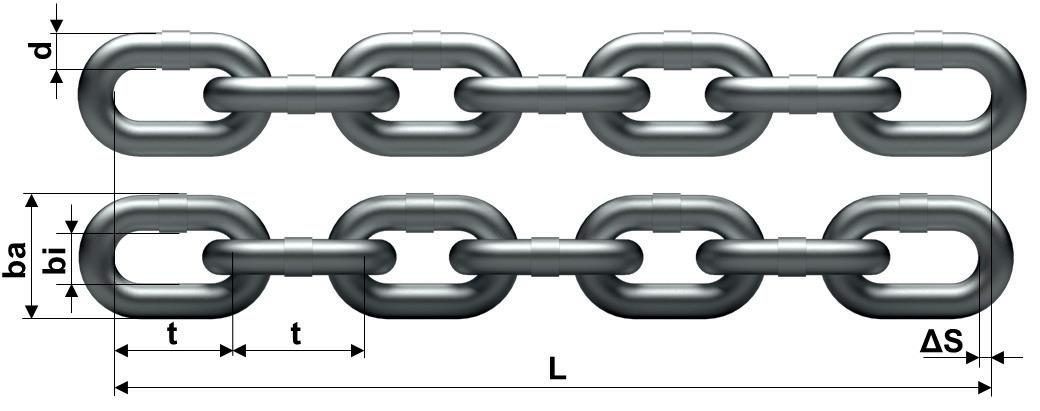
Chain length "L" production tolerance = +0,3 / -0,15 % = 0,45 % total; this means that the difference between chain lengths of 10 m is max. 45 mm. Chain length production tolerance Δ S of matched chain lengths is 0,05 % or max. 3 mm for two or multiple chain strand conveyors.
Example of the order
16 pcs. pewag hero 22x 86 6580 G80 E BK L= 239 links = 20.554 mm supplied as matched pairs.
Surface hardness [HV 10]1) / inner link curve min. 800
Core hardness [HV]
ca. 300
Surface blank, shot peened, waxed
Marking batch number on the forgings
Chain length production tolerance
Chain length "L"
0,05 % for matched chains, double and multiple chain strand conveyors
Remark manufactured of forgings in friction welding process
pewag hero-V – chains are made from CrNiMo-special alloyed steel and are suitable for different applications. The reduced surface pressure results in a significant increase of the chain load capacity.
The pewag hero chain fits on conventional wheels and sprockets. Pairing is not required due to the high manufacturing precision.
Technical data
Chain length "L" production tolerance = +0,3 / -0,15 % = 0,45 % total; this means that the difference between chain lengths of 10 m is max. 45 mm. Chain length production tolerance Δ S of matched chain lengths is 0,05 % or max. 3 mm for two or multiple chain strand conveyors.
Example of the order 16 pcs. pewag hero-V 22x 86 6580 BK L= 239 links = 20.554 mm supplied as matched pairs.
Surface hardness [HV 10]1) / inner link curve
Surface blank, shot peened, waxed
Marking batch number on the forgings
Chain length production tolerance 0,05 % for matched chains, double and multiple chain strand conveyors
Chain length "L" production tolerance +0,30 / -0,15 % = 0,45 %
Remark manufactured of forgings in friction welding process
Round steel chains made from CrNi or CrNiMo special alloy steels are designed for use in bucket and scraper conveyors operating under high dynamic and static loads. They are supplied as matched pairs to ensure precise parallel alignment of the chain links.
Surface finish: polished and waxed
Further dimensions and qualities on request.
0,16 3)
Case hardening depth EHT 550 HV 3 ... d min. 0,063 4) 0,06 5) 0,11 6)
Material incl. d = 22 mm: CrNi-alloyed
Material from d = 26 mm: CrNiMo-alloyed -
Proof/Breaking load tolerance -10 % permissible depending on the batches
Stress at breaking force [N/mm2]:
* 14 Ø, 16 Ø, 19 Ø – 420; 22 Ø, 26 Ø, 30 Ø - 400; 34 Ø, 38 Ø - 370
Stress at manuf. test force [N/mm2]:
** 14 Ø, 16 Ø, 19 Ø – 210; 22 Ø, 26 Ø, 30 Ø - 250; 34 Ø, 38 Ø - 230
Carburizing depth HTÄ after macroetching:
1) 30 Ø, 34 Ø - 0,09 d;
2) 30 Ø, 34 Ø - 0,09 d; 38 Ø - 0,08 d
3) 14 Ø, 16 Ø, 19 Ø, 22 Ø, 26 Ø - 0,16 d; 30 Ø - 0,14 d; 34 Ø – 0,13d
38 Ø – 0,12d
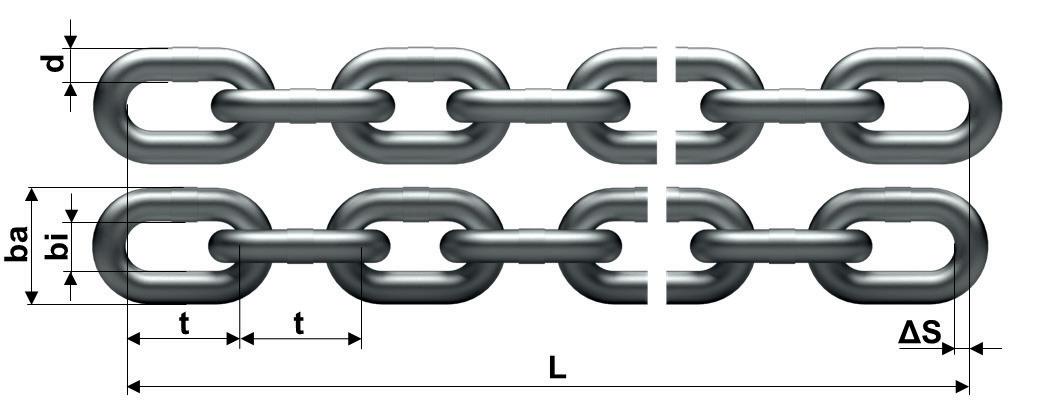
• Chain length "L" production tolerance = +0,3 / -0,15 % = 0,45 % total; this means that the difference between chain lengths of 10 m is max. 45 mm.
• Chain length production tolerance Δ S of matched chain lengths is 0,05 % or max. 3 mm for two or multiple chain strand conveyors
• G40 E10 grade chains can only be used with non-toothed systems.
Case hardening depth EHT 550 HV 3: 4) 30 Ø, 34 Ø - 0,05 d; 5) 30 Ø, 34 Ø - 0,05 d; 38 Ø - 0,04 d 6) 14 Ø, 16 Ø, 19 Ø, 22 Ø, 26 Ø - 0,11 d; 30 Ø 34 Ø - 0,09 d; 38 Ø - 0,08 d
Round steel chains for conveyors with low conveying capacities and service hours, e.g. agricultural applications or cleaning scraper conveyors under belt conveyors etc;
Surface finish: up to chain diameter 11 mm natural blackoiled, polished and waxed or as specified by the customer.
16 x
Further dimensions and qualities on request. Upon request, we can also manufacture round steel chains according to customer specifications: dimensions and quality grade.
Technical Datas
• Chain length "L" production tolerance = +0,3 / -0,15 % = 0,45 % total; this means that the difference between chain lengths of 10 m is max. 45 mm.
• Chain length production tolerance Δ S of matched chain lengths is 0,05 % or max. 3 mm for two or multiple chain strand conveyors.
• Chain length tolerance Δ S of matched chain ends max. 0,5 mm.
of the order
Chain ends made from Mn-, MnCr-, or CrNi-alloyed steel are designed for use in DIN bucket elevators with chain shackles or in scraper conveyors with BM attachments. The chain ends are connected to the next larger pitch chain shackle for use in friction drive systems.
Surface finish: polished and waxed
Available lengths: 5, 7, 9, 11, or 13 chain links
Further dimensions and qualities on request.
1) Recommended chain shackle acc. to DIN for wheels.
Breaking stress [N/mm2]
Proof stress [N/mm2] 125 210
Breaking elongation approx. [%] 2 2
Surface hardness at interlink HV 10 750 750
Carburizing depth HTÄ ... d +/- 0,01d 0,10 1) 0,10 1)
Case hardening depth EHT 550 HV 3 ... d min. 0,06 2) 0,06 2)
Material incl. d = 22 mm: CrNi-alloyed
Material from d = 26 mm: CrNiMo-alloyed - -
Proof/Breaking load tolerance -10 % permissible depending on the batches
Technical Datas
• Tolerance type A: calibrated, as matched chain ends, for chain sprockets
• Tolerance type B: non-calibrated, as matched chain ends, for plain chain wheels
• Chain length tolerance Δ S of matched chain ends max. 0,5 mm
Carburizing depth HTÄ after macroetching: 1) 30 ø –36 ø – 0,09 d
Case hardening depth EHT 550 HV 3: 2) 30 – 36 ø – 0,05 d
Chain ends made from Mn-, MnCr-, or CrNi-alloyed steel are designed for use in DIN bucket elevators with chain shackles or in scraper conveyors with BM attachments. The chain ends are connected to the next larger pitch chain shackle for use in friction drive systems.
Surface finish: polished and waxed Available lengths: 5, 7, 9, 11, or 13 chain links
Further dimensions and qualities on request. 1) Recommended chain shackle acc. to DIN for wheels.
Breaking
Proof stress [N/mm2]
Material incl. d = 22 mm: CrNi-alloyed
Material from d = 26 mm: CrNiMo-alloyed
Proof/Breaking load tolerance -10 % permissible depending on the batches
Technical Datas
• Tolerance type A: calibrated, as matched chain ends, for chain sprockets
• Tolerance type B: non-calibrated, as matched chain ends, for plain chain wheels
• Chain length tolerance Δ S of matched chain ends max. 0,5 mm Carburizing depth HTÄ after macroetching:
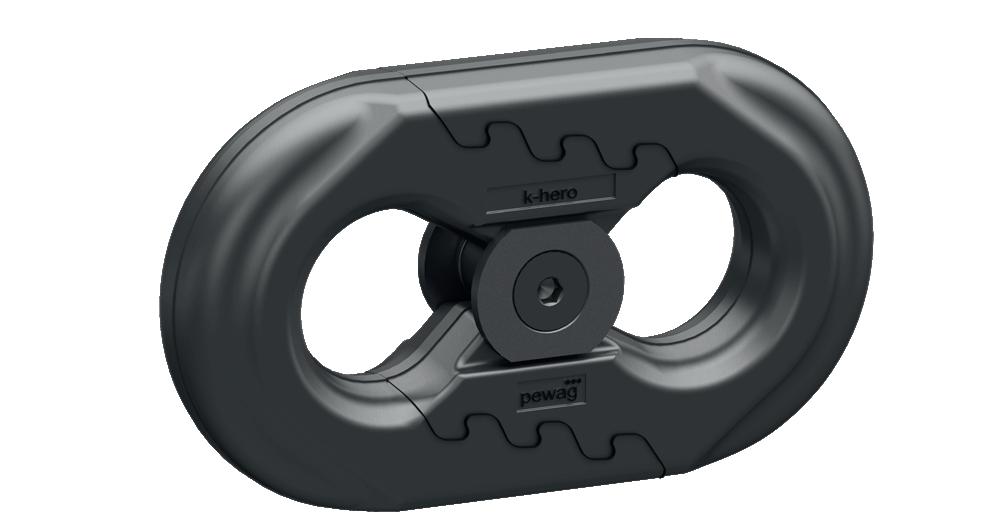
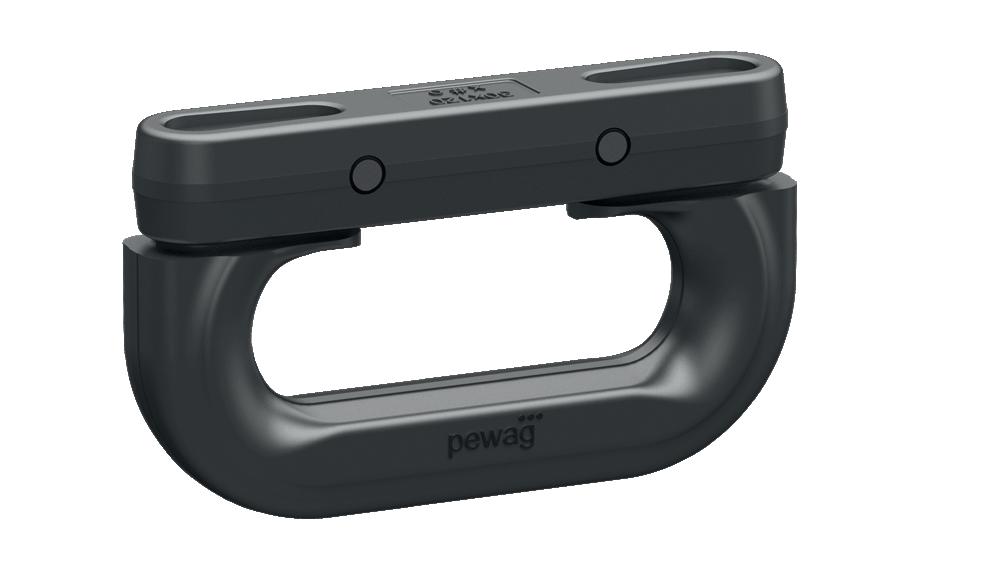
K-series connecting links are designed for use with round steel and hero chains. They share the same advanced technological features and high wear resistance as the corresponding chains. Please ensure that the couplings are assembled and installed according to the instructions provided in the packaging. These couplings are intended for use as vertical links only and can operate over sprockets, as well as over plain or grooved wheels.
Surface finish: sandblasted and waxed
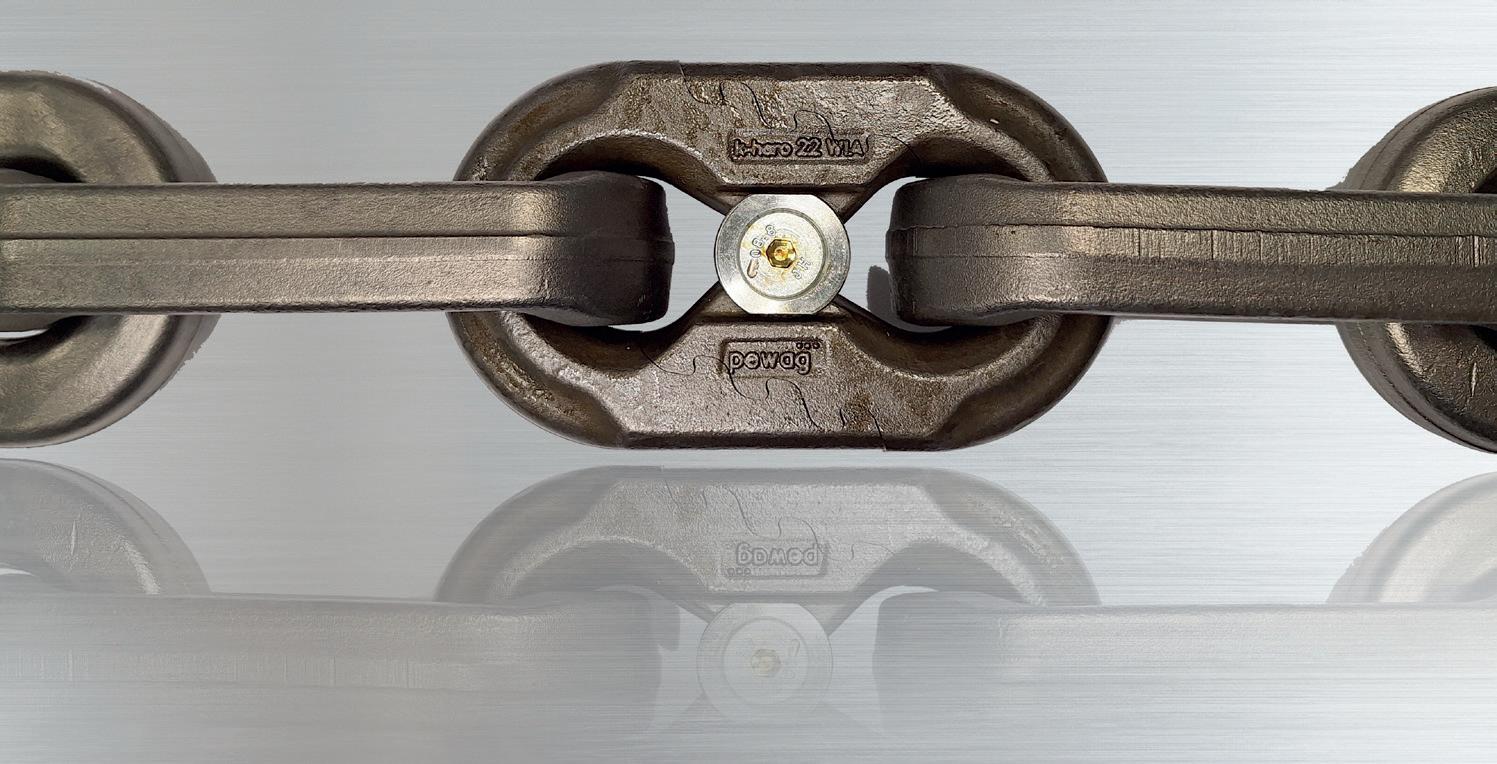
V-series connecting links are designed for use with round and hero chains. They share the same advanced technological characteristics and high wear resistance as the corresponding chains. Please ensure that the connecting links are assembled and installed in accordance with the provided instructions. These connecting links are used as vertical links in bucket elevators with back-mounted buckets. For positive discharge bucket elevators, the connecting links must be installed as horizontal links.
Surface finish: sandblasted and waxed
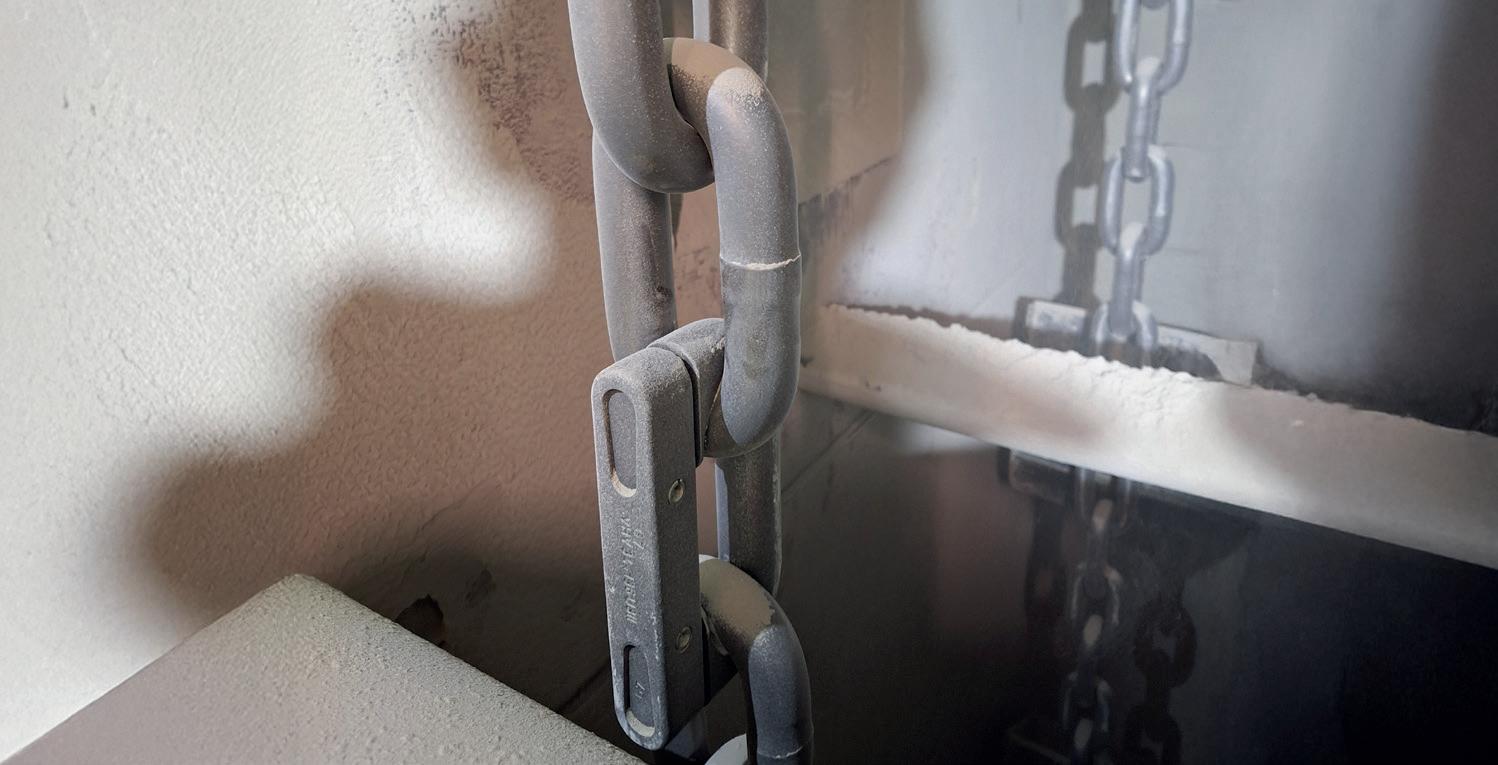
Connecting links with closing plate and locking pin are designed for use with factory-standard chains and operate over pocket wheels as vertically mounted chain links. They provide the same breaking load as the corresponding G80-grade chains.
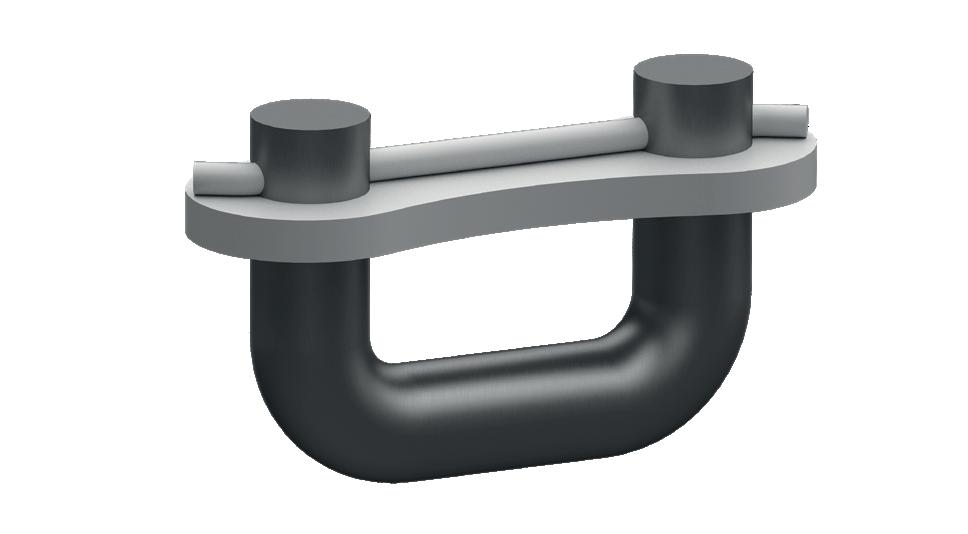
Any other sizes on request.
Scope of delivery
• Connecting link
• 1 pcs. closing plate
• 1 pcs. locking pin
Connecting link for chains; run over sprockets and/or pocket wheels depending on the chain pitch; recommended assembly as vertical mounted chain links; breaking load approx. 1,5 times of the proof load.
Surface finish: electro-galvanized
Example of the order 100 pcs. connecting links
VG 8 x 31
Any other sizes on request.
Scope of delivery
• Screw connecting link
• Grub screw DIN 913
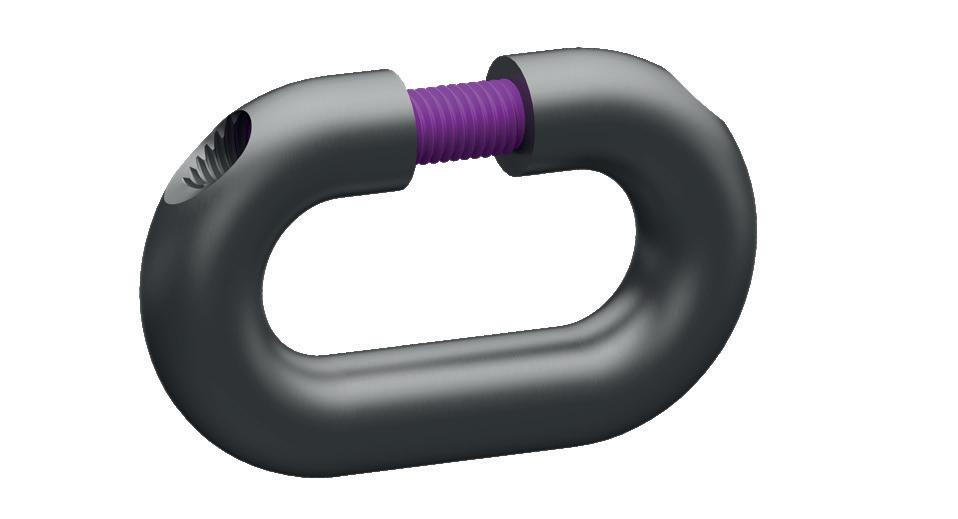
Example of the order 100 pcs. ScrewVG 16x80
Flight attachments are designed for use with chain ends and for bolting flight bars. The parts are forged, quenched and tempered, with inductively hardened interlink contact areas (hardening depth 0.1 × d, surface hardness min. 600 HV10). They operate over chain sprockets, pocket wheels, and plain chain wheels with or without a groove.
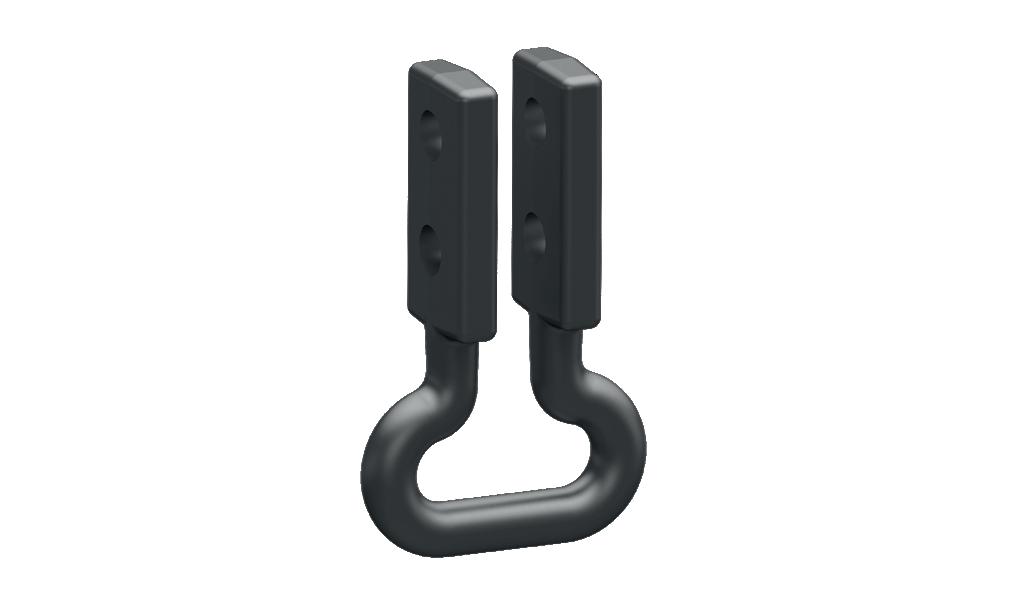
flight attachments
Any other sizes on request.
* Only through-hardended.
Scope of delivery
Only light attachment without mounting parts
Example of the order 100 pcs. flight attachments BM 10 x 35
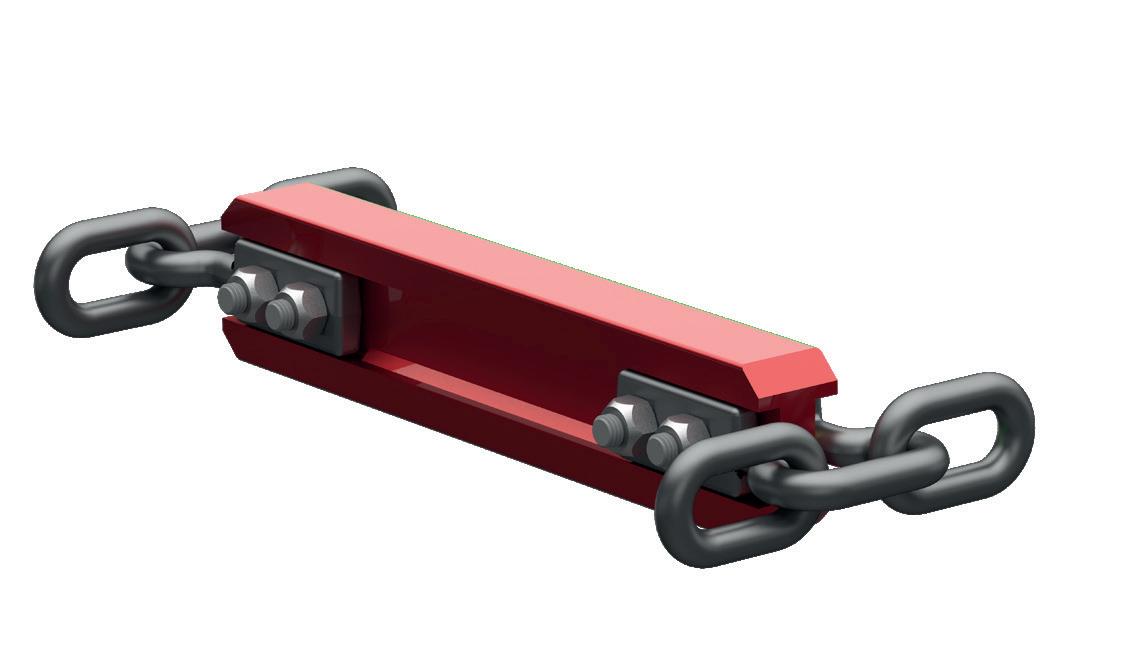
Chain shackles are suitable for connecting chain ends according to DIN 764 and DIN 766, as well as for attaching buckets in bucket elevators in accordance with DIN 15251. For friction drive systems, the DIN standard recommends using the next larger pitch chain shackle. Chain shackles should only be used in combination with distance plates. All shackles are drop-forged, with machined threads and collars.
Shackles C45vi: Through-hardened to a strength of approx. 1100 N/mm²; interlink contact areas inductively hardened, surface hardness min. 600 HV10.
Surface finish: waxed
The specified breaking load is only achieved when using the distance plate.
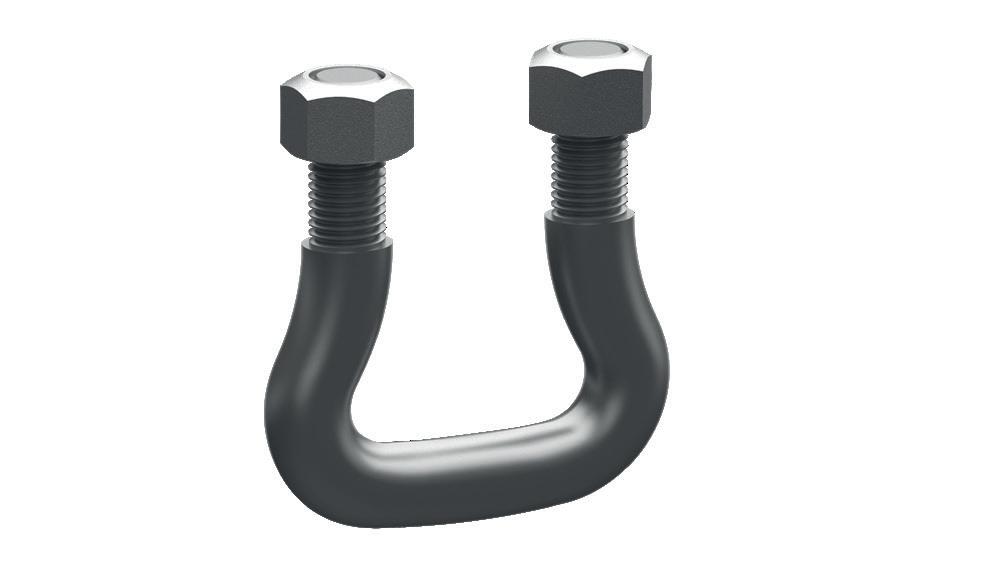
* Incl. 2 pcs. hex. nuts without distance plate.
** Quality G80 E10 vi on request.
Scope of delivery
• Chain shackle
• 2 pcs. hex. nuts DIN 934
• 1 pcs. distance plate (upon request)
* Chain shackle dia. d1.
These chain shackles provide higher breaking loads compared to standard chain shackles in accordance with DIN 745, ensuring increased operational safety. When replacing DIN 745 chain shackles with DIN 5699 versions in existing bucket elevators with side-mounted buckets, please note that the chain center distance will increase.
Surface finish: waxed
The specified breaking load is only achieved when using the distance plate.
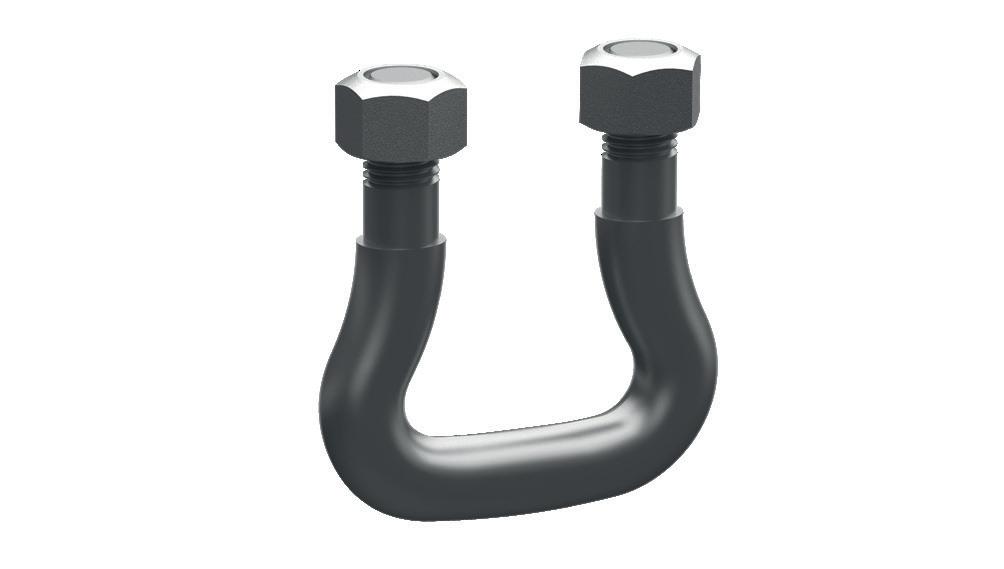
* Incl. 2 pcs. hex. nuts without distance plate.
** Quality G80 E10 vi on request.
Scope of delivery
• Chain shackle
• 2 pcs. hex. nuts DIN 934
• 1 pcs. distance plate (upon request)
* Chain shackle dia. d1.
Flight attachments are designed for severe service in two-strand and multi-strand chain conveyors, these flight attachments run over chain sprockets and plain chain wheels, with or without grooves. Made from forged MnCr steel and case-hardened for exceptional wear resistance. Welding surfaces are prepped for attachment to the flight bar. Features simple assembly and disassembly on the slack chain and are suitable for reverse operation.
Surface finish: sandblasted and waxed
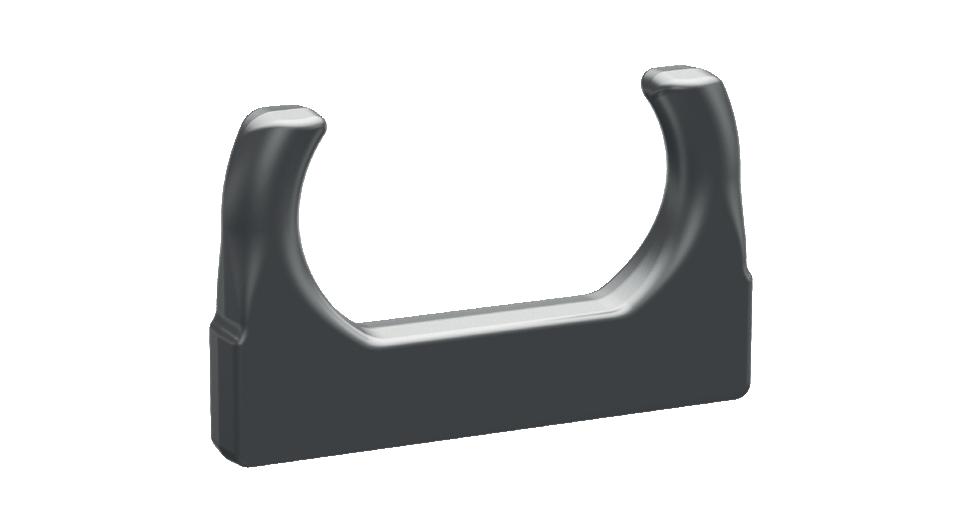
Recommended welding additive Böhler DMO-IG (EN ISO 21952-A: G MoSi; AWS A5.28: ER70S-A1 (ER80S-G)) or similar additives
Scope of delivery Flight attachment
Example of the order 100 pcs. flight attachments KFB 22 x 86
* Available on request
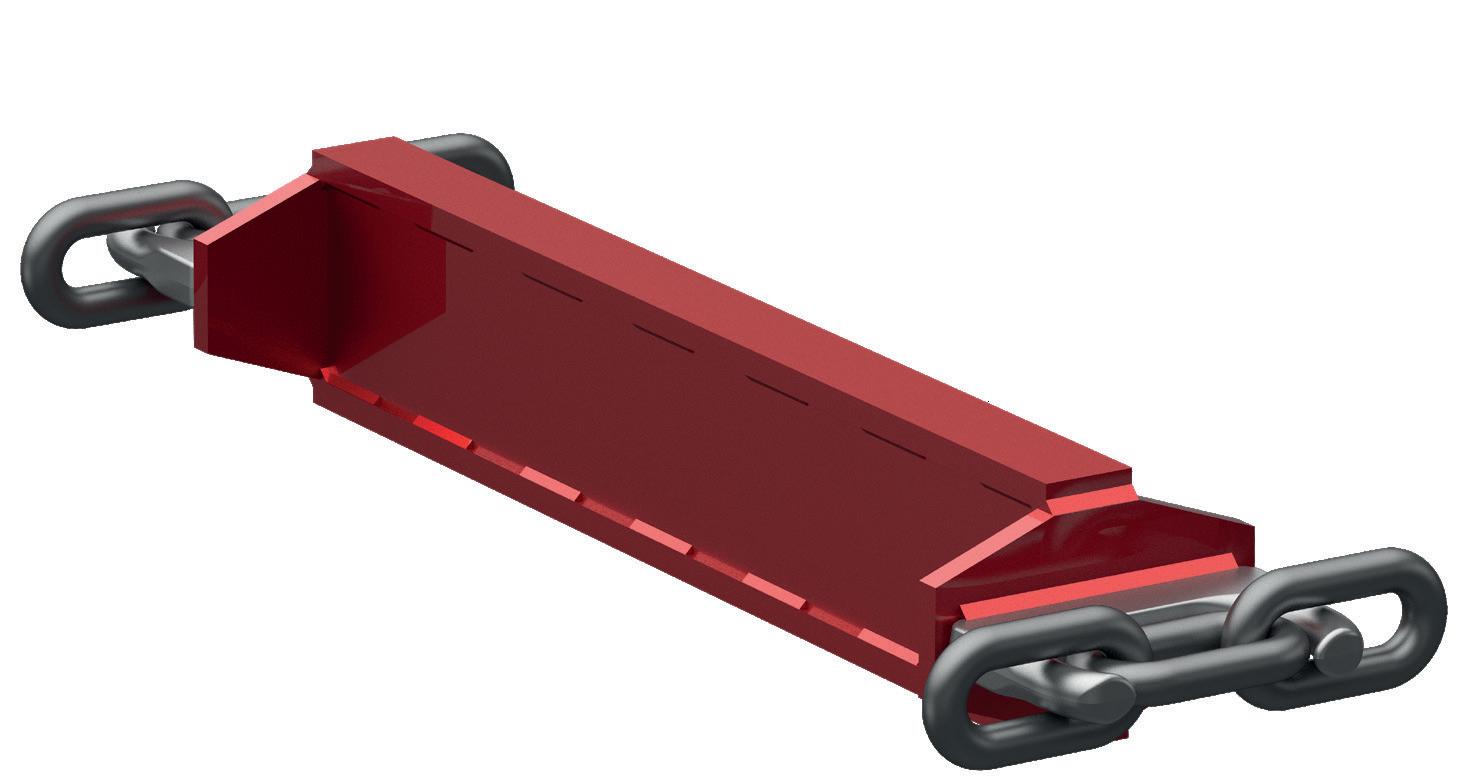
Designed for demanding operating conditions, these plug-in flight attachments are suitable for double-strand and multistrand chain conveyors. They run over sprockets and smooth idler wheels, with or without grooves. Each attachment features two bolts made of forged MnCr-alloyed, case-hardened steel, welded into a steel plate for high wear resistance.
To fit, insert the plug-in flight into the vertical chain links and secure it with the scraper bar, tightening the lock nuts or hex bolts to the specified torque.
Surface finish: sandblasted and waxed
Scope of delivery
• 1 pcs. Flight attachment
• 2 pcs. locking nut DIN 980-8 (for FDD with threaded pins)
Example of the order 100 pcs. flight attachments FDD 22 x 86
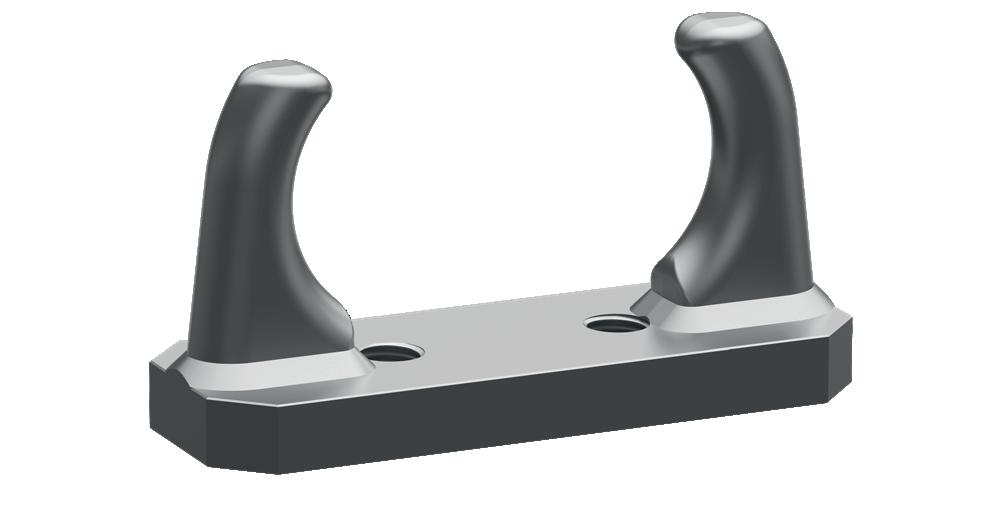
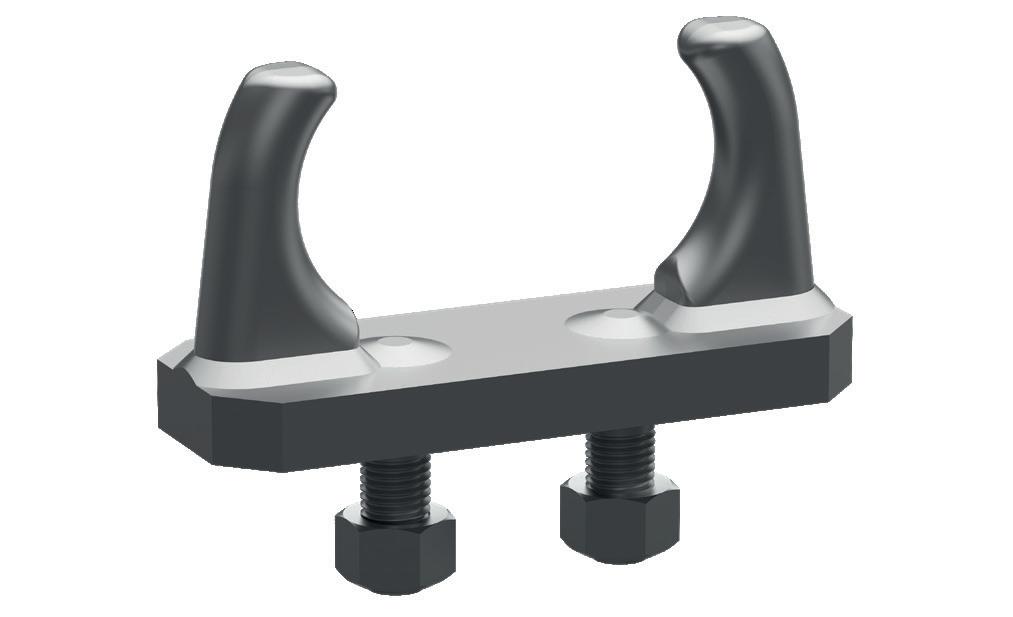
* Available on request
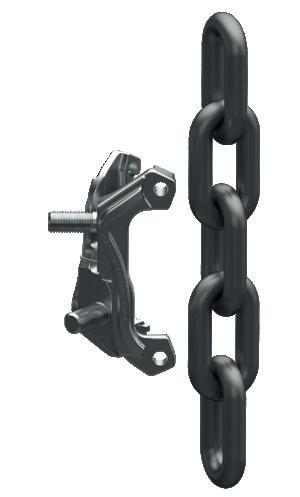
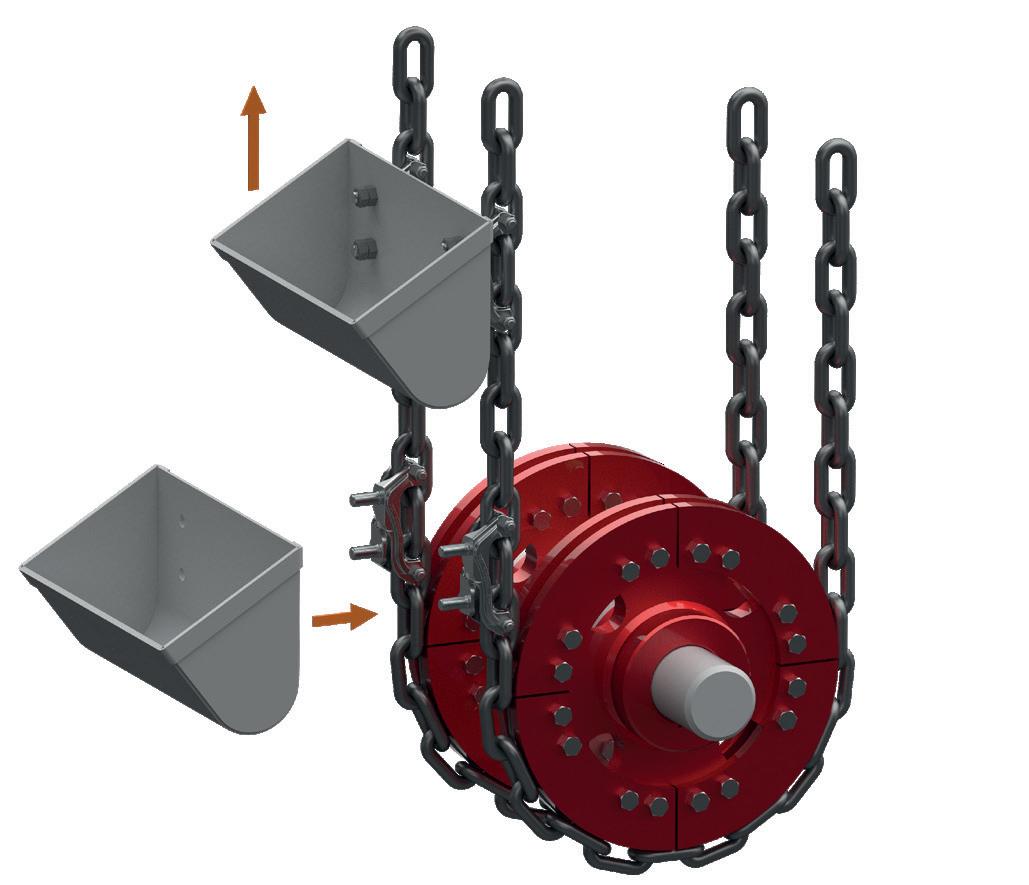
Designed for use with hero and round steel chains, chain sprockets and plain segmented chain wheels. Suitable for back-mounted buckets, allowing simple assembly and disassembly on the chain.
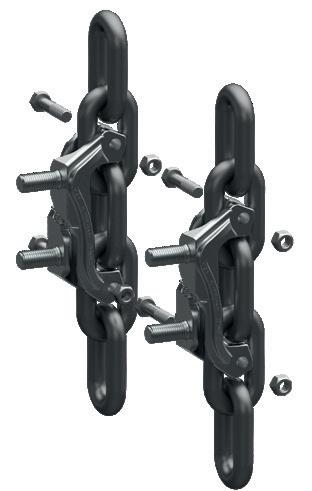
Each attachment consists of two identical forged halves, including bolts, and is heat-treated for durability. Mounting dimensions conform to standard shackles, enabling conversion of existing chain ends and shackle systems. Existing buckets and chain wheels can typically be reused.
Provides higher operational safety, as the BDS attachment does not transmit chain pull. No wear parts – fully reusable.
Surface finish: sandblasted and waxed
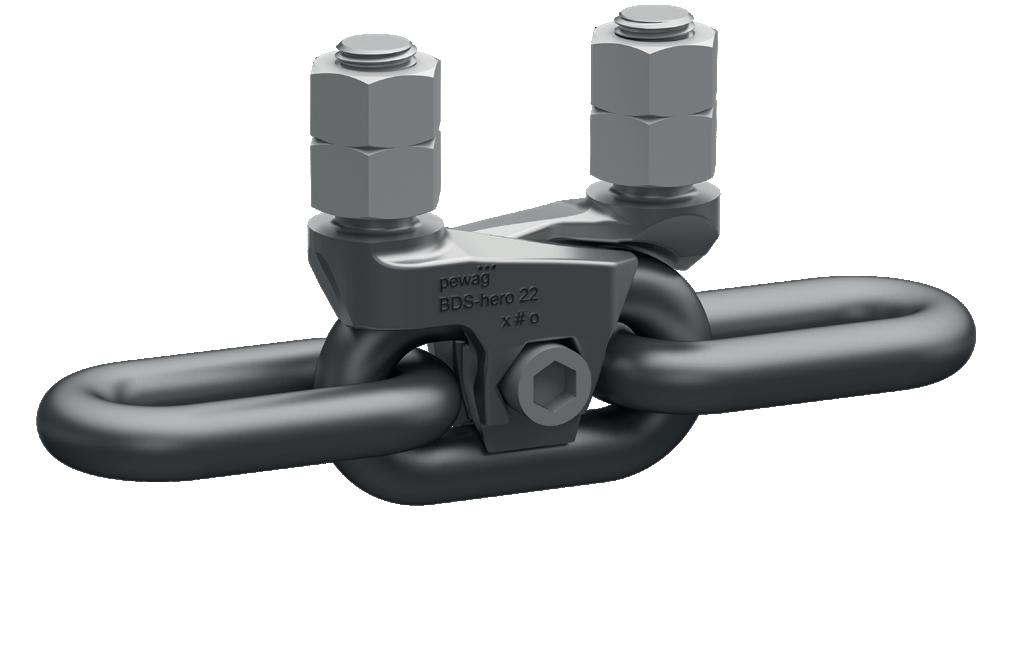
BDS-series bucket attachments
Scope of delivery
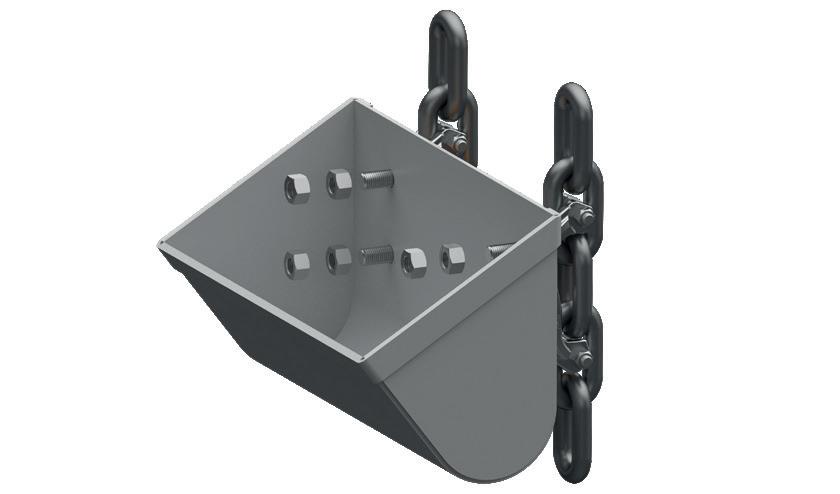
• 2 pcs. pre-assembled BDS clamp halves (with hex. socket head cap screw DIN 912-8.8 and locking nut DIN 980-8)
• 4 pcs. hex nuts DIN 934-8
Example of the order
80 pcs. bucket attachments BDS 22 x 86
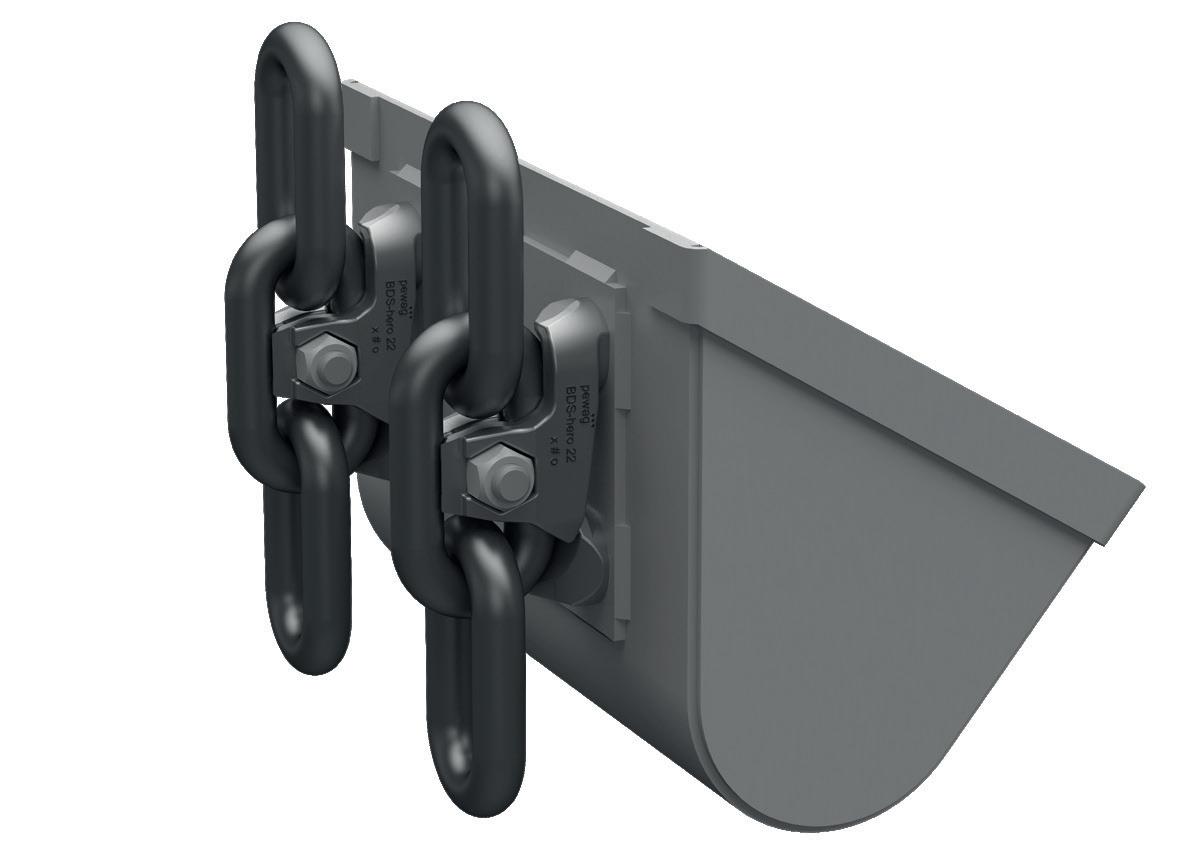
Designed for use with hero and round steel chains, chain sprockets and plain segmented chain wheels. Suitable for back-mounted buckets, enabling simple assembly and disassembly on the chain.
The BDDS attachment features high wear resistance, with hardened surfaces at the chain contact points. Mounting dimensions correspond to standard shackles, allowing conversion of existing chain ends and shackle systems. Existing buckets and chain wheels can generally be reused. Provides enhanced operational safety, as the BDDS attachment does not transmit chain pull.
Surface finish: sandblasted and waxed
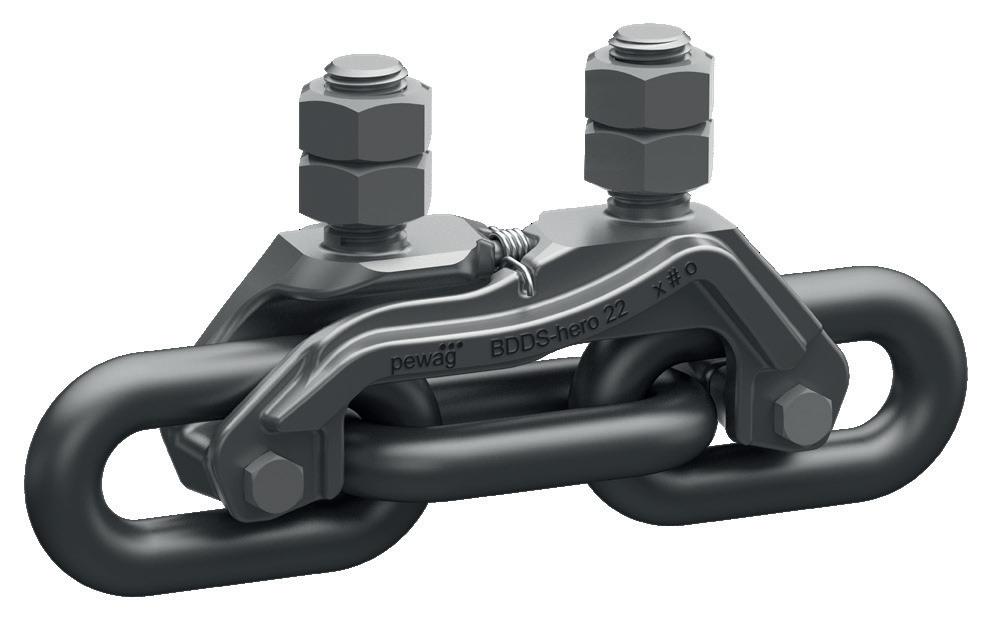
BDDS-series bucket attachments
Scope of delivery
• 2 pcs. pre-assembled BDDS clamp halves (with hex. bolt DIN 931-8.8 and locking nut DIN 980-8)
• 4 pcs. hex nuts DIN 934-8.
Example of the order
80 pcs. bucket attachments BDD-S 22 x 86
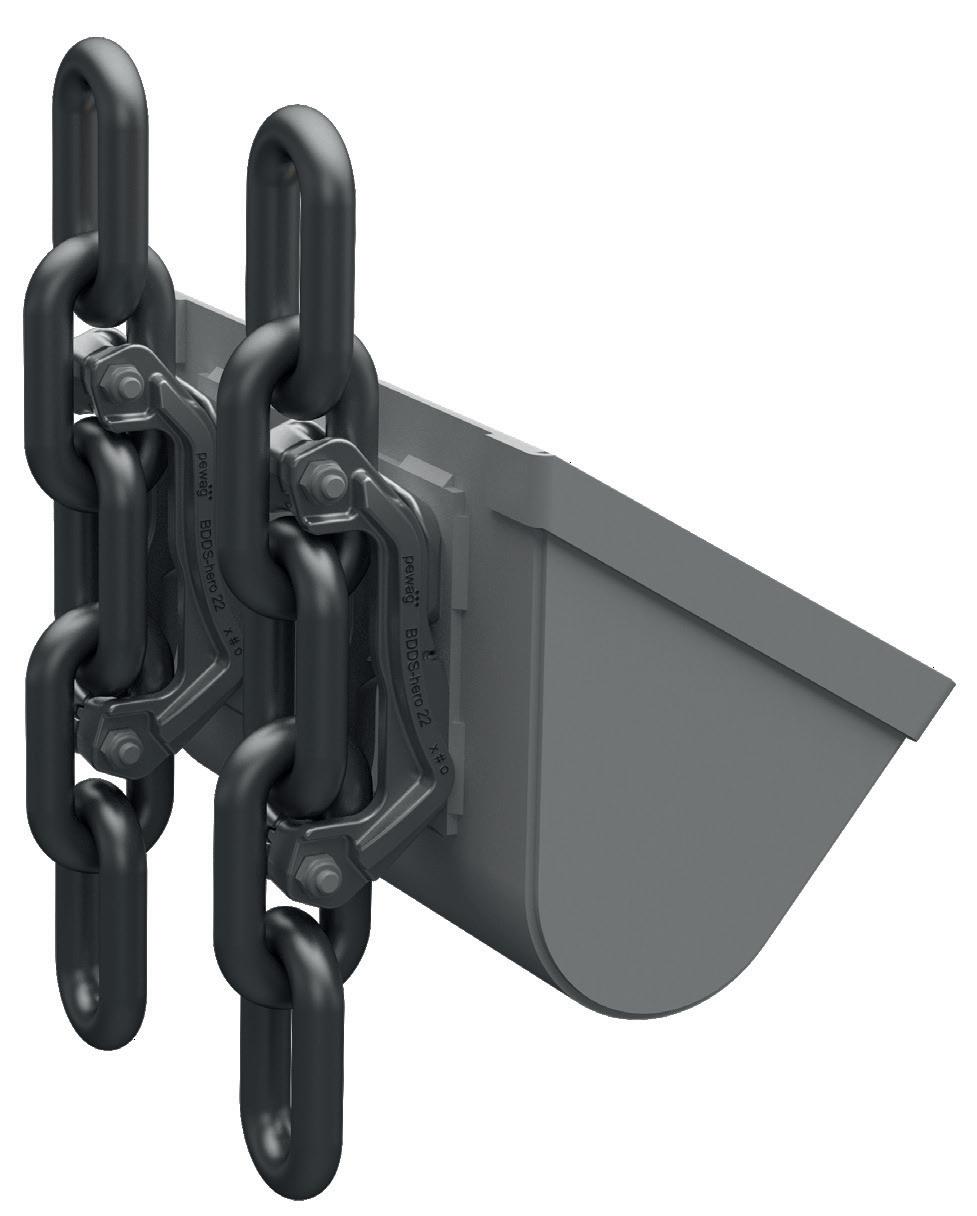
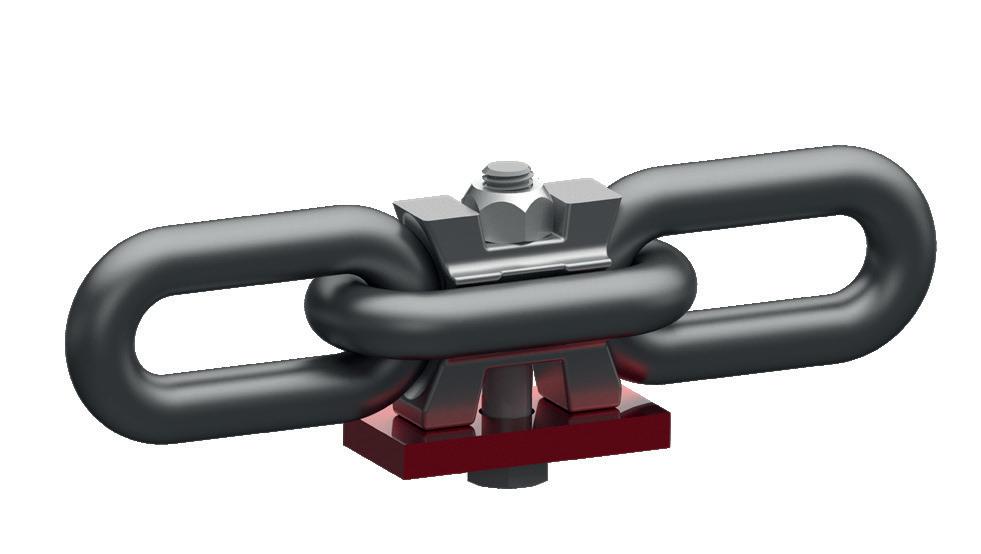
Designed for use with round steel chains and side-mounted buckets, compatible with RHV sprockets and plain segmented chain wheels. Allows simple assembly and disassembly on the chain.
Each attachment consists of two forged and case-hardened halves. Mounting dimensions allow conversion of existing chain ends and shackle systems, while existing chain wheels and buckets can generally be reused.
Provides enhanced operational safety, as the SDS attachment does not transmit chain pull.
Surface finish: waxed
SDS bucket and flight attachments
Scope of delivery
• 2 pcs. SDS-halves
• 1 pc. hex. bolt DIN 931-8.8 (bolt length has to be specified)
• 1 pc. locking nut DIN 980-8.
• Distance plate (upon request) Size should be specified
Example of the order
80 pcs. bucket attachments SDS 22 x 86 with mounting bolt and nut
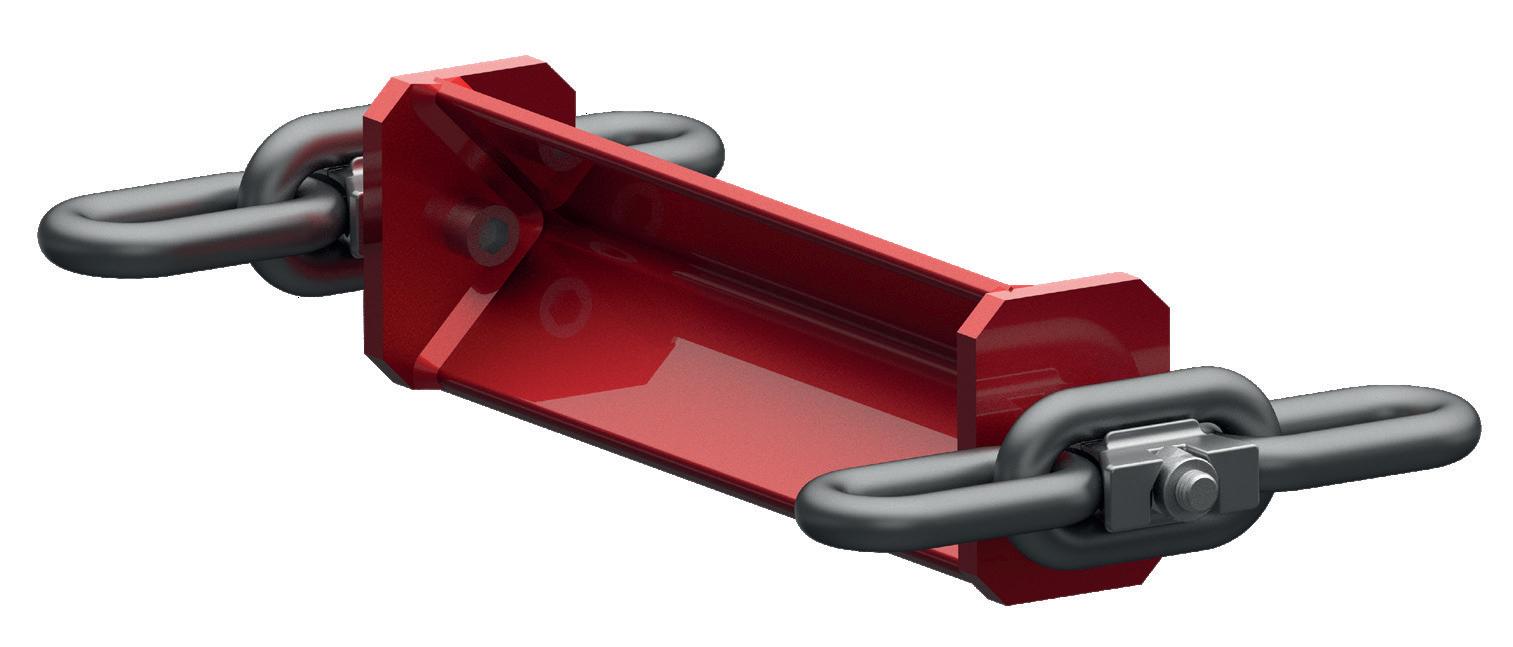
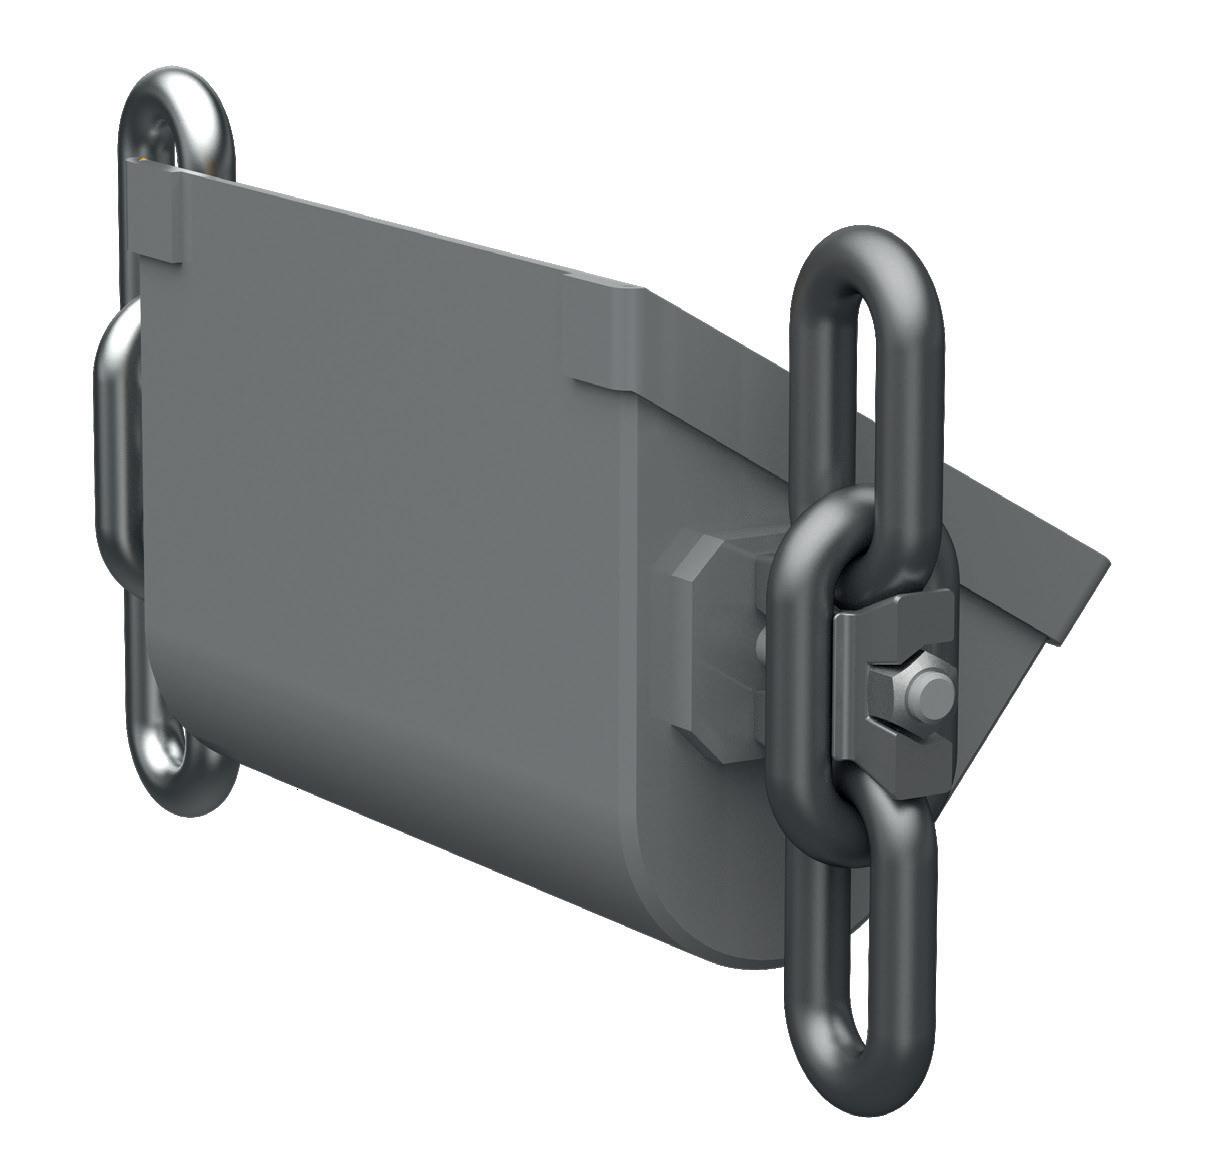
Bucket attachment suitable for round steel chains and for side mounted buckets, runs over sprockets RHV and plain segmented chain wheels; simple assembly and disassembly on the chain; 4 halves, forged and case hardened, 2 halves welded to plate, existing chain end and shackle system can be converted, same chain wheels and buckets can usually be used. Higher service safety because the SDD attachment does not have to transmit any chain pull.
Surface finish: waxed
bucket attachments
Scope of delivery
• 2 pcs. SDD-halves welded to plate
• 2 pcs. locking SDD-halves
• 2 pcs. hex. bolts DIN 931-8.8 (Bolt length has to be specified)
• 2 pcs. locking nuts DIN 980-8.
Example of the order
80 pcs. bucket attachments SDD 22 x 86 with mounting bolts and nuts
* Any other sizes and dimensions "e" on request.
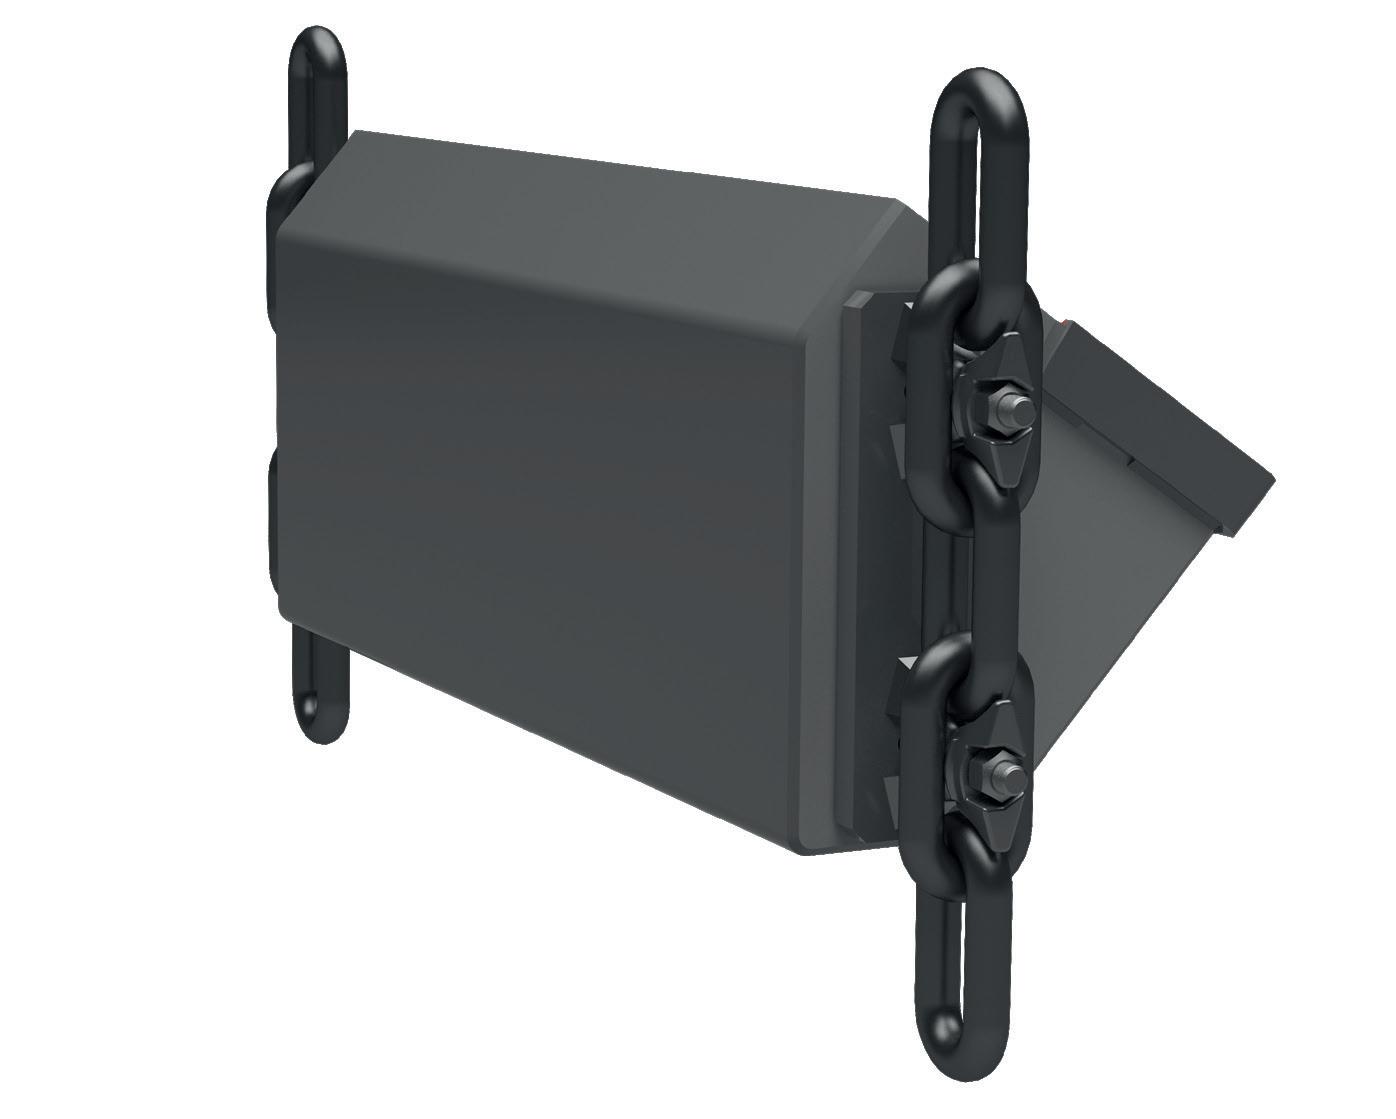
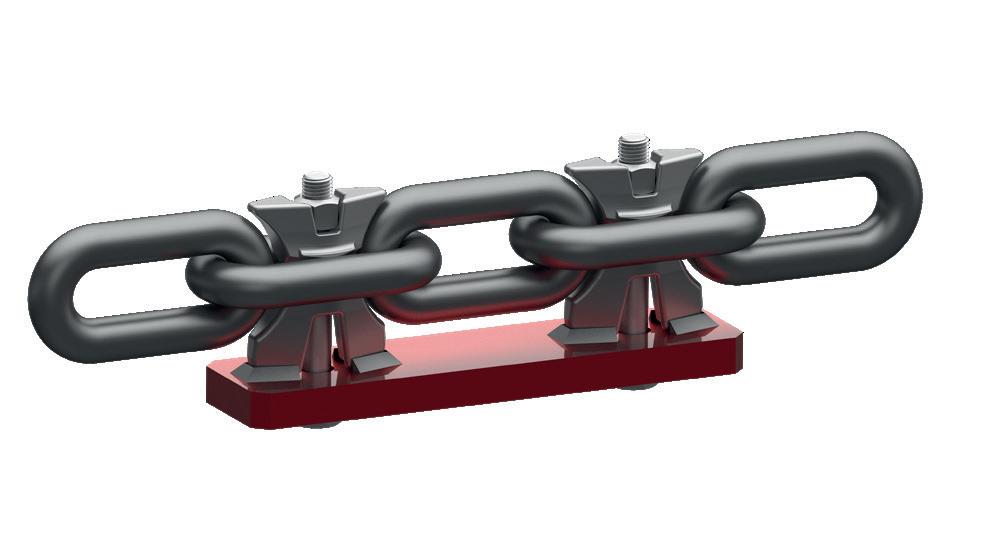
Designed to be bolted directly onto the flight bar, these attachments run over pocket wheels on horizontally mounted chain links.
Surface finish: electro galvanized (gzn)
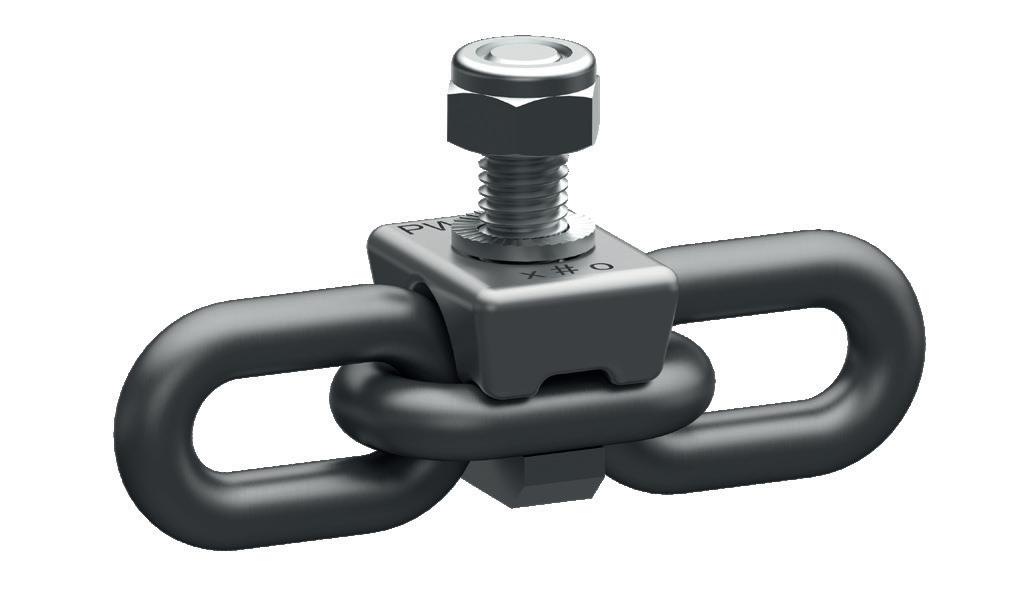
Scope of delivery
• 1 pcs. intermediary fitting piece (drop-forged)
• 1 pcs. highly durable special T-head bolt
• 1 pcs. locking nut DIN 980-8
• 1 pcs. lock washer
Example of the order
200 pcs. flight attachments SG 8 x 31
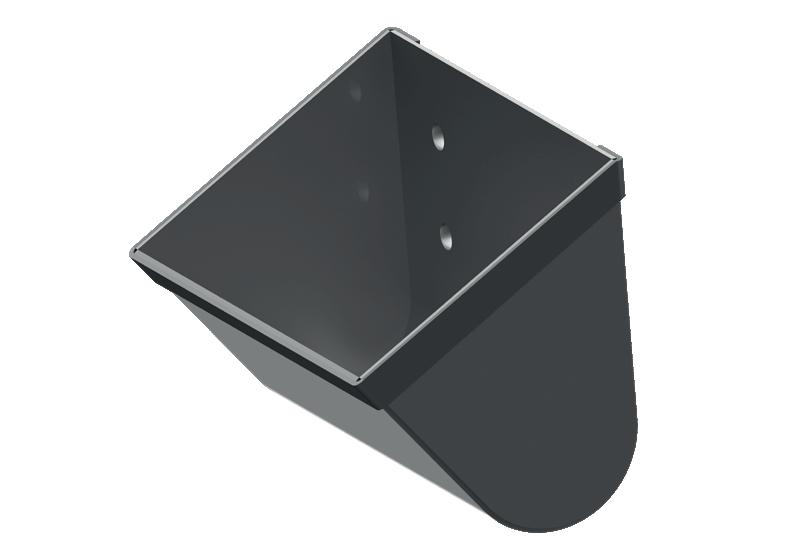
Steel elevator buckets of welded construction can be manufactured according to DIN standards or to any design specified by the customer. They are suitable for handling heavy powders, coarse grains, and lumpy materials such as sand, cement, gravel, and coal. Buckets made from cast polymer materials are also available for medium-duty operating conditions.
Bucket attachment with shackles (DIN 15236-4)
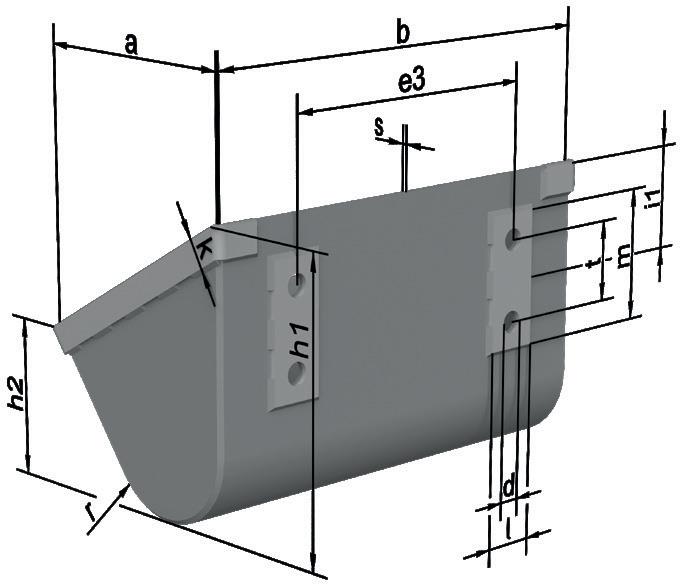
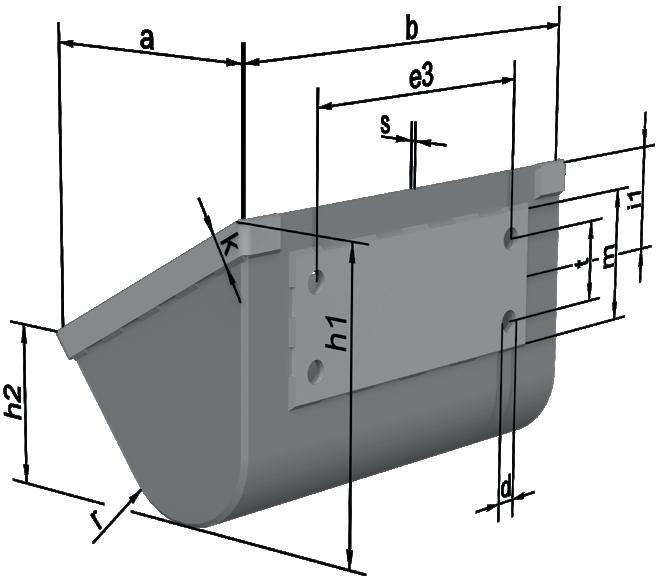
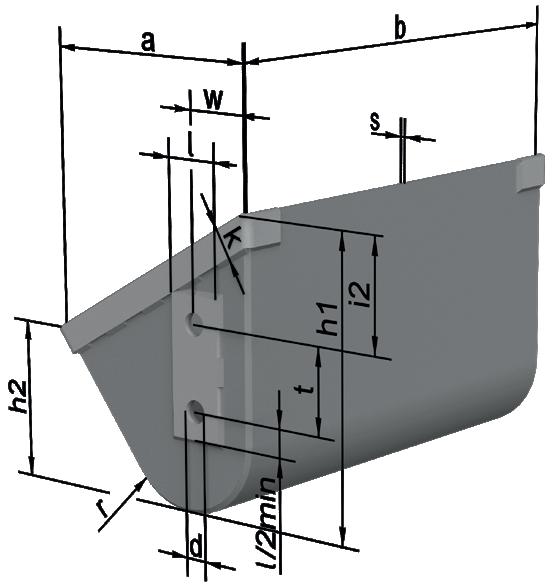
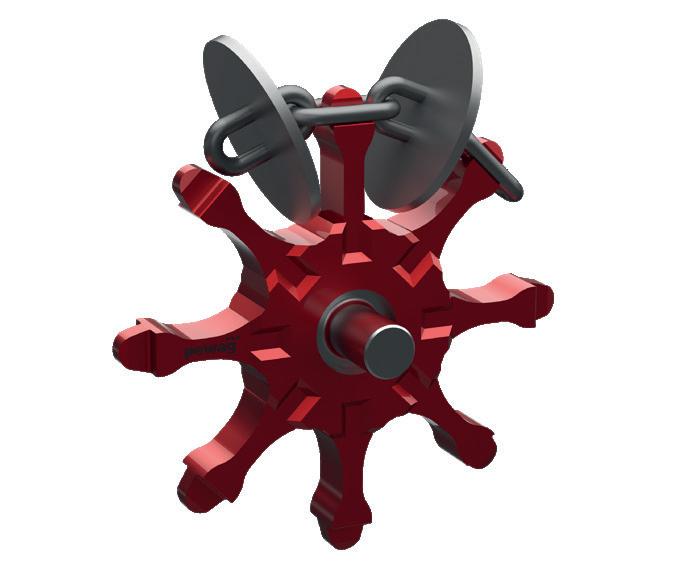
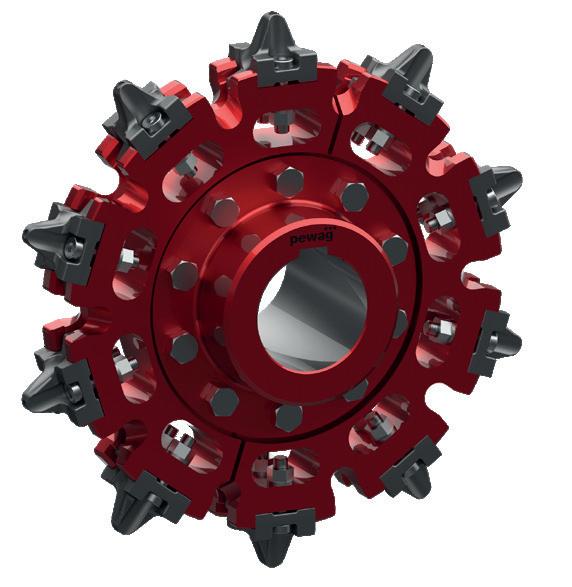
Toothed chain wheels are designed for use with hero and round steel chains. They feature replaceable and adjustable individual teeth made from MnCr-alloyed steel, case-hardened for high wear resistance. The sprockets are welded steel fabrications, and any number of teeth or hub design can be supplied.
Keyways are machined in the hubs of matched wheels to ensure precise alignment of the teeth.
Hub design, bore diameter, and key size can be customized according to customer requirements. Shimplates can be fitted under the teeth to adapt the pitch circle diameter of the sprocket when the chain lengthens due to wear at the interlink points, ensuring smooth chain operation and maximum use of the case-hardened layer.
Maintenance: Shimplates and new teeth can be mounted without disassembling the chain.
Chain sprockets RHV-A: with cleaning slots are recommended for scraper conveyors.
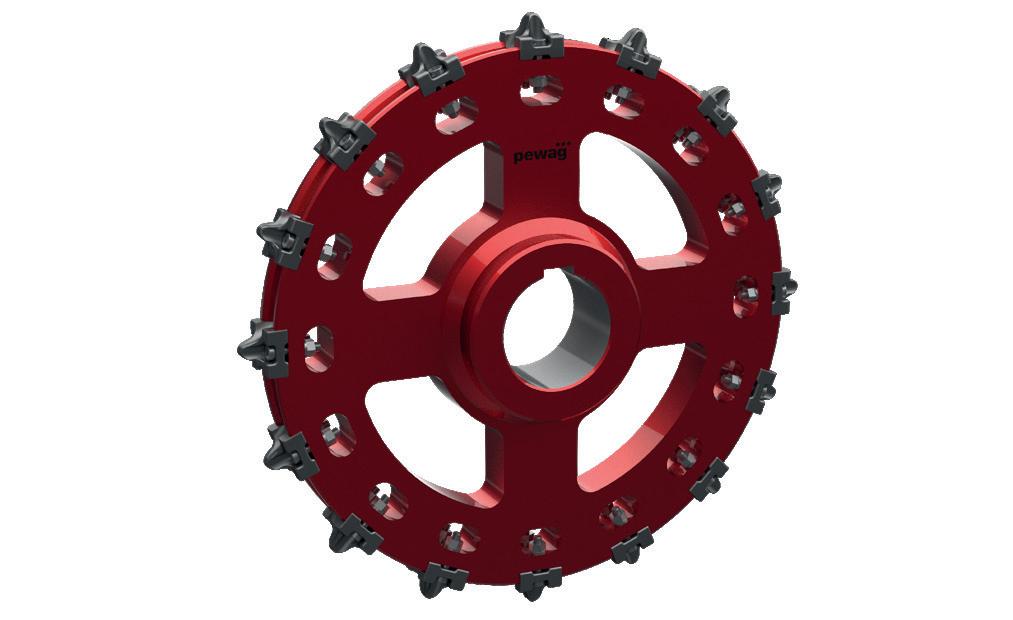
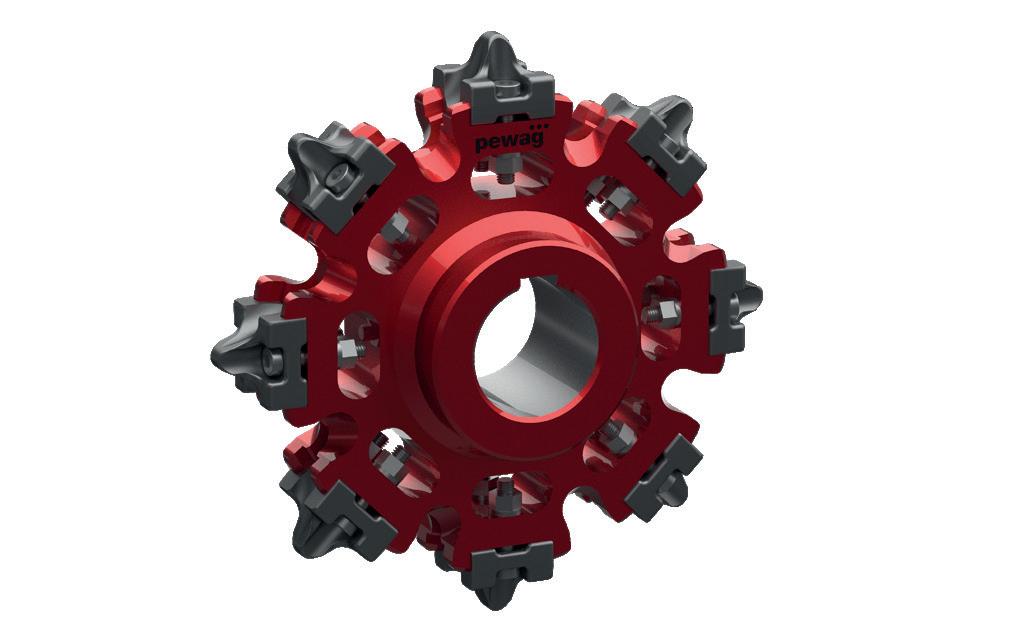
RHV
Any other number of teeth and sizes on request. Hub length and hub diameter can be specified by the customer.
The teeth are compatible with hero and round steel chains. Each tooth is made from MnCr-alloyed steel, case-hardened for high wear resistance, with a surface hardness of 800 HV10. The individual teeth can be adjusted with shimplates to adapt the pitch circle diameter of RHV(-A) sprockets for chains that have lengthened due to wear at the interlink points, ensuring continued smooth running of the chain.
Surface finish: sandblasted and waxed
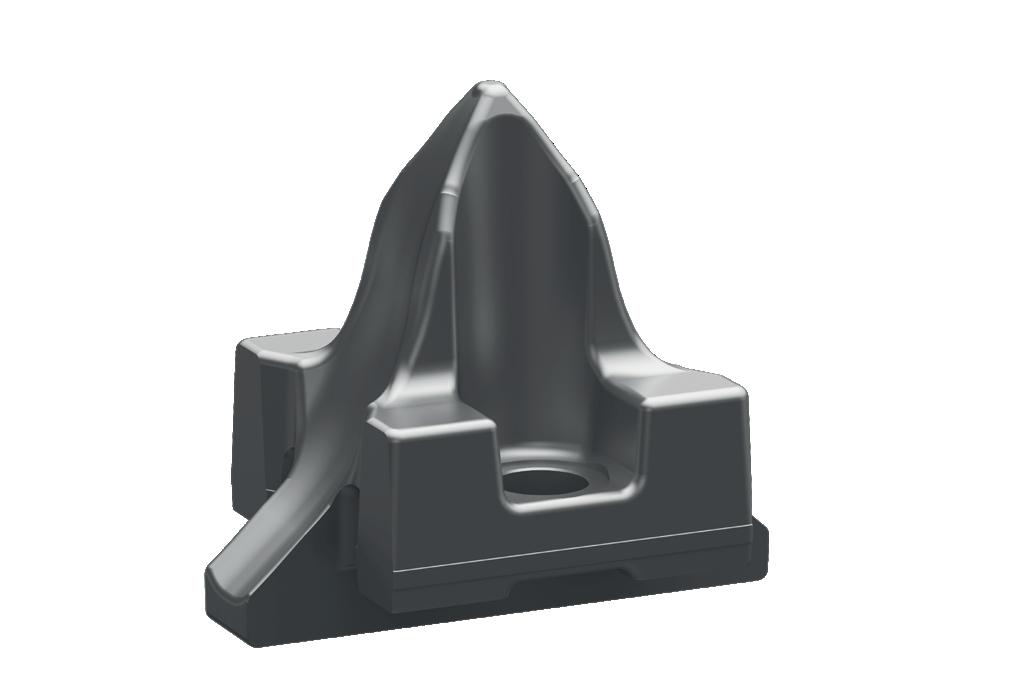
Scope of delivery
• Individual teeth E-Series
• Mounting parts
* Mounting parts: hex. socket head cap screw DIN 7984 - 8.8; spring washer DIN 127 and hex. nut DIN 934 - 8. Individual teeth with shimplates the screw length has to be advised
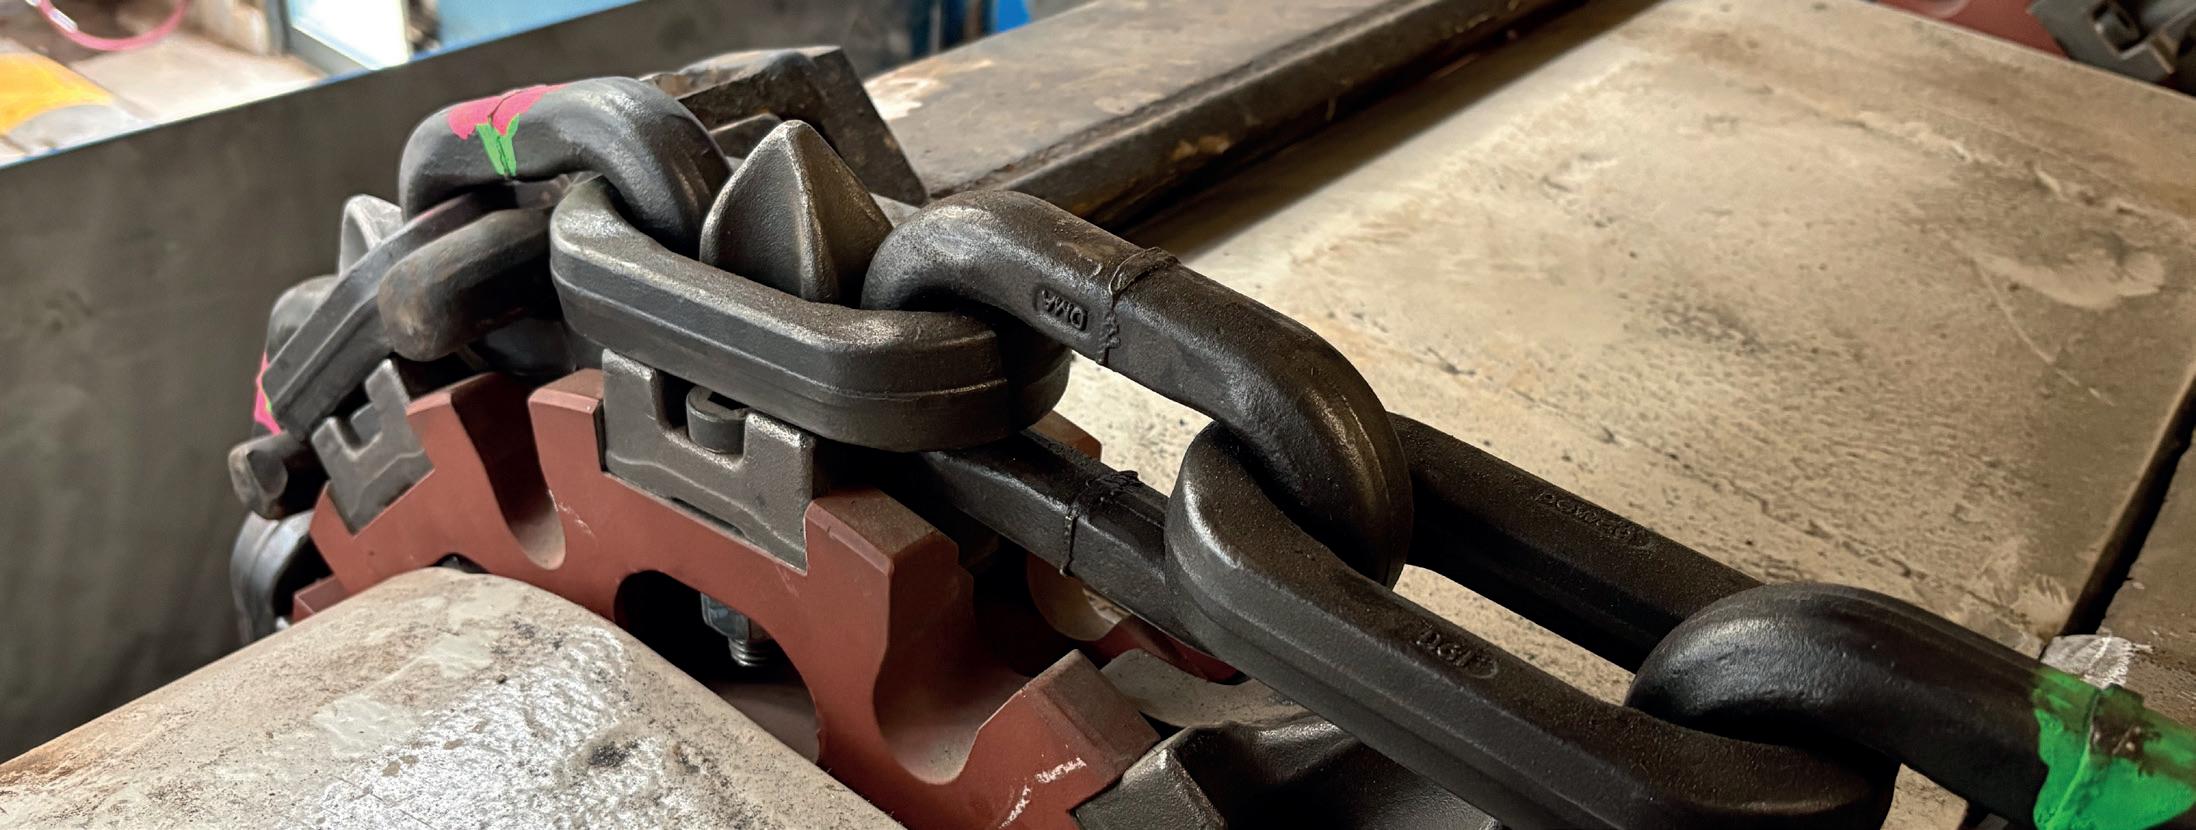
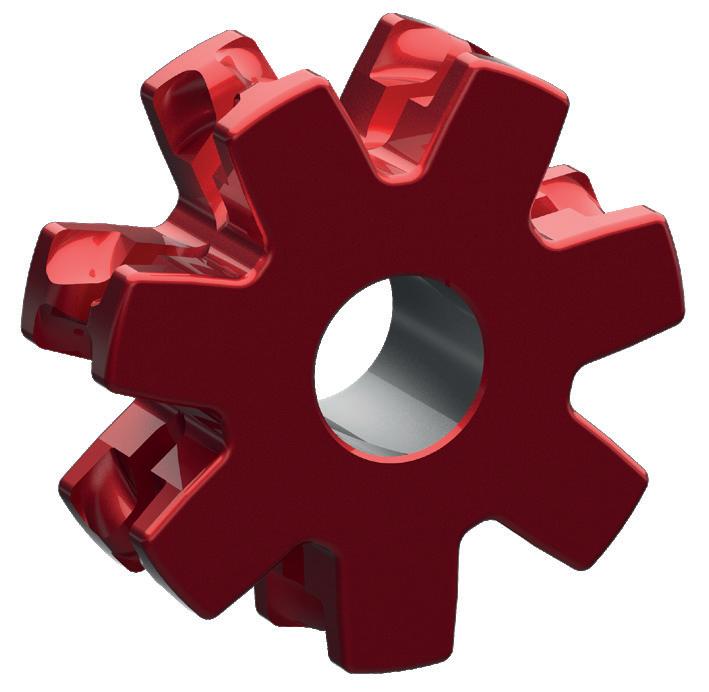
Sprockets are welded steel fabrications, available either as a single-piece design or with replaceable tooth segments for drive and tail sections. They are case-hardened for high wear resistance.
Fabricated steel sprockets can be supplied for any medium or long pitch chains with any number of teeth. Hub design, bore diameter, and key size can be customized according to customer requirements.
IR sprocktes in segmented version consist of: wheel body (1), IR segments (2), counter disc (3) and screw connection.
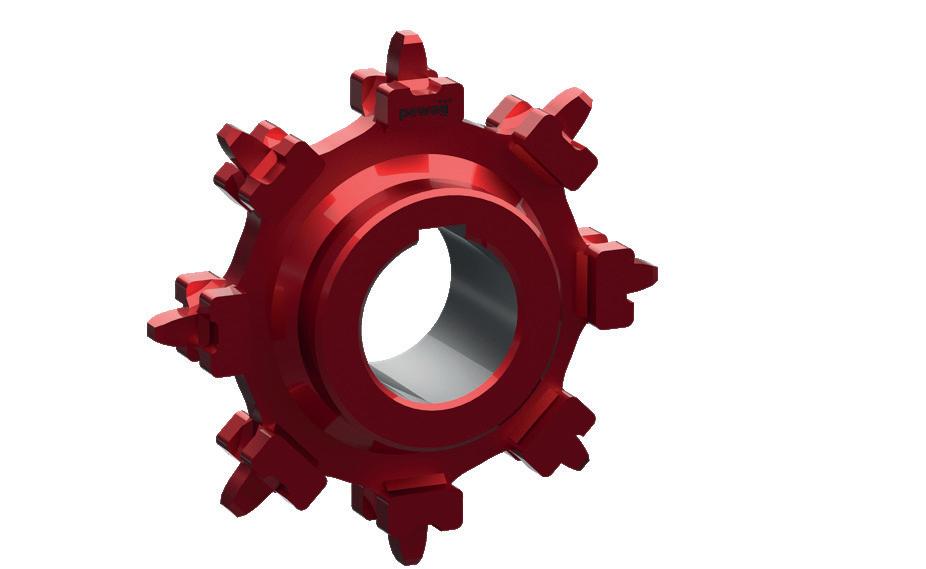
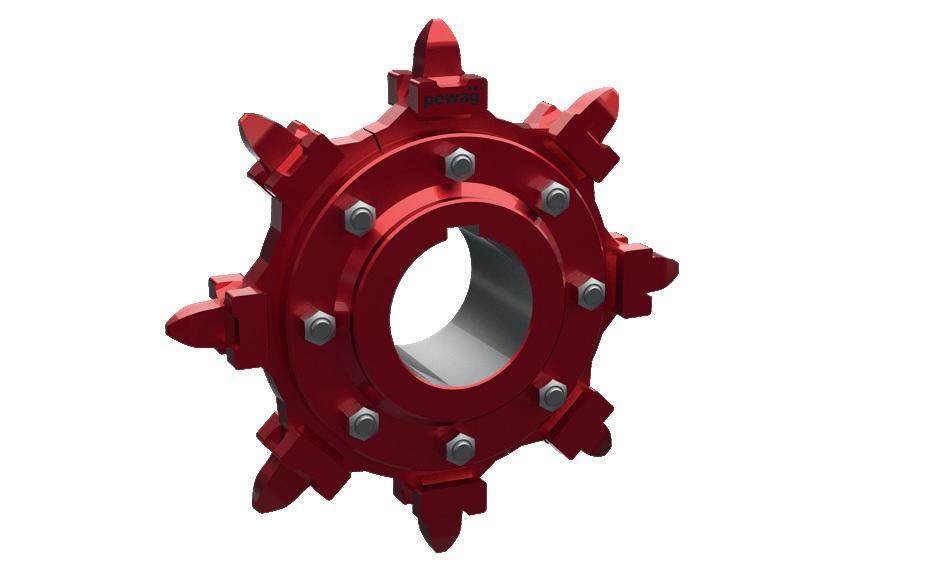
IR-SEG sprocket
IR-SEG
Any other number of teeth and sizes on request. Hub length and hub diameter can be specified by the customer.
Scope of delivery
• Chain sprocket IR ... , in one piece, case hardened and with machined hub
• Chain sprocket IR ... -Seg, machined hub, 2 pcs. case hardened tooth segments, counter plate with mounting bolts and nuts
conveyor chains and components
Example of the order 2 pcs. chain sprockets IR 16/10-64 -Seg ready to install for chain 16 x 64, Number of teeth z = 10 Offset hub: length I = 130, length I1 = 50 Hub bore dia. = 100 H7 and keyway acc. to DIN 6885
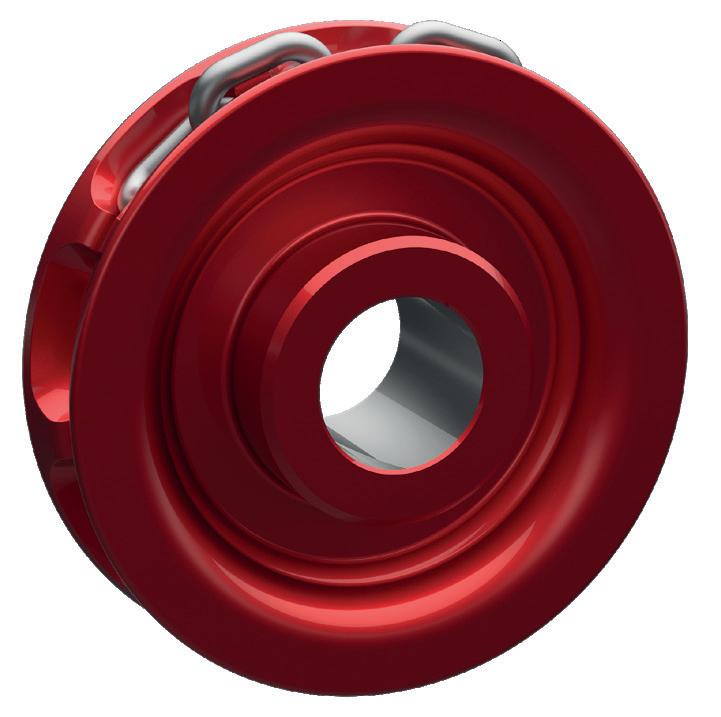
Pocket wheels are welded steel fabrications, available either as a single-piece design or with replaceable pocket segments for drive, guide, and tail sections. They are case-hardened for high wear resistance.
Fabricated steel pocket wheels can be supplied for any chain pitch-tooth combination, with any number of pockets. Hub design, bore diameter, and key size can be customized according to customer requirements.
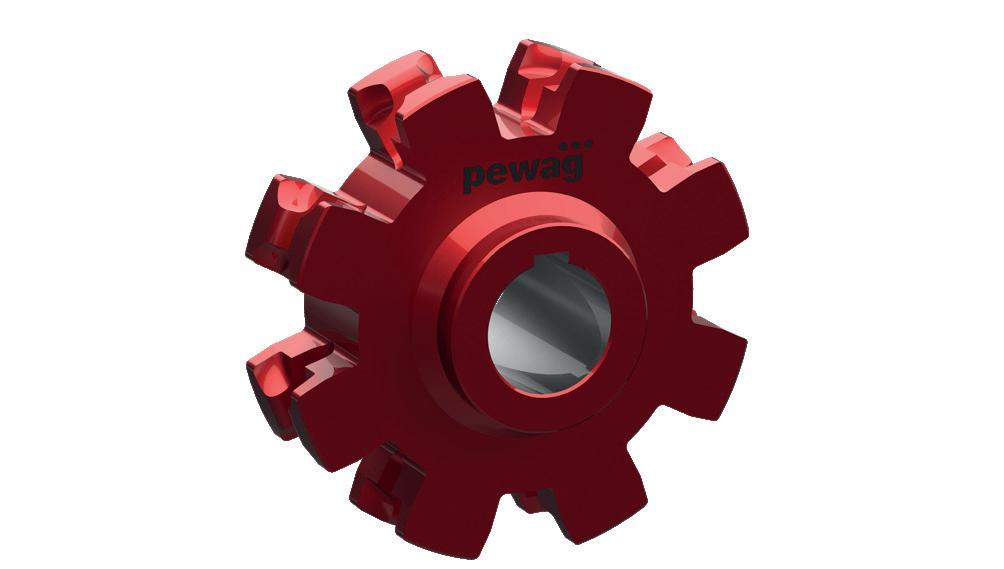
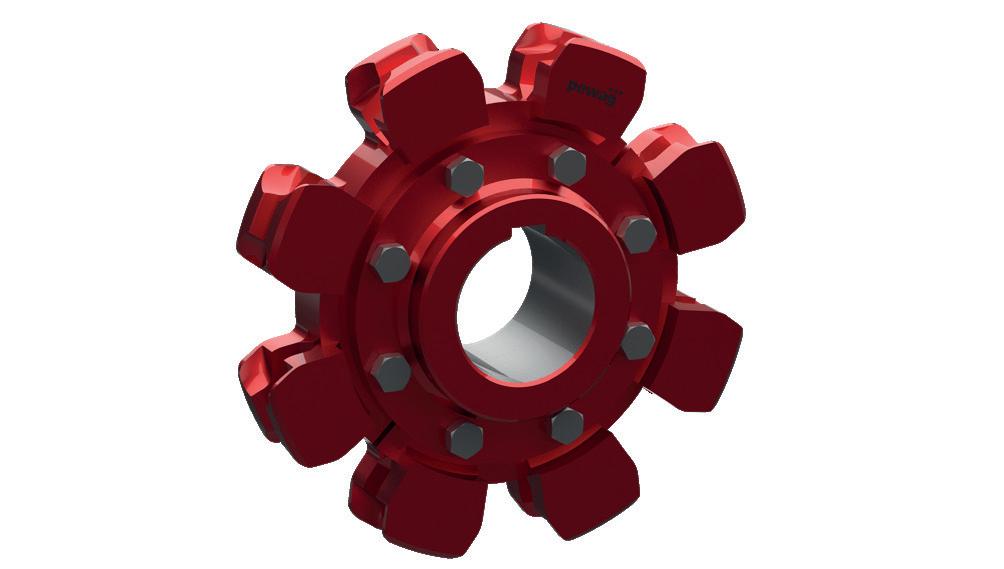
KR(-SEG) pocket wheels
Any other number of teeth and sizes on request. Hub length and hub diameter can be specified by the customer.
Scope of delivery
• Pocket wheel KR …, in one piece, case hardened and with machined hub
• Pocket wheel KR ... -Seg, machined hub, 2 pcs. case hardened segments, counter plate with mounting bolts and nuts
Example of the order 2 pcs. pocket wheels KR 19/10-75-Seg ready to install for chain 19 x 75, Number of teeth z = 10
Offset hub: length I = 150, length I1 = 50
Hub bore dia. = 100 H7 and keyway acc. to DIN 6885
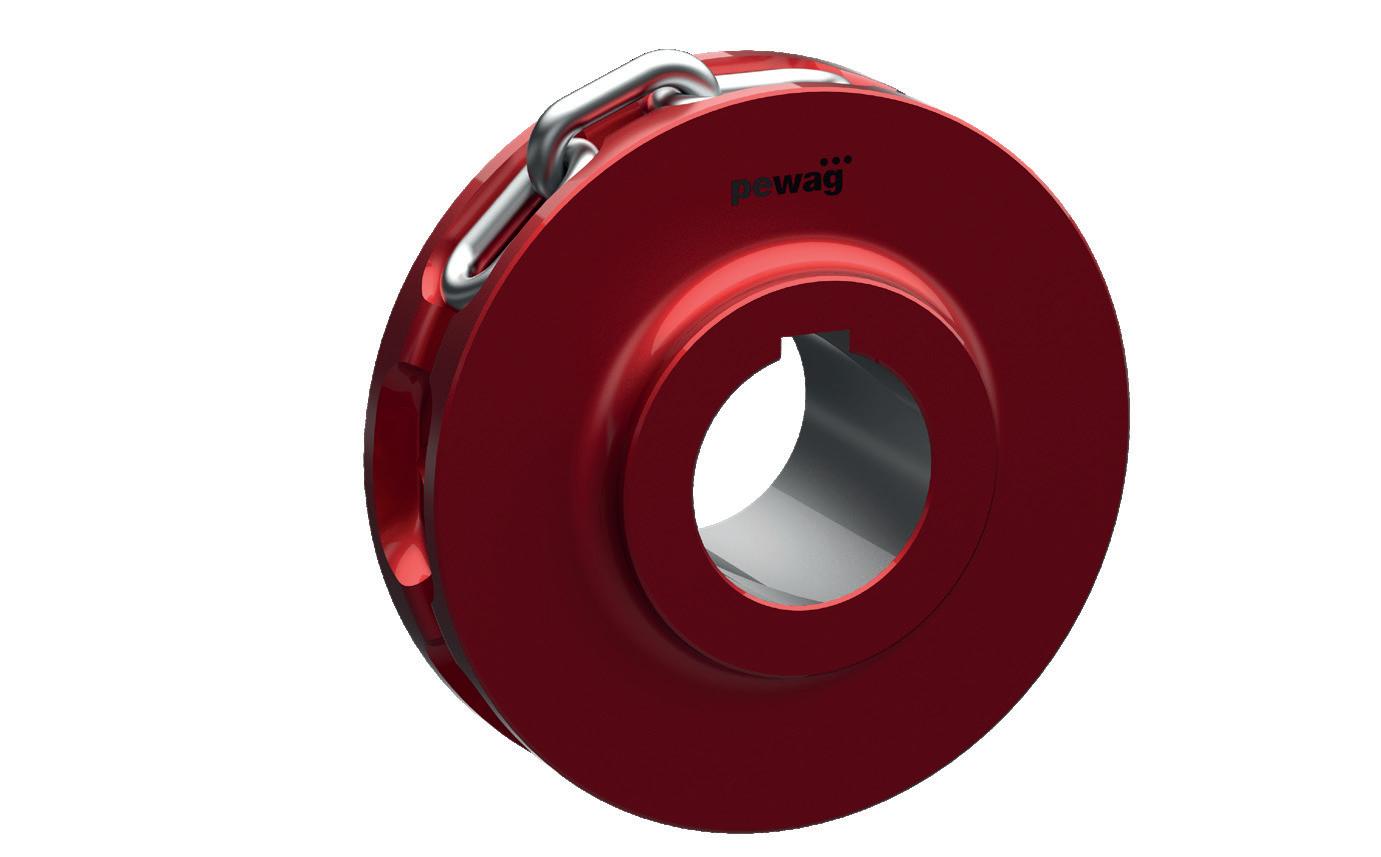
Pocket wheels are welded steel fabrications, available either as a single-piece design or with replaceable pocket segments for drive, guide, and tail sections. They are case-hardened for high wear resistance.
Fabricated steel pocket wheels can be supplied for any chain pitch-tooth combination, with any number of pockets. Hub design, bore diameter, and key size can be customized according to customer requirements.
Material
CrMo-alloyed steel, through hardened MnCr-alloyed steel, case hardened
Scope of delivery
Pocket wheel machined, material has to be specified
Example of the order
4 pcs. pocket wheels TR 10/12-28 for chain 10 x 28, No. of teeth z = 12
Hub length central = 80 mm (40 + 40)
Hub bore dia = 50 H7 and keyway acc. to DIN 6885
Any other number
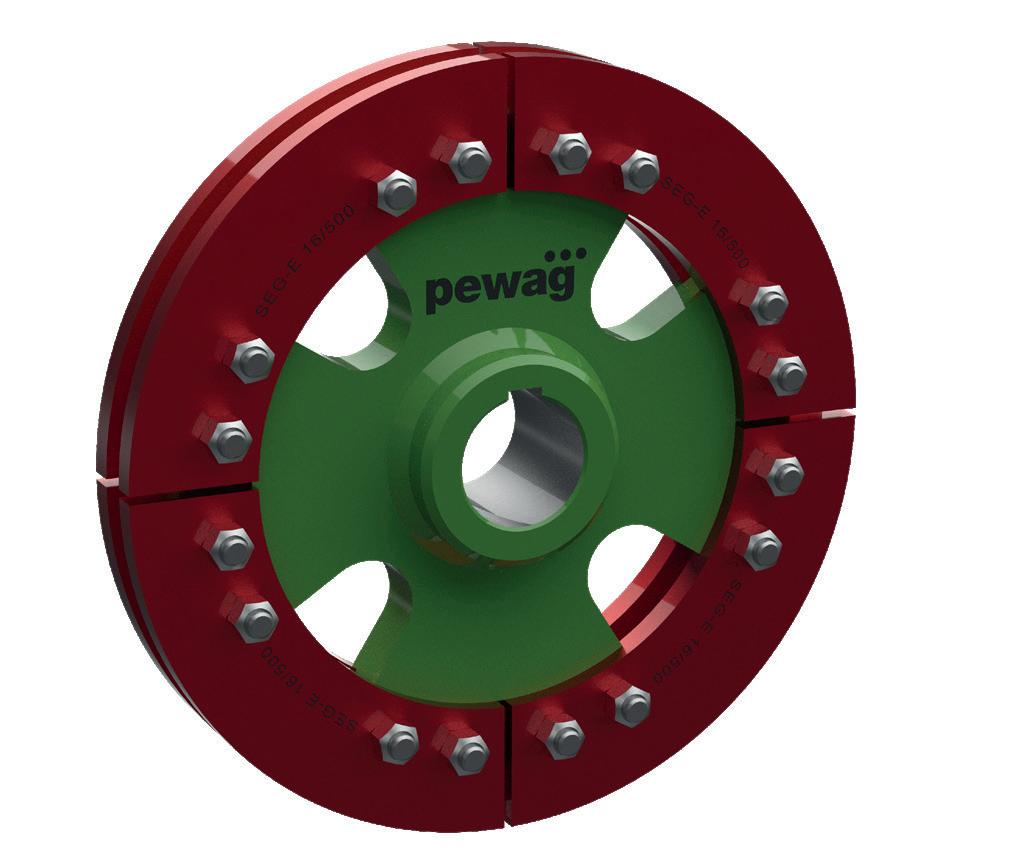
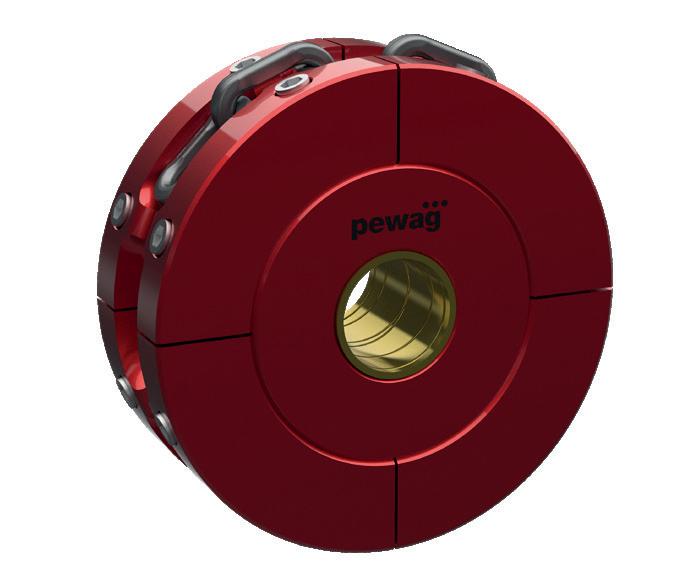
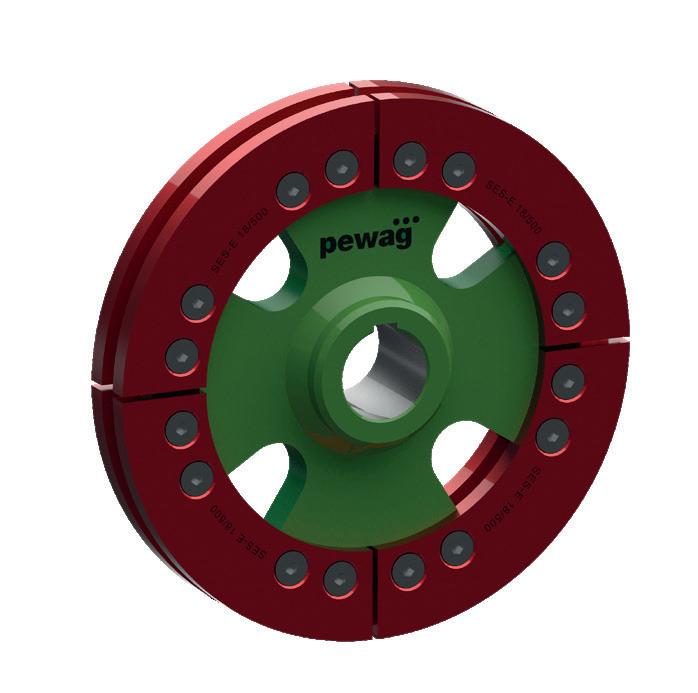
Plain segmented chain wheels are designed for use with hero and round steel chains, as well as chain ends according to DIN 764 and DIN 766.
SEG-E Features:
Steel hub with cleaning slots, welded steel fabrication
Replaceable hardened steel segments, highly wear-resistant, surface hardness min. 700 HV10 Bore diameter and key size can be customized according to customer requirements, SEG-E plain segmented chain wheels are suitable as drive and tail units.
Any other sizes on request.
Example of the order
2 pcs. drive-plain segmented chain wheels
Hub length central e = 160 mm (80 + 80)
SEG-E 23/800 for chain 22 x 86, pitch circle dia. = 800 mm
Hub bore dia. = 150 H7 and keyway acc. to DIN 6885
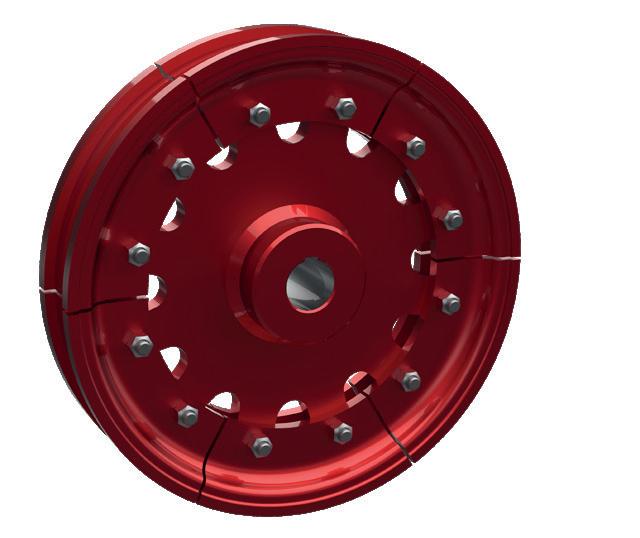
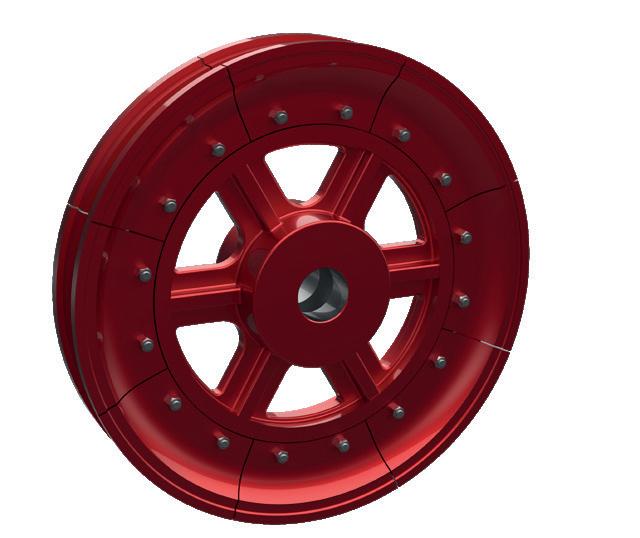
Designed for use with hero and round steel chains or chain ends (DIN 764 / DIN 766).
Replaceable segments made from highly resistant chilled cast iron (400–450 HB30); long service life; replaceable without removing the chain.
Suitable for back- and side-mounted buckets (with DIN 5699 shackles).
Hubs: Gray cast GGN (no cleaning slots) or steel STN (with cleaning slots); bore diameter and key size customizable.
Any other sizes on request.
* For this wheel sizes, type KS segments without
steel hub STN
Designed for use with hero, round steel chains, or chain ends (DIN 764 / DIN 766).
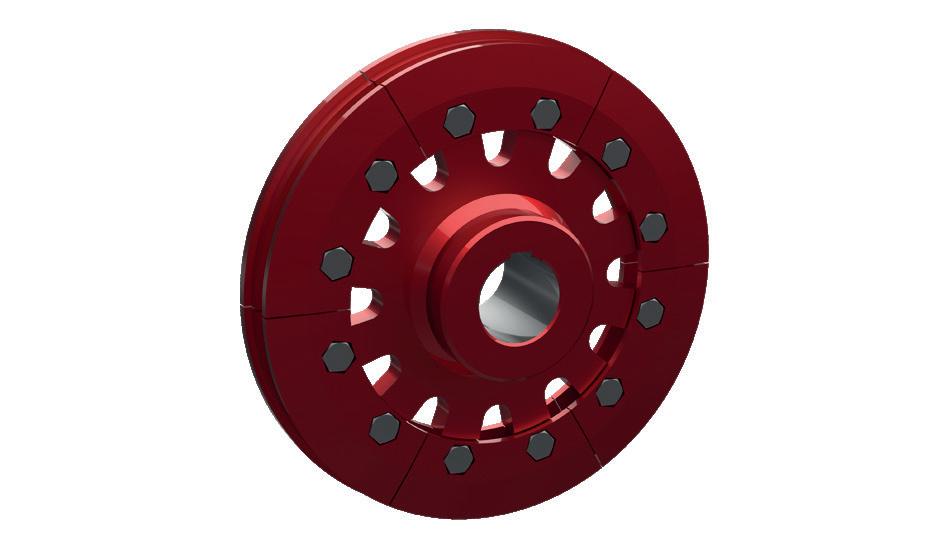
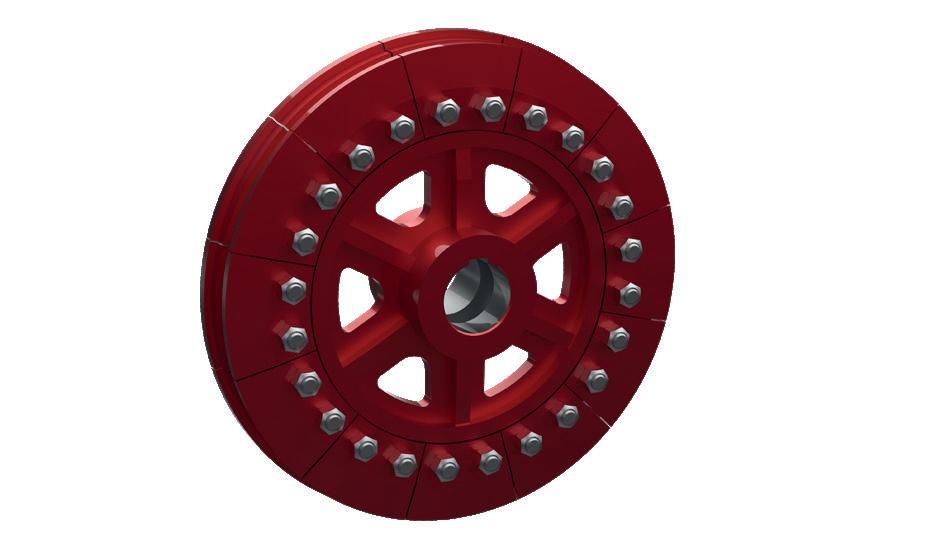
Drive and tail wheels with replaceable segments made from highly resistant chilled cast iron (400–450 HB30); long service life; segments replaceable without demounting the chain.
Suitable for side-mounted buckets.
Hubs: Gray cast GGN (no cleaning slots) or steel STN (with cleaning slots); maximum bore diameter limited for GGN; bore diameter and key size customizable.
Any other sizes on request.
Example of the order
2 pcs. drive-plain segmented chain wheel KSE 23/800 for chain 22 x 86, pitch circle dia. = 800 mm
Hub length central e = 160 mm (80 + 80)
Hub bore dia. = 150 H7 and keyway acc. to DIN 6885
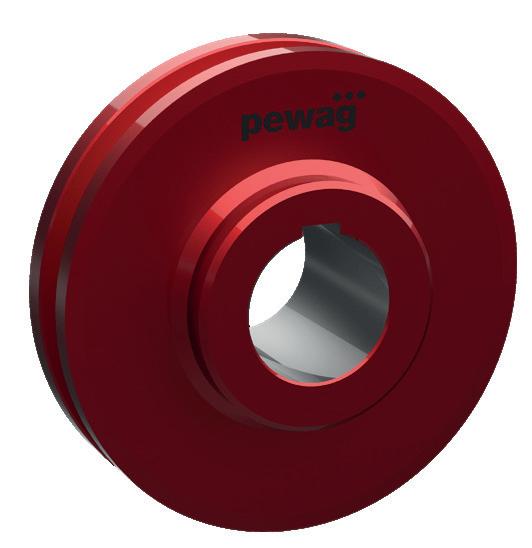
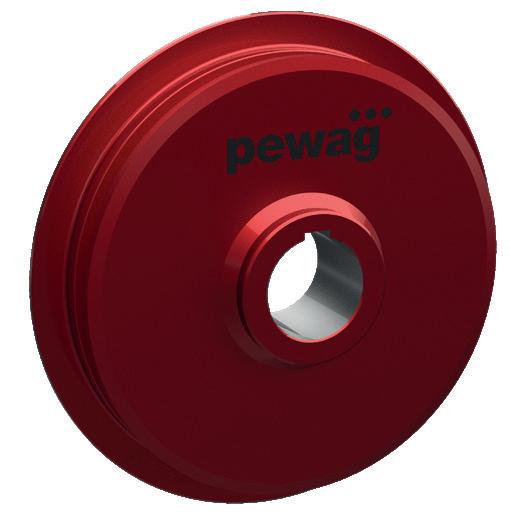
Plain tail and idler wheels UK, UL, ULR and ULS are designed for scraper and bucket conveyor. They are welded steel constructions with case-hardened chain contact surfaces, providing exceptional wear resistance. Available in any external or pitch circle diameter. Hub design, bore diameter, and keyway dimensions can be customized to meet customer specifications.
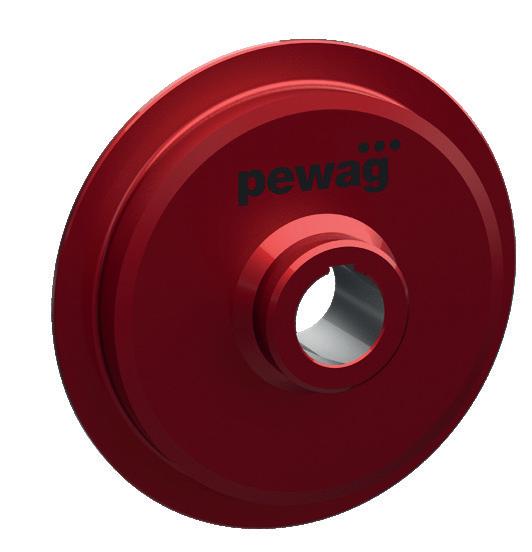
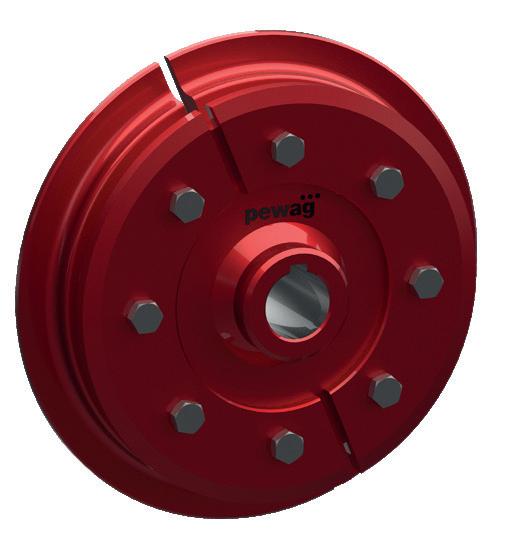
Any other sizes and dimension on request. * Hub length and hub diameter can be specified by the custome.
Example of the order
2 pcs. idler wheels ULR 22/550 for chain 22 x 86, pitch circle dia. = 550 mm
Offset hub: length l = 150 mm, length l1 = 100 mm Hub bore dia. = 80 H7 and keyway acc. to DIN 6885
Available on request with various hub designs or without a machined bore. All dimensions can be supplied. Sprockets are fully customized to match the chain geometry and heat treatment.
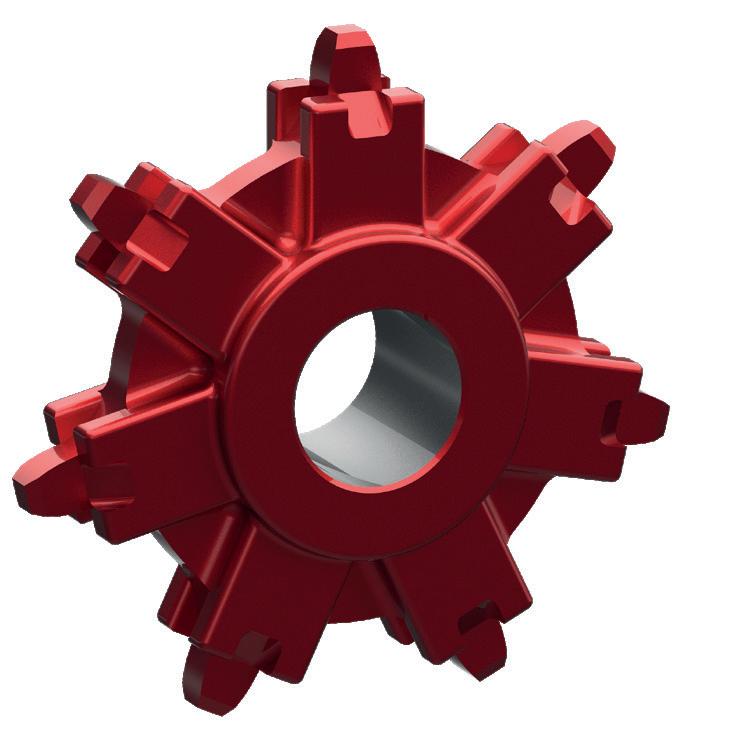
Example of the order
4 pcs. pocket wheels TR 8/9-31 GS 52 for chain 8 x 31, No. of teeth z = 9
Hub bore dia = 50 H7
keyway acc. to DIN 6885
Example of the order
4 pcs. pocket wheels KR 10/10-38 GS 52
E for chain 10 x 38, No. of teeth z = 10
Hub bore dia = 50 H7
keyway acc. to DIN 6885
Example of the order
4 pcs. chain sprockets IR 10/10-38 GS 52 E for chain 10 x 38, No. of teeth z = 10
Hub bore dia = 50 H7
keyway acc. to DIN 6885
pewag chains for military and scrap facilities
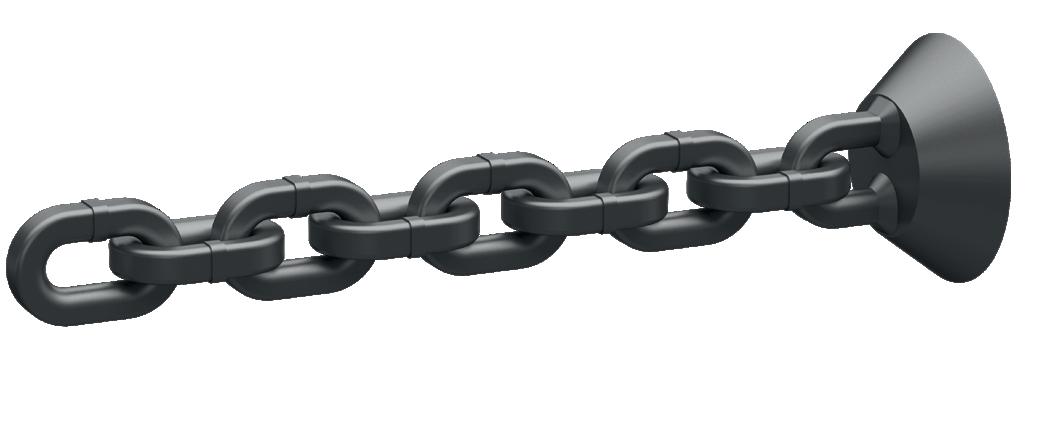
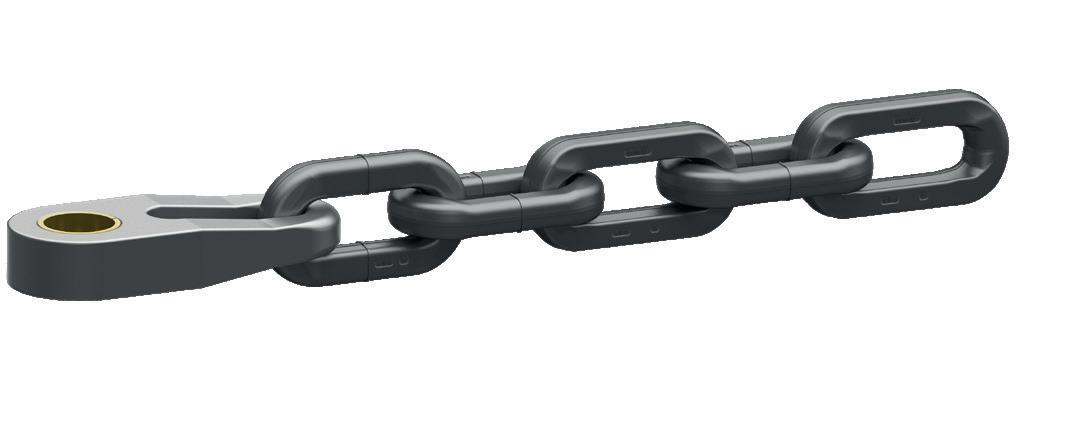
We supply customized chains designed for use in scrap metal recycling plants and demining equipment. These chains are manufactured with a lightly case-hardened surface, and their high tensile strength ensures an excellent service life. Chain dimensions and detailed design parameters are defined by the customer
pewag custom chain wheels
We offer the possibility to manufacture chain wheels precisely according to the specific requirements and drawings of our customers.
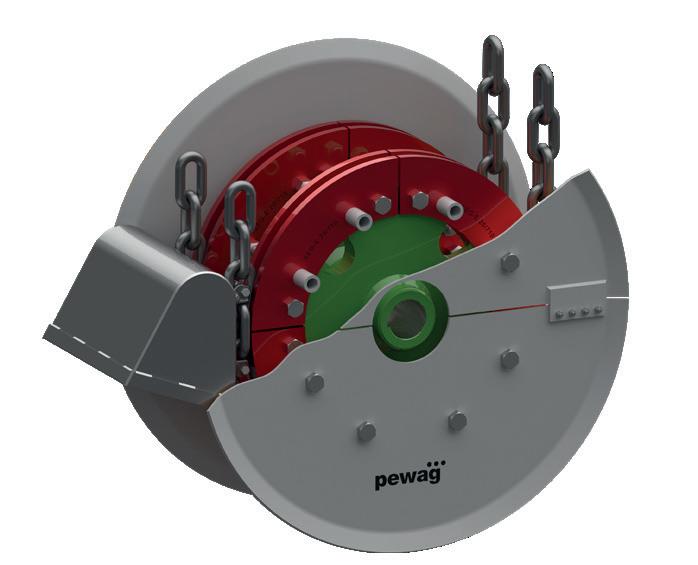
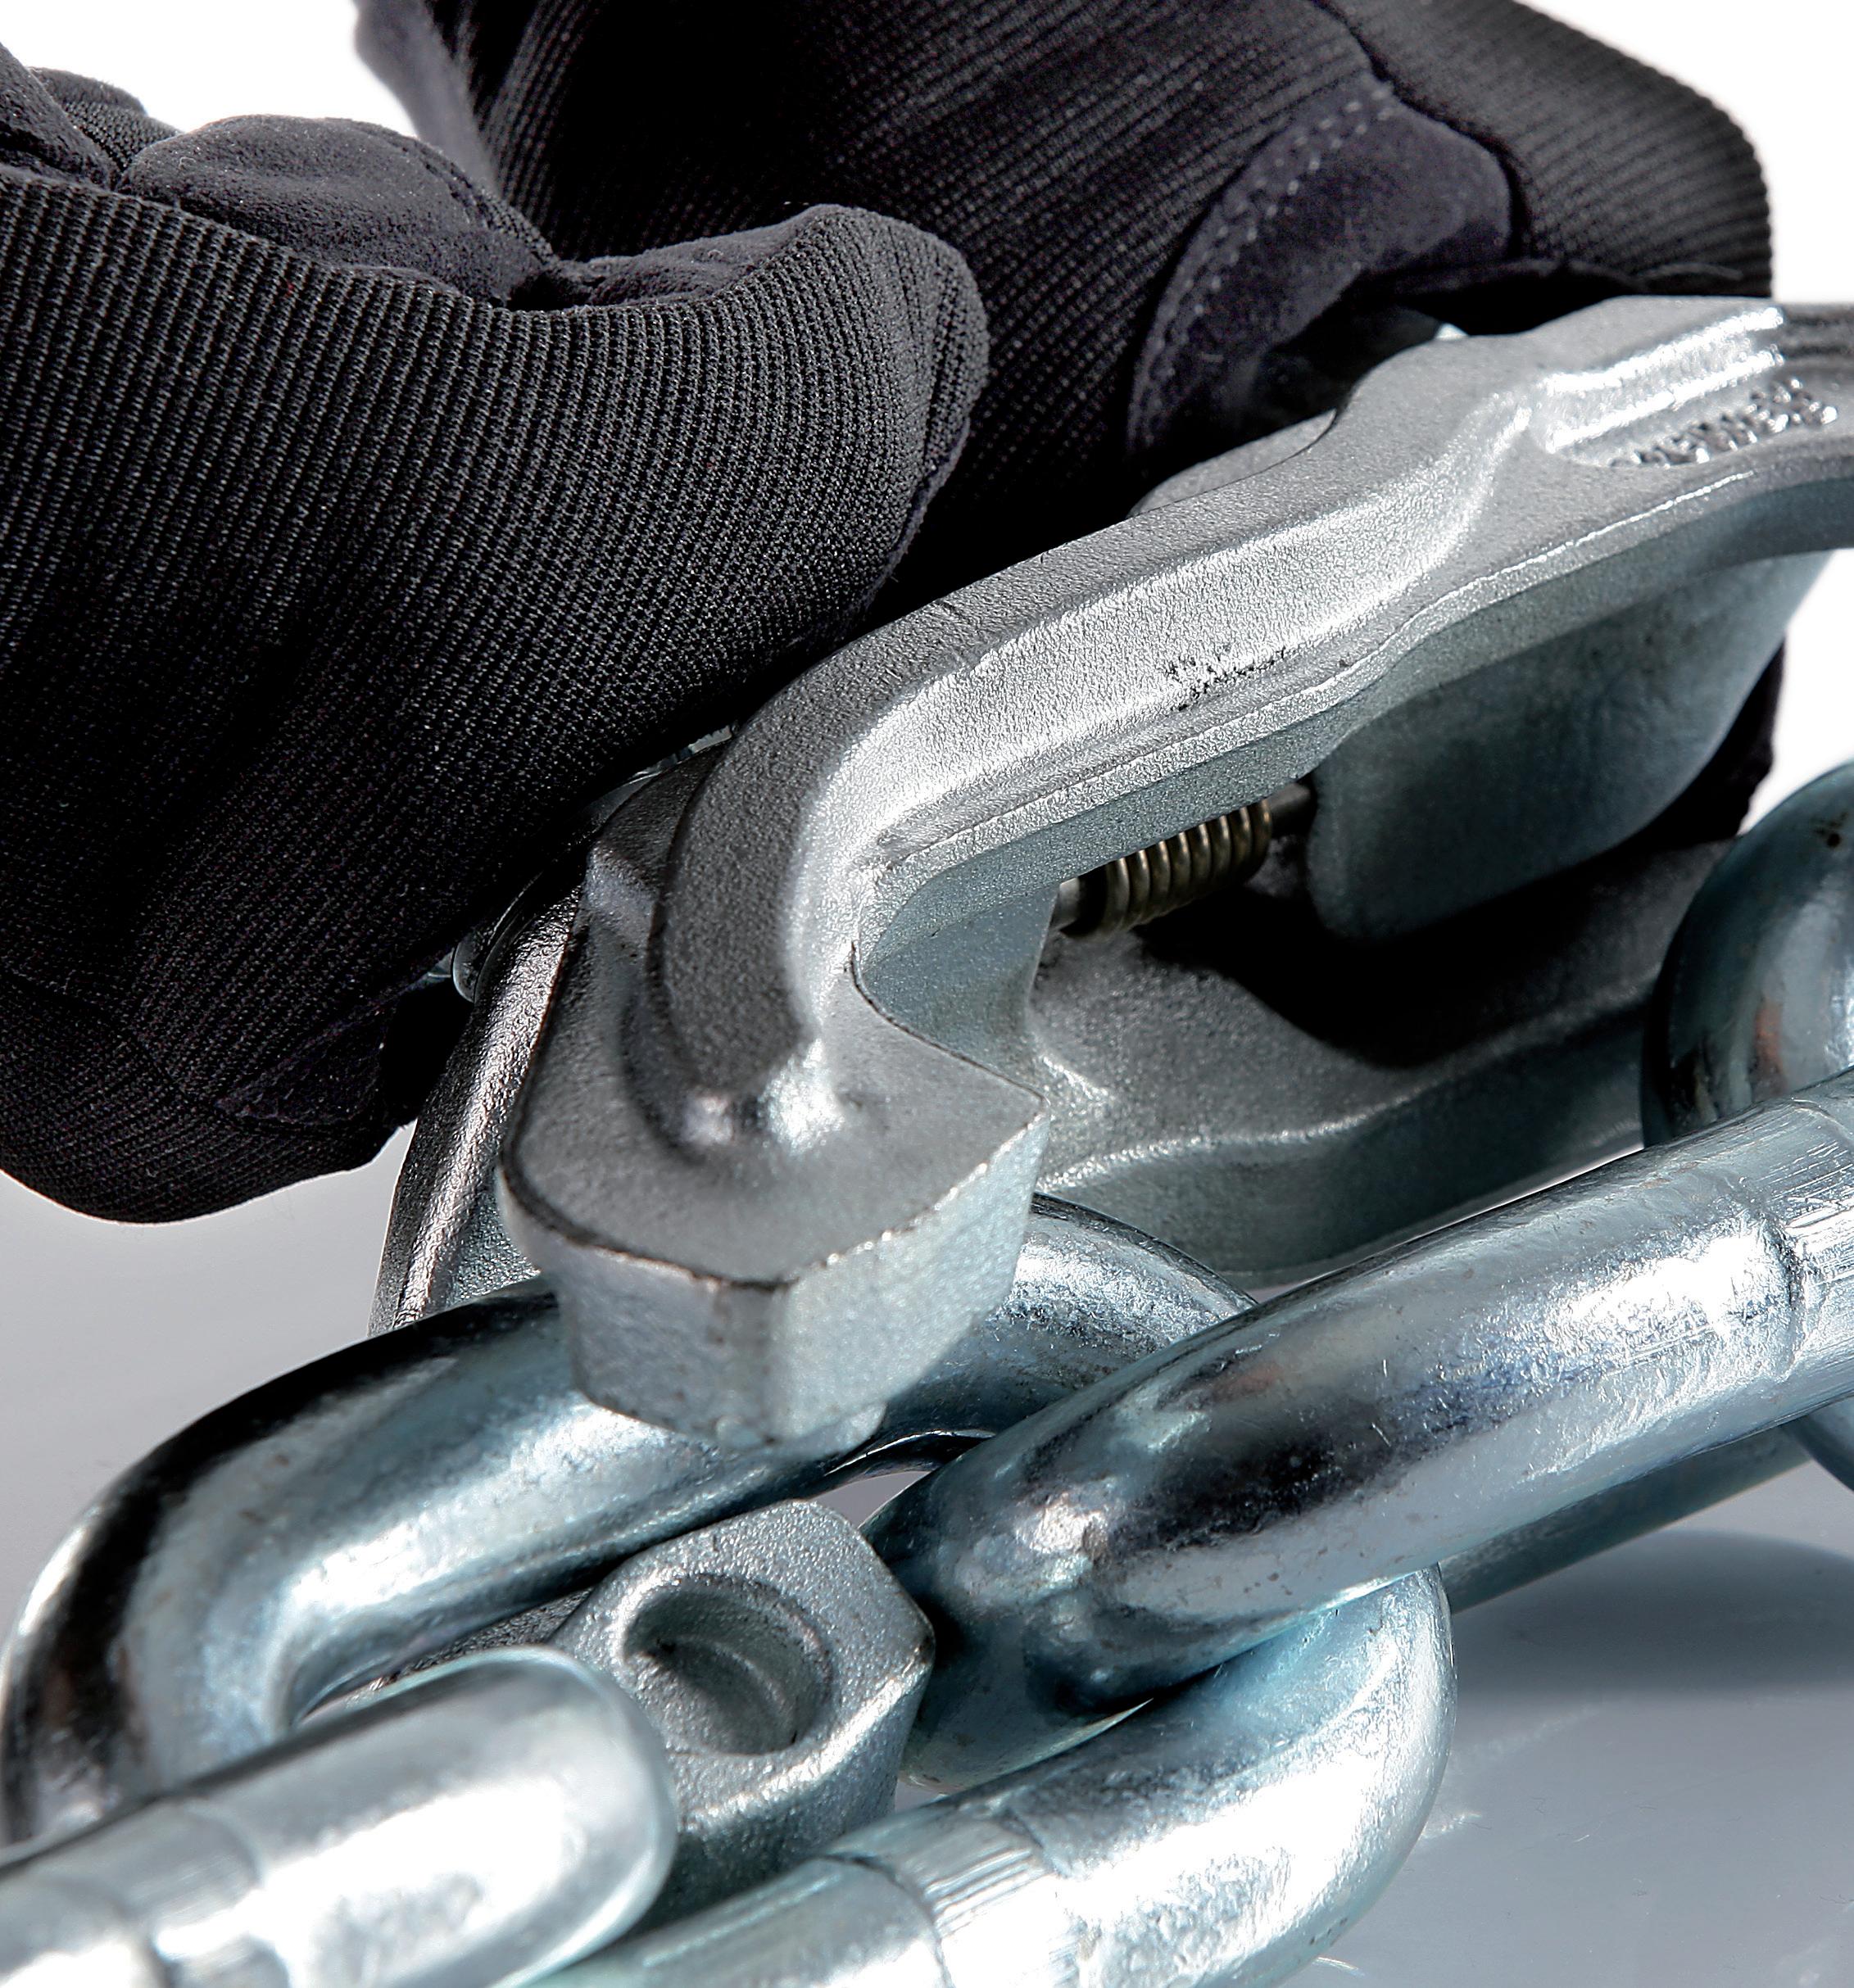
When measuring the actual dimensions, make sure that the chain links are straight and tensioned!
Conveyor / Elevator mark:
Chain dimension:
Annotation: The nominal values may deviate from the actual values. To get exact wear rate results, take the actual “2dnom” and “t nom ” values as a basis for the calculation
2d (method 1) or L-ta (method 2)
During the measuring take care that the chain links are straightened and under tension
Inspection date: Delivery note no.: Left Side
Method 1 (2d – measurement)
2d - total of welded link and full link diameter
Wear rate calculation:
Method 2 (3-link – measurement)
L - outside measurement over 3 links
ta - outside measurement over 1 link
Wear rate calculation:
2d nom – 2dactual t nom x 100 = wear in [%] ( –1)x 100 = wear in [%]
Recommendations:
• Shim plates should be fitted on the RHV(-A)-chain wheels, when the chain is lengthened at a wear rate of approx. 2,5 %.
• The replacement of the chain is recommended at a wear rate of approx. 5 %.
• For friction drive systems the chain replacement is recommended at a wear rate of approx. 5%.
When measuring the actual dimensions, make sure that the chain links are straight and tensioned!
Conveyor / Elevator mark:
Chain dimension:
Inspection date:
Delivery note no.:
L – actual chain lenght over 3, 5, 7 or 9 links
2d – actual dimension over two chain diameters
t – nominal pitch of the chain
Method 1 of wear measurement (3, 5, 7, 9 – links measurement)
Actual lengthening of the pitch due to wear:
t w - actual calculated pitch
Method 2 (2d measurement)
2dactual – actual dimensions over 2 chain diameters 2d nom - nominal dimensions over 2 chain diameters
2d nom – 2dactual t nom x 100 = wear in [%]
L (method 1) or 2d (method 2)
During the measuring take care that the chain links are straightened and under tension
Recommendations:
• Shim plates should be fitted on the RHV-chain wheels, when the chain is lengthened at a wear rate of approx. 2,5%.
• The replacement of the E10 chain is recommended at a wear rate of approx. 3,5%, for E16 chain, when it is 5% worn
• For friction drive systems the chain replacement is recommended at a wear rate of approx. 5%.
Pay attention to maintaining the correct chain center distance; Drive, guide and tail shafts must be installed parallel and all the wheels must be in line.
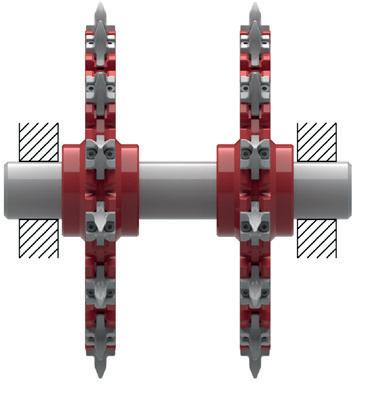
• Connect individual chain lengths with connecting links
• Install the connected chain lengths into the conveyor trough
• Connect into an endless loop
• Assemble the flight attachments and flight bars
• Tension the assembled system
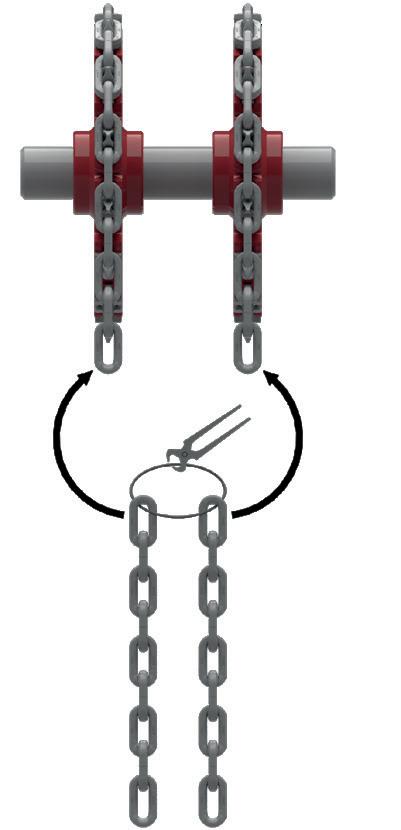
The chain lengths are supplied bundled in pairs. In order to avoid mixing up of the chain lengths, the wire for the bundling should only be opened in the course of the assembly; the chain lengths must be assembled in the conveyor lying parallel, this is the only way to guarantee that chain loops will be of the same length; if the chain lengths are mixed before installation the final links of every chain lengths are marked with the chain length number and are colour coded.
It is possible to get the chain lengths perfectly matched with the chain length numbers resp. the colour marking; during the assembly of the chain lengths please take care that the welds of the vertical chain links point to the wheel center. The position of the other links can be as required.
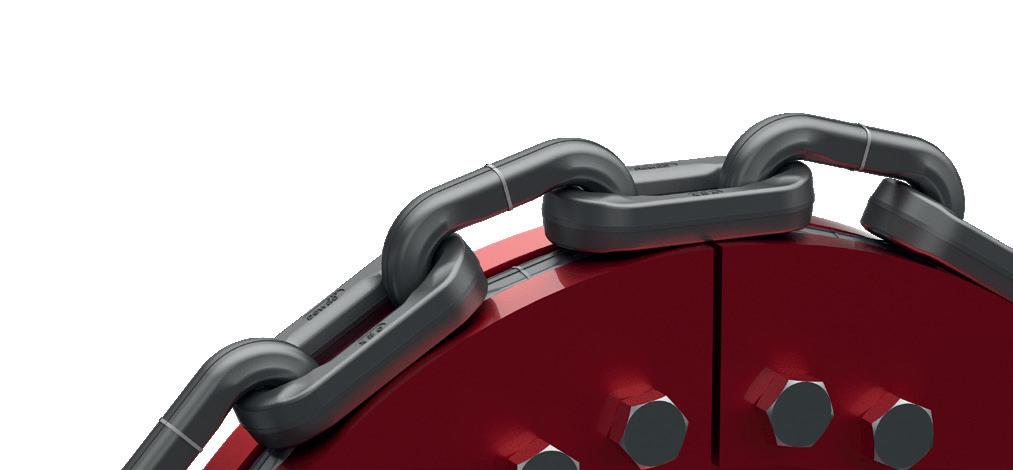
When installing a hero chain, please note that one horizontal link must be a solid forged link (marked with pewag).
It must be insured that the maximum axial offset "X" of the chain relatively to the axis of the chain wheels is not exceeded. The maximum permissible axial offset depends on the groove width of the plane chain wheels.
Make sure, that the clearance "D" is maintained between existing vertical chain guides over chain wheels and the circum radii of the chain.
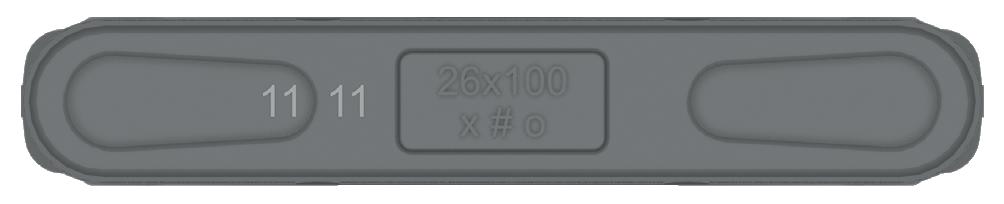
Connecting links V-series can be mounted as vertical or horizontal chain links. Locking lash and connecting link with the same ID-numbers must be used. Locking lash must be mounted on the connecting link showing the marking outside. The locking lash is secured with roll pins. It’s not permissible to mount any attachment to the V-series connecting link.
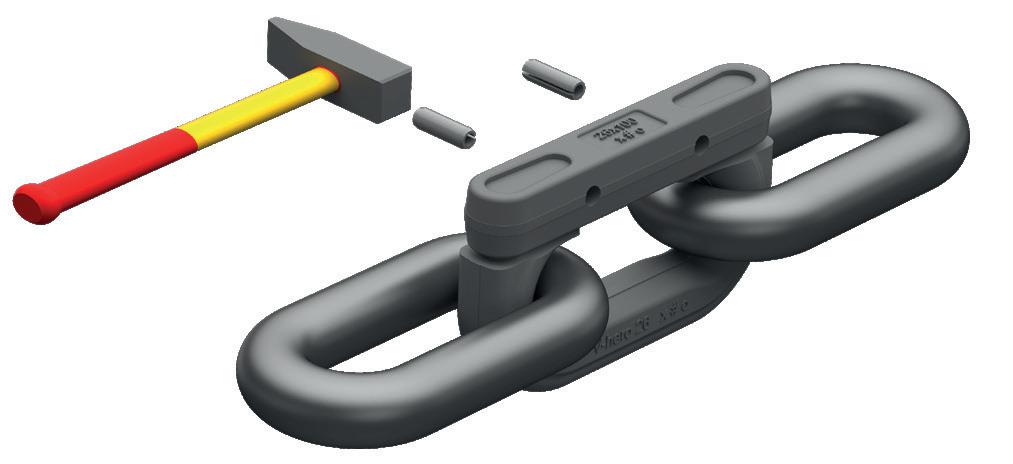
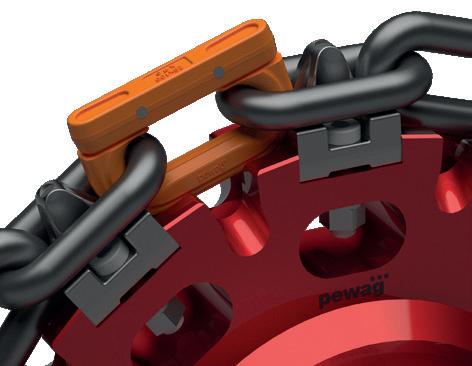
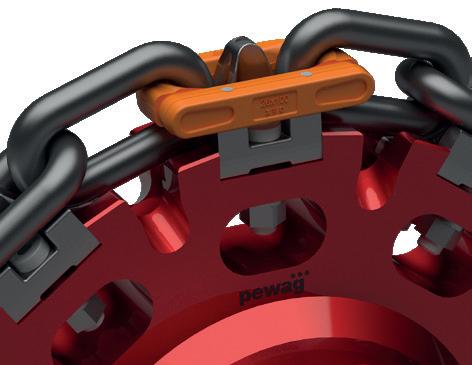
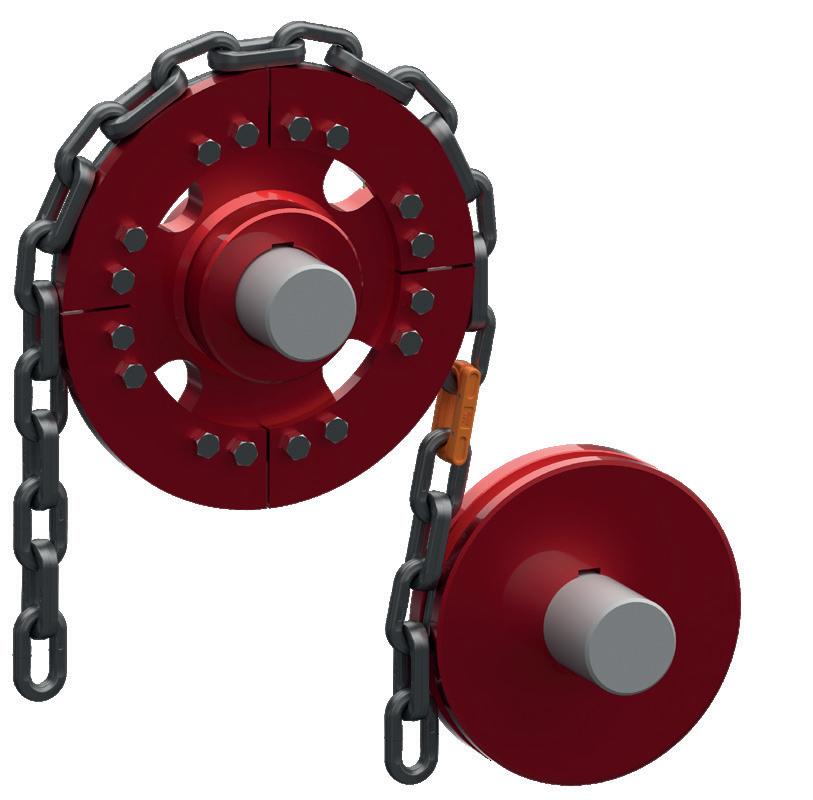
If an idler wheel is used on the conveyor, the V-series chain connecting link must be installed horizontally
When unboxing and assembling the K-Series connecting link, do not join halves from different boxes.
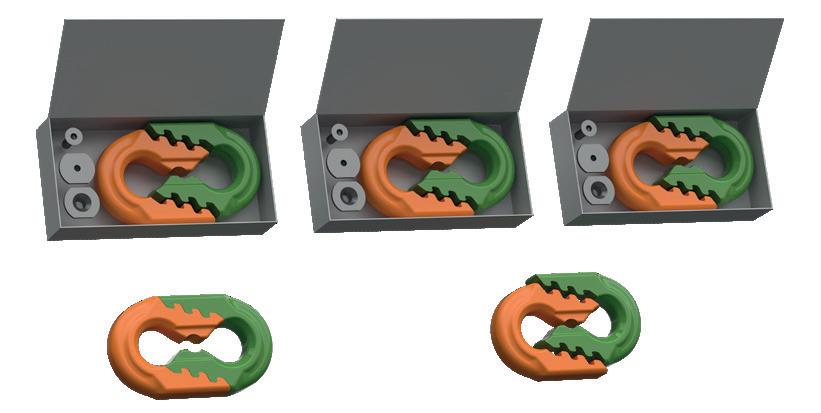
Chain connecting links K-series can only be mounted as vertical chain links for all conveyors and chain systems.
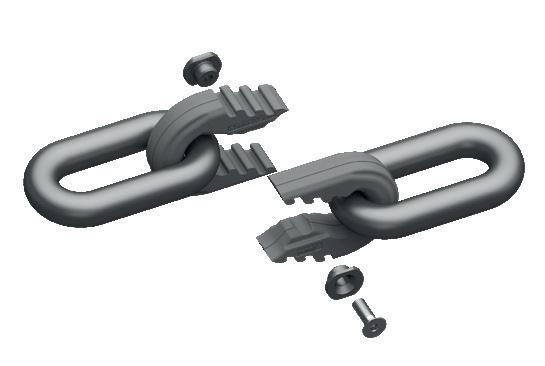
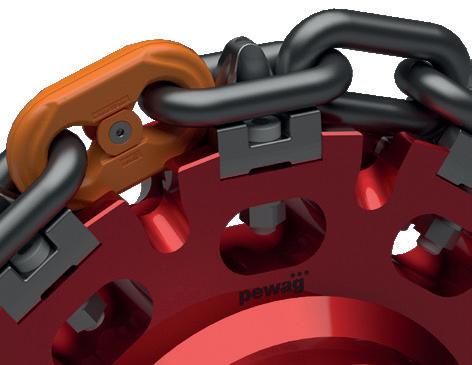
Tighten the countersunk screw to the tightening torque shown in the table below. The screw may only be used once.
The KFB flight attachment should be welded centrally at the end of the flight bars. Keep the attachment square to the flight bar and pay attention to maintaining the tolerance for the chain center when welding. Installation of the flight bar/attachment assemblies is carried out with the chain loop slack. Push together the chain links in horizontal or vertical and install the flight bars at the required flight spacing.
Recommended welding additive: Böhler DMO-IG (EN ISO 21952-A: G MoSi; AWS A5.28: ER70S-A1 (ER80S-G)) or similar additives
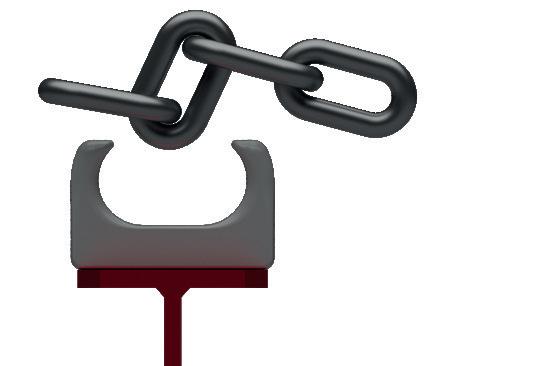
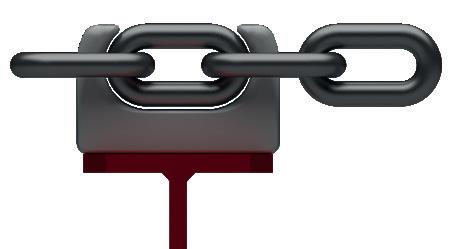
Weld on SDS/SDD with distance plate on bucket/scrapper side wall, pay attention to correct position and alignment. Install the buckets/scrappers on the vertical chain links in the required bucket spacing, insert 2nd SDS/SDD-locking halves and tighten the attachment bolts to the specified torque.
Recommended welding additive: Böhler DMO-IG (EN ISO 21952-A: G MoSi; AWS A5.28: ER70S-A1 (ER80S-G)) or similar additives
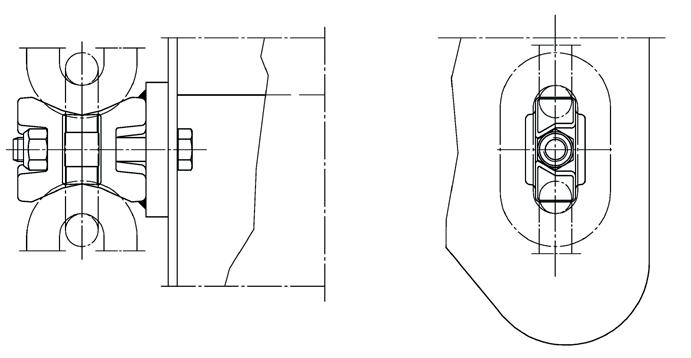
Bolt the BDS halves onto a vertical chain link at the required spacing, aligning them with parallel bolts and the center of the chain link. Tighten the BDS fastening cap screw to the required torque. Screw the buckets together using hex nuts and secure with a lock nut.
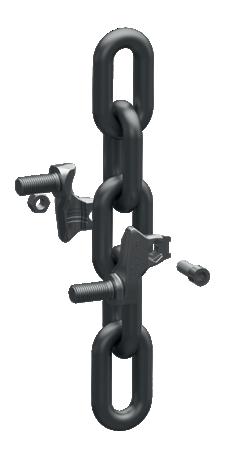
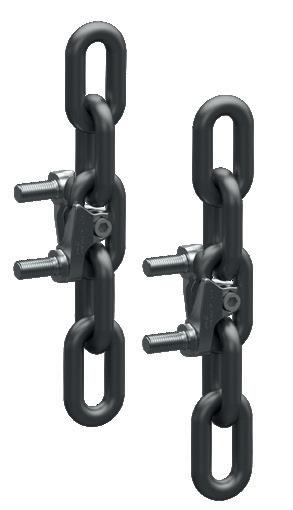
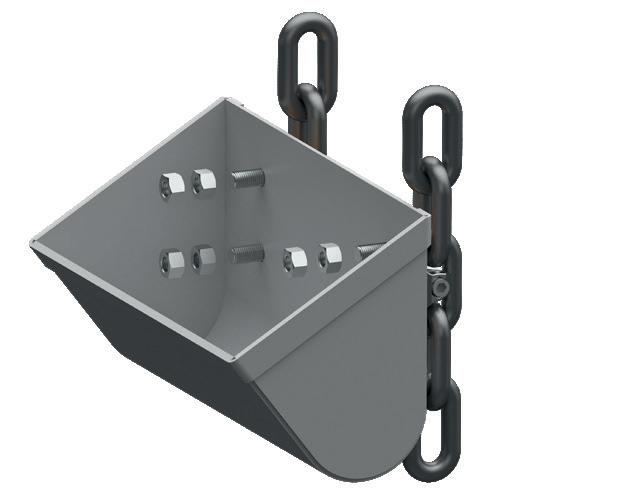
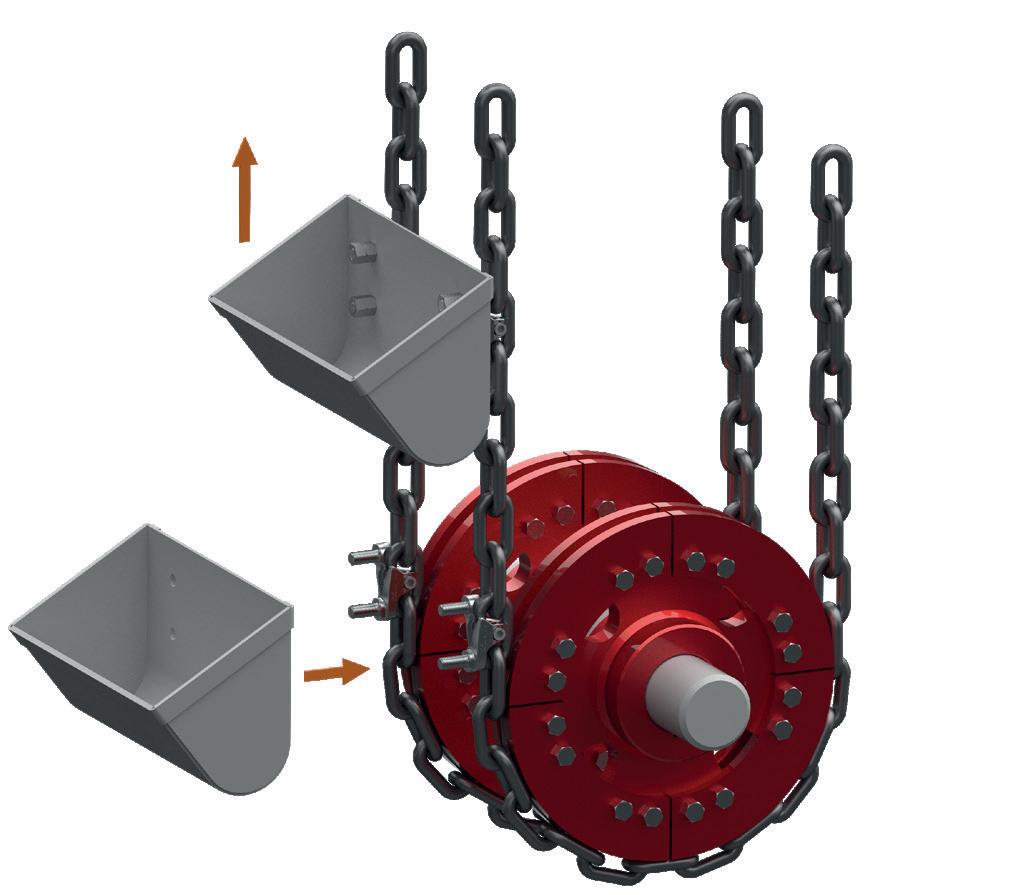
Bolt the BDDS halves onto a vertical chain link at the required spacing, aligning them with parallel bolts and the center of the chain link. Tighten the BDDS fastening cap screw to the required torque. Screw the buckets together using hex nuts and secure with a lock nut.
Chain shackles are connected with the chain ends to form an endless chain loop. Chain shackles should be used together with distance plates. All nuts must be tighten to the enclosed specified torque and secured with safety plates, spring washers or counter nuts to reduce the possibility of loose nuts.
The chain tension must be checked regularly. Untoothed conveyor chain systems + chain shackle systems require a weight pretensioned tail station. Basically, the chain tension should only be as high as it really necessary for troublefree operation. Both chain loops must be equally tensioned. Excessive tensioning will increase the chain wear and reduce the chain life time.
Pay attention to a uniform charging over the full width of the buckets/scrappers. Both chain loops must be equally loaded due to conveying material and chain tractive forces. Asymmetric loading on the chain loops lead sooner or later to an increase in pitch due to wear and to slanting conveyor. Chains should be protected against overloading or blocking against coarse material by means of suitable safety clutches, shear pins etc. At specific intervals the chains, connecting links, attachments and chain wheels should be checked for damage, corrosion or unusual wear.
All screw connections should be checked for tight fit and retightened as necessary. When the chain is replaced, the chain connecting links must also be replaced. No welding should be carried out on chains, connecting links or case hardened components.
The conveying speed should be adjusted to the conveying capacity so that a maximum loading of the flight bars or buckets is achieved.
The chain tension must be checked regularly, especially during commissioning of new chains to check the elongation of the chain due to wear.
Scraper conveyors designed with long sections of unsupported chains require very high pretensioning loads. This can be avoided by supporting the chain with guide rails.
Densely packed material may cause the chain to disengage from sprockets or idler rollers. To prevent this strong rigid chain guide assemblies should be located before, after and around the contact points of changes in chain travel.
The pitch circle dia. of the sprocket RHV(-A) is adapted with shimplates to the individual teeth. Shimplates and new teeth can be installed without disassembling the chain. The thickness of the shimplates can only be determined by measuring the chain lengthened due to wear. As soon as the case hardened layer is worn off the wear will increase rapidly. Chains and sprocket teeth will wear out under normal operating conditions at the same time.
Shimplates should be fitted when the chain is lengthened due to wear by approx. 2,5 %. The replacement of chain with quality grade E10 is recommended by a chain wear of approx. 3,5 % and E16 by 5 %. For friction drive systems the chain replacement should be carried out by an interlink wear of approx. 5 %. If both chain loops wear out equally the max. chain wear per link dia. of approx. 1/5 of the new link dia. is admissible. As soon as the vertical links run onto the groove base of the chain wheels the segments should be replaced.
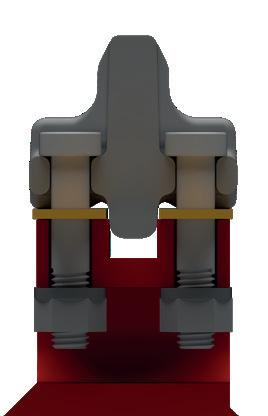
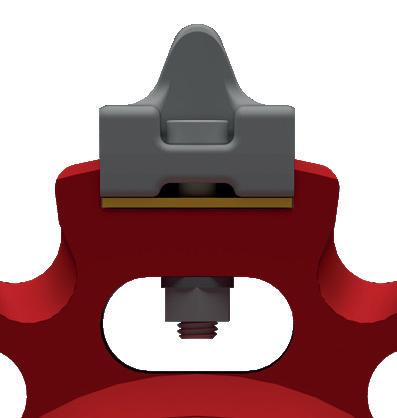
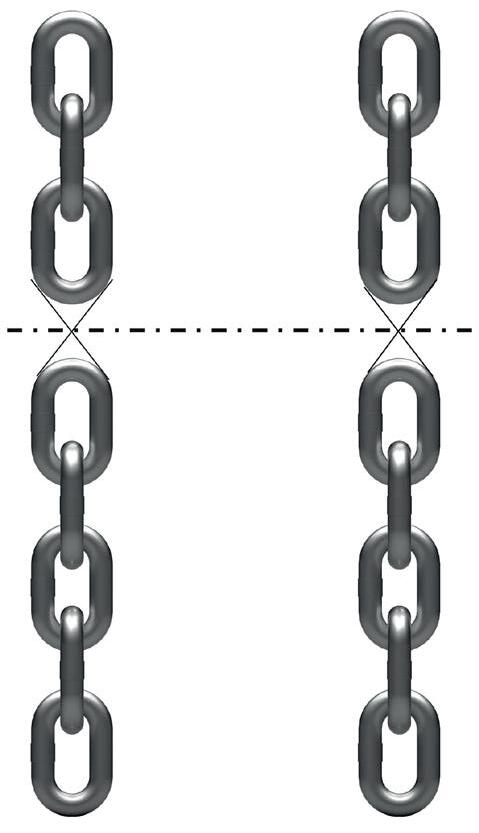
In the course of the initial assembly it may be necessary to shorten the chain in order to obtain the exact required chain length of the make-up lengths, or as chain elongates due to wear.
If chain shortening is necessary an even number of chain links (2, 4, 6, and so on) must be cut out from both chain loops. Links must be cut out with a cutting disc or a burner.
Pay attention not to damage or overheat the neighboring links.
pewag austria GmbH
A-8041 Graz, Gaslaternenweg 4, Phone: +43
saleinfo@pewag.com, www.pewag.com
www.pewag.com