The Leading Protective Coatings Magazine July – September 2026
In this issue: UP FRONT Restoration at the Dollywood theme park in Tennessee ANALYSIS Marine solutions that can benefit floating offshore wind SPOTLIGHT The preservation of cultural icons over the past 50 years
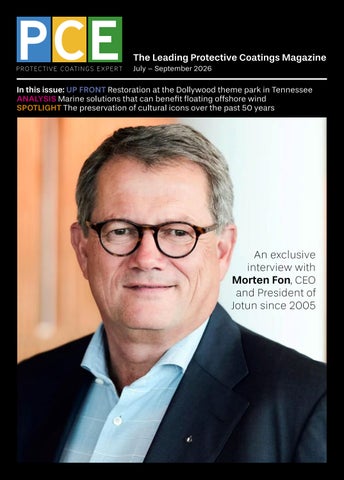
An exclusive interview with Morten Fon, CEO and President of Jotun since 2005
ENVIRONMENTALLY FRIENDLY
ECONOMICAL
HIGH QUALITY
Discover our high-performance
SHIP CLEANING SYSTEMS Hammelmann GmbH Carl-Zeiss-Straße 6–8 59302 Oelde / Germany
mail@hammelmann.de Tel.: (0) 25 22 / 76 - 0 Fax: (0) 25 22 / 76 - 140
Experience the full range of Hammelmann ship cleaning systems:
SAFE
CONTENTS 6 UP FRONT What most don’t know about painting roller coasters, and the restoration of attractions at Dollywood theme park in Tennessee
58 UPDATE With the ongoing challenges and disruptions placing increasing strain on chemical and industrial coatings manufacturers, Forbeats explains how toll processors can help them navigate volatility
The Leading Protective Coatings Magazine July – September 2026
In this issue: UP FRONT Restoration at the Dollywood theme park in Tennessee ANALYSIS Marine solutions that can benefit floating offshore wind SPOTLIGHT The preservation of cultural icons over the past 50 years
An exclusive interview with Morten Fon, CEO and President of Jotun since 2005
Editor: Mark Langdon mark@pce-international.com Advertisement Manager: Nick Carugati nick@pce-international.com Production Manager: Tatum Le Patourel tatum@satzuma-creative.co.uk Designer: Fiona Andreanelli fiona@satzuma-creative.co.uk Accounts: Claire Long claire.long@mpigroup.co.uk Publisher: Andrew Deere andrew.deere@mpigroup.co.uk MPI Group Peel House, Upper South View Farnham, Surrey GU9 7JN, England Tel: +44 (0) 1252 732220 Email: info@mpigroup.co.uk www.mpigroup.co.uk MPI Group, as a body, is not responsible for any opinions expressed in PCE by contributors. All rights reserved. No part of this publication may be reproduced, stored in a retrieval system, or transmitted, in any form or by any means, electronic, mechanical, photocopying, recording or otherwise, without prior permission of MPI Group. © Marine Publications International Ltd 2021
CONTENTS PCE JULY – SEPTEMBER 2026
46 IN FOCUS Flyability and MaDfly recently performed the first UAV inspection of methanol fuel tanks on a container ship and PPG looks at rethinking onboard ship maintenance
86 NEWS The latest products, appointments and industry news
J U LY – S E P T E M B E R 2 0 2 6
32 LIFTING THE LID Safinah looks beyond glassflake content, Teknos explores coating qualification for the emerging CCS infrastructure and AkzoNobel investigates why passive fire protection shouldn’t be treated like ‘just paint’
76 CORRODERE ACADEMY The latest articles, news and directory listing from Corrodere Academy
PROTECTIVE COATINGS EXPERT
22 SPOTLIGHT The restoration team at John Canning & Co looks back on the company’s past 50 years and how paints, coatings and the technology used have changed during that time
Volume No.19 Issue No.3 ISSN No. 2054-1813
64 REVIEW How Walco Industries completed a three-day hydrodemolition project in a working port, and why Finnish forestry machine manufacturer Ponsse puts its trust in Teknos
2 BENEATH THE SURFACE An interview with Morten Fon, CEO and President of Jotun since 2005, on the paint major’s 100th anniversary
16 ANALYSIS With floating offshore wind entering a new phase of commercial development, PPG investigates how marine solutions could benefit the sector
1
2
BENEATH THE SURFACE
BENEATH THE SURFACE PCE JULY – SEPTEMBER 2026
MORTEN FON, CEO & PRESIDENT OF JOTUN SINCE 2005, TALKS TO PROTECTIVE COATINGS EXPERT
Jotun now and in the early days (inset)
3
BENEATH THE SURFACE PCE JULY – SEPTEMBER 2026
Jotun started with marine coatings from its very beginning in 1926. Founded in Sandefjord, Norway, with a shipyard just across the fjord, the company first supplied coatings to the local whaling industry. As shipping patterns changed and Norwegian shipowners increasingly transported oil, Jotun’s role evolved alongside them, gradually extending its reach well beyond Norway. Shipping has never been static, and neither has Jotun. Over the decades, both regulation and technology have driven significant change, often requiring rapid adaptation. Reaching a 100-year milestone naturally invites reflection. For Jotun, it is also about looking forward – anchored in a strong corporate culture that has remained consistent through decades of growth and change.
4
BENEATH THE SURFACE PCE JULY – SEPTEMBER 2026
Q. Jotun is currently celebrating its 100th anniversary. How does Jotun compare now, with then? A. In the beginning Jotun was a small Norwegian company that focused on the Norwegian marine coatings market. Today it is a global paints and coatings company focusing on four segments: marine coatings, protective coatings, powder coatings and decorative paints. Jotun has built strong positions in the four segments globally, but Scandinavia, the Middle East and Asia are strongholds where Jotun holds a very strong position. The majority owner throughout the 100 years has been the Gleditsch family, with Orkla as the partner since 1972. Q. What do you think has been the biggest change Jotun has seen since 1926? A. The biggest change has been going from a small Norwegian company to become global and to hold the Number Seven position globally within the overall paints and coatings market, and the leader within marine coatings. Today Jotun is developing
based on a strong reputation and delivering advanced products and solutions of high quality delivered by an excellent organisation worldwide. Q. You have been CEO and President since 2005. What were your main aims when you first took the job? A. From the beginning I focused on two elements that have been very important over the last 21 years: First to continue to build a solid corporate culture, based on strong values – respect, boldness, loyalty and care. Secondly, strengthen the organic growth strategy and make sure we focused on the four selected segments to grow the company organically and continue to adapt to markets around the world. This has proved to be successful: Jotun has grown faster than the competition and we have been creating value for shareholders. Q. Do you think you have managed to achieve all of these, or do you think you still have more to do?
A. I believe that we can do more of the same based on the same factors, but we also have areas that we need to develop. Growing the company is important and growing organically is our Jotun way. The best way is to deliver products, solutions and services that are better than our competitors. At the same time, we must become more efficient day by day.
A. Jotun must be in the forefront of technology, and we must continue to invest in R&D within our focus areas and develop new products, solutions and services that are bringing the industry forward. One example is the HullSkater, a part of our Hull Skating Solutions, where we have been thinking “outside the box”, and developed robotics for cleaning hulls today and in the future.
Q. There always seems to be consolidation going on within the paint industry. Is Jotun looking to expand in this way in the future?
Q. What about Morten Fon outside Jotun – what do you do to relax and what hobbies do you have?
A. Jotun will stick to our organic growth strategy; hence we will not be part of any consolidation or restructuring of the industry. We will continue to develop organically. There is one exception to this, and that is to buy companies that have technology that we can fit into our portfolio, and within the four segments.
A. My family and my social life outside Jotun have always been important to me, and I have been playing golf for many years in addition to some sailing. Q. Is there anything you would like to add? A. Jotun has been giving me lots of opportunities to develop and I would like to see that other penguins (we call our employees penguins) have the same opportunity. I hope I have been a good role model when it comes to career development after 37 years in the company. ■
BENEATH THE SURFACE PCE JULY – SEPTEMBER 2026
Q. What do you think are the biggest challenges for Jotun going forward, and what plans are you putting in place to meet these challenges?
5
6
UP FRONT
UP FRONT PCE JULY – SEPTEMBER 2026
ON A ROLL: WHAT MOST DON’T KNOW ABOUT PAINTING ROLLER COASTERS
It is not every day you get to work on the kind of structure people plan holidays around, take photos of and point to from across the park. Coasters are big, bold, iconic and a little intimidating up close – which is exactly what makes them such a cool canvas, says Melissa Bamford, Director of Marketing at the USA’s Baynum Solutions.
HullSkater, part of Jotun’s Hull Skating Solutions
UP FRONT PCE JULY – SEPTEMBER 2026
7
8
R
oller-coaster painting is full of details most people would never think about. It is not just picking a colour and covering steel. A coaster is a moving, working ride system, and that makes the job a lot more specialised than it looks from the ground. There are areas you paint, areas you protect, areas you test and sometimes areas you intentionally leave alone. Every decision must account for the ride itself, the coating system, the park environment and the people who will be riding underneath it when the season starts.
The no-paint zone One of the most interesting details in rollercoaster painting is knowing where not to paint. On many steel coasters, there is a visible worn area on the running rails where the road wheels ride. That wear path shows exactly where the train contacts the rail.
UP FRONT PCE JULY – SEPTEMBER 2026
That area is not just part of the paint job; it is part of how the ride operates. Because paint on the running surface can affect friction and ride performance, crews are often directed to stay off that wear path. In many cases, that means holding the coating back approximately 1/4 inch (6mm) from the visible line. There are exceptions. On some rides, or in some specific situations, the owner or manufacturer may request that the rail be painted fully if it does not create the same operational concern. But either way, it is not random. The decision is intentional, and it is one of those small details that makes coaster painting different from painting a normal steel structure.
One giant ride – a roller at a time A lot of roller-coaster painting is done by brush and roller. From the ground, it seems as if something that large would obviously be sprayed. But in a park environment, spraying can create major overspray concerns.
Coasters are surrounded by buildings, queue lines, ride vehicles, signs, landscaping, pathways, other attractions, water features, lighting, guest areas and finished surfaces.
9
And with the specialised industrial coatings used on steel structures, overspray is not just a little mist that disappears. Many of these coating systems are urethanes or similar high-performance coatings, and those particles can travel much further than people expect if wind and conditions are not carefully controlled. Brush-and-roller lets crew work around running rails, hardware, catwalks, brake areas, station components, platforms, transitions and sensitive surroundings without sending coating where it absolutely does not belong. It is slower – it is more physical – it takes patience. But there is something amazing about watching a massive coaster come back to life, one rolled section at a time. A coaster repaint is not as simple as picking a new colour and getting to work. The coating that is already on the ride matters. What was used before can determine what can be applied next, how the surface needs to be prepared and whether the new coating system will bond properly. Crews also must consider the ride manufacturer’s requirements, the environment, exposure and the coating manufacturer’s recommendations. Even the colour changes matter. Not every colour covers the same way. A dramatic colour change may require additional coats – and on a roller coaster, one more coat does not mean touching up a wall; it means touching up the whole structure again. That is where testing and paint manufacturer support can play a big role. Pull tests, coating evaluations and technical support help determine what system should
UP FRONT PCE JULY – SEPTEMBER 2026
Old paint gets a vote
10
be used. Paint OEMs will often help write the specification that applicators follow, so the project starts with the right plan instead of guesswork.
The view is great and the sway is real
UP FRONT PCE JULY – SEPTEMBER 2026
One of the wildest parts of the job is that when you are up there painting, you can actually feel the coaster move. Not in a dramatic, something-is-wrong way, but in a roller-coasters-are-built-to-move way. From the ground, that idea feels technical. From the lift, basket or tie-off point, it feels very real. That is the part people do not think about when they see a freshly-painted coaster from the ground. The work is not happening on a flat wall or a quiet building. It is happening in the air, on a ride structure, with a view most people will never get.
WHERE FADING MEETS PROTECTION: RESTORING AN ICON IN THE SMOKIES Dollywood theme park in Tennessee doesn’t shout for attention: it’s layered into the landscape. Nestled in the foothills of the Smoky Mountains, its rides don’t just sit
on the terrain; they disappear into it. That’s exactly what made the restoration of the Tennessee Tornado roller coaster such a unique coatings challenge, and ultimately, such a rewarding one.
11
Some projects start with a bid, but this one started with a climb. In 2013, Baynum’s team conducted an initial walkthrough of the Tennessee Tornado, bringing a NACE Level 2 Coatings Inspector to evaluate the original factory-applied system. Test patches were applied directly to the structure – high above the terrain – validating adhesion, compatibility and long-term performance potential. Then the story paused. The ride kept running and the mountain kept growing. Over the years, as Dollywood continued to thoughtfully invest across the park, the Tennessee Tornado project remained part of the broader conversation until the right window arrived in 2024. When the project was ultimately awarded, the groundwork had already been laid, technically and strategically.
UP FRONT PCE JULY – SEPTEMBER 2026
Taking test samples on the Tennessee Tornado
12
When fading works – until it doesn’t There’s a nuance here that makes this project different. Over time, the original finish naturally faded – creating a weathered, rust-toned appearance that blended seamlessly into the Smoky Mountain backdrop. It wasn’t designed that way, but it worked. The ride settled into its environment in a way that felt authentic to the park’s setting. But aesthetics does not drive coatings decisions: protection does. At a certain point, the equation shifts – from ‘it works visually’ to ‘it must perform structurally’. That’s when Dollywood made the call.
Access defines everything The Tennessee Tornado was installed in 1999 – long before the surrounding landscape matured and the park expanded around it. Today, access is the issue: steep terrain, dense growth, limited staging areas and minimal direct approach to large portions of the structure.
Tennessee Tornado before restoration
To execute the project, Baynum deployed: • 135ft (41m) and 85ft (26m) boom lifts for primary access • Specialised spider basket systems for the lift hill
UP FRONT PCE JULY – SEPTEMBER 2026
• Multi-position setups to reach over 2,700ft (820m) of track, rising to 163ft (50m). This is where Baynum’s crews operate at their best: in environments where conventional access simply doesn’t work.
Precision over speed Unlike many industrial applications, these rides are not spray-coated; they are brush and roll only. Because in a guest environment, especially one embedded in terrain like this, coatings can’t travel – containment isn’t optional. Every square foot of structural steel is coated manually, ensuring:
13
• Controlled application • Proper film build • Zero unintended impact to surrounding areas. It’s slower – more deliberate – and exactly what the project demands. The coatings system was designed to halt corrosion, stabilise existing substrates and deliver long-term durability, all while maintaining the existing colour profile. Surface Preparation Standards: • SSPC-SP1: High-pressure cleaning up to 5,000 psi with biodegradable degreasers • SSPC-SP2: Hand-tool cleaning (scraping, sanding, wire brushing) • SSPC-SP3: Power-tool cleaning (grinders, dual-action sanders, wire wheels)
The Shooting Star undergoing restoration
UP FRONT PCE JULY – SEPTEMBER 2026
System and surface preparation
14
Flat rides, fully reimagined While the Tennessee Tornado tells a story of scale and access, Dollywood’s Shooting Star and Sky Rider attractions highlight precision, theming and guest-facing detail. Shooting Star: A thematic revival This Zamperla junior drop tower is designed for families, and its visual presence matters just as much as its operation. The goal wasn’t just to repaint; it was to restore and elevate the ride’s original theme. • Full structural refresh with red, white and blue colour scheme Shooting Star seat repair
Coating System: • Rust conversion • Primer: Sherwin-Williams Macropoxy 646 • Finish: Sherwin-Williams Sher-Loxane 800 Semi-Gloss The project was executed in two phases: • Guest-visible sections along the midway
UP FRONT PCE JULY – SEPTEMBER 2026
• Remaining track and lift hill tucked deep within the terrain.
• Gradient detailing reintroduced in upper sections • Gondola restoration (FRP), including: • Complete sanding and surface preparation • Spot repairs to damaged fibreglass • High-finish repaint system for durability and appearance. Executed using high-detail spray techniques, this project leaned into Baynum’s thematic finishing capabilities: combining coatings performance with visual accuracy.
A classic, renewed
Sky Rider: Precision & consistency at height
What began as an evaluation years earlier ultimately became a full restoration of one of Dollywood’s most recognisable attractions.
A Chance Rides Aviator attraction, Sky Rider lifts guests 70ft (21.3m) into the air, putting every detail on display.
For Baynum, it was the kind of project that defines the work: technical planning, difficult access, precise execution and respect for the ride’s original character. For Dollywood, it meant extending the life of a modern classic. “Baynum has been a great partner in helping us maintain and conserve our more classic attractions,” said Barry Stiltner, Director of Maintenance. “The Tennessee Tornado, for example, is the last Arrow coaster, and thanks to Baynum, it looks better than it did when we opened it in 1999.”
Scope included: • Structural steel coating system (epoxy + polysiloxane) • Replacement and stencilling of star elements • Full treatment of sweeps, mast and ride vehicle hardware. Coating System • Primer: PPG Amerlock 2 Epoxy • Finish: PPG PSX 700 Polysiloxane.
Working against the season This work happens in the off-season, when conditions are far from ideal. Crews operate through: • Fluctuating temperatures • Moisture variability • Tight, non-negotiable timelines. Baynum adapts with specialised materials and adjusted application methods that
allow coatings to perform even in colder conditions.
15
Safety at every elevation Working at heights exceeding 150ft (46m) across irregular terrain requires more than standard safety protocols. Crews operate with: • Full fall protection systems • Engineered access solutions • Continuous hazard assessment across changing elevations. In this environment, safety is constant, not conditional.
More than a coating project What makes projects like these stand out isn’t just the scale or the technical execution; it is the balance. Preserving the character of beloved attractions, protecting critical assets and ensuring the guest experience feels as timeless as the memories attached to it. At parks like Dollywood, the best off-season work is often the kind guests never notice – they simply enjoy the ride. ■ Work in progress on the Tennessee Tornado (left) and Sky Rider (below)
UP FRONT PCE JULY – SEPTEMBER 2026
The result is a clean, consistent finish designed to withstand environmental exposure while maintaining visual clarity across all ride elements.
ANALYSIS PCE JULY – SEPTEMBER 2026
16
17
ANALYSIS
Floating offshore wind is entering a new phase of commercial development. Floater designs are continually being refined to meet the needs of deeper waters and greater energy demands. The options for offshore infrastructure assets are rapidly expanding; even data centres could one day be co-located in floating offshore wind sites with platforms like Aikido Technologies’ modular prefabs, says Chris Magel, PPG Oil and Gas Segment Manager, Europe, Middle East and Africa, Protective Coatings.
ANALYSIS PCE JULY – SEPTEMBER 2026
MARINE SOLUTIONS BENEFIT FLOATING OFFSHORE WIND
18
W
ith the development of new floating offshore wind technologies, protective coating systems must also adapt to a new set of challenges. Floating wind platforms are too large to be transported overland and therefore spend a great deal of time in the water during staging and assembly. They require specific port resources and water depths, which result in global sourcing practices and long transport distances for some components. During operation, floating wind towers must withstand continuous wave action, high winds, vibrations and seawater immersion over design lives of 30 years or more. These structures occupy a hybrid space between vessel and wind tower, demanding a combination of marine and energy-grade coatings to prevent corrosion and extend asset service life. For floating wind towers, high-performance protective systems need to reduce the attachment of marine organisms during transport, protect ballast tanks from pitting and cracking and resist impact damage from debris and other vessels.
Wind towers with marine components
ANALYSIS PCE JULY – SEPTEMBER 2026
Compared with fixed-bottom offshore wind towers, floating towers have a unique set of requirements. Floaters borrow aspects from marine engineering designs to maintain stability in deep waters instead of relying on monopile or jacket foundations built into the seabed. There are four main types of platform design in use today, although many other variations have been proposed. Semi-submersible platforms and spar buoys are the most common to date. • Semi-submersible structures use multiple ballasted columns • Spar buoy platforms have a large cylindrical ballast tank that extends deep below the water
• Tension leg platforms rely on taut mooring lines anchored to the seabed to limit platform movement • Barge designs use buoyancy from a broad, shallow floating platform to support the turbine. For maximum power generation, the industry is moving toward larger turbines. In China, the 16MW Three Gorges Pilot turbine has a rotor diameter of over 800ft (250m). Supersized components increase manufacturing, transport and installation complexity and place greater demands on every aspect of the turbine’s sourcing and construction. These floating structures also endure some of the most aggressive environmental conditions in the world, including extreme temperature fluctuations and high wind speeds and wave heights from storms.
Why asset protection strategies must adapt As floating offshore wind projects seek funding, the levelized cost of electricity (LCOE) is an important metric used to evaluate site and design decisions. Lowering the LCOE can help make a proposal more competitive. Material selection, and protective coatings in particular, play a direct role in calculating LCOE and influencing asset service life. Highly durable coatings that can maintain protection in the demanding conditions of offshore wind farms can help protect structural integrity and support longer turbine service life expectations. Extending the service life expectation of a turbine helps lower its LCOE, but it also has the potential to increase operation and maintenance costs if the structure requires frequent maintenance. Repairing damaged coatings in offshore environments is much more complex and costly than performing maintenance in a fabrication yard. Crews must be specially
Surface preparation often requires power tools to remove corrosion and deteriorated coating before the new coating can be applied. Rinses between coating layers remove salts that could otherwise contribute to osmotic blistering and premature coating failure. Undetected coating failures are also more likely to happen in remote offshore wind installations, which could jeopardise the operation and power-generating ability of the entire turbine. Owners and developers need corrosion protection systems that minimise maintenance requirements and simplify repair procedures. Coatings that combine long-term durability with efficient application can help reduce total lifecycle costs.
Reducing environmental impact Beyond cost reductions, there is another layer to coating selection for floating turbines. In the renewable energy sector, projects can be evaluated based on environmental metrics such as reducing carbon emissions or protecting biodiversity. While sustainable production practices are not currently standardised, regulatory frameworks and guidelines are emerging, and many organisations have set voluntary goals to reach net-zero carbon emissions. Some governments require developers to submit an Environmental Impact Assessment (EIA), which is informed by the EU’s EIA Directive. Environmental product declarations (EPDs and lifecycle assessments – LCAs) are also increasingly used to provide environmental information for materials and technologies. LCA methodologies are addressed in ISO 14040 and ISO 14044, while the availability of EPDs and LCAs varies by specific product and technology. According to the World Forum Offshore Wind (WFO), the fabrication stage is responsible
for the highest amount of carbon emissions in the offshore wind value chain, making material innovation a key part of improving environmental performance. Within the coatings industry, these priorities are encouraging the development of formulations designed to reduce VOC emissions and avoid certain substances of concern. Some formulations can also be applied without the addition of thinners, which may help reduce VOC emissions associated with application, as well as the shipping and packaging, associated with thinners.
19
The latest innovations in protective coating technologies can help developers meet performance requirements while supporting more sustainable solutions for floating offshore wind towers.
Fouling prevention during transport Another emissions-intensive process is the transport of wind tower blades, nacelles, tanks and platforms to the wind farm site. Biofouling from marine organisms directly affects fuel consumption during transport. Accumulated clusters of molluscs or barnacles increase surface roughness and hydrodynamic drag during tow-out operations. Research estimates that biofouling can significantly add to the mass of floaters and mooring lines, with some models indicating an increase of up to seven per cent on the platform alone. In marine vessels, drag caused by biofouling has been studied extensively, and the highest increases in drag are observed on vessels that operate at lower speeds. Slower vessels are more susceptible to the growth of biofouling, meaning that large floating wind tower components in wet storage or being towed out to sea are particularly vulnerable to the effects of marine fouling. Marine organisms can cause damage to coating systems, leaving steel substrates unprotected. Their adhesion can also result in the spread of invasive aquatic
ANALYSIS PCE JULY – SEPTEMBER 2026
trained to perform work on floating structures and properly carry out coating application procedures.
20
species when wind tower components are manufactured in one location and transported to another region. These challenges make antifouling coatings, which have a long history of use on commercial vessels, a valuable addition to floating offshore wind protection strategies. By reducing the attachment of marine organisms, appropriate antifouling systems can help limit increases in surface roughness and hydrodynamic drag during transport. Reducing biofouling may also help lower the risk of transporting non-native organisms between regions.
Corrosion protection in ballast tanks
ANALYSIS PCE JULY – SEPTEMBER 2026
Ballast tanks are another critical area where floating offshore wind platforms benefit from coating technologies developed for the marine industry. These internal compartments provide the ballast needed to maintain platform stability, and are subjected to continuous or intermittent seawater exposure. Ballast tanks are also very difficult to inspect and maintain. Corrosion that occurs at weld seams can lead to leaks, which could compromise the structural integrity of the tank. Heavy-duty epoxy linings provide resistance to seawater immersion while maintaining the flexibility needed to accommodate the thermal cycling and variable loads found in floating structures. Coating systems that meet the International Maritime Organization’s Performance Standard for Protective Coatings (IMO PSPC) for seawater ballast tanks are widely used as a benchmark for long-term corrosion protection in harsh marine exposure conditions.
Epoxy evolution At the waterline, the splash zone is the most corrosive area for floating offshore wind towers. Floating debris, ice, and contact from maintenance vessels or mooring operations can cause impact damage. Continuous motion caused by wind and waves generate
The splash zone is the most corrosive area for floating offshore wind towers
flexural stresses and pressures on fairlead tensions. Protective coatings must be flexible enough to withstand these movements without cracking or losing adhesion. High-build epoxy coatings have been used for decades in marine vessels and offshore oil and gas structures. Epoxy chemistry provides the adhesion and barrier properties needed to help protect wind tower structures from demanding environmental exposure. As opposed to unsaturated polyester coatings, amine-cured epoxy coatings form a highly crosslinked polymer network with inherently low water permeability, which allows glassflake loading to be optimised for
the specific coating chemistry and improves application efficiency. The next generation of epoxy coatings also includes formulations designed without solvents that release VOCs. These low-VOC epoxy technologies are already gaining approval for corporate specifications and major floating wind tower prototypes scheduled to launch later this year.
Expanding horizons Floating offshore wind will continue to open new areas for renewable energy development as the availability of new, shallower seabed sites decreases. In order to maximise service life, owners
and developers should explore materials and solutions that are designed for the specific demands of deepwater sites by drawing on, and continually improving upon, proven technologies from the marine and offshore energy sectors. The coatings specified during fabrication can contribute to reducing maintenance requirements, environmental impacts and lifecycle costs for these valuable floating structures. Chris Magel is the PPG Oil and Gas Segment Manager, Europe, Middle East and Africa, Protective Coatings. He has 15+ years of experience in protective coatings for the oil and gas industry. ■
ANALYSIS PCE JULY – SEPTEMBER 2026
21
22
SPOTLIGHT
SPOTLIGHT PCE JULY – SEPTEMBER 2026
THE POWER OF PRESERVATION
The restoration team look back on the past 50 years of John Canning & Co, restoring painting finishes in America’s historic landmark spaces, including how paints, coatings and the technology used have also changed during that time.
Part of the Sterling Memorial Library ceiling after restoration
SPOTLIGHT PCE JULY – SEPTEMBER 2026
23
24
F
or 50 years, John Canning & Co has helped preserve and restore some of America’s most significant historic interiors. From state capitols, courthouses, entertainment venues and theatres to churches, museums, universities and other historic landmarks, Canning’s work has helped preserve the architectural finishes and decorative details that define the character and identity of these historic spaces. Over the past five decades, the preservation industry has changed considerably. Improved conservation materials, advanced analytical tools and evolving technologies have broadened what is possible in the restoration of historic buildings. At the same time, many of the traditional materials and techniques used by generations of craftspeople remain essential to achieving historically appropriate and compatible results.
SPOTLIGHT PCE JULY – SEPTEMBER 2026
Canning prides itself on using traditional materials and techniques. Whilst technology has transformed how we investigate, document and preserve historic finishes, the fundamental principles of preservation remain the same: understand the original material, respect the history of the building and make informed decisions that support its long-term preservation.
A glimpse at the earlier years of decorative painting: (Below) Director of Studio Design Jacqueline Canning-Riccio; (Below right) Founder, John Canning and (Right) Craftsperson Michael Deluca
The evolution of paints and coatings The paints and finishes found in America’s historic buildings reflect the materials, technologies and artistic practices of their time. Colour was supplied by pigments, which were combined with binders that held the pigment particles together and secured them to the substrate. Water, drying oils, natural resins, waxes and other media were used, often with additional fillers, driers and modifiers to produce finishes with distinct appearances, working properties and longterm performance.
These developments expanded the range of available coatings and transformed painting practice, but they also introduced important considerations for preservation professionals. Modern coating systems may differ substantially from historic materials in composition, ageing behaviour and interaction with building fabric. A product that performs well on contemporary construction can be unsuitable or potentially damaging when applied to historic plaster, masonry, woodwork or surviving decorative finishes. For this reason, preservation work involves far more than matching a historic colour or sheen. Coating selection must account for properties such as permeability, flexibility, adhesion, sheen, reversibility and compatibility with the substrate and any existing finish layers. Depending on the project and what our investigations uncover, we adopt these preservation advances while also sticking to more tradition-based paints. By traditionbased paints we are referring to the historic formulations or colour palettes designed
for the building’s period, which can include using limewash, linseed oil paint, mineral pigments, sticking with architectural colour palettes and so on.
25
When evidence indicates that an original decorative scheme was created using a traditional material, recreating or repairing that finish may require the use of historically appropriate paints, pigments, binders and application techniques. In these cases, tradition-based materials can help achieve the appearance, texture, depth and surface quality of the original work. Using traditional materials is not simply about reproducing the past. It can also be important for compatibility. When appropriate, Canning’s artisans use traditional materials and time-tested techniques to preserve the visual and material character of historic spaces. These methods are supported by decades of hands-on experience and an understanding of how historic finishes were originally designed, prepared and applied.
Preserving traditional craftsmanship Canning has had the opportunity to work on numerous projects that demonstrate the importance of traditional materials and techniques. One notable example is the Old Senate Chamber in the Maryland State House, where Canning restored eighteenth-century plaster walls and ornamentation using original methods and materials of the period. True and faithful to the restoration process, we mixed traditional old-fashioned soft distemper and linseed oil paint to use. Distemper is the ideal paint for traditional lime plaster. It dries to a very desirable soft matte finish and, since it is high in permeability, allows the plaster to breathe and thoroughly cure. We applied the paint with six-inch (150mm)-wide brushes. The soft distemper formulation included pigment; a binder such as animal-skin or bone glue or casein; preservatives including
SPOTLIGHT PCE JULY – SEPTEMBER 2026
Traditional coatings commonly included limewash, distemper, casein paint, tempera and oil-based paints. These materials were often mixed or modified by craftspeople to meet the needs of a particular project. Their appearance could vary based on the pigments used, the preparation of the surface, the application method and the surrounding environment. During the late 19th and 20th centuries commerciallyproduced paints became more widely available, while new pigments, binders, resins and synthetic materials expanded the range of colours and finishes that could be achieved. As the twentieth century progressed, acrylic and latex paints became increasingly common. Modern coatings offered convenience, consistency, durability and faster application. They also made it easier to produce a wide range of colours and sheens on a large scale.
26
Examples of Canning painting the walls using 150mm-wide brushes at the Old Senate Chamber
carbolic acid and borax; alum as a hardener and glycerine, soap or sugar as a retarder. This project demonstrates how traditional materials can remain highly relevant within modern preservation practice. Rather than replacing historic techniques with contemporary products, Canning was able to recreate the original material characteristics and application methods to achieve a result appropriate to the building’s historic fabric.
Revealing hidden histories Another notable project was the Philadelphia Academy of Music, where Canning worked to expose and define the building’s original decorative design scheme. The investigation involved paint analysis of up to 16 layers in some areas, along with aggressive exposure methods used to reveal faint, ghosted patterns that remained beneath subsequent layers of paint. Left: One of the many paint exposures where some of the faint ghost patterns of the original decoration scheme are visible. The ghost patterns correspond to original designs that can be seen in the archival photograph used, which is presumed to be from the building’s completion in 1857
SPOTLIGHT PCE JULY – SEPTEMBER 2026
Below: Decoration work in progress based on the findings from Canning’s paint analysis and exposures
27
The ghost patterns corresponded with original designs visible in an archival photograph believed to date from the building’s completion in 1857. By comparing the physical evidence uncovered through paint exposure with historic documentation, Canning was able to better understand the original decorative scheme and use those findings to guide the restoration work. The Philadelphia Academy of Music demonstrates the importance of investigation before intervention. Historic decorative finishes can contain layers of information that are not immediately visible. Through careful exposure and analysis, seemingly lost designs can sometimes be recovered and used to inform accurate restoration.
Preserving the original design intent
When Canning was hired to preserve the historic finishes of Sterling Memorial Library, it was essential to understand Rogers’ original design intent, as this was a major component of the visual aesthetic of the decoration. Rogers’ architectural style incorporated ageing and wearing features, as well as materials intended to appear centuries old. Rogers’ own directions, documented on his drawings and other project documents, provided important information about how these aged effects were intended to be achieved. Preserving the finishes therefore required more than simply cleaning or
Left: Narthex of the Sterling Memorial Library, showing level of dirt at top; mid-area as a result of the cleaning methods listed in the specifications, and bottom area as a result of John Canning & Co cleaning system
repainting the surfaces. It required an understanding of the traditional materials and methods that James Gamble Rogers had specified as part of the building’s original design.
Uncovering original decoration Another project centred on historic decorative paint was Canning’s work at the Basilica of the Sacred Heart of Jesus in Hanover, Pennsylvania. Following the completion of the initial paint investigation, Canning revealed that the basilica contained remarkably well-preserved original paint designs beneath the existing decorative paint layers. This discovery led to the largest paint exposure our firm has encountered, revealing the original decorative paint and fine art designs throughout the interior.
SPOTLIGHT PCE JULY – SEPTEMBER 2026
Over the decades, Canning has also had the privilege of working on numerous projects for Yale University’s Sterling Memorial Library, which was built in 1930 and stands at the heart of the university. Designed by James Gamble Rogers in the Collegiate Gothic style as a ‘cathedral of learning’, the building presents a particularly interesting preservation challenge because its decorative character was intentionally designed to convey the appearance of age.
28
Examples of the historic paint exposures in progress at the Basilica of the Sacred Heart of Jesus
The scale and condition of the surviving original decoration made this an extraordinary discovery within the preservation industry. The project demonstrated the remarkable amount of information that can remain concealed beneath later layers of paint, and reinforced the importance of thorough investigation when approaching historic interiors.
SPOTLIGHT PCE JULY – SEPTEMBER 2026
Blending technology and traditional craft A strong example of Canning’s blending modern materials and technological advances with traditional craft is our restoration work done for Doris Duke’s Shangri-La in Honolulu, Hawaii. The Shangri-La was commissioned by heiress and philanthropist Doris Duke in the 1930s as a private residence and a showcase for her extensive collection of architectural elements and art from the Middle East. The original decoration was stencilled directly onto the wooden columns, mouldings, panels and architectural details of the residence. Previous efforts to seal the painted decoration with shellac were made, but over time this severely discoloured the
decoration, along with the environmental conditions, since this was a waterfront residence, extensively decaying the paint and the substrate. For the restoration, we recreated over 30 classic Islamic patterns of painted decoration, with up to seven separate stencil plates for each design. We formulated solutions that would stand up to the environment and conserve what remained of the original materials. The technological advances in relation to historic paint analysis played a vital role in examining the precise colours used originally. A huge part of understanding the original colour palette was removing the underlying shellac coating to properly reveal the original decoratively-painted surfaces. This was done on the Masonite panels and original wooden columns and mouldings. After the original decorations were exposed and any shellac residue was further reduced and evened out, the original decorative artwork was analysed for colour and pattern. The colours were examined using highpowered microscopes under different light conditions. This investigation determined
29
Some examples of the damage done to the decoration at Shangri-La
that a seven-colour palette including primary reds and blues, yellow, green and beiges was needed. With the analysis findings, we conducted a thorough investigation of original and potential replacement materials to accurately restore the design and colour palette while also adhering to the need for durability and longevity. To duplicate the 1930s Islamic art, tracings of the remaining original work were computer-digitised to create line drawings, which were used to produce machine-cut stencils. With our
approach, modern materials and technology were used to restore the beauty of these decorations, but also to allow the materials to endure the natural elements of their surroundings. While traditional materials remain essential in many projects, over the past 50 years advances in conservation science have provided new ways to evaluate historic materials, understand deterioration and develop more precise treatment approaches. We adopt technological advances when they provide meaningful
SPOTLIGHT PCE JULY – SEPTEMBER 2026
Restoration work in progress at Shangri-La
30
Doris Duke’s Shangri-La after restoration
benefits to the preservation process. This may include improved analytical methods, more accurate documentation, advanced imaging, modern conservation materials or specialised technologies that allow treatments to be performed with greater precision and control. Some examples of this include microscopy analysis, vector design software, laser cutters, precision-cut stencils etc. Canning has adopted many of these new advances for our historic preservation projects, whether it’s to properly reinstate the historic colour palette throughout an interior, or to produce exact replicas of a design scheme. SPOTLIGHT PCE JULY – SEPTEMBER 2026
Significant developments One of the most significant developments in preservation over the past several decades has been the advancement of microscopic analysis. Small paint samples can be examined as cross-sections, allowing researchers to study the sequence of layers from the original finish through later repainting campaigns. This process, known as paint stratigraphy, can reveal the evolution of a building’s decorative history and may also show evidence of environmental exposure, alterations and previous repairs.
Even though the paint stratigraphy process started in the 1950s, the advancement in technology can provide additional information about pigments, binders, coatings and other material characteristics. These tools help conservators distinguish between visually similar layers, identify changes that may not be apparent during an on-site investigation and better understand how historic finishes were constructed. However, technology alone does not determine the outcome of a preservation project. Data must be interpreted within the context of the building. The relationship between colours, architectural features, light, shadow, historical documentation and decorative conventions all contribute to a complete understanding of the original design. A laboratory result becomes meaningful when it is connected to the history and physical character of the space. This combination of
science, research and artistic expertise is central to Canning’s approach. Innovation is most valuable when it helps preserve more original material, reduces unnecessary intervention, improves the accuracy of an investigation or provides a more sustainable solution. Rather than viewing traditional and modern approaches as opposites, Canning evaluates how each can contribute to the goals of a project. In some projects, the goal is to uncover and preserve the original finishes. In others, the original decoration may be too deteriorated or incomplete to remain visible, requiring careful recreation based on physical evidence, archival research and historic design conventions. Each project presents different challenges. There is no single formula for restoring a historic finish.
Major advances For more than 50 years, Canning has evolved alongside major advances in preservation technology, materials and professional practice. Yet our work remains anchored in the principles that have guided historic preservation for generations: rigorous observation, exceptional craftsmanship, respect for original materials and an unwavering commitment to authenticity. Today, our craftspeople,
conservators, artisans and project teams unite time-honoured expertise with leading scientific and technological resources.
31
The future of preservation will be defined not by a choice between innovation and tradition, but by their integration. Emerging tools, from advanced imaging and material analysis to digital documentation and conservation science, will offer ever more precise ways to investigate historic materials, interpret original finishes and plan more targeted interventions. But technology alone cannot preserve a historic place. It can reveal the story embedded in a decorative surface, yet it cannot replace the trained eye, practiced hand and informed artistic judgment required to conserve or faithfully recreate it. Preservation’s future depends on sustaining both forms of knowledge: the scientific insight that deepens our understanding of historic materials and the craft traditions that give that understanding lasting form. ■
SPOTLIGHT PCE JULY – SEPTEMBER 2026
Below: Example of a microscopy paint sample. Right: Microscopy analysis in progress by David Riccio
32
LIFTING THE LID
Beyond glassflake content Simon Daly, Senior Consultant – Energy & infrastructure at Safinah, looks at when how is more important than how much, and the role played by modern coatings guidance in protecting offshore wind’s most vulnerable zone. As offshore wind farms continue to develop as an increasing part of our energy mix, and operating as they do in extremely demanding environments, the durability of corrosion protection systems has become a critical factor in asset reliability, maintenance costs and lifecycle performance. Nowhere is this challenge more apparent than in the splash zone, the area where steel foundation structures are subjected to the combined effects of seawater immersion, wave action, atmospheric exposure, UV light, abrasion and mechanical abrasion.
LIFTING THE LID PCE JULY – SEPTEMBER 2026
Historically, glassflake-reinforced coatings have played a prominent role in protecting these high-risk areas. Their long track record has established them as one of the industry’s preferred solutions for extending coating life and reducing maintenance interventions. However, recent discussions within industry standards and specifications have raised an important question: is coating performance determined simply by the amount of glassflake present, or by how that glassflake is engineered and formulated into effective coating systems?
Recent work examining offshore coating guidance suggests that the industry may need to focus less on glassflake quantity and more on coating optimisation supported by real-life and laboratory performance assessments.
33
The science behind the barrier The effectiveness of glassflake coatings has always been linked to their ability to impede the movement of moisture and corrosive species through the coating film. When moisture attempts to penetrate a conventional coating, it can migrate through microscopic pathways towards the steel substrate. By incorporating lamellar glassflake particles into the coating matrix, these pathways become substantially longer and more complex. Instead of moving directly through the coating, moisture molecules must navigate around thousands of overlapping plate-like particles, which themselves are impervious to the passage of moisture. This phenomenon is commonly known as the ‘tortuous path’ effect. The result, when correctly formulated, is a significant reduction in permeability and therefore ultimately a slower rate of corrosion initiation. Even relatively small additions of glassflake have been shown to deliver notable improvements in resistance to moisture vapour transmission, demonstrating why the technology has remained central to offshore corrosion protection for decades, and has been incorporated into numerous resin chemistries, such as epoxies, polyesters and vinyl esters. For offshore wind structures where maintenance access is difficult and costly, improving barrier performance can translate directly into longer maintenance intervals and lower lifetime costs.
Evolution of glassflake technology Traditional glassflakes were produced using a ‘bubble’ manufacturing process, creating comparatively thick particles with lower aspect ratios. While effective for their time, these particles offered inherent limitations in barrier efficiency. Modern production techniques use advanced spinning technologies capable of producing considerably thinner flakes with far higher aspect ratios. Some modern particles can be manufactured at sub-micron thicknesses while maintaining excellent uniformity and consistency.
Characteristic
Traditional glassflake
Modern glassflake
Manufacturing method
Bubble process
Spun process
Particle thickness
3-18 μm
<3 μm
Aspect ratio
Lower
Significantly higher
Barrier performance
Good
Excellent
Optimisation flexibility
Limited
High
This development is important because aspect ratio, the relationship between particle diameter and thickness, has a direct influence on barrier performance. Higher-aspect-ratio particles create much longer and more complex diffusion pathways, allowing equivalent or even superior protection to be achieved with lower overall glass content, and at the same coating dry film thickness.
LIFTING THE LID PCE JULY – SEPTEMBER 2026
Table 1
34
In simple terms, today’s glassflake particles work harder than their predecessors. The relative permeability of the binder type itself must also be considered, and is why a system-type approach, considering both binder and filler, is necessary to formulating individual coating products.
Why more glass is not always better However, coating optimisation is far more complex than applying a minimum glassflake percentage requirement. For many years, specifications have often associated high-performance splash zone coatings (as well as internal coatings of other equipment such as storage tanks and pressure vessels) with a glassflake content exceeding 20% by mass. Whilst the origins of this number, as well as how it is defined, often lack clarity, and despite its undoubted good intention of improving product performance, this requirement originates from a period when glassflake particle technology was very different from what is available today. Research and development over recent decades have demonstrated that coating performance depends on several interrelated factors:
• glassflake particle size • particle thickness, these two determining its • aspect ratio • resin chemistry • other fillers present, and critical pigment volume concentration (CPVC), • adhesion promoter levels • application characteristics. Increasing glassflake loading indefinitely does not necessarily improve performance. In many cases, excessive glass content can actually reduce coating effectiveness, negatively affect application properties or push formulations beyond their optimum pigment volume concentration. A coating containing less than 20% by weight but engineered around modern high-aspect-ratio particles, and fully optimised, may offer the same or better performance than coatings simply meeting this legacy compositional requirement.
LIFTING THE LID PCE JULY – SEPTEMBER 2026
Table 2 Factor
Influence on performance
Glassflake thickness and aspect ratio
Increases diffusion path length
Resin chemistry
Determines durability and adhesion
Glassflake content
Must be optimised, not maximised
Adhesion promoter levels
Enhances substrate and filler bonding
Application quality
Critical to ensuring performance as intended
Qualification testing
Verifies real-world performance
Performance must remain the ultimate measure This shift in understanding presents an important challenge for standards development. Modern performance standards and specifications may often identify required generic chemistries, mandate coating film thicknesses and impose compositional limits on some ingredients as well as defining minimum performance requirements.
35
However, what happens when these different needs conflict with each other? Examples include:
• Performance requirements being met with alternate chemistries and scheme thicknesses • Performance requirements being met despite compositional requirements not being observed • Compositional requirements which are incompatible or non-optimised when used with specific chemistry types.
• Corrosion creep • Cathodic disbondment resistance • Adhesion retention • Cyclic ageing performance • Water immersion resistance. The offshore sector has long relied on rigorous qualification testing because it reflects realworld performance more closely than compositional requirements alone and because of the challenges in using real-life performance via track record, not least of which is the impact that imposing field-based performance history has on recent innovation. Data presented from multiple qualified coating systems demonstrates strong performance across adhesion retention, corrosion resistance and long-term durability, reinforcing the argument that testing, combined wherever available with proven field experience, should remain the primary basis for coating selection. This in itself presents a contradiction in that longer, field-based performance evidence may no longer be fully aligned with modern laboratory testing for a variety of reasons, such as:
LIFTING THE LID PCE JULY – SEPTEMBER 2026
More importantly, many of the established qualification tests for offshore coatings do not directly require a specific glassflake loading. Instead, they focus on measurable outcomes such as:
36
• Product may no longer be available • Pre-qualification testing requirements may no longer be the same • Acceptance criteria may have been tightened. This is why the continued development of pre-qualification testing requires a considered approach, with several modern standards accepting testing results over and above earlier versions of the document. An example of this is the NORSOK M-501 system, which permits the acceptance of some test results as far back as 2004, provided that all other requirements of the current edition are met and the minimum coating scheme thicknesses mandated in the current edition are also observed. This pragmatic approach permits innovation whilst acknowledging the extensive performance history of established coating technologies, and at the same time avoiding the unnecessary requalification of systems that have already demonstrated long-term durability and compliance in offshore service environments.
What this means for offshore wind Generally, the offshore wind industry has access to an ever-increasing range of products including glassflake coatings, which are typically subjected to extensive and relevant prequalification testing as well as an increasing body of field performance evidence, which is likely to grow as decommissioning accelerates. Additionally, corrosion and coatings professionals have an increasing library of evidence (field or laboratory-based) on which to base their decisions. The industry is able to draw on its own coating experiences, history and guidance, as well as those in other industries preceding it. Major coating failures in the splash zone are rare and generally attributable to other factors. This is allowing the industry to focus more attention in other areas such as:
• Improving the design of structures to allow effective coating • Ensuring a focus on quality control throughout the fabrication and coating application processes • Understanding how protective coatings can be used synergistically with other means of corrosion protection
• Questioning whether what the industry does now is also suitable as we move into a period of
LIFTING THE LID PCE JULY – SEPTEMBER 2026
longer design life and new foundation structure challenges (floating wind). Safinah can assist with offshore wind coating specification-writing, pre-qualification testing programme design and review, as well as third-party coating inspection for offshore wind projects. ■
GEOMET® 321 LT PFAS Free
Low curing
Low solvent
High protection
High ductility
Achieve new depths of performance.
38
LIFTING THE LID
Coating qualification for emerging CCS infrastructure A joint investigation provides new qualification data for internal flow coatings in CO₂ transport pipelines. As Carbon Capture and Storage (CCS) projects continue to expand globally, the development of reliable CO₂ transport infrastructure is becoming a critical enabler for large-scale deployment. While extensive research has been conducted on the behaviour of pipeline steels in CO₂ environments, comparatively little information has been available regarding the performance of internal flow coatings under the operating conditions expected in future CO₂ transport networks. To address this gap, Teknos Group, Mülheim Pipecoatings (MPC) and Salzgitter Mannesmann Forschung (SZMF) have completed a joint technical investigation evaluating the behaviour of an internal flow coating under CCS-relevant CO₂ transport conditions. The study examined coating performance in gaseous, liquid and supercritical CO₂, including selected impurity mixtures representative of industrial capture streams.
Growing need for qualification data Carbon dioxide transport pipelines differ significantly from conventional hydrocarbon pipelines. Depending on pressure and temperature, CO₂ may exist in gaseous, liquid or dense-phase supercritical states. In addition, captured CO₂ streams can contain varying concentrations of impurities originating from different capture technologies and industrial processes. These factors introduce operating conditions that require careful consideration during material and coating selection.
LIFTING THE LID PCE JULY – SEPTEMBER 2026
Before and after exposure 1
Before and after exposure 2
Internal flow coatings are widely used in pipeline systems to reduce internal roughness, improve flow efficiency, minimise particulate formation and deposit accumulation and provide corrosion protection during storage, transport and commissioning. Despite their importance, systematic qualification data for flow coatings exposed to CCS-relevant CO₂ environments has remained limited.
39
“Much of the industry’s research has understandably focused on pipeline steels and corrosion mechanisms,” explains Harri Lipsonen, Product Development Director, Infra and Energy at Teknos. “However, internal flow coatings are an integral part of many pipeline systems. As CCS infrastructure develops, it becomes increasingly important to understand how these coatings behave under realistic CO₂ transport conditions and to generate reliable qualification data that supports engineering decisions.”
Test programme reflecting operational conditions The investigation was designed to evaluate both the chemical stability and mechanical integrity of the coating under conditions representative of future CO₂ pipeline operation. The programme included exposure to gaseous, liquid and supercritical CO₂, as well as selected impurity compositions representative of capture and transport streams. Additional testing addressed longterm exposure behaviour, rapid decompression events and low-temperature operating scenarios. Exposure conditions covered a range of CCS-relevant pressure and temperature envelopes, with testing periods extending to several months to investigate potential time-dependent effects.
Stable behaviour Results from the investigation showed stable coating performance throughout the tested operating envelope. Across all investigated CO₂ phases, no blistering, cracking or delamination was observed. Coating thickness remained within the range of unexposed reference samples, while adhesion properties showed no measurable changes after exposure. Testing in pure CO₂ environments demonstrated coating integrity maintained under gaseous, liquid and supercritical conditions. Similarly, exposure to selected impurity mixtures did not result in measurable changes in coating performance within the investigated range. “From a coating qualification perspective, one of the most important observations was the consistency of the results across the different CO₂ phases,” says Lipsonen. “We did not observe significant differences in coating behaviour between gaseous, liquid and supercritical CO₂ within the investigated test envelope. This provides valuable information for pipeline projects that may operate under varying transport conditions.”
LIFTING THE LID PCE JULY – SEPTEMBER 2026
Following exposure, specimens were evaluated using a combination of visual inspections, coating thickness measurements, adhesion testing, mechanical performance assessments and microstructural analyses. The methodology was designed to provide a comprehensive comparison against unexposed reference samples.
40
Long-term exposure and operational stress testing In addition to phase-specific testing, the investigation examined the effects of prolonged densephase CO₂ exposure over periods extending to several months. According to the project results, surface condition, adhesion performance and mechanical properties remained comparable to reference samples throughout the exposure period. No degradation trends associated with longterm CO₂ exposure were identified within the investigated timeframe. The programme also included operational stress scenarios relevant to pipeline commissioning and abnormal conditions. Specimens were subjected to rapid decompression from elevated pressure levels as well as low-temperature exposure representative of CCS operating environments. No coating damage, cracking, delamination or adhesion loss was observed after testing. “These operational scenarios are particularly relevant because pipeline systems do not operate under steady-state conditions at all times,” notes Lipsonen. “Understanding coating performance during pressure release events and low-temperature exposure helps build confidence in long-term operational reliability.” Cross-cut after exposure 1
Cross-industry collaboration The project combined expertise from coating development, industrial coating application and independent testing. According to the partners, this multidisciplinary approach was essential to ensuring that laboratory investigations remained aligned with practical pipeline operating requirements.
LIFTING THE LID PCE JULY – SEPTEMBER 2026
MPC contributed application expertise gained from large-diameter pipeline projects, whilst SZMF provided independent testing and analytical capabilities. Teknos contributed coating development expertise and experience in pipeline coating technologies. Cross-cut after exposure 2
41
“Qualification of materials for emerging CCS applications requires collaboration across the value chain,” says Lipsonen. “By bringing together coating specialists, application experts and independent researchers, it becomes possible to generate data that is both technically robust and relevant to real-world pipeline projects,” adds Martin Mehler, Global Key Account Manager, Infra and Energy at Teknos. The project partners emphasise that qualification requirements will remain project-specific, depending on factors such as impurity composition, pressure-temperature envelopes, operating scenarios and expected service life. Nevertheless, the investigation provides a valuable technical reference point and contributes to the growing body of knowledge surrounding CO₂ pipeline infrastructure. As governments and industry accelerate CCS deployment worldwide, evidence-based qualification approaches for materials and coatings are expected to become increasingly important. The results of this investigation provide application-relevant data supporting the development of reliable CO₂-ready pipeline systems and contribute to closing a long-standing knowledge gap regarding the performance of internal flow coatings in CCS applications. By proactively addressing emerging industry challenges through structured testing and crossindustry collaboration, Teknos is helping to build the technical foundation required for the next generation of CO₂ transport infrastructure.
About the project The investigation was conducted jointly by Teknos Group, MPC and SZMF. The results were presented at the Pipeline Coating Conference 2026 and are available in a technical white paper on internal flow coatings for CO₂ transport pipelines. ■
LIFTING THE LID PCE JULY – SEPTEMBER 2026
Future CCS pipeline development
42
LIFTING THE LID
Why passive fire protection shouldn’t be treated like ‘just paint’ Passive fire protection (PFP) may sit within the same broad coatings family as the rest of the sector, but it plays a very different role and does not always receive the scrutiny that the role demands. Recent years have seen a drift towards treating PFP as a commoditised purchase, sometimes characterised by a ‘just a paint’ attitude, rather than as a safety-critical coatings system. Given what is at stake, that drift is worth examining, says Toby Stein, Downstream Marketing Manager, AkzoNobel. Passive fire protection (PFP) is the last line of defence for people, assets and operations in some of the most demanding environments served by the coatings industry; from LNG facilities and fuel refineries to petrochemical plants, offshore platforms and other high-hazard industrial infrastructure. PFP and insulation schemes are rightly classed as Safety and EnvironmentalCritical Equipment (SECEs), and quality and robustness need to be engineered in from the start of a project. However, it can sometimes receive less emphasis during the later stages of a project as budgets come under increased scrutiny.
LIFTING THE LID PCE JULY – SEPTEMBER 2026
At face value, this makes little sense. To understand why PFP can sometimes be treated as a commoditised, late-stage line item, it is important to look at how the project supply chain is structured. PFP systems are often specified and procured through multiple stakeholders, each with different priorities and project objectives. While systems must meet the required safety and performance standards, procurement decisions can naturally focus on upfront cost and installation considerations, making it more challenging to recognise the wider long-term value that PFP can deliver throughout an asset’s operational life. This isn’t a new problem, but it has become more pronounced as the number of suppliers has grown. Choice is a good thing, but where ‘qualified applicator’ status could once be used to consistently uphold best practice, a wider supplier base means an applicator unhappy with a supplier’s quality and budget requirements can simply move to another. That dynamic accelerates commoditisation, and with it, a gradual erosion of standards. Cost competition becomes a problem when it drives a race to the bottom in a system whose entire purpose is safety. Ironically, the net result can easily be a solution that neither optimises PFP design nor saves money over the full lifecycle.
Technical decision This is also why choosing between PFP systems is a technical decision, not a generic, interchangeable one. Epoxy PFP and lightweight cementitious (LWC) systems are different technologies, with different mechanical, thermal and durability profiles, even though both sit under the PFP umbrella. Epoxy systems from International, such as Chartek, can be significantly tougher than LWC systems, which are more prone to damage over the life of
an asset and typically need more repair as a result, bringing additional cost and operational disruption with it. Recognising that distinction early can support more informed decisionmaking, helping to balance upfront costs with longer-term performance considerations.
43
Improved safety standards At the same time, safety standards are ratcheting up. Industrial facilities are held to increasingly demanding safety and environmental standards, and regulators expect owners and operators to demonstrate ongoing compliance. Because PFP is present across so many safetycritical areas of any industrial facility, damaged or failing protection can become one of the more visible indicators that something in that compliance picture isn’t right.
© Corrocoat
LIFTING THE LID PCE JULY – SEPTEMBER 2026
This reflects a broader trend across the industry, with designers and EPCs increasingly engaging suppliers on PFP optimisation and structural design. Such collaboration is always welcome, but the scope to influence project outcomes is often greater when that engagement takes place earlier in the design process. Early technical input can help identify opportunities to optimise both performance and cost. Ideally, those conversations begin during the PreFEED and FEED stages, before key engineering, procurement and construction decisions
LIFTING THE LID PCE JULY – SEPTEMBER 2026
44
become locked into the project. Suppliers have established expertise in structural fire design and performance-based design over recent years, and that capability is worth far more when it shapes a project from an early stage than when it is called upon to rescue one.
Project delivery change Part of what has driven this pattern is a broader shift in how the industry organises project delivery. Asset owners historically retained more in-house capability to scrutinise testing, design quality and PFP requirements directly. Many have since moved away from that model, shifting toward more rules-based decision-making and delegating greater responsibility
to EPCs, who in turn delegate fabrication and application further down the chain. Each additional link increases the distance between the owner who ultimately depends on the system performing, and the people specifying and installing it, and that distance is itself a contributor to commoditisation.
45
None of this is solved by writing a better specification alone. A genuinely good outcome is behaviour-based rather than rules-based, depending on culture and mindset as much as on the wording of a document. Specifications are often relatively light, and even a well-written one struggles to capture whether the people applying a system bring a safety-first mindset to the task. Inspection and test plans matter, but only if the right behaviours are present and are properly communicated through supervision. Successful PFP delivery is ultimately relationshipdriven, not transactional. Without collaboration and aligned expectations between owner, EPC, supplier and applicator, even the most carefully-drafted specification can become a box-ticking exercise rather than a guarantee of performance.
Beyond supplier relationships For the coatings industry, this points to a role that goes beyond any individual supplier relationship. Treat PFP with the same technical rigour applied to other high-performance coatings. Resist the slide towards commoditised, lowest-upfront-cost procurement rather than simply accepting it as inevitable. Each of these steps narrows the gap between what a specification says and what an asset actually needs when its safety-critical protection is called upon. There’s nothing wrong with competition or with owners having a wider choice of credible, qualified PFP suppliers. What matters is that PFP is specified, designed and installed with the same seriousness as the risk it exists to manage. ■
Advance your career
in the Shipping Industry with a globally recognised online diploma • Shipbuilding & Ship Repair • Superyacht Project Management, Refit & Newbuild
• Technical Ship Management • … and many more Flexible Supportive Expert-led Maritimetrainingacademy.com courses@maritimetrainingacademy.com +44 (0) 1252 739779
LIFTING THE LID PCE JULY – SEPTEMBER 2026
POPULAR COURSES INCLUDE:
IN FOCUS PCE JULY – SEPTEMBER 2026
46
47
IN FOCUS
Flyability and MaDfly recently performed the first UAV inspection of methanol fuel tanks on a container ship.
IN FOCUS PCE JULY – SEPTEMBER 2026
ANOTHER DRONE INSPECTION FIRST
48
M
aritime drone service provider MaDfly and Flyability, together with a leading container ship operator and classification societies ABS and Lloyd’s Register, have successfully completed the first dronebased inspection trial of an inert methanol fuel tank on board a container ship using the tethered Elios 3 UT. With the growing pressure on decarbonisation for the maritime industry, methanol has emerged as a primary alternative to traditional hydrocarbons. However, this evolution brings new operational complexities, requiring innovative approaches to the inspection and maintenance of methanol fuel tanks.
IN FOCUS PCE JULY – SEPTEMBER 2026
Remote inspection Traditional tank inspection methods require extensive tank cleaning, ventilation and risky personnel entry. However, with the development of advanced maritime UAVs, it has now become possible to inspect these tanks remotely, without requiring any human entry, and allowing faster recommissioning after the inspection. A particularly important step in the inspection of methanol tanks with drones is inerting, which involves introducing inert gas into a tank to reduce the oxygen content to less than 5-8% by volume, creating an inert condition. This minimises the risk of combustion during inspection and maintenance operations. The drone is then able to safely fly inside the tanks to conduct the necessary structural assessment.
Container ship trial The trial tank inspection was successfully completed with the Elios 3 UT and Tether Power Unit on April 24th 2026, in Gdansk, Poland, on board the 2,100 TEU Laura Maersk and in the presence of representatives from both ABS and LR. The operation marked a major milestone in maritime safety, proving that inert tanks can be thoroughly and safely inspected in under
two hours without requiring human entry into dangerous, enclosed spaces. “I am very happy with the results of this trial, which I believe has clearly shown that modern drone technology makes it possible to efficiently inspect low-flashpoint fuel tanks on our Net Zero methanol-fuelled vessels with high-quality results and increased safety compared to traditional inspection,” said Bjorn Ola Stråby, Senior Lead Naval Architect at Maersk.
Two-hour flight The operational execution was spearheaded by drone inspection specialists from MaDfly,
“The test conducted on board the Laura Maersk perfectly demonstrates this level of maturity. Leveraging MaDfly’s operational expertise and thorough preparation in close collaboration with Maersk teams, and supported throughout by Flyability, we successfully demonstrated that a methanol-
inert tank can be inspected in less than two hours, with a high level of accuracy and reliability, validated by ABS and Lloyd’s Register.
49
“This success also reflects a strong alignment between innovation and vision. We would like to highlight Ola’s forwardthinking approach and courage, having anticipated from the vessel design stage the integration of drone-based inspection methods. His trust in MaDfly and in these emerging technologies was instrumental in achieving this milestone. We thank Flyability for their continuous support, technical excellence, and positive mindset,
IN FOCUS PCE JULY – SEPTEMBER 2026
whose long-term partnership with Flyability has helped push the boundaries of what remote inspection technology can achieve in confined spaces. “Since the early days with the Elios 1, MaDfly has had the privilege to follow and actively contribute to Flyability’s remarkable technological evolution,” said Thierry Guillot, CEO at MaDfly.
50
as well as the classification societies for their constructive feedback. For MaDfly, this project marks a significant step forward in demonstrating the operational value of drone-based inspection solutions for the maritime industry.”
Class compliance The success of the trial also relied on a rigorous, collaborative framework. ABS and LR provided vital oversight to validate the drone’s methodology against strict maritime classification standards, ensuring that the data captured meets the regulatory requirements.
IN FOCUS PCE JULY – SEPTEMBER 2026
“This demonstration was an important step in showing that unmanned inspections could be a solution for methanol tank surveys, looking to improve safety by avoiding personnel entry into an enclosed space,” said Georgios Koutsoumpas, Senior Technology Engineer at ABS, who attended the demonstration on the Laura Maersk. “ABS was pleased to contribute to the development of the inspection procedure and the supporting risk assessment, all of which helped to ensure the demo was carried out on a sound technical and safety basis. The Elios 3 UT drone delivered clear image quality, reliable UTMs, and was able to access difficult-to-reach areas inside the tank.” Eduardo Antunes, Survey Regulations and Procedures Manager at Lloyd’s Register, who also attended the demonstration, commented: “This trial demonstrates that UAV-based inspection can significantly enhance safety by removing the need for confined space entry in certain cases, while delivering high-quality visual data to support survey decision-making. The livestreaming capability proved effective in enabling detailed inspection of structural features and coating condition. From a regulatory perspective, this trial provides a solid foundation for the continued development and acceptance of remote inspection techniques in classification surveys.”
The future of RITs By proving that remote technology (RITs) can safely deliver high-quality structural data inside methanol fuel tanks, Flyability, MaDfly and its partners have established a new benchmark for the future of sustainable fleet maintenance. ■
IN FOCUS PCE JULY – SEPTEMBER 2026
51
52
IN FOCUS
IN FOCUS PCE JULY – SEPTEMBER 2026
RETHINKING ONBOARD MAINTENANCE
Ewout Bosman, PPG Global Marine SeaStock Segment Director, Protective and Marine Coatings, explains why a straightforward coating maintenance routine can improve consistency and asset protection.
IN FOCUS PCE JULY – SEPTEMBER 2026
53
54
O
nboard maintenance has long been recognised as an essential part of protecting vessel integrity between dry dockings. Yet the environment in which maintenance is performed has changed significantly. Today’s crews operate under increasing time pressure, vessels are expected to remain in service longer between scheduled maintenance periods and the industry continues to face persistent workforce shortages. For instance, the latest BIMCO/ICS Seafarer Workforce Report estimates that the global shipping industry is currently short of more than 39,000 officers. To meet future demand, the industry will need an additional 22,747 officers and 8,475 ratings or non-officer crew members entering the workforce each year through 2030. These changing conditions are prompting operators to evaluate maintenance systems based on how consistently repairs can be executed on board, how efficiently products can be managed and how maintenance practices can be standardised across fleets. This shift is driving renewed interest in maintenance solutions that simplify routine repairs without compromising corrosion protection.
IN FOCUS PCE JULY – SEPTEMBER 2026
Maintenance begins between dry dockings Every voyage exposes a vessel to saltwater, ultraviolet radiation, changing temperatures and mechanical wear. Even minor coating damage can quickly develop into corrosion if left untreated, increasing repair requirements during the next scheduled dry docking and potentially affecting long-term asset integrity. Routine inspections and localised repairs remain among the most effective ways to preserve protective coating systems and extend service life. Industry data shows proactive maintenance programmes can reduce emergency repair costs by 20-30%.
Across an entire fleet, improvements in routine maintenance can translate into significant savings while extending component life and improving operational reliability. Despite its importance, onboard maintenance rarely happens under ideal conditions and is seldom the primary purpose of a crew’s time on board. Instead, crew members perform repairs between
Why simplicity matters
55
Two-component coating systems are the traditional solution for many applications where maximum durability, chemical resistance and long-term protection are required. However, preparing a twocomponent coating requires crews to measure separate components accurately, follow specific mixing ratios and work within a limited pot life before the coating
IN FOCUS PCE JULY – SEPTEMBER 2026
operations, inspections, equipment maintenance and countless other responsibilities. They are professional seafarers. Every minute spent preparing coatings, searching for products or correcting application mistakes is time they cannot spend on other operational priorities. Maintenance products should fit into that reality rather than add unnecessary complexity.
IN FOCUS PCE JULY – SEPTEMBER 2026
56
begins to cure. In practice, those tasks often take place inside confined paint lockers while crews balance other operational priorities. Mixing frequently happens by estimation rather than precision. Preparing too much coating creates unnecessary waste. Preparing too little interrupts the repair. Every additional step creates another opportunity for inconsistency.
application helps reduce variability between crews operating in different regions and under different conditions. Standardised maintenance practices also simplify training, product forecasting and inventory management, while giving operators greater confidence that repairs are being completed consistently throughout the fleet.
Ready-to-use one-component coatings simplify that process. Crews prepare the surface, stir the coating and begin application immediately without measuring separate components or managing pot life. Fewer preparation steps reduce opportunities for mixing errors, while helping standardise maintenance practices across vessels.
Open the door to almost any vessel’s paint locker and you’ll find a variety of primers and topcoats, many of which require separate hardeners and thinners before they can be applied. Managing, storing and mixing these additional components adds complexity to onboard maintenance and consumes valuable storage space.
That maintenance consistency across dozens or even hundreds of vessels can directly influence long-term asset performance and maintenance costs. Simplifying coating preparation and
Simplifying inventory management
Simplifying maintenance coatings can reduce the number of products crews need to manage, improve inventory control and minimise partially-used materials that ultimately require disposal. The result is a more efficient maintenance process that
Supporting sustainability Environmental performance is becoming another consideration in routine maintenance decisions. Operators increasingly evaluate coatings for corrosion protection and for waste generation, volatile organic compound (VOC) emissions and inventory efficiency. Ready-to-use onecomponent coatings can help reduce leftover mixed material that ultimately requires disposal, while low-VOC formulations support evolving environmental expectations.
Innovation for better maintenance Advances in onboard maintenance extend beyond coating formulation. Digital inventory management tools are enabling operators to monitor coating consumption across fleets, optimise seastock inventories and identify recurring maintenance trends before they develop into larger asset integrity issues. Improved visibility allows operators to maintain appropriate stock levels while reducing unnecessary purchases and excess inventory. Training remains equally important. Standardised seastock programmes that combine classroom instruction with practical application help reinforce best practices in corrosion prevention, surface preparation and coating application, improving consistency regardless of crew experience. For example, PPG supports shipowners through global seastock training programmes. Having delivered more than 200 crew training sessions worldwide to date, these programmes combine classroom instruction with hands-on practice using the same products and equipment crews use on board. PPG’s One Range portfolio reflects this approach by offering ready-to-use onecomponent coatings, including water-based, low-VOC and fast-drying formulations designed for onboard maintenance.
The portfolio eliminates mixing errors, streamlines application and simplifies paint locker inventory by reducing the number of separate components crews must manage. The portfolio complements, rather than replaces, traditional two-component coating systems by providing an alternative for maintenance applications where ease of use, inventory simplification and reduced waste are key considerations.
57
Together, simplified coating systems, structured training and digital maintenance tools enable a more standardised approach to onboard maintenance that supports both operational efficiency and long-term asset protection.
Looking ahead The future of onboard maintenance will not replace established coating technologies. High-performance two-component systems will continue to play a critical role in protecting vessels operating in demanding environments. However, maintenance strategies are evolving. As operators seek greater consistency across global fleets, coating selection will increasingly be evaluated not only on corrosion protection but also on ease of application, maintenance standardisation, inventory efficiency and lifecycle performance. For routine onboard maintenance, simplifying the maintenance process can improve execution, reduce variability and help operators protect assets more effectively between dry dockings. Ewout Bosman is PPG Global Segment Director for Marine Seastock, Protective and Marine Coatings, where he leads international initiatives focused on sustainable maintenance strategies for the maritime industry. With almost two decades of experience in the coatings industry, Bosman brings deep expertise in segment strategy, product and portfolio management and innovation across global markets. ■
IN FOCUS PCE JULY – SEPTEMBER 2026
allows crews to spend less time organising products and more time completing repairs.
58
UPDATE
UPDATE PCE JULY – SEPTEMBER 2026
UNDER PRESSURE: HOW TOLL PROCESSORS CAN HELP BUILD RESILIENCE
Ongoing challenges and disruptions are placing increasing strain on chemical and industrial coatings manufacturers. Ben Beattie, Director of UK-based toll processor Forbeats, explains how toll processors can help them navigate volatility.
UPDATE PCE JULY – SEPTEMBER 2026
59
60
I
n recent years, the chemical sector has been affected by Brexit complications, the lingering effects of the pandemic, the war in Ukraine, disruption to Red Sea shipping routes and instability in the Middle East, all of which have created logistical, regulatory and cost challenges. The movement of hazardous materials – a core component of the chemical and industrial coatings industries – is also becoming increasingly complex. Stricter handling requirements, combined with longer and less direct shipping routes, are slowing the flow of goods and increasing the risk of delay at multiple points in the supply chain. In the UK, the situation is being exacerbated by reduced road haulage capacity and higher transport costs. Driver shortages and operational constraints mean that even when materials reach the country, moving them efficiently to production sites is not guaranteed.
UPDATE PCE JULY – SEPTEMBER 2026
One of the most immediate challenges is the reliability of material supply. Delays in the delivery of key inputs are making it increasingly difficult to maintain consistent production schedules. As supply chain pressures persist, market behaviour is also evolving. Price volatility is becoming more pronounced, with traditional pricing mechanisms proving harder to sustain, while tightening supply is reducing buyer leverage and increasing competition for available materials. Alongside this, manufacturers are also facing increased regulatory divergence, including post-Brexit regulation UK REACH, border checks and country-of-origin documentation, which is increasing complexity and cost for importers and exporters.
Need for resilience While these disruptions have become a constant theme across all industries, chemical
firms are experiencing unique vulnerabilities. A report by Argon & Co, which drew insights from 800 senior business leaders, has found that only one in five are building formal scenario planning capabilities. According to the report, rising raw material costs are the biggest supply chain challenge for 40% of the responders, while 33% experience demand volatility and forecasting difficulties. It notes a pattern of short-term fixes replacing long-term capability-building – while companies recognise the need to invest in resilience, margin constraints mean they are being highly selective in how they act – and stresses that resilience needs to be treated as a core capability, not a periodic project. To help build resilience, chemical and coatings manufacturers should consider partnering with experienced toll processors as they serve as critical enablers of flexibility, efficiency and compliance in an environment where disruptions such as capacity constraints, regulatory demands and raw material shortages threaten business operations.
From overflow to strategic backbone Toll processors are moving beyond their traditional role as mere overflow facilities, emerging as strategic partners that enable manufacturers to weather uncertainty, maintain compliance and deliver essential chemicals and lifesaving medicines without interruption. Partnering with a toll processor allows manufacturers to swiftly adapt to changing market demands, whether due to geopolitical events, regulatory updates or shifts in consumer preferences. This ensures that production schedules can be adjusted promptly, minimising downtime and meeting market needs effectively. Two of the greatest benefits offered by toll processors are on-demand capacity and agility. They can provide manufacturers and
developers with instant access to additional, GMP-compliant capacity without the need for major capital investment. This flexibility enables chemical and coatings companies to ramp up production to meet surges in demand, manage unplanned shutdowns or maintenance at internal facilities, and fulfil new contracts or respond to supply interruptions promptly. By offering scalable and agile support, toll processors help avoid costly downtime while preserving customer trust.
surplus stock, alternative raw material sources and pre-qualified service providers. This enables toll processors to source hard-to-find ingredients during shortages, implement contingency plans to keep production moving and navigate customs and documentation challenges efficiently. By leveraging these networks, manufacturers can gain access to resources and expertise that would be difficult to replicate in-house.
Reputable toll processors also invest in state-of-the-art technology and maintain environments that meet the strictest production standards, meaning they can offer services such as micronisation, sieving and screening, custom blending and packing and repacking, including sterile or controlled-environment handling.
Furthermore, a well-established partner network gives access to a spectrum of other services, ensuring that toll processors can offer genuine and bespoke endto-end solutions. Besides full contract manufacturing, additional services can include custom packing and repacking, labelling, warehousing, logistics, administrative paperwork and import and export services. With all these available from a single provider, this ensures an outsourcing solution that is complete, efficient and cost-effective.
Ingredient access An often-overlooked advantage of toll processors is their extensive network of trusted suppliers and logistics partners. Many maintain up-to-date databases of
UPDATE PCE JULY – SEPTEMBER 2026
61
UPDATE PCE JULY – SEPTEMBER 2026
62
Compliance & traceability With increasing regulatory scrutiny, toll processors can support chemical and coatings manufacturers in maintaining compliance by implementing stringent quality assurance protocols and keeping detailed records, facilitating traceability and adherence to regulations. Experienced toll processors operate under robust quality management systems, ensuring full compliance with Current Good
Manufacturing Practice, ISO 9001 and other sector-specific standards. Moreover, they have the specialist plant and equipment necessary to handle sensitive or hazardous materials safely. Processors with a history of operating across international regulatory frameworks are also particularly valuable for companies working across global markets. Besides giving assurances of safety, having the necessary policies, procedures, equipment and expertise in place enables toll processors to overcome operational
simply be a matter of availability. In tightlyregulated industries like chemicals and coatings, the wrong choice can result in delays, recalls or regulatory non-compliance. As such, potential partners should be carefully considered based on key criteria:
63
• Regulatory compliance and certifications: Toll processors must operate under strict regulatory protocols, as regulatory missteps can result in fines, recalls or blocked market access. • Technical expertise and capabilities: Toll partners should offer specialised processing capabilities and demonstrate experience with both standard and highpotency materials. • Quality control and analytical support: Robust in-house quality control and adherence to data integrity standards should be non-negotiable. • Confidentiality and IP protection: Intellectual Property (IP) is the lifeblood of many pharmaceutical businesses. Nondisclosure agreements and IP protection protocols should be in place, as a breach of confidentiality or IP leakage can have catastrophic commercial consequences.
bottlenecks. Being fully equipped and prepared, production can be scaled up at speed, delivering economy-of-scale savings without compromising quality. For chemical and coatings manufacturers, this offers peace of mind – knowing that products are manufactured and handled according to the highest standards, reducing the risk of compliance failures or recalls.
Choosing a toll processing partner Selecting a toll processor should not
As market volatility continues to rise and operational demands grow more complex, and as companies move to strengthen local supply networks and reduce dependency on single regions, toll processors should be seen as a pragmatic and strategic asset rather than a back-up overflow option. From mitigating risk to enabling innovation, the right toll processor partner can offer chemical and coatings manufacturers the expertise, reliability and resilience to navigate challenges and disruptions. ■
UPDATE PCE JULY – SEPTEMBER 2026
• Supply chain integration and responsiveness: Location, supplier network, and operational agility all influence a toll processor’s ability to deliver on time.
64
N O I T I L O M E D O HYDRLIVE PORT IN A
REVIEW PCE JULY – SEPTEMBER 2026
REVIEW
Yalin Deniz Tektas, an estimator at British Columbia-based Walco, explains how the company completed a threeday terminal project without disrupting operations.
REVIEW PCE JULY – SEPTEMBER 2026
65
66
W
hen a shipping terminal needs concrete removed, the work doesn’t stop the port. Vessels still dock, trucks still move and every hour of downtime has a cost. That’s exactly the environment our crew stepped into – and it’s exactly the kind of complex, highconsequence project Walco Industries is built for. Hydrodemolition in a live port is not just about removing concrete; it’s about adapting to the environment, controlling water, maintaining production and delivering a clean repair surface within a very limited work window.
REVIEW PCE JULY – SEPTEMBER 2026
Walco Industries recently completed a hydrodemolition project at an active shipping terminal, and it started with an important reminder: in an active port, plans can change quickly. Before our crew arrived on site, the project start date changed three times due to shifting terminal operations, vessel schedules, access limitations and coordination with other ongoing activities. This made the project very different from a typical isolated construction site. The work had to be planned around a live terminal environment where access was limited, space was tight and production time was extremely valuable. Once the work window became available, speed became a top priority. The hydrodemolition scope was completed through 24-hour operations over three days. Maintaining that level of production in an
active port required strong coordination, reliable equipment and a clear plan before work began. The scope involved controlled concrete removal using robotic hydrodemolition – a method that uses high-pressure water to selectively remove concrete while preserving the existing reinforcing steel and minimising damage to the surrounding structure. Speed, accuracy and a reliable
containment plan were the main priorities throughout.
Working inside a live terminal One of the defining features of this project was the need to work around continuous terminal activity. Equipment movement, truck access, hose routing, water supply, wastewater handling and daily production planning all required careful coordination before and during the work.
Because space was limited, every piece of equipment had to be positioned with purpose. The hydrodemolition robots, highpressure pumps, vacuum trucks, water lines and support vehicles all had to operate together without disrupting the surrounding terminal. There was very little room for wasted time. A small delay in access, water supply or equipment movement could
REVIEW PCE JULY – SEPTEMBER 2026
67
68
affect the entire workflow. For that reason, coordination was just as important as the concrete removal itself.
active port environment where uncontrolled discharge was not acceptable.
Closed-loop water management
A key benefit of hydrodemolition is its ability to remove specified concrete while leaving reinforcing steel intact. This allowed the team to expose the repair areas cleanly and prepare the surface for the next stage of work.
REVIEW PCE JULY – SEPTEMBER 2026
Hydrodemolition is an effective concrete removal method, but it also creates a significant responsibility: managing the water used during the operation. On this project, the containment areas were provided and maintained by the client. Once runoff water was captured within those areas, our team pumped it back into our system for treatment and reuse. This allowed us to operate with a closed-loop water recycling setup – the captured water, which contained concrete slurry, fine particles and debris, was directed through our treatment system before being returned to the hydrodemolition operation. By filtering and reusing the collected water, we reduced the amount of make-up water required and limited the volume of wastewater that needed to be managed off site. This was especially important in an
Accurate removal
The robotic system helped the crew achieve both speed and accuracy. Whilst the limited work window demanded fast production, the removal still had to meet the required depth, limits, and quality expectations. That balance was one of the central challenges of the project: production mattered, but not at the expense of safety, water management or the final repair surface. The robotic system also reduced the amount of direct manual demolition required, allowing the crew to support the operation while the robot performed the highpressure concrete removal.
Planning made the difference This project required more than performing
hydrodemolition work. It required detailed planning, clear communication and the flexibility to adapt to changing site conditions.
69
Because the work ran continuously over three days, the plan had to support uninterrupted production. Equipment, water supply, wastewater handling, crew coordination and communication with the client all needed to stay aligned throughout. Access limitations, active terminal operations, environmental requirements, equipment staging and the closed-loop treatment system all influenced the daily workflow. Strong coordination between the client and our team was one of the most important factors in completing the work successfully.
Project outcome
The client was impressed with both the quality of the work and the speed of the operation. The project confirmed that when equipment setup, water management and field coordination are properly aligned, hydrodemolition can deliver strong production results without sacrificing accuracy or control. Credit goes to the Walco crew who kept production running safely and efficiently across three straight days of 24-hour operations. Overall, the project provided valuable experience in performing hydrodemolition inside an active terminal and reinforced the fact that that success depends on more than high-pressure water – it depends on preparation, communication, speed, accuracy and the ability to adapt quickly when site conditions change. ■
REVIEW PCE JULY – SEPTEMBER 2026
The terminal project demonstrated how robotic hydrodemolition can be successfully executed in a restricted, sensitive and active port environment. Through careful planning, controlled removal, continuous coordination and closed-loop water treatment, the hydrodemolition scope was completed within three days – on schedule and without safety incidents.
70
REVIEW PCE JULY – SEPTEMBER 2026
REVIEW
TRUST, COLLABORATION & QUALITY Trust isn’t given in the coatings industry – it’s earned, and Ponsse puts its trust in Teknos coatings for its forest machines that operate everywhere from the Arctic to the tropics.
REVIEW PCE JULY – SEPTEMBER 2026
71
72
S
urface treatment specialist Hannu Tarvainen knows what the coatings market has to offer. His conclusion is simple. “Partnering with Teknos is all about trust. If I had to summarise our collaboration in one word, that would be it – Trust.” Ponsse Plc is one of the world’s largest manufacturers of forestry machines. Founded in 1970 in Vieremä, Finland, the family-owned company is still based in the same location despite having grown into an industry leader with worldwide exports. Ponsse manufactures a wide range of harvester and forwarder machines that are designed around the modern, environmentally-friendly cut-to-length logging method. Ponsse’s machines operate in extremely demanding conditions ranging from arctic to subtropical and tropical locations, as well as environments of heavy atmospheric corrosivity. The extreme mechanical and environmental stresses to which the equipment is subjected also place significant demands on the surface treatment of components and subassemblies. With few exceptions, Ponsse has used Teknos products since the 1970s.
REVIEW PCE JULY – SEPTEMBER 2026
Direct to metal – direct savings “Teknos’s direct-to-metal products are by far the best in the industry,” says Tarvainen. “We’ve tested everything that’s available in the market and the quality of Teknos coatings really is exceptional. They’re easy to apply, finish looks great, and the mechanical durability and corrosion resistance are superb. And they retain the gloss really well too.”
Due to the heavy demands of the operating environment, all parts on Ponsse’s machines are coated to corrosivity category C4. The front and rear subframes use Teknodur Combi 340 with a dry film thickness of 150μm, while sheet metal parts are finished with two-stage powder coating. All shades on Ponsse machines follow colour standards developed in collaboration with Teknos.
One major advantage of direct-to-metal coatings is that they do not need a separate primer. “If we had to prime everything, it would really slow down our production,” says Tarvainen. “Also, with Teknos’s coatings, we get better-looking and more attractive products with a thinner film, which means direct cost savings for our production.”
“Switching to Teknodur Combi 340 a few years ago allowed us to cut our VOC emissions dramatically,” Tarvainen recounts. “Now we can ramp up our production without being limited by VOC emissions. We have also done a lot of collaboration with Teknos on developing our powder coating process, and the results have been great.”
73
Surface finishing is a critical process for Ponsse, and one that requires the highest level of quality in production. “Teknos is our long-term partner, supporting us in our daily operations,” says Tuomas Pasma, Senior Manager, Quality & Sustainability, Ponsse. “Teknos’s team is always there to help if there are any issues with coatings. I’m actually very rarely in contact with them, since as a quality manager I only hear about the biggest problems, and with Teknos, everything has run great.” Ponsse has approximately 20 painting subcontractors working on different parts of the machines that are ultimately assembled and finished at the company’s factory in
Vieremä. Teknos works closely with Ponsse’s network of subcontractors, ensuring a high standard of quality and providing technical support when necessary. “Subcontractors are very important for both Ponsse and Teknos,” says Jan Åkerlund, Key Account Manager, Teknos. “We can’t have any irregularities or delays that impact production. The whole supply chain has to operate smoothly.” Teknos regularly updates Ponsse’s subcontractors with the latest technical information and guidance together with Ponsse. Training for subcontractors is held both on location and at Teknos’s training centre, covering various quality-related
REVIEW PCE JULY – SEPTEMBER 2026
Supporting the entire chain
74
topics such as corrosion resistance and best practices for coating application. “We want to be more than just salespeople for the customer,” explains Åkerlund. “Our aim is to be a technical partner that can help in every aspect of operations. The collaboration with Ponsse has been great, and it’s a pleasure to work with a team of such knowledgeable professionals.“
Extensive research In addition to supporting everyday surface coating tasks, Teknos’s team also conducts extensive research together with Ponsse to develop the processes and products used in Ponsse’s production. The long-term collaboration and deep technical knowhow continue to pay dividends as the two companies look ahead to continuing their partnership. “If you sell coatings, you also have to know how to paint and actually use the equipment,” adds Tarvainen. “Forget about coming around here to just sell some paint and tell us that someone else will do the
REVIEW PCE JULY – SEPTEMBER 2026
Hannu Tarvainen & Jan Åkerlund measuring the film thickness
user training in two weeks. The best part about working with Teknos is that not only are they experts on using their own products, but also the customer is never left alone. They always keep their promises, and we do everything together to make the process work.” ■
REVIEW PCE JULY – SEPTEMBER 2026
75
76
In partnership with PCE Magazine News from the Corrodere Academy Corrodere Academy provides globally recognised accredited training and qualifications to the protective coatings and corrosion control industry. Their aim is to raise standards throughout the industry worldwide and help students learn, discover and succeed.
Corrodere Academy & PFPNet Highlight the Importance of Specialist Passive Fire Protection Inspector Training technical knowledge of PFPNet, a not-forprofit industry group focused on improving knowledge, understanding and competency in passive fire protection.
CORRODERE ACADEMY PCE JULY – SEPTEMBER 2026
As the oil, gas and energy industries continue to place greater emphasis on the performance and integrity of safety-critical systems, Corrodere Academy and PFPNet are highlighting the importance of specialist training for inspectors working with Passive Fire Protection (PFP). Passive Fire Protection is a specialist discipline requiring technical knowledge that extends beyond conventional coatings inspection. To help address this need, Corrodere Academy previously partnered with PFPNet to develop the Level 2 Passive Fire Protection Coatings Inspection course. Designed for coating inspectors working in hydrocarbon environments, the course covers both epoxy intumescent and cementitious passive fire protection coatings, providing inspectors with knowledge of two of the most widely used PFP systems across the energy sector. The collaboration combines Corrodere Academy’s experience in coatings inspection training with the specialist
RAISING STANDARDS IN PASSIVE FIRE PROTECTION PFPNet was established nearly a decade ago to create a dedicated technical community for organisations and professionals involved in specifying, engineering, applying and inspecting passive fire protection within the energy industries. “PFPNet is a not-for-profit, subscriptionfunded industry group established to improve knowledge, understanding and competency regarding passive fire protection used in the oil, gas and energy industries,” explains John Dunk of PFPNet. “It is operated by its members for its members, who identify the key technical and other issues that PFPNet addresses and provides guidance on.” Today, PFPNet’s global membership includes major oil and gas companies, engineering firms, EPC contractors, regulatory authorities, PFP material manufacturers, application contractors and other organisations involved in passive fire protection.
77
“While other groups may occasionally address PFP, there was no dedicated community focused on the critical issues faced by this sector. PFPNet was founded to fill that gap and has successfully fulfilled this role.” WHY SPECIALIST PFP TRAINING MATTERS Training has become an important part of PFPNet’s work. In 2024, the organisation established PFPNet E-Tech as a separate entity dedicated to developing and delivering training. Its activities include the online Introduction to PFP in the Energy Industries course,
alongside specialist inspector training intended to improve understanding of the safety-critical role of passive fire protection. “PFPNet developed inspector training courses to help inspectors fully grasp the critical nature of fire protection and the key aspects essential for successful installation,” says Dunk. “These courses emphasise the differences between anticorrosion coatings, which prevent corrosion, and the safety-critical nature of fire protection coatings.” For coating inspectors moving into PFP inspection, this distinction is particularly important. While many inspection principles may be familiar, PFP systems perform a fundamentally different function, with correct installation playing a critical role in protecting structures and equipment in the event of a fire.
CORRODERE ACADEMY PCE JULY – SEPTEMBER 2026
According to Dunk, the organisation was originally created in response to the absence of a dedicated industry group addressing PFP challenges within the energy sector.
CORRODERE ACADEMY PCE JULY – SEPTEMBER 2026
78
UNDERSTANDING BOTH EPOXY & CEMENTITIOUS PFP
COMBINING PFP & INSPECTION EXPERTISE
The Level 2 Passive Fire Protection Coatings Inspection course covers both epoxy intumescent and cementitious PFP systems within a single programme.
The ongoing collaboration draws on the respective strengths of both organisations, with PFPNet contributing specialist PFP knowledge and Corrodere Academy bringing its experience in developing and delivering coatings inspection training internationally.
When developing the course, PFPNet and Corrodere Academy identified the value of giving inspectors an understanding of both systems while highlighting the common principles underpinning their inspection. “PFPNet and Corrodere recognised that combining epoxy and cementitious coatings into one course benefits the industry by highlighting their common foundations,” Dunk explains. “This approach enables course candidates to train on and work with both types of products throughout their careers.” Knowledge of both systems can support inspectors working across a wide range of energy and process-industry assets, including offshore platforms, refineries, LNG facilities and petrochemical plants.
“PFPNet has partnered with Corrodere Academy to deliver Level 2 training for PFP inspectors,” says Dunk. “This partnership combines PFPNet’s technical knowledge with Corrodere’s experience and expertise in developing and delivering training globally.” The Level 2 Passive Fire Protection Coatings Inspection course is available as a standalone qualification and can also be taken alongside Insulation Inspection or Thin Film Intumescent Coating Inspection as part of specialist training packages. Corrodere Academy and PFPNet advance passive fire protection knowledge and consistent inspections in oil, gas and energy.
Corrodere Academy News
79
CORRODERE EXPANDS INTERNATIONAL TRAINING NETWORK ACROSS USA & INDIA Corrodere Academy is continuing to grow its international training network, welcoming three new partners across the United States and India and making recognised coatings and corrosion training accessible to more professionals worldwide. The latest partnerships expand the availability of Train the painter, inspection and specialist training programmes in two important international markets.
STRAIGHT OUTTA SURFACE TRAINING BRINGS TRAIN THE PAINTER TO THE USA Straight Outta Surface Training (S.O.S.T.) has become Corrodere Academy’s official training partner and representative in the United States, providing contractors, asset owners and coatings professionals with greater access to structured applicator training.
Founded by Amy and Kris Kemper, S.O.S.T. was established in response to a challenge they had seen first-hand across the US coatings industry – experienced applicators developing their skills on the job without always having access to a recognised training and career development pathway. Kris first encountered Train the painter more than 10 years ago and has since used the programme internationally. “I’ve seen first-hand how effective the programme is across different markets. People across the industry kept coming to us asking for a real solution to that same training gap – so we went and found it.” Through S.O.S.T., Train the painter will provide US applicators with a structured development pathway, while giving contractors and asset owners a recognised benchmark for workforce competency.
CORRODERE ACADEMY PCE JULY – SEPTEMBER 2026
TM
80
Corrodere Academy News CORROSION TECHNICIAN ASSOCIATION JOINS US NETWORK
CORRODERE ACADEMY RECOGNISED IN SAUDI ARAMCO SPECIFICATION
Corrodere’s presence in the United States is being strengthened further through a new partnership with the Corrosion Technician Association (CTA).
Corrodere Academy has been officially listed as an approved training provider in the February 2026 revision of Saudi Aramco Engineering Procedure SAEP-316.
CTA will sell a wide range of Corrodere programmes, including Train the painter, ICorr Coating Inspector courses and specialist training.
The specification sets out requirements for the training, competency and certification of coating personnel working on Saudi Aramco projects, including applicators, supervisors and inspectors.
The partnership will provide additional routes for US coatings and corrosion professionals to access recognised training, from practical applicator development through to inspection and specialist technical programmes.
CORRODERE ACADEMY PCE JULY – SEPTEMBER 2026
Together, S.O.S.T. and CTA significantly increase Corrodere Academy’s ability to support individuals, contractors and organisations looking to develop workforce competency across the United States.
Corrodere’s recognised training pathways include ICorr coating inspection, Train the painter and Crew Supervisor training, providing contractors and coating professionals with established routes to develop and demonstrate workforce competency. The inclusion further strengthens the international recognition of Corrodere Academy training and supports organisations working to meet Saudi Aramco requirements.
CORROTECH INSTITUTE EXPANDS ACCESS ACROSS INDIA In India, Corrotech Institute has joined Corrodere Academy’s international training network and will sell and deliver the full suite of Train the painter programmes, ICorr inspection courses and specialist training. The partnership represents an important expansion for Corrodere in India, providing local access to internationally recognised training pathways across applicator, inspection and specialist disciplines. With a growing network of international training partners, Corrodere Academy is continuing its mission to make high-quality, structured coatings and corrosion training more accessible – wherever in the world professionals are developing their skills.
81
Corrodere Academy News STUDENT SUCCESS: SINAN ICIK ACHIEVES DISTINCTION Congratulations to Sinan Icik, who has successfully completed the Diploma in Coatings for Corrosion Control - achieving a Distinction. Sinan, currently working as a QA/QC Manager on bridge projects in Ukraine, undertook the Diploma to deepen his knowledge of paint chemistry, materials testing and corrosion fundamentals as he works towards his long-term goal of developing his career in corrosion engineering.
PFPNET CELEBRATES 10 YEARS OF PASSIVE FIRE PROTECTION EXPERTISE
TRAIN THE PAINTER LOGBOOK APP SUPPORTS TRAINING ON THE GO
Congratulations to PFPNet as it celebrates 10 years of collaboration, technical expertise and knowledge sharing across the passive fire protection industry.
The Train the painter Logbook App is available to Train the painter students, Registered Companies and Affiliate Training Providers, making it easier to keep training records organised and up to date.
Since 2016, PFPNet has brought together specialists from across the global hydrocarbon and energy sectors, contributing to technical guidance, training, research, international standards and industry best practice. Corrodere Academy is proud to work with PFPNet to deliver the PFPNet Passive Fire Protection Coating Inspection course, developed using PFPNet’s specialist technical expertise. The training covers both epoxy and cementitious PFP systems and provides inspectors with the knowledge required to assess the quality of PFP installation. Ten years on, PFPNet continues to play an important role in strengthening competency and technical understanding throughout the passive fire protection industry.
The app allows trainee progress and task hours to be recorded digitally, giving students and supervisors a straightforward way to manage practical training requirements. From monitoring progress to maintaining training records, the Logbook App keeps essential information together and accessible wherever training takes place. ■
CORRODERE ACADEMY PCE JULY – SEPTEMBER 2026
“The Diploma programme is a great chance to learn in depth about paint chemistry, paint material testing and corrosion basics. For me, training and learning are never-ending processes.” Congratulations, Sinan – a fantastic achievement!
82
Corrodere Academy Registered Companies & Affiliate Providers 3T Training Services
Bin Quraya Company Ltd Blast Clean and Coatings Ltd
A1 Powder Coatings Ltd Abbey Protective Coatings Ltd
Bradleys Metal Finishers
Access & Coating Group
Brand Energy & Infrastructure Services (BEIS) BRIC
ADCAM Fabrications Ltd
BRIC Brook Blast Ltd
Advanced Industrial Coatings Ltd (AIC) AkzoNobel Alp Access Altrad Prezioso (Angola)
Buckingham Coatings C Jones & Sons Ltd C&D Access
Applewood Painting Company Cairnhill Structures Arabian Pipecoating Company Ltd (APCO)
ARS UK Ltd
CAKE Commercial Services Ltd
Carpenter & Paterson Ltd
CORRODERE ACADEMY PCE JULY – SEPTEMBER 2026
Caterpillar (NI) Ltd Assured Coatings
Cimolai S.p.A
Atlas Coating Ltd Atlas Coating Ltd AW Rail Services Ltd
Cladspray Solutions Ltd Coating Consulting Services COFIP Solutions
Barrier Fire Protection Ltd
Complete Coating Services
BDS Industrial Painting
Control de Revestimientos SL Corrosion Academy South Africa
Bell Group Ltd
Bilfinger
Corrous Industrial Group
Curtiss Wright Surface Technologies
Corrodere Academy Registered Companies & Affiliate Providers
Dalkia Facilities Ltd
83
FMC Technologies Ltd T/A Technip FMC
Dangle Academy Ltd Galco Steel Ltd Dart Industrial Services Ltd Grand Bahama Shipyard Ltd Denholm Universal Ltd
Group Industrial UK Ltd
DF Coatings Ltd
Hankinson Whittle Ltd
Diversified Lines Petroleum Services (DLPS)
Harrisons Engineering Lancashire Ltd HAY-TEK (Madacan)
EIS Infrastructure Services
HC Technical Consulting and Contracting Services Ltd Herrington Industrial Services Ltd
Elite Blasting Solutions Ltd Hi-Tech Surface Treatment Ltd Elite Coatings International Ltd Hunter Steel Ltd
Hutchinson Engineering Ltd Enzo Corrosion Services Eptec ESCS Training & Recruitment Ltd
Impact Coatings Industrial Blasting & Coatings Training (IBCT) Inspection Services (Scotland) Ltd
Falcon Tower Crane Services InterGroup Ltd Ferrous Protection Ltd FI Coatings Ltd
Firecote Ltd
IV Rail Ltd
J & D Pierce
Jack Tighe Ltd
CORRODERE ACADEMY PCE JULY – SEPTEMBER 2026
Elliott Environmental Drainage Ltd
84
Corrodere Academy Registered Companies & Affiliate Providers NEBC Site Services Ltd Jaeren Overflatebehandling AS JMK Training NL Williams Group K&N Finishers (Southern) Ltd
NMDC Energy Norco Composites Ltd
KAEFER Ltd
KGD Enterprises Ltd
Northpoint Ltd
L & N Labour Solutions Lanarkshire Welding Co. Ltd
NSB Infrastructure
Lassarat Angola Comercial Lda
Nusteel Structures Ltd NZ Corrosion Services Ltd
Ledwood Protective Coatings Ltd
One Stop Coatings
Liebherr Container Cranes Ltd
OneAIM Optimiza Protective & Consulting, SL
LJF Powder Coating Ltd
CORRODERE ACADEMY PCE JULY – SEPTEMBER 2026
MacTaggart Scott
Panthera Solutions Inc PAPYRUS, Lda
Marval Marine Services Ltd Pershore Dip Coating Limited McGeoch Technology Ltd Metallisation Ltd
Powertherm Contract Services Ltd PPG Coatings Europe B.V.
Metspray NZ
Prezicon Ltd PSI Global Training Ltd
Miller Fabrications Ltd MONTI - Werkzeuge GmbH Mozambique Inspection & Corrosion Services Lda NARUS Auditoria e Consultoria
RAMP UK ltd Rapid (NW) Ltd Ri3 Technical Services & Specialty Coatings
Corrodere Academy Registered Companies & Affiliate Providers
RLP Painting Contractors Ltd
85
Technomechanica Ltd
Robert Nicholas Ltd Rodopi Academy Tema Protective Coatings S E Railway Ltd
Searay Services Ltd
Thomson Protective Coatings
TIS (NGA) Ltd Trade Techs Northern Ltd
Shanghai Zhenhua Heavy Industries Co Ltd
Transocean Coatings Nigeria Ltd Travers Protective Coatings Ltd
Shirley Industrial Painters & Decorators Ltd Shutdown Maintenance Services Ltd (SMS)
UHP Systems Ltd
ULA (BG) Ltd SMT Ltd (Standish Metal) Vale Protective Coatings Ltd
VIP Verniciatura Industriale Pesarese Srl Solent Protective Coatings Ltd
VolkerLaser
Specialist Coatings & Inspection Ltd (SCI)
W G Beaumont & Son Ltd
Specialist Painting Group Ltd (SPG) STM Coatech Kalite Denetim Belgelendirme Ltd
Wardle Painters Ltd
Straight Outta Surface Training LLC Wescott Industrial Services Ltd Taziker Industrial Ltd Tech Dec Ltd
William Hare Ltd
Technija JSC
Wilson IS Ltd
CORRODERE ACADEMY PCE JULY – SEPTEMBER 2026
Smulders Projects UK
NEWS PCE JULY – SEPTEMBER 2026
86
NEWS
SUCCESSFUL PAINTING PARTNERSHIP HMG Paints has partnered with specialist commercial contractor Anglia Decor to successfully deliver a comprehensive
Utilising HMG’s advanced 1K DTM (Direct to Metal) system, Anglia Decor transformed the tired yellow unit into
a completely refreshed white and red livery. The project highlights how high-performance coatings can streamline commercial transformations with zero operational downtime.
Operating within a live commercial environment presented a unique set of logistical challenges. Anglia Decor was tasked with executing a complete coating upgrade while ensuring minimum disruption to customers accessing their storage units. Overcoming these strict site constraints required a combination of skilled application craftsmanship and a rapid turnaround, which was enabled by HMG’s highly efficient coating system.
87
Anglia Decor chose HMG Paints over competing manufacturers due to HMG’s product coverage capabilities, ease of ordering and exceptional technical service provided by representative Roger Blinco. To minimise on-site delays, HMG coordinated direct-tosite deliveries, ensuring all coatings arrived precisely when needed to support a seamless set-up and an efficient workflow. “We would recommend using HMG products and support service; we have found the 1K DTM has great coverage and gives a uniform finish,” said Steve Massey, owner of Anglia Decor. “The ease of order and quick delivery time made it incredibly easy to set up the job, get started, and achieve a high-quality result on a busy, live site.”
NEWS PCE JULY – SEPTEMBER 2026
refurbishment of a selfstorage warehouse unit.
88
The 1K DTM system used on the project is engineered to combine primer and topcoat properties into a single, high-performance formulation. Formulated for direct application to metal substrates, the product offers excellent adhesion, corrosion resistance and colour retention. Applied via spray application by the Anglia Decor team, the coating delivered an impeccable, uniform finish across the facility’s surfaces, significantly upgrading the unit’s aesthetic appeal and long-term durability.
VERIFIED VESSEL PERFORMANCE
NEWS PCE JULY – SEPTEMBER 2026
International, AkzoNobel’s marine coatings brand, has announced that Lloyd’s Register (LR) has verified its vessel performance analysis methodology as compliant with ISO 19030, the global standard for measuring changes in hull and propeller performance. The independent validation strengthens confidence in how vessel speed loss is measured and reported, providing shipowners, charterers and vessel performance analysts with greater assurance when using performance data to support operational decisions. LR confirmed that International applies ISO 19030-compliant methodology to analyse vessel performance
Barry Kidd
Dr Chris Craddock
data across its reporting. ISO 19030 provides a standardised framework for vessel performance measurement, enabling a consistent and transparent approach to evaluating in-service outcomes. The standard is widely recognised across the industry as the benchmark for measuring vessel performance, and independent verification of alignment with the standard represents an important milestone for operators seeking reliable and comparable data.
verification is a significant milestone for International and our customers, reinforcing confidence in the robustness and transparency of the analysis underpinning our reporting.
Following verification of the methodology by LR, International used it to report the performance of the Intercept 8500 LPP coating indicating a speed loss up to 1.2% over the docking cycle. “ISO 19030 gives the industry a consistent and transparent way to measure vessel performance,” says Barry Kidd, Business Development Manager, Vessel Performance, AkzoNobel. “This independent
“Achieving low speed loss is the result of multiple factors coming together from selecting coating technology that aligns with how a vessel operates, through to highquality application in dock and ongoing operational and maintenance decisions. By combining high-quality data with this approach, we enable more informed, datadriven decision-making. For well-managed fleets, this supports consistently strong performance outcomes and helps operators meet both their economic and environmental goals,” Kidd continues. “As pressure grows on the maritime industry to improve efficiency and demonstrate measurable emissions performance, the ability to rely on consistent, independently-verified data is becoming increasingly
PosiTector Inspection ®
Unrivaled probe interchangeability Coating Thickness Probes n Ferrous n Non-Ferrous n Combination n Ultrasonic
Surface Profile Probes n Depth Micrometer n Replica Tape Reader
Environmental Conditions Probes n Integral n Cabled Magnetic Probe n Anemometer Probe n 1/2” NPT n Infrared
WiFi
Hardness Probes n Shore n Barcol
Salt Contamination Probe n Bresle Method
Gloss n 60 ° n 20 ° /60 ° n 20 ° /60 ° /85 °
Ultrasonic Wall Thickness Probes n Corrosion n Multiple Echo Thru-Paint n Precision n Low Frequency n Xtreme
Customized Inspection Kits... Build your own kit from a selection of gauge bodies and probes to suit your needs. Coating Thickness
Surface Profile
Environmental Conditions
Hardness
Salt Contamination
Scan here to learn more
Ultrasonic Wall Thickness
Backwards Compatibility! The PosiTector gauge accepts ALL coating thickness (6000/200), environmental (DPM), surface prole (SPG/RTR), salt contamination (SST), hardness (SHD/BHI), gloss (GLS), and ultrasonic wall thickness (UTG) probes manufactured since 2012. DeFelsko Corporation l Ogdensburg, New York USA Tel: +1-315-393-4450 l Email: techsale@defelsko.com 1-800-448-3835 l www.defelsko.com
90
NEWS PCE JULY – SEPTEMBER 2026
important,” says Dr Chris Craddock, Global Lead, Marine Asset & Operational Performance, Lloyd’s Register. “By confirming vessel performance analysis methodology from International against ISO 19030, LR is helping to strengthen confidence in how hull and propeller performance is measured, reported and compared across the sector. That matters because trusted performance data supports better operational decisions, clearer investment choices and more credible progress towards shipping’s decarbonisation goals.” The news also comes at a time of increasing regulatory focus on shipping emissions, with the International Maritime Organization’s regulatory framework placing greater scrutiny on vessel efficiency across the industry.
THREE BECOME ONE FOR WATER JETTING SAFETY A new UK unified code of practice has been launched to promote the safety of all forms of water jetting. The
Water Jetting Association (WJA), the UK trade body for the water jetting industry, which has developed the code, says it marks the biggest step forward in standardisation in the waterjetting industry in decades. The unified set of standards is designed to help minimise all risks associated with water jetting, including fluid injection injuries that can cause serious harm and even fatalities. The WJA Black Code, as it is being called, now sets safety standards for all types of water jetting including pressure washing, sewer jetting, industrial cleaning, surface preparation and hydrodemolition. It brings together standards previously defined in three WJA codes of practice. “Our new single code of practice represents the biggest step forward in defined water jetting standards since the WJA introduced its first code in 1982,” says WJA Chairman
Lee O’Callaghan. “It’s an exciting and important milestone for the WJA, our members and for every organisation that uses water jetting. There is now one code for water jetting across all pressures. “It will also be easier for procurement professionals and users of water jetting services to specify water jetting standards, which is critical given the hazards associated with the process. All they now have to do is to require contractors to comply with the WJA code of practice.” The UK Health and Safety Executive has advised on the development of the new code of practice, and will refer to it as industry best practice when carrying out its investigations into possible safety lapses. The WJA says this reinforces the importance for water jetting contractors of all types to adhere to the code when carrying out their work.
Elevate your coatings expertise with
SPECIAL
OFFER
78
SAVE
£
When you purchase both Fitz’s Atlas of coating surveys and Fitz’s Atlas of coating defects. Only £300 for both (usually £189 each)
Streamline your coating surveys with Fitz’s Atlas of coating surveys - a handy guide containing comprehensive detail and visual assessment for coatings evaluation.
Understand coating defects with Fitz’s Atlas 2, providing a detailed visual guide with a a description of the defect, probable causes, how to prevent it and how to repair it.
To order visit Fitzsatlas.com
+44(0)1252 732220
office@mpigroup.co.uk
92
LATEST FIRE PROTECTION Hempel has launched Hempafire Optima 515, the latest addition to its waterborne cellulosic passive fire protection (PFP) range. Developed for civil infrastructure projects, the new product is designed to protect interior steel structures while helping customers reduce paint consumption and total application costs. Hempafire Optima 515 has been developed for civil infrastructure projects
At all pressure levels, water jetting presents significant safety risks. It is why, over 30 years, the WJA developed its highly respected codes of practice, each known by the colour of its cover.
NEWS PCE JULY – SEPTEMBER 2026
The Blue Code for high and ultra-high pressure water jetting was the first, followed by the Red Code for water jetting in sewers and drains. The Purple Code for pressure washers was launched in 2024. The WJA Black Code, which has a black cover, brings these three codes of practice together in a fully revised and updated format, which is designed to be easier to use. Lee O’Callaghan says: “In its digital format via the WJA App, the new WJA Black Code is easier to search than ever before,
so water jetting teams can rapidly find the guidance they need. We hope these significant ease-of-use advances mean the WJA Black Code will come to be used as a daily reference guide on worksites across the UK. We hope it will lead to many more companies, delivering all types of water jetting, using it create their safe systems of work and their risk assessments and method statements.” The new WJA Black Code will continue to underpin the WJA’s City & Guildsapproved water jetting training programme, the most extensive in the UK, with more than 22,000 operatives trained every year. Every operative who attends and passes a WJA training course will be given access to the new code of practice, via the WJA App.
Hempafire Optima 515 provides protection for steel exposed to cellulosic fire scenarios, offering fire ratings of up to 150 minutes. It has been tested in accordance with the BS 476 standard and certified by the third-party certification body ApplusFire. “Passive fire protection has always been about safety, but today’s projects also require more efficient application and reduced material consumption,” says Roger Soler, Product Manager C-PFP at Hempel A/S. “With Hempafire Optima 515, we are strengthening our waterborne PFP offering for civil infrastructure projects while helping customers meet certified fire protection requirements and improve efficiency on site.” Hempafire Optima 515 is engineered for productivity and cost efficiency across low- to mid-section factor open steel sections, which
High-quality, easy-to-apply wraps that protect irregularly shaped fittings and require minimal surface preparation.
Wax-Tape® #1
Wax-Tape® #2
A very durable wrap that uses a thick, non-stitch bonded synthetic fabric and has no clay fillers, so it stays conformed to irregular profiles. The wrap requires no abrasion blasting, can be backfilled immediately and is compatible with cathodic protection.
A unique, microcrystalline-wax-saturated wrap that slowly firms up to provide excellent above and belowground protection. Comes in a variety of colors and usually requires no outerwrap.
Anticorrosion Wrap:
Self-Firming Anticorrosion Wrap:
Wax-Tape® HT-3000
High-Temperature Anticorrosion Wrap:
Designed for operating temperatures up to 230°F (110°C), Wax-Tape® HT-3000 wrap can be used on high-temperature oil and gas piping, on compressor station discharge piping, beneath thermal insulation and in high ambient temperature conditions.
Only Trenton makes Wax-Tape brand anticorrosion wrap systems, with primers, wraps and outerwraps.
®
www.trentoncorp.com
94
represent a large share of structural steel fire protection projects. Its advanced thermal insulation performance delivers certified fire protection with reduced dry film thickness requirements, supporting optimised material consumption while maintaining compliance. Developed to enhance application efficiency within its class, Hempafire Optima 515 features a high 75% solids content. The product can be applied with ease at up to 1.5mm DFT per coat and dries rapidly to a smooth, high-quality finish. This enables most steel sections to achieve the required fire protection rating in just two coats within a single working shift.
NEWS PCE JULY – SEPTEMBER 2026
The result is a faster, more streamlined application process that reduces labour requirements, shortens project timelines, minimises downtime and lowers overall project costs, delivering greater value for both contractors and asset owners alike. The launch is complemented by Hempafire Optima 510, a versatile solution optimised for lightweight steel sections. Together, Optima 510 and Optima 515 provide a broader solution, enabling specifiers to select the appropriate coating for different section
requirements within the same project. Both coatings feature very low VOC content and emissions and are supported by independently-verified Environmental Product Declarations. These declarations provide transparent, documented environmental information that may assist project teams in meeting green building certification requirements, subject to the specific criteria and assessment protocols of each rating scheme. The range is compatible with Hempel-approved primers and topcoats for waterborne PFP systems, allowing the coating system to be adapted to project requirements and aesthetic preferences. Hempafire Optima 515 has initially been launched in the Middle East, with expansion to additional countries that follow BS 476 standards planned in the coming months.
NEW SELF-CLEAN COATING A new self-cleaning extrusion coating which uses natural rainfall to help remove dust and stains from exterior walls has been launched by AkzoNobel in China. The Trinar SC Series was developed specifically to support the country’s urban renewal. The new coating
will address demand in the high-end building market for products capable of protecting buildings that have complex curved surfaces and irregular architectural forms. The coating features hydrophilic self-cleaning technology and is certified to the international AAMA 2605 weatherability standard. As well as offering long-lasting surface protection, the coating therefore also retains a pristine, like-new façade appearance over time. “This is a significant innovation which will enable customers to unlock the long-term value of selfcleaning technology, with no changes to existing customers’ coating lines – and zero compromise on colour selection or finish texture,” explains James Kavanagh, Commercial Director of AkzoNobel’s Coil and Extrusion business. He adds that by reducing the frequency of manual highrise cleaning procedures, the next-generation coating can contribute to lowering operation and maintenance costs across a building’s entire lifecycle. It can also help reduce the amount of water, chemicals and maintenance resources typically associated with cleaning building exteriors. This makes it ideally suited for the construction
95
The façade of 16 On An Street in Hong Kong, coated with Trinar SC Series coatings
The factory-applied Trinar SC Series will help the construction industry meet the new operational and maintenance challenges brought about by China’s ongoing pursuit of premium building quality. To help achieve striking design impact, many high-end commercial buildings feature complex curved surfaces and irregular architectural forms, which makes façade cleaning and upkeep far more technically demanding. “As cities reach new heights and aesthetics evolve with the times, the steady upgrading of urban spaces is positioning architectural design at the core of shaping urban identity,” Kavanagh continues. “With
a global commercial track record of more than 25 years in coil self-cleaning coatings, we’re ideally placed to meet this increasing demand.” Long-term on-site testing of the new coating was carried out at an office building project in Dongying Economic Development Zone. Throughout the trial period, the new product delivered exceptional, consistent self-cleaning performance. Beyond this pilot project, the system has also been successfully deployed in a range of premium building schemes, including 16 On An Street in Hong Kong. The launch will soon be rolled out to more high-end building applications, further strengthening AkzoNobel’s portfolio of highperformance architectural coatings designed to support the evolving
needs of China’s premium construction sector.
INDIAN ACQUISITION Tri Polarcon Pvt Ltd, a Punebased manufacturer and exporter of construction chemicals in India, has acquired 100% ownership of Rockhard Polycoats Pvt Ltd, a fellow Pune-region manufacturer known for its work in industrial epoxy flooring, protective coatings and structural repair. The two companies work in adjacent parts of the construction chemicals industry. Tri Polarcon, which sells under the Triflor brand, makes epoxy, PU, EPU and water-based flooring, waterproofing, protective and anti-corrosive coatings, sealants, grouts, adhesives, mortars and concrete admixtures, backed by in-house R&D and manufacturing. Rockhard Polycoats, headquartered in Pune, has
NEWS PCE JULY – SEPTEMBER 2026
requirements of irregular curtain wall geometries, as well as supporting more sustainable building operations over time.
96
built a more specialised portfolio — industrial epoxy and PU flooring, protective coatings, antistatic flooring, car parking flooring, and structural repair work including restoration and steel protection — segments that typically take years of site experience and long-standing contractor relationships to build. India’s construction chemicals sector has been shaped in recent years by larger, more technically demanding projects – industrial facilities, warehousing, infrastructure, and pharma and food-grade builds – that increasingly need flooring, waterproofing,
coatings and structural repair handled together rather than through separate vendors. “I’ve spent more than twenty years in this industry, and I know a deal like this doesn’t mean much on its own,” said Vijay Mohite, Chief General Manager of Tri Polarcon. “What matters is what we do with it – bringing two strong teams together and making sure customers actually feel the benefit.” Tri Polarcon says it intends to build on Rockhard Polycoats’ existing technical capabilities and client relationships rather than replace them, framing the acquisition as the start of an integration
Understanding the problem to find your solution • Protective Coatings • Tank Linings • Waterproofing • Hygiene Coatings • Bund & Sump Linings • Polyurea • Resin Flooring
01362 691484 www.corrolesseatern.co.uk
process rather than the end of one. The company has not disclosed transaction value, employee numbers or an integration timeline. The deal adds to a broader pattern of consolidation in India’s construction chemicals and coatings sector, where manufacturers have been widening their range to keep up with larger, more complex projects. With this acquisition, Tri Polarcon takes another significant step towards becoming one of India’s leading names in industrial epoxy and PU flooring, waterproofing, protective coatings and construction chemical solutions. ■
COMING UP
OCTOBER-DECEMBER 2026 ISSUE THE LEADING PROTECTIVE COATINGS MAGAZINE
SPECIAL EDITORIAL FEATURES: • Metallisation • Petrochemical • Floor Coatings • Polyurea/Polyurethane FOCUS: Marine EVENTS: PDA Europe
Subscribe to receive PCE Magazine
PCE will continue to showcase its regular features; Lifting the Lid, Upfront and Spotlight, as well as featuring the latest news and developments in marine and offshore coatings PCE International is published quarterly by MPI Group Peel house, Upper South View, Farnham, Surrey. GU9 7JN. UK To advertise in the magazine, on the website and /or newsletter contact Nick Carugati: nick@pce-international.com
Endorsed by
Stand Out as an Industry Expert in Protective Coatings & Corrosion Control
Approved by
Distance learning Diploma in Coatings for Corrosion Control A prestigious advanced qualification for experienced coating specialists • Join an exclusive network of coating & corrosion professionals • Become eligible to apply for MICorr membership with ICorr • Achieve the DipCC designation
arrow_left_roundel Scan to view course content & enrol +44 (0) 1252 732236 info@corrodere.com corrodere.com