
International Research Journal of Engineering and Technology (IRJET) e-ISSN: 2395-0056
Volume: 13 Issue: 04 | Apr 2026 www.irjet.net p-ISSN: 2395-0072

International Research Journal of Engineering and Technology (IRJET) e-ISSN: 2395-0056
Volume: 13 Issue: 04 | Apr 2026 www.irjet.net p-ISSN: 2395-0072
Pranjali Lokhnade1, Diya Lokhande2, Namrata Nikam3 , Omkar Khairmode4, Vikas Jadhav5
1-3
Student, Dept. of Mechanical Engineering, KBP Polytechnic, Satara, Maharashtra, India
4Lecturer, Dept. of Mechanical Engineering, KBP Polytechnic, Satara, Maharashtra, India
5Owner, Shree Ganesh Industries, Karad, Maharashtra, India
Abstract This paper emphasizes to increase the productivity and to minimize the manpower and labor cost. The main objective of our project to move the clamping device and feed to the sheet up to 0.5mm to 1.2mm and length is to 300mm to the machine to carry the other operation like blanking, shearing, etc. This is used in many industrial applications. In our paper double acting cylinder is used instead of single acting cylinder to minimize the cost of production and to achieve a lighter weight. This is operation is carried out sequence first pressurised air passed in small double acting cylinder up to 8 bar to 10 bar pressure and they clamp the sheet, at this idle time of large double acting cylinder field with pressurised air and our sheet is fed. When does it complete their forward stroke? In return stroke direction control valve 5/2 is used with changes to the position and field air passes to the muffler. Muffler is used to reduce the noise of operation. So, from this project we achieve more productivity, Reduce manpower and labour cost. It also reduces the fatigue of operators.
The alternators plates are being manufactured by the blanking operation on blanking machine. The sheet is provided manually for the blanking operation. After then blank is provided and again remove the sheet manually. Thus, it causes improper utilization sheet metal. And the timerequiredfortheoperationismoreandwhichleadsto low productivity.Byobserving we came toconclusion that operation is not safe for the blanking and for the operator also as the fingers of the operator are hurted. As per the companynorms,safetyofemployeesisbeingcomefirst.So by analyzing all these factors the company took a decision to reduce the cycle time for the blanking operation and in the interest of safety of operators we are design and manufacturing the attachment which will reduce the cycle time andabsolutelysafe tohandle.Anyphysical activityin this world by human being causes great discomfort. For remaining competitive every attempt is been made to minimize the required labour and cost. Keeping focus on achievealltheseobjectivesbrainstormingsessionwasheld and decided to design and develop attachment which can reducethemanualeffortngreatextentintermstoachieve higher productivity, safe working, accident free and economic.
Aircompressorsare the energyconversionelements in pneumaticsystem.Theyimpartmechanicalenergytoairby compressing it. The main difference between pumps and compressoristhatthefluiddeliveredbycompressorsair,is compressedand under pressure at the time it isdelivered, evenifthereisnoloadonthesystem.Mostdevicesusedto compress air are similar in concept and perhaps even in hardware to hydraulic pump and selection considerations arealsosimilar.Anaircompressorisadevicethatconverts power (using an electric motor, diesel or gasoline engine, etc.) into potential energy stored in pressurized air (i.e compressed air). By one of several methods, an air compressor forces more and more air into a storage tank, increasing the pressure. When tank pressure reaches its upper limit the air compressor shuts off. The compressed air,then,isheldinthetankuntilcalledintouse
Pneumatic cylinders (sometimes known as air cylinders) are mechanical devices which use the power of compressedgastoproduceaforceinareciprocatinglinear motion. In pneumatic cylinder a compressed air is used as working fluid andconverts it into kinetic energy as the air expandsinanattempttoreachatmosphericpressure.This air expansion forces a piston to move in the desired direction.Thepistonisadiscorcylinder,andthepistonrod transfers the force it develops to the object to be moved. Engineers prefer to use pneumatics because they are quieter,cleaner,anddonotrequirelargeamountsorspace for fluid storage. Because the operating fluid is a gas, leakage from a pneumatic cylinder will not drip out and contaminate the surroundings, making pneumatics more desirablewherecleanlinessisarequirement.
The directional valve is one of the important parts of a pneumatic system. Commonly known as DCV, this valve is used to control the direction of air flow in the pneumatic system. The directional valve does this by changing the position of its internal movable parts. This valve was selected for speedy operation and to reduce the manual effort and also for the modification of the machine into automatic machine by means of using a solenoid valve. A solenoid is an electrical device that converts electrical
International Research
Volume: 13 Issue: 04 | Apr 2026 www.irjet.net p-ISSN: 2395-0072
energy into straight line motion and force. These are also used to operate a mechanical operation which in turn operatesthevalvemechanism.Solenoidsmaybepushtype or pull type. The push type solenoid is one in which the plunger is pushed when the solenoid is energized electrically. The pull type solenoid is one in which the plungerispulledwhenthesolenoidisenergized.Thename of the parts of the solenoid should be learned so that they canberecognizedwhencalledupontomakerepairs,todo serviceworkortoinstallthem.
D. FRL Unit
Air leaving a compressor is hot, dirty, and wet which candamageandshortenthelifeofdownstreamequipment, suchasvalvesandcylinders.Beforeaircanbeuseditneeds to be filtered, regulated and lubricated. An air line filter cleans compressed air. It strains the air and traps solid particles(dust,dirt,rust)andseparatesliquids(water,oil) entrainedinthecompressedair.Filtersare installedinthe air line upstream of regulators, lubricators, directional controlvalves,andairdrivendevicessuchascylindersand air motors. Airline filters remove contaminants from pneumatic systems, preventing damage to equipment and reducing production losses due to contaminant related downtime. Downtime in an industrial plant is expensive; often it is the result of a contaminated and poorly maintainedcompressedairsystem
III. DESIGN AND CALCULATIONS
A. Force Calculation:
DiameterofPiston(d)=10mm
DiameterofBore(D)=32mm
Lengthofcylinder(L)=300mm
B. Free Air Consumption:
DiameterofPiston(d)=10mm
DiameterofBore(D)=32mm
Lengthofcylinder(L)=300mm
TABLE II. FREEAIRCONSUMPTION
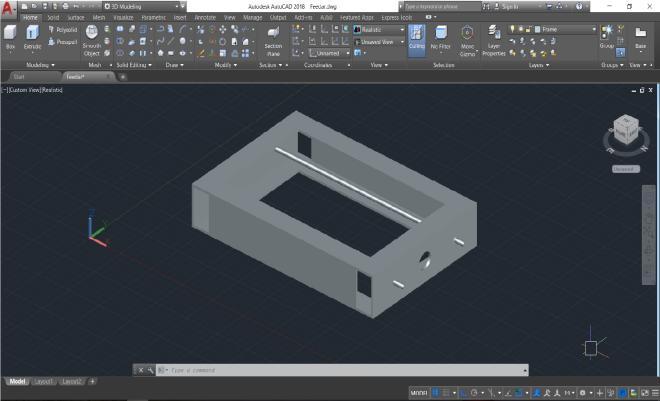
A. Time requirement:
Manual operation: The cycle time to produce one blank without feeder is 5-7 second. In one hour without feeder blank produces 600 on sheet. By considering shift of 8hrs theblankproducesare4200
Machine operation: The cycle time to producing one blank with feeder is 3-5 second. In one hour with feeder blank produces 900 on sheet. By considering shift of 8 hrs the blankproducesare6300.
TABLE III. TIMEREQUIRED
B. Cost per piece:
ManualOperation:TheshiftrateofoperatorisRs.300.And numberofjobscompletedin1shiftis4200asperthetable givenabove.So,thecostofonejobisRs.0.07.
Machine Operation: The shift rate of operator is Rs. 300. And number of job completed in 1 shift is 6300 as per the tablegivenabove.SothecostofonejobisRs.0.04
International Research Journal of Engineering and Technology (IRJET) e-ISSN: 2395-0056
Volume: 13 Issue: 04 | Apr 2026 www.irjet.net p-ISSN: 2395-0072
TABLE IV. RATEFORONEJOB
Saving for one job = Rate for manual operation for 1 jobRateformachineoperation.
Inonedayforonejob
=Rs.0.07–Rs.0.04
=Rs.0.03
Savingfor6300 =Rs.0.03X6300
Jobsinoneday =Rs.189
Monthlysaving =Rs.189X26
=Rs.4,914
Yearlysaving =Rs.4914X12
=Rs.58,968
C. Electricity Consumption: TABLE V. ELECTRICITYCONSUMPTION
Electricitycost =UnitRateX(KW-Hr)
=Rs.10X0.746X208 =Rs.1,551.68
Electricitycost(Yearly) =Rs.1,551.68X12 =Rs.18,620.16
D. TotalCost:
MonthlyMaintenancecost =Rs.500
YearlyMaintenanceCost =Rs.500X12 =Rs.6,000
TotalCostSavingYearly =PartA–(PartB+PartC) = Rs. 58,968 – (Rs.208 + Rs. 6,000)
TotalCostSavingYearly =Rs.52,759
TotalCostofMachine =Rs.9,440
Thus by above cost analysis we can calculate the attachment profitable and the attachment has a high returnsoninvestment.
In this paper the design and manufacturing of pneumaticfeederispresented.Thebenefitofthispaper is that is help to pass the metal sheet and reducing the human effort. The solution is economically viable, due to its simple construction and the use of inexpensive materials and construction methods. The reduced processing cycle also allows a higher production rate. The design of machine is simplified and robust life of machine is longer and the operator can do the blanking operation without paying too much attention and it can be easily done with less time compared to conventional method of using file for the blanking operation. As all safety precaution are implemented during manufacturing there will be no harm to a person operating the machine. With thehelpofthisattachmentwehaveprovedthatoperation time is reducing 2 to 3 sec and 30% production are increased.Thus the productivityofthe blankingoperation isimprovedresultingintohighprofittothecompany.
[1] MadhuKumarV“DesignandFabricationofPneumaticSheet MetalCutting andBending Machine.InternationalJournalof EngineeringResearchAndAdvancedTechnology(IJERAT).
[2] VishalTambat,NilkanthRane,OmkarSavant,4PankajYadav. Pneumatic Shearing and Bending Machine, IJRRCME, Vol. 2, Issue1,pp:(9-18),Month:April2015–September2015.
[3] Aniruddha Kulkarni, Mangesh Pawar “Sheet Metal Bending Machine. IJIERT, I SSN: 2394-3696 VOLUME 2, ISSUE 3, March.-2015
[4] Li, T.C., Wu, H.W., Kuo, M.J.: A study of gas economizing pneumaticcylinder.JournalofPhysics:Conferenceseries48, 1227–1232 (2006). Beater, P.: Pneumatic Drives: System Design,ModellingandControl.Springer,Berlin(2007).
[5] Zhang, Y., Cai, M., Kong, D.: Overall Energy Efficiency of Lubricant-Injected Rotary Screw Compressors and Aftercoolers. In: Asia-Pacific Power and Energy Engineering Conference2009,pp.1–5(2009).
[6] Koyamada, K., Tamura, S., Ono, O., Cai, M., Kagawa, T.: Simulation for Energy Savings in Pneumatic System. In: Systems Modeling and Simulation, pp. 258–261. Springer, Japan(2007).
[7] Doll, M., Sawodny, O.: Energy Optimal Open Loop Control of Standard Pneumatic Cylinders. In: 7th International Fluid PowerConference,Aachen,pp.259–270(2010).
[8] Herrmann, C., Kara, S., Thiede, S.: Dynamic life cycle costing based on lifetime prediction. International Journal of SustainableEngineering4(3),224–235(2011).18.
[9] Yang,A.,Pu,J.,Wong,C.B.,Moore,P.:By-passvalvecontrolto improve energy efficiency of pneumatic drive system. ControlEngineeringPractice17(6),623–628(2009).
International Research Journal of Engineering and Technology (IRJET) e-ISSN: 2395-0056
Volume: 13 Issue: 04 | Apr 2026 www.irjet.net p-ISSN: 2395-0072
BIOGRAPHIES
PranjaliLokhnade
DiyaLokhande
NamrataNikam
OmkarKhairmode
VikasJadhav