
International Research Journal of Engineering and Technology (IRJET) e-ISSN: 2395-0056
Volume: 13 Issue: 03 | Mar 2026 www.irjet.net p-ISSN: 2395-0072
International Research Journal of Engineering and Technology (IRJET) e-ISSN: 2395-0056
Volume: 13 Issue: 03 | Mar 2026 www.irjet.net p-ISSN: 2395-0072
Manjunatha N S1 , S Shylin H Jose2 , B S Praveen Kumar3
1 P G Student, Dept. of Mechanical Engineering, Adiyaman college of Engineering, Hosu, Tamil Nadu, India
2 Professor, Dept of Mechanical Engineering, Adiyaman college of Engineering, Hosu, Tamil Nadu, India
3 Professor, Dept. of Mechanical Engineering, GEC, Kushalnagara, Karnataka, India
Abstract - ShieldedMetalArcWelding(SMAW)isoneofthe most widely adopted welding processes in industrial fabrication due to its simplicity, cost-effectiveness, and adaptability. However, welding-induced distortion remains a significant challenge, particularly in mild steel plates, where non-uniform heating and cooling cycles generate residual stresses and dimensional inaccuracies. Excessive distortion adverselyaffects structural integrity, assemblyprecision, and overallmanufacturingefficiency.Thisreviewpaperpresentsa comprehensive analysis of existing research on SMAW parameter optimization aimed at minimizing distortion. Key process parameters such as welding current, arc voltage, travel speed, electrode diameter, root gap, groove angle, and welding position are examined. Various optimization techniques includingTaguchimethod,ANOVA,GreyRelational Analysis (GRA), Response Surface Methodology (RSM), and Finite Element Analysis (FEA) are critically reviewed. The study identifies dominant parameters influencing distortion and highlights the importance of systematic parameter selection over conventional trial-and-error methods. The findingsprovideastrongfoundationforfurtherexperimental investigationandregressionmodeldevelopmentfordistortion control in mild steel SMAW applications.
Keywords: SMAW, Welding Distortion, Mild Steel, Taguchi Method, ANOVA, Heat Input, Optimization Techniques.
Weldingisapermanentmetaljoiningprocesswidelyusedin manufacturing, construction, and heavy engineering industries.Amongvariousweldingprocesses,ShieldedMetal Arc Welding (SMAW) remains highly popular due to its operational flexibility and low equipment cost. Despite its advantages,SMAWfrequentlyresultsinweldingdistortion due to uneven thermal expansion and contraction during heatingandcoolingcycles.Thisthermalimbalanceproduces Transverse shrinkage, Longitudinal shrinkage, Angular distortion, Rotational distortion, Bending, Buckling. Distortionleadstomisalignment,increasedreworkcost,and reduced dimensional accuracy. Therefore, optimizing welding parameters to minimize distortion has become a criticalresearchfocus.
Distortionprimarilyoccursduetothefollowingreasons
•Non-uniformheatdistribution
•Excessiveheatinput
•Improperclamping
•Largegrooveangle
•Highweldingcurrent
•Lowweldingspeed
•Heatinput
Sanjayetal(2023)optimizedofstickweldingparameters for joining dissimilar materials, specifically AISI 304 stainless steel and mild steel. They focused on evaluating mechanical properties, particularly tensile strength, while considering distortion and residual stresses developed duringwelding.V-groovebuttjointsof5mmthicknesswere weldedusingE6013electrodes,withweldingcurrentvaried from 90 A to 120 A. Tensile strength increased with increasingweldingcurrent,withmaximumtensilestrength observed at 120 A. All specimens fractured in the weld region, indicating the weld zone as the critical area. They found that proper selection and optimization of welding current significantly improve weld quality and joint performance in dissimilar SMAW welds [1]. Muhammad SaadAfzalet.al(2025)investigatedtheinfluenceofSMAW parameters on weld quality and mechanical properties of mild steel joints. Five SMAW process parameters were selected, with each parameter set at four evenly divided levels. Those sections were made using a combination of screening experiments, machine specifications, guidance from the American Welding Specification handbook, and inputfromweldingexperts.Theparameternames,units,and levelsweredepictedinTable-1. Theyfocusedonoptimizing weldingcurrent,voltage,andtravelspeedtoenhancetensile strength while minimizing weldingdefectsanddistortion. Theirresultsindicatethatweldingcurrentplaysadominant role in affecting joint strength and heat input, while improperparameterselectionleadstoexcessivedistortion andreducedweldintegrity.
Volume: 13 Issue: 03 | Mar 2026 www.irjet.net
increases.AstheWeldingcurrentofthemildsteelincreases, the longitudinal shrinkage also increases means the longitudinal shrinkage is proportional to the welding current.Bargraphwasplottedasshowninchart-1,2and3. Longitudinalshrinkageisminimumwhencurrentandplate thicknessisless
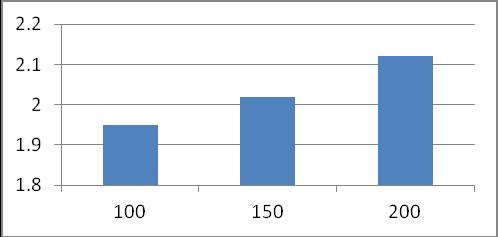
Theirstudyrevealsthatsystematicparameteroptimization significantlyimprovesweldquality,mechanicalproperties, andoverallfabricationefficiency Theoptimizedsettingwas welding current of 160A, groove angle of 60◦electrode diameterof3.25mm,rootgapof3mmandrootfaceof3mm [2]. L S. Sisira et al (2019) conducted experimental and analytical study on the effect of SMAW parameters on distortionandmechanical propertiesofmildsteel welded joints. They focused on key process variables such as welding current, voltage, travel speed, and electrode diameter, and evaluates their influence on heat input, angulardistortion,andtensilestrength.Experimentaltrials were conducted using butt welded mild steel plates, and distortionmeasurementsweretakenafterweldingtoassess deformationbehavior.StatisticaltechniquessuchasTaguchi method and ANOVA were employed to identify the most significant parameters affecting distortion. The results indicated that welding current and travel speed are the dominant factors influencing heat input and subsequent distortion, with higher heat input leading to increased angular deformation. Their study reveal that systematic optimization of welding parameters significantly reduces distortion while maintaining acceptable mechanical performance, thereby improving overall weld quality and dimensional accuracy [3]. Okwudili Simeon Ogbonna et al (2022)optimizedofTIGweldingparametersfordissimilar butt jointsof AISI1008 mildsteel and AISI316austenitic stainlesssteelusingagreybasedTaguchimethod.AISI316 austenitic stainless steel and AISI 1008 mild steel plates havingdimension(100×40×6)mmhavebeenselectedas thebasematerialsforTIGweldinginbuttjointconfiguration with 2.5mm gap between the two plates. A 1.6mm thick austeniticstainlesssteelweldingwire,ER309L,wasusedas thefillermaterial.Theresultsrevealedthatweldingcurrent was the most significant parameter with a 78.15% contributionbasedonANOVAanalysis[4].DevendraSingh et al (2020) investigated the effect of plate thickness and current on the longitudinal shrinkage in mild steel butt joints.Studiesrevealthatasthethicknessofmildsteelplate increases, the longitudinal shrinkage in distortion also
Chart -1: Longitudinalshrinkageatyaxisandcurrentatx axisof6mmthicknessMSplate.
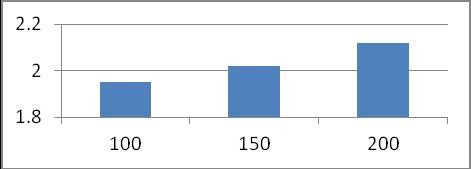
Chart -2: LongitudinalshrinkageatYaxisandcurrentatx axisof7mmthicknessofMSplate.
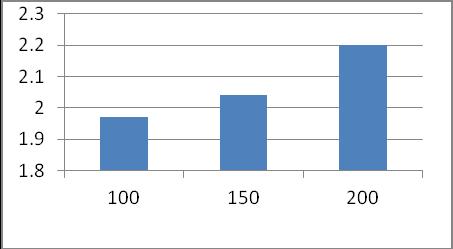
Chart -3: LongitudinalshrinkageatYaxisandcurrentatx axisof8mmthicknessofMSplate[5].
Harshal K Chavan et al (2012) simulated the complex arc weldingprocessbyusingthefiniteelementmethod(ANSYS) and studied the effects of varying the welding process parametersonthethermosmechanicalresponsesalsofound a relationship between them. Their study reveal that the welding speed increases by, the responses such as displacement, strain decreases. An increase of 33% of welding speed results in a significant decrease in Ydisplacement (11%), Z displacement (12%), and X-elastic strain (35%) [6]. P. Bharatha (2014) determined the influenceofvariousweldingparametersontheweldbeadof
International
Volume: 13 Issue: 03 | Mar 2026 www.irjet.net p-ISSN: 2395-0072
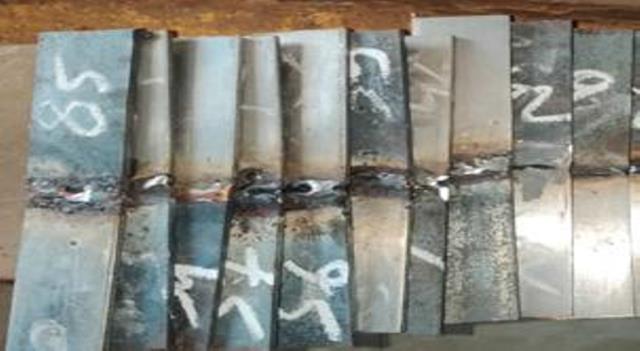
AISI316weldedjoint.IntheirworktheANOVAtechniqueis usedtoidentifytheinfluenceoftheweldingspeed,current, electrode, root gap on the strength of the material. It was foundthatweldingspeed(46.51%contribution)hasgreater influenceonbendstrengthandcurrent(96.75%)hashighest influenceontensilestrength.Furtherithasfoundthatroot gapshavesomeinfluenceonbothtensileandbendstrengths [7].BalaramNaiketal(2018)optimizedofshieldedmetal arcweldingprocessonDuplexStainlessSteel(DSS2205). They found that the influence of filler wire material is minimum and welding position is maximum for the maximum ultimate tensile strength. The influence of filler wire material on the hardness is minimum and welding currentismaximum.Similarlyweldingcurrentontheimpact energyisminimumandweldingpositionismaximum[8].M SSatish(2025)investigatedtheeffectofhardfacingonAISI 1020mildsteel usingSMAWandMIG weldingtechniques with chromium-rich electrodes. findings showed that MIG welding, under controlled parameters, offers better performance in applications requiring high surface durability and wear resistance, while SMAW remains advantageousfordeeperfusionandstructuralbonding[9]. Ade Nurfauziah et al (2023) used ASTM A36 carbon steel thatmaterialwasweldedbymanyvariablesthathavebeen determined and the limitations of the problem during the study.Itwasfoundthatthepolarityandrootgapdistance usedaffectedtheweldingresults,wheretheDCENpolarity at 2 mm root gap showed better welding translucency results.AsfortheresultsofweldingwithDCEPpolarityat3 mmRootgaptheresultsofbetterweldingpenetration.Their studies reveal that the use of different polarities and root gaps results in different welding qualities [10]. Abhishek Singh Gangwar et al (2017) their studies focused on how muchdistortionoccurinlowcarbonsteel(MS)platesand high carbon steel (EN-31) Plates of various cross-sections andthickness.Theystudiedexperimentallyratherthanby usinganysoftware,sothatwecangetmoreeffectivedata. Theamount of distortioncanbecontrolledor minimize if pre-settingtechniquesareappliedthroughweldingfixtures. Studies reveal that it can’t be suggested that what will happen if different types of weld cross section, different typesofplatethickness,anddifferenttypesofplatematerial are used in butt welding joints. Hence further study is necessary.Iftheotherparametersofweldinglikespeedof welding,voltageofwelding,timeofweldingetc.whichwere kept constant in this study work. Hence scope of further workisstillleftwideopen[11].AdeNurfauziahetal(2023) Studied the effect of root gap distance and polarity on defectsinSMAWweldingprocedureThestudyrevealedthat theweldingtranslucencyisaffectedbypolarityandrootgap distance, where the DCEN polarity showed better translucentweldingresultsthanweldingwithDCEPpolarity, eventhoughitwasstillnotinaccordancewiththestandard [12].ShivaniPantetal(2024)EvaluatedWeldingElectrode AngleandRootGapEffectsonJointQuality MS1018andSS 304metallicplates wereconnectedtogetherusingthearc weldingprocess.Twoidenticallysizedplates(110*50*6mm) areweldedtogethertocreateabuttjointasshowninfig-1.
The three most crucial process elements that affect bead shape are the welding. The results showed that while the heat input increased, the tensile strength increased. The hardness was predicted to increase as the current range increased, with the ideal parameters beinghigh hardness, hightensilestrengthforweldatcurrentof110A,Electrode angleof45degree,andRootgapof2mm[13].
RajeevRanjan(2014)OptimizedSMAWprocessesbyusing factorialdesignapproach.Thestudiesrevealthat astrong jointofmildsteel isfoundtobeproducedinthiswork by using the SMAW technique. If amperage is increased, weldingdepositionareagenerallyincreases.Iftravelspeed is increased welding deposition area generally decreases [14].S.H.Zoalfakaretal(2017)studiesfocusedontheeffect ofweldingparametersonmechanicalandmicrostructural propertiesofSt.37/2,St.44/2andSt.52/3jointsproducedby shielded metal arc welding (SMAW) was analyzed in the presentstudy.Differentheatinputs(H)wereappliedtobuttweldingjointsbycontrollingcurrent.Tostudytheeffectof grooveanglesonmechanicalproperties,thespecimenswere machinedwithdifferentgrooveangles40˚,60˚,80˚and100˚. Inordertodeterminetheeffectofweldingprocessonthe localheataffectedzone(HAZ)thermalcycleduringwelding, threedifferentconditionswerechosen,wheretemperatures were recorded by using K-type thermocouples and a data acquisitionsystemcardofUSB6008,NationalInstrument type.Taguchiapproachwasappliedtodeterminethemost influentialcontrolfactorswhichwillyieldbettermechanical propertiesofthejoints,whereTaguchi’stoolssuchassignalto- noise ratio (S/N) have been used to observe the significantparametersandtheoptimalcombinationlevelof SMAW parameters [15]. Abhishek Singh Gangwar et al (2017) focused on, one of the welding defects known as Distortion.Distortionisthechangeinshapeanddifference betweenthepositionsofthetwoplatesbeforeweldingand after welding. Distortion occurs due to good amount of temperaturedifferenceatvariouspointsalongthejointand thusatanyinstantcertainareaofbasemetalexpandsand otherincludingweldbeadcontract.Itwasstudieddownby experimentallyratherthanbyusinganysoftware,sothatto get more effective data. It has been found out the limit of angular distortion for three types of design for different thicknessofplatesi.e.6mm,5mmand4mm.with1200,
International Research Journal of Engineering and Technology (IRJET) e-ISSN: 2395-0056
Volume: 13 Issue: 03 | Mar 2026 www.irjet.net p-ISSN: 2395-0072
900, and 600 Vee. These values of distortion will help the welder before welding to the present job and hence minimizedistortion.But,stillthereislackofinformationof this study. It can’t be suggested that what will happen if differenttypesofweldcrosssection,differenttypesofplate thickness,anddifferenttypesofplatematerialareusedin butt welding joints. Hence further study is necessary. Extensiveresearchhasbeenconductedtostudydistortion behaviorsandprocessoptimizationinSMAW.Thefollowing findingsarediscussedbelow.
2.1 Effect of welding current and heat input
Literature studies reveal that distortion increases with higher welding current and heat input. Increase in plate thickness and current significantly increases longitudinal shrinkage.Higherweldingspeedsreducedistortiondueto lowerheatinput.
2.2 Taguchi based optimization
Taguchiorthogonalarraymethods(L9,L16,L27)havebeen widely applied to determine optimal parameter combinations.Studiesrevealthefollowing:
Weldingspeedsignificantlyinfluencesdistortion.
Currentstronglyaffectstensilestrength.
Grooveangleimpactsangulardistortion.
Electrodediameteraffectsimpactstrength.
Taguchi methods improve robustness and reduce experimentaltrials.
2.3 ANOVA analysis
ANOVAhasbeenusedtodeterminepercentagecontribution ofeachparameter.Researchfindingsindicatethefollowing Weldingcurrentoftenhasthehighestcontributiontoward distortion.Voltagesignificantlyinfluenceswelddeposition area.Weldingspeedplaysamajorroleinangulardistortion control.
2.4 Grey relational and multi objective optimization
Grey-based Taguchi methods have been used for multiresponseoptimizationincluding:
Tensilestrength
Hardness
Impactstrengths
Distortion Thesetechniqueshelpachievebalancedoptimizationrather thansingle-responseimprovement.
2.5 Finite Element Analysis (FEA)
FEA tools such as ANSYS are used to simulate thermal distribution and predict distortion.12% increase in heat
input may cause up to 65% increase in displacement. Increasedweldingspeedreducesstrainanddeformation. Narrowgroovepreparationreducescumulativedistortion.
Table -2: Comparativeanalysisofkeyfindings
Parameter
Influence on Distortion
Research Consensus
WeldingCurrent HighImpact Major contributor
WeldingSpeed InverselyProportional Criticalfactor
GrooveAngle Affectsangulardistortion Moderate influence
RootGap
Electrode
Influencespenetration& shrinkage Moderate
Diameter Affectsheatinput Moderate
WeldingPosition Affectsangulardistortion Significant
Fromtheliteraturereview,thefollowinggapsareidentified limited regression models specifically for distortion prediction in mild steel SMAW. Most studies focus on mechanical strength rather than distortion. Few studies integrateexperimentalvalidationwithstatisticalmodelling. Multithicknessmildsteelplateoptimizationrequiresfurther study.
Basedonliteraturesurvey,thepresentstudyproposes:
Application of Taguchi method for parameter optimization.DesignofExperimentsbasedOA.
Evaluationofdistortionfordifferentmildsteelplate thicknesses.
Identificationofoptimalcurrent,rootgap&electrode anglecombinationsforminimumdeformation.
ANOVAforcontributionanalysis.
Developmentofregressionmodelsfordistortion prediction
This review shows that distortion in SMAW welded mild steelplatesisstronglyinfluencedbyweldingcurrent,heat input, and welding speed. Higher heat input increases angular and longitudinal distortion, whereas optimized travel speed significantly reduces thermal gradients. OptimizationtechniquessuchasTaguchimethod,ANOVA, Grey relational analysis, and FEA have proven effective in minimizing distortion while maintaining mechanical performance. Systematic parameter selection ensures repeatabilityandcostefficiencycomparedtoconventional trialanderrorapproaches.Theliteraturestronglysupports the need for integrated statistical modelling and experimental validation for reliable distortion control in SMAWprocesses.
International Research Journal of Engineering and Technology (IRJET) e-ISSN: 2395-0056
Volume: 13 Issue: 03 | Mar 2026 www.irjet.net p-ISSN: 2395-0072
[1] SanjayKumarGupta,SanjaySingh,(2023)‘Analysisand OptimizationofShieldedMetalArcWeldingParameters on Mechanical Properties of Dissimilar Materials’. InternationalJournalofScientificResearchinScience, EngineeringandTechnology
[2] AneelaWakeel,MuhammadAliNasir,MuhammadAbas, Mohsin Iqbal Qazi, Muhammad Saad Afzal, (2024) ‘Optimizationofprocessparametersforshieldedmetal arc welding for ASTM A 572 grade 50’, Journal of EngineeringResearch13(2025)1072-1088.
[3] KWeerasekralageL.S.,Sisira,M.S.A.Karunaratne,S.D. Pathirana (2019) ‘Optimization of Shielded Metal Arc Welding (SMAW) process for mild steel’, Annual SessionsofIESL,pp.[841-847],2019©TheInstitution ofEngineers,SriLanka.Publication
[4] Esther Titilayo Akinlabi, N Nkosinathi Madushele, Okwudili Simeon Ogbonna, Olawale Samuel Fatoba, StephenAkinlabi,(2023)‘Multi‑responseoptimization of TIG dissimilar welding of AISI 1008 mild steel and AISI 316 stainless steel using grey‑based Taguchi method, The International Journal of Advanced ManufacturingTechnology(2023)
[5] Devendra Singh, Sivakumar (2020) ‘Effect of plate thicknessandcurrentonthelongitudinalshrinkagein mildsteelbuttjoints’,InternationalResearchJournalof EngineeringandTechnology(IRJET)
[6] Mr.GunwantDShelake,Mr.Harshal,K.Chavan,Dr.M.S. Kadam(2012)EffectofHeatInputandSpeedofWelding on Distortion in MIG Welding, (IJIERD), ISSN 0976 –6979.
[7] M. SenthilKumar, P. Bharatha, V.G. Sridharb (2014) ‘Optimization of 316 stainless steel weld joint characteristics using Taguchi technique’ 12th Global congress on manufacturing and management, GCMM 2014,PublishedbyElsevierLtd.
[8] A. Balaram Naik, A. Chennakesava Reddy, S. Raja SrikaranRao(2018)‘TheAnalysisofSMAWparameters foroptimizationofmechanicalpropertiesusingTaguchi method on DSS material’, International Journal for ResearchinAppliedScience&EngineeringTechnology (IJRASET)ISSN:2321-9653
[9] C. T. Jayadeva, K. M. Kenchi Reddy, M S Satish, C. T. Jayadeva,(2025)‘Impactofweldingparametersonthe metallurgicalpropertiesofchromiumbasedhardfacing depositsusingSMAWandMIG’,©2025IJCRT|Volume 13,Issue7July2025|ISSN:2320-2882.
[10]AdeNurfauziah,AnandaYhutoWibisonoPutraNurlela, Topik Hidayat, Wahyu Efendi Manullang, (2023) ‘The
effect of root gap distance and polarity on defects in SMAW welding procedure’, Journal of Welding Technology.Volume5,No.2.
[11]Abhishek Singh Gangwar, Anurag Srivastava, Neha Gupta,Rajan,(2017),‘Experimentalstudyofdistortion in butt welds of mild steel plates and En-31 plates havingdifferentthicknessandweldcrosssections’,IOSR Journal of Mechanical and Civil Engineering (IOSRJMCE)e-ISSN:2278-1684,p-ISSN:2320-334X,Volume 14,Issue3Ver.IV
[12]AdeNurfauziah*,Nurlela,TopikHidayat,WahyuEfendi Manullang,AnandaYhutoWibisonoPutra(2023),‘The effect of root gap distance and polarity on defects in SMAW welding procedure’ , Journal of Welding Technology.Volume5,No.2,December2023
[13]ShivaniPant,LaithJasim,MJMurali,Dr.K.Kavithamani, AnitaGehlot(2024),‘Evaluatingweldingelectrodeangle and root gap effects on joint quality’, E3S Web of Conferences.491ICECS(2024).
[14]Rajeev Ranjan (2014), ‘Parametric optimized SMAW processes by using factorial design approach’ . International Journal of Scientific and Research Publications,Volume4,Issue9,September20141ISSN 2250-3153
[15]S. H. Zoalfakar, A. A. Hassan (2017), ‘Analysis and optimizationofshieldedmetalarcweldingparameters on mechanical properties of carbon steel joints by Taguchi method’, International Journal of Advanced EngineeringandGlobalTechnologyIVol-05,Issue-01, January2017
[16]Abhishek Singh Gangwar, Anurag Srivastava, Neha Gupta and Rajan (2017), ‘Experimental study of distortioninbuttweldsofmildsteelplatesandEn-31 plates having different thickness and weld cross sections’ , IOSR Journal of Mechanical and Civil Engineering (IOSR-JMCE) e-ISSN: 2278-1684, p-ISSN: 2320-334X, Volume 14, Issue 3 Ver. IV. (May – June 2017),PP51-80
International Research Journal of Engineering and Technology (IRJET) e-ISSN: 2395-0056
Volume: 13 Issue: 03 | Mar 2026 www.irjet.net p-ISSN: 2395-0072
Manjunatha N S is a postgraduate student in the department of Mechanical Engineering at ACE Hosur. My research focuses on welding technology. Currently, workingonSMAW
Dr. S. Shylin H Jose is associate professor in the department of Mechanical Engineering at ACE Hosur. 18+ years of teaching experience. Currently guiding studentstogetdegreesandenhance technicalskills.
Dr. B S Praveen Kumar isprofessor in the department of Mechanical Engineering at GEC Kushalnagara. 20+ years of teaching experience. Weldingtechnologyistheinterested field of study. Currently guiding studentstogetdegreesandenhance technicalskills.