Note: Use Bookmarks panel to navigate
Product: INTEGRATED TOOLCARRIER
Model: IT12 INTEGRATED TOOLCARRIER 4NC
Configuration: IT12 INTEGRATED TOOLCARRIER 4NC00001-UP (MACHINE) POWERED BY 3204 ENGINE
Disassembly and Assembly
3204 VEHICULAR ENGINES
Media Number -SENR3230-00
Piston Cooling Orifices
SMCS - 1307-010
Publication Date -01/10/1985
Date Updated -06/05/2020
SENR32300025
Remove And Install Piston Cooling Orifices
START BY:
a. remove crankshaft and gear
NOTE: The piston cooling orifices are installed in the No. 2 and 4 main bearing bosses in the cylinder block. See illustration B18488P1 on Page 90. A replacement is necessary only if they are damaged. Normally it will only be necessary to be sure the orifices are clean.
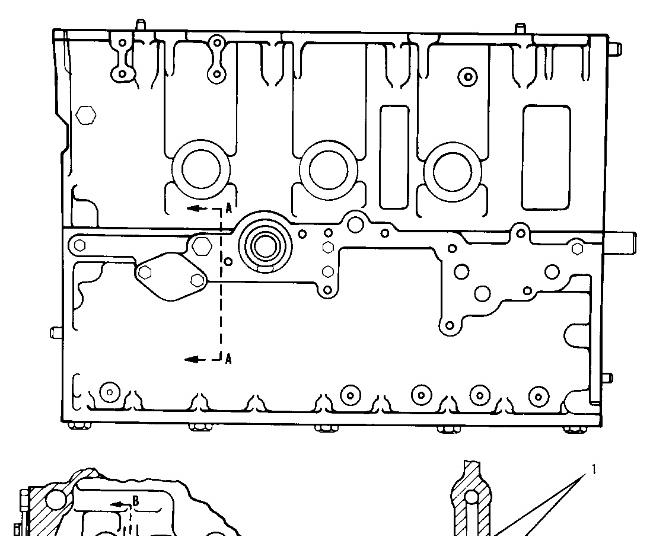
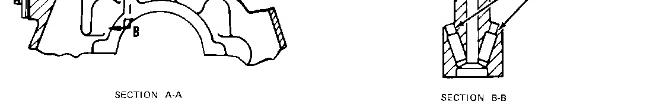
1. Use a soft punch to remove four orifices (1) from the cylinder block.
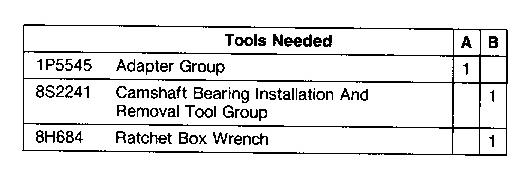
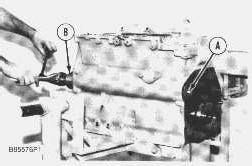
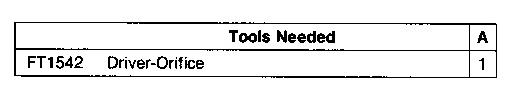
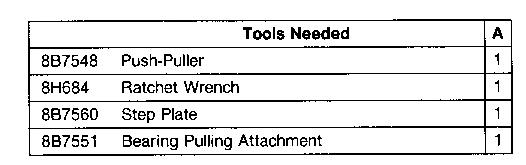
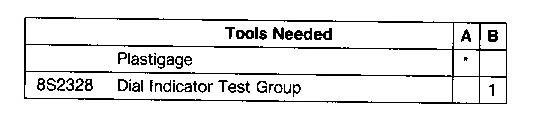
2. Use tool (A) to install the orifices in main bearing bosses No. 2 and 4 until they are against the counterbore. Be sure the orifices are open after they are installed.
END BY:
a. install crankshaft and gear Copyright 1993 - 2024 Caterpillar Inc. All Rights Reserved.
Network For SIS Licensees. Wed Feb 28 23:01:14 UTC+0530 2024
This is the sample of the manual click on the download link for complete manual
DOWNLOAD LINK
For some reason if link does not work download this pdf and then click
Product: INTEGRATED TOOLCARRIER
Model: IT12 INTEGRATED TOOLCARRIER 4NC
Configuration: IT12 INTEGRATED TOOLCARRIER 4NC00001-UP (MACHINE) POWERED BY 3204 ENGINE
Disassembly and Assembly
3204 VEHICULAR ENGINES
Media Number -SENR3230-00
Crankshaft And Gear
SMCS - 1202; 1204-011; 1204-012
Publication Date -01/10/1985
Date Updated -06/05/2020
SENR32300024
Remove Crankshaft And Gear
START BY:
a. remove timing gear cover
b. remove flywheel housing
c. remove pistons and connecting rods
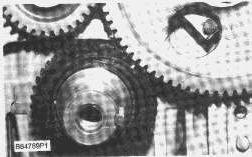
1. Turn the crankshaft until the "C" mark on the crankshaft drive gear is in alignment with the "C" mark on the camshaft drive gear as shown.
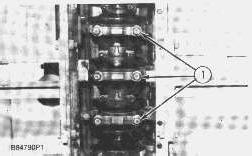
2. Remove the three center main bearing caps (1).
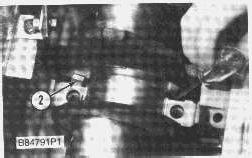
3. Remove thrust bearings (2) from each side of the center crankshaft journal.
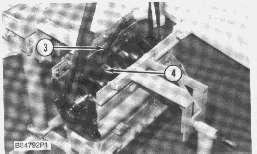
4. Remove bolt (3). Remove the oil pickup tube support strip and the clip from the cylinder block as a unit.
5. Install one of the flywheel bolts in the end of the crankshaft.
6. Fasten a nylon strap and a hoist on crankshaft (4) as shown.
7. Remove the two end caps.
NOTICE
Be careful not to damage the crankshaft journals when the crankshaft is removed.
8. Remove crankshaft (4) from the cylinder block. The weight of the crankshaft is 52 kg (115 lb.).
NOTICE
If new main bearings are not to be installed during crankshaft installation, put identification marks on the original bearings as to their location in the engine.
9. Remove the crankshaft main bearings from the cylinder block and from the main bearing cap.
10. Check the condition of the main bearings and crankshaft. Make reference to Guideline For Reusable Parts: Main And Connecting Rod Bearings, Form No. SEBF8009 and Visual Inspection Of Crankshafts, Form No. SEBF8043.
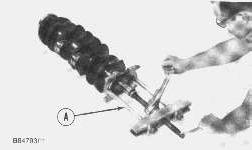
11. Use tooling (A), and remove the drive gear from the crankshaft.
Install Crankshaft And Gear
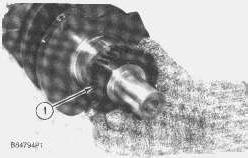
1. Heat the crankshaft drive gear to a maximum temperature of 315° (600°F). Install drive gear (1) on the crankshaft with the "C" mark on the gear toward the pulley end of the crankshaft.
If the crankshaft journals and bores for the block and rods were measured at disassembly and found to be within specifications, no further checks are necessary. However, if the serviceman still wants to measure the bearing clearances, Plastigage is recommended. Lead wire, shim stock or use of a dial bore gauge can damage the bearing surface.
The serviceman must be very careful to use Plastigage correctly. The following points must be remembered:
...Make sure that the backs of the bearings and the bores are clean and dry.
...Make sure that the bearing locking tabs are properly seated in their slots.
...The crankshaft must be free of oil where the Plastigage touches it.
...If the main bearing clearances are checked with the engine upright or on its side, the crankshaft will have to be lifted up with a force equal to the weight of the crankshaft and held against the crown of the bearing. If the crankshaft is not supported, the weight of the crankshaft will cause incorrect readings.
...Put a piece of Plastigage on the crown of the bearing half that is in the cap. Do not allow the Plastigage to extend over the edge of the bearing.
...Install the bearing cap using the correct torque-turn specifications. Do not use an impact wrench. Be careful not to dislodge the bearing when the cap is installed.
...Do not turn the crankshaft with the Plastigage installed.
...Carefully remove the cap, but do not remove the Plastigage. Measure the width of the Plastigage while it is in the bearing cap or on the crankshaft journal. Do this by using the correct scale on the package. Record the measurements.
...Remove the Plastigage before installing the cap.
When using Plastigage, the readings can sometimes be unclear. For example, all parts of the Plastigage are not the same width. Measure the major widths to make sure that they are within the specification range. Also, experience has shown that when checking clearances tighter than 0.10 mm (.004") the readings may be low by 0.013 to 0.025 mm (.0005 to .0010"). Out-of-round journals can give faulty readings. Also, journal taper may be indicated when one end of the Plastigage is wider than the other.
NOTE: For complete details concerning measuring bearing clearances, see Engine Bearings And Crankshafts, Form No. SEBD0531.
NOTICE
Make sure the upper and lower halves of the main bearings are installed so the bearing tabs fit into the notch in the cylinder block and main bearing caps.
2. If the bearings were removed from the engine, clean the bearing surfaces in the cylinder block for the main bearings. Install the upper main bearing halves (bearings with the oil hole) in the cylinder block.
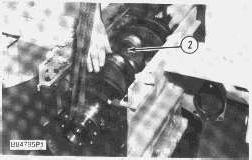
3. Fasten a nylon strap and a hoist on crankshaft (2), and put it in position in the cylinder block with the "C" marks on the camshaft drive gear and crankshaft drive gear in alignment.
NOTE: Install the bearings dry when the clearance checks are made. Put clean engine oil on all of the bearings for final assembly.
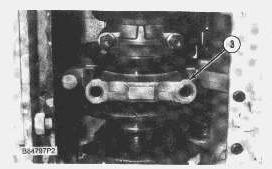
4. Check the main bearing clearances with Plastigage (A) as follows:
a. Put a piece of Plastigage (A) between the crankshaft and the main bearing.
NOTICE
Make sure the part number on the main bearing cap is toward the front of the engine and the number on the main bearing cap is the same as the number on the cylinder block on the left side of each main bearing cap.
NOTE: Do not turn the crankshaft when Plastigage (A) is in position.
b. Install main bearing cap (3). Put 2P2506 Thread Lubricant on the bolt threads and the contact surfaces of the bolt heads. Install the bolts. Tighten the bolts on the side where the main bearing tabs are located, to a torque of 61 ± 6 N*m (45 ± 4 lb.ft.). Tighten the bolts on the opposite side to a torque of 61 ± 6 N*m (45 ± 4 lb.ft.).
c. Put a mark on each bolt head and the bearing caps. Turn the bolts that are opposite the main bearing tabs an extra 60° ± 5° from the mark. Turn the bolts on the side where the main bearing tabs are located an extra 60° ± 5° from the mark.
d. Remove main bearing caps (3), and measure the Plastigage. This will determine the bearing clearance. The main bearing clearance with a new bearing must be 0.076 to 0.168 mm (.0030 to .0066 in.). The maximum permissible clearance with used main bearings is 0.18 mm (.007 in.).
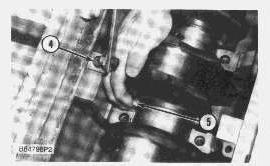
5. Put clean engine oil on thrust bearings (5) for the No. 3 main bearing saddle. Install a thrust bearing on each side of No. 3 main bearing saddle with the identification "BLOCK SIDE" toward the bearing saddle and the side with the oil grooves toward the crankshaft.
6. Install main bearing caps (3), and tighten the bolts as in steps 4b and 4c.
7. Put the clip and oil pickup tube support strip in position on the cylinder block as a unit, and install bolt (4) that holds them in place.
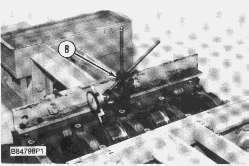
8. Check the end play of the crankshaft with tool (B). Be sure the dial indicator is against a machined surface. The end play is controlled by the thrust bearings on each side of No. 3 center main bearing. The end play with new bearings must be 0.064 to 0.480 mm (.0025 to .0189 in.). The maximum permissible end play with used bearings is 0.64 mm (.025 in.). Make a replacement of the thrust bearings if needed.
END BY:
a. install pistons and connecting rods
b. install flywheel housing
c. install timing gear cover
Product: INTEGRATED TOOLCARRIER
Model: IT12 INTEGRATED TOOLCARRIER 4NC
Configuration: IT12 INTEGRATED TOOLCARRIER 4NC00001-UP (MACHINE) POWERED BY 3204 ENGINE
Disassembly and Assembly
3204 VEHICULAR ENGINES
Media Number -SENR3230-00
Publication Date -01/10/1985
Crankshaft Rear Seal and Wear Sleeve
SMCS - 1161-012; 1161-011
Remove Crankshaft
Date Updated -06/05/2020
SENR32300023
Rear Seal And Wear Sleeve
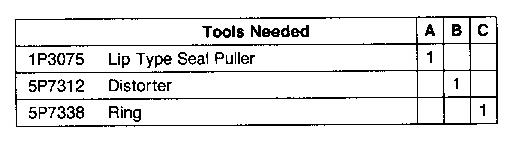
START BY:
a. remove flywheel
NOTE: Whenever the crankshaft seal is removed from the wear sleeve, a new Wear Sleeve and Seal Group must be installed as a set. If the seal is put back on the wear sleeve, the seal can be damaged.
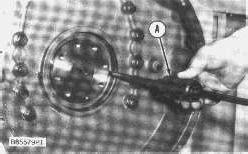
1. Remove the crankshaft rear seal with tool (A).
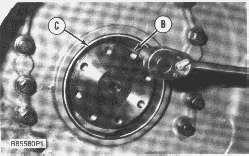
2. Install tool (C) in the rear seal bore.
3. Install tool (B) between tool (C) and the wear sleeve. Turn tool (B) until the edge of the tool makes a flat place (crease) in the wear sleeve. Do this in two or more places until the wear sleeve is loose.
4. Remove tool (C) and the wear sleeve by hand.
Install Crankshaft Rear Seal And Wear Sleeve
NOTICE
If the crankshaft rear seal and wear sleeve come apart during installation, the seal and wear sleeve become scrap. A new seal and wear sleeve must be installed as a set.
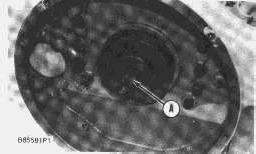
NOTE: The correct lubricant is on the new wear sleeve and seal group and no additional lubricant is necessary.
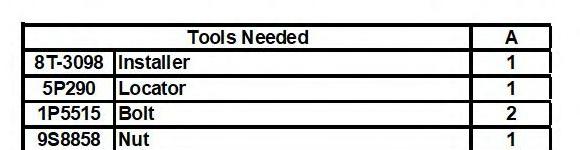
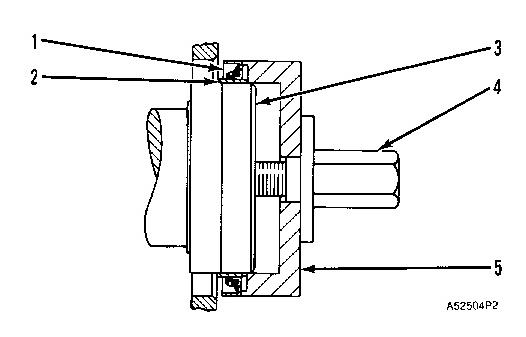
1. Install the crankshaft rear seal and wear sleeve with tooling (A) as follows:
a. Clean and prepare the crankshaft outside diameter with 6V1541 Quick Cure Primer. Apply 9S3265 Retaining Compound to the crankshaft outside diameter.
b. Install locator (3) and the bolts on the rear of the crankshaft.
c. Put wear sleeve (2) and seal (1) as a unit on locator (3) with the lip of the seal toward the front of the engine.
d. Put installer (5) in position on the locator.
e. Put clean engine oil on the face of nut (4), and install it on the locator. Tighten the nut until installer (5) makes contact with locator (3). Remove tooling (A).
END BY:
a. install flywheel
Product: INTEGRATED TOOLCARRIER
Model: IT12 INTEGRATED TOOLCARRIER 4NC
Configuration: IT12 INTEGRATED TOOLCARRIER 4NC00001-UP (MACHINE) POWERED BY 3204 ENGINE
Disassembly and Assembly
3204 VEHICULAR ENGINES
Media Number -SENR3230-00
Flywheel Housing
SMCS - 1157-012; 1157-011
Publication Date -01/10/1985
Date Updated -06/05/2020
SENR32300022
Remove Flywheel Housing
START BY:
a. remove flywheel
b. remove oil pan
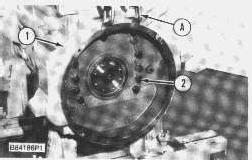
1. Remove the starter from the engine.
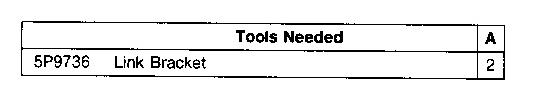
2. Fasten tooling (A) and a hoist to the flywheel housing as shown.
NOTICE
Be careful not to damage the crankshaft rear seal when flywheel housing (1) is removed.
3. Remove bolts (2) and the washers that hold the flywheel housing to the cylinder block.
4. Remove flywheel housing (1) and the gasket. The weight of the flywheel housing is 39 kg (85 lb.).
Install Flywheel Housing
1. Clean the old gasket from the surfaces of the cylinder block and flywheel housing that make contact with each other. Install a new gasket on the cylinder block.
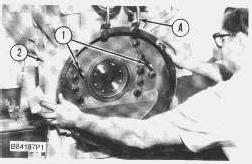
2. Install two 7/16"-14 NC × 7 in. (178 mm) long guide bolts (1) in the cylinder block as shown.
3. Put clean engine oil on the crankshaft rear wear sleeve and on the lip of the seal.
NOTICE
Be careful not to damage the crankshaft rear seal when flywheel housing (2) is installed.
4. Fasten tooling (A) and a hoist to flywheel housing (2) as shown. Put the flywheel housing in position on the cylinder block, and install the bolts that hold it. Tighten the bolts to a torque of 90 ± 15 N·m (65 ± 11 lb.ft.).
5. Cut the bottom of the gasket even with the flywheel housing and cylinder block. Put 5H2471 Gasket Cement on the bottom of the gasket where the gasket makes contact with the oil pan gasket.
6. Install the starter on the engine.
END BY:
a. install oil pan
b. install flywheel
Copyright 1993 - 2024 Caterpillar Inc.
Rights Reserved.
Network For SIS Licensees. Wed Feb 28 23:00:45 UTC+0530 2024
Product: INTEGRATED TOOLCARRIER
Model: IT12 INTEGRATED TOOLCARRIER 4NC
Configuration: IT12 INTEGRATED TOOLCARRIER 4NC00001-UP (MACHINE) POWERED BY 3204 ENGINE
Disassembly and Assembly
3204 VEHICULAR ENGINES
Media Number -SENR3230-00
Flywheel
SMCS - 1156-012; 1156-011
Remove Flywheel
Publication Date -01/10/1985
Date Updated -06/05/2020
SENR32300021
START BY:
a. remove engine
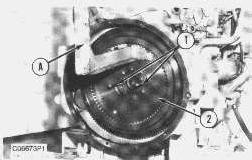
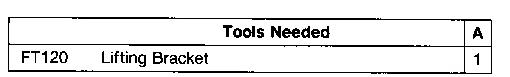
1. Put tooling (A) in position on the flywheel with the end of the tool engaged in the groove of the flywheel as shown.
2. Remove two of the bolts, opposite each other, that hold the flywheel to the crankshaft. Install two 7/16"-20 NF × 7 in. (178 mm) long guide bolts (1) in the crankshaft.
3. Remove the remainder of the bolts, and remove flywheel (2) from the crankshaft. The weight of the flywheel is 27 kg (60 lb.).
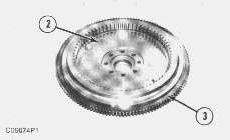
4. Remove ring gear (3) from flywheel (2) with a punch and hammer.
Install Flywheel
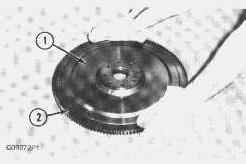
1. Heat ring gear (2) to a maximum temperature of 204°C (400°F). Install the ring gear on flywheel (1) with the part number toward the engine when the flywheel is installed.
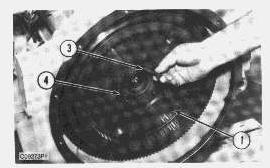
2. Install two 7/16"-20 NF × 7 in. (178 mm) guide bolts opposite each other in the end of the crankshaft.
NOTICE
When a new flywheel is installed, check the thickness of the new flywheel at the bolt holes in relation to the thickness of the old flywheel. Install the correct length bolts so they will be fully engaged in the
crankshaft flange. Bolts that are too long will make contact with the block on the back side of the crankshaft flange and pull the crankshaft back. This will cause the crankshaft thrust bearing to fail.
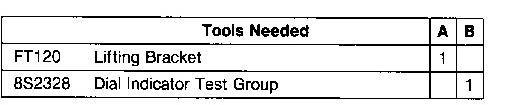
3. Put tooling (A) in position on the flywheel with the end of lifting bracket engaged in the groove of the flywheel as shown. Put flywheel (1) in position on the guide bolts, and make sure offset hole (4) in the flywheel (identified by dash mark) and the mark on the end of the crankshaft are in alignment.
NOTICE
Make sure the correct sealant is put on the bolt threads. The holes for the bolts in the crankshaft flange are drilled through so the holes are open to the oil in the engine. Leakage along the bolt threads can be the result if the correct sealant is not used.
4. Put 9S3263 Thread Lock on the bolt threads, and install all but two of the bolts in the flywheel. Remove tooling (A) and the guide bolts. Install the remainder of bolts (3) in the flywheel. Tighten the bolts to a torque of 75 ± 8 N·m (55 ± 6 lb.ft.).
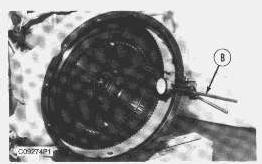
5. Use tooling (B) to measure the face runout and bore runout of the flywheel. The face runout and bore runout must not be greater than 0.15 mm (.006 in.) total indicator reading. See Specifications for the correct procedure to measure the face runout and bore runout of the flywheel.
END BY:
a. install engine Copyright 1993 - 2024 Caterpillar Inc. All Rights Reserved. Private Network For SIS Licensees.
Product: INTEGRATED TOOLCARRIER
Model: IT12 INTEGRATED TOOLCARRIER 4NC
Configuration: IT12 INTEGRATED TOOLCARRIER 4NC00001-UP (MACHINE) POWERED BY 3204 ENGINE
Disassembly and Assembly
3204 VEHICULAR ENGINES
Media Number -SENR3230-00
Publication Date -01/10/1985
Crankshaft Main Bearings
SMCS - 1203-010
Date Updated -06/05/2020
SENR32300020
Remove And Install Crankshaft Main Bearings
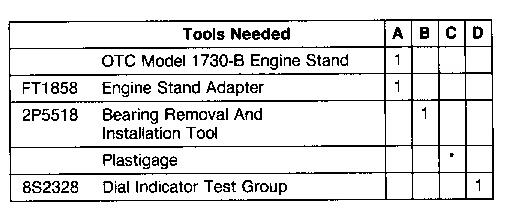
START BY:
a. remove oil pan
1. Put the engine on tooling (A).
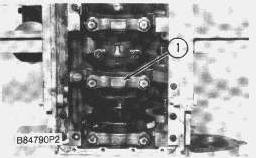
2. Remove the bolts that hold main bearing cap (1). Remove main bearing cap (1) and the lower half of the main bearing.
3. Remove the bearing from the cap.
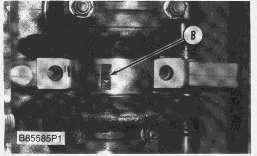
NOTICE
If the crankshaft is turned in the wrong direction, the tab of the bearing will be pushed between the crankshaft and cylinder block. This can cause damage to either or both.
NOTE: The center and two end main journals have no oil hole. To remove these bearings, put a thin piece of soft material that will not damage the crankshaft journal against the end of the bearing opposite the tab. Hit the bearing with the soft material until the tab of the bearing is free from the groove in the cylinder block. Remove the upper half of the main bearing.
4. Remove the upper half of the other main bearings as follows:
a. Turn the crankshaft until tool (B) can be installed in the crankshaft journal. Install tool (B).
b. Turn the crankshaft in the direction which will push the upper main bearing out, tab end first.
c. Check the condition of the bearings. (See Guideline For Reusable Parts, Main And Connecting Rod Bearings, Form No. SEBF8009.)
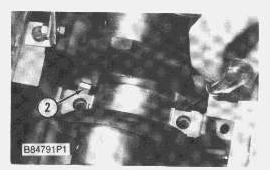
5. Remove crankshaft thrust bearings (2) from each side of the No. 3 main bearing saddle.
NOTE: Install the main bearings dry when the clearance checks are made. Put clean engine oil on the main bearings for final assembly. Also, be sure the tabs on the back side of the main bearings fit in the grooves of the main bearing caps and cylinder block.
6. Clean the surfaces in the cylinder block for the main bearings. Use tool (B), and install new upper halves of main bearings (bearings with the oil hole) in the cylinder block. Do not put oil on the bearing.
7. Clean the surfaces of the main bearing caps for the main bearings. Install the new lower halves of the main bearings in the main caps without oil.
The serviceman must be very careful to use Plastigage correctly. The following points must be remembered:
...Make sure that the backs of the bearings and the bores are clean and dry.
...Make sure that the bearing locking tabs are properly seated in their slots.
...The crankshaft must be free of oil where the Plastigage touches it.
...If the main bearing clearances are checked with the engine upright or on its side, the crankshaft must be supported. Use a jack under an adjacent crankshaft counterweight and hold the crankshaft against the crown of the bearing. If the crankshaft is not supported, the weight of the crankshaft will cause incorrect readings.
...Put a piece of Plastigage on the crown of the bearing half that is in the cap. Do not allow the Plastigage to extend over the edge of the bearing.
...Install the bearing cap using the correct torque-turn specifications. Do not use an impact wrench. Be careful not to dislodge the bearing when the cap is installed.
...Do not turn the crankshaft with the Plastigage installed.
...Carefully remove the cap, but do not remove the Plastigage. Measure the width of the Plastigage while it is in the bearing cap or on the crankshaft journal. Do this by using the correct scale on the package. Record the measurements.
...Remove the Plastigage before installing the cap.
When using Plastigage, the readings can sometimes be unclear. For example, all parts of the Plastigage are not the same width. Measure the major widths to make sure that they are within the specification range. Also, experience has shown that when checking clearances tighter than 0.10 mm (.004") the readings may be low by 0.013 to 0.025 mm (.0005 to .0010"). Out-of-round journals can give faulty readings. Also, journal taper may be indicated when one end of the Plastigage is wider than the other.
For complete details concerning measuring bearing clearances, see Engine Bearings And Crankshafts, Form No. SEBD0531.
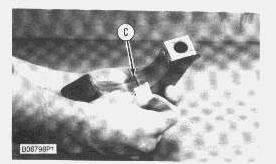
8. Check the main bearing clearance with Plastigage (C) as follows:
a. Put a piece of Plastigage (C) on the crown of the bearing half that is in the cap or on the crankshaft journal as shown.
NOTICE
Make sure the part number on the main bearing caps is toward the front of the engine and the number on the main bearing caps is the same as the number on the outside (camshaft side) of the cylinder block.
b. Put main bearing caps (1) in position on the cylinder block. Put 2P2506 Thread Lubricant on the bolt threads and the contact surfaces of the bolt heads, and install the bolts. Tighten the bolts on the side where the main bearing tabs are located to a torque of 61 ± 6 N·m (45 ± 4 lb.ft.). Tighten the bolts on the opposite side to a torque of 61 ± 6 N·m (45 ± 4 lb.ft.).
c. Put a mark on each bolt head and the bearing caps. Turn the bolts that are opposite the main bearing tabs an extra 60° ± 5° from the mark. Turn the bolts on the side where the main bearing tabs are located an extra 60° ± 5° from the mark.
d. Remove main bearing caps (1), and measure the Plastigage. This will determine the bearing clearance. The main bearing clearance with a new bearing must be 0.076 to 0.168 mm (.0030 to .0066 in.). The maximum permissible clearance with used main bearings is 0.18 mm (.007 in.).
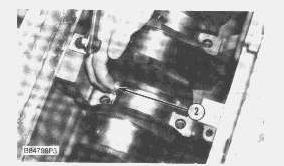
9. Put clean engine oil on thrust bearings (2) from the No. 3 main bearing saddle. Install a thrust bearing on each side of No. 3 main bearing saddle with the identification "BLOCK SIDE" toward the bearing saddle and the side with the oil grooves toward the crankshaft.
10. Install main bearing caps (1), and tighten the bolts as in Steps 8b and 8c.
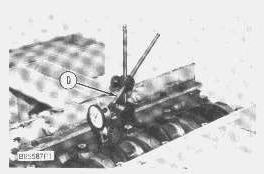
11. Check the end play of the crankshaft with tool (D). Be sure the dial indicator is against a machined surface. The end play is controlled by the thrust bearings on each side of No. 3 center main bearing. The end play with new bearings must be 0.064 to 0.480 mm (.0025 to .0189 in.). The maximum permissible end play with used bearings is 0.64 mm (.025 in.). Make a replacement of the thrust bearings if needed.
END BY:
a. install oil pan
Copyright 1993 - 2024 Caterpillar Inc. All Rights Reserved. Private Network For SIS Licensees.
Wed Feb 28 23:00:23 UTC+0530 2024
Product: INTEGRATED TOOLCARRIER
Model: IT12 INTEGRATED TOOLCARRIER 4NC
Configuration: IT12 INTEGRATED TOOLCARRIER 4NC00001-UP (MACHINE) POWERED BY 3204 ENGINE
Disassembly and Assembly
3204 VEHICULAR ENGINES
Media Number -SENR3230-00
Camshaft Bearings
SMCS - 1211-012; 1211-011
Publication Date -01/10/1985
Date Updated -06/05/2020
SENR32300019
Remove Camshaft Bearings
START BY:
a. remove camshaft
b. remove timing gears and plate
c. remove flywheel housing
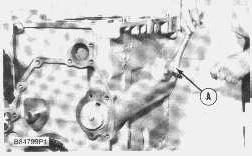
NOTE: The camshaft bearings may be pulled toward the inside or the outside of the cylinder block for removal.
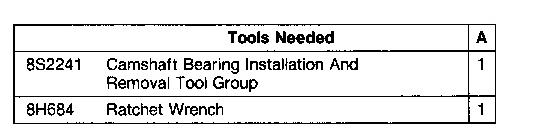
1. Use tooling (A), and remove the rear camshaft bearing.
2. Remove the remainder of the camshaft bearings with tool (A).