
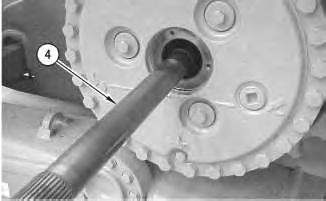
Illustration 7
g00871057
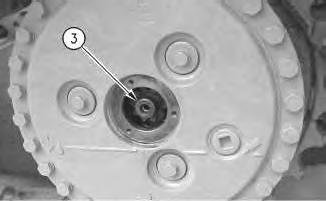
Illustration 8
g00871054
2. Use Tooling (A) to install inner axle (4) and outer axle (3).
Note: This machine has two axles on the left side of the machine and one axle on the right side of the machine.
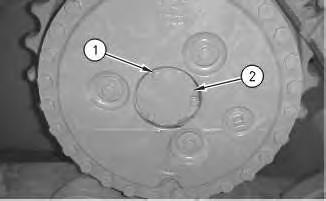
Illustration 9
3. Install cover (2) and bolts (1).
g00870292
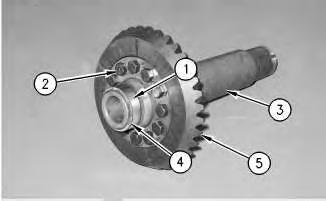
Illustration 1
g00504759
1. Put bevel gear (5) in position on bevel gear shaft (3). Install bolts (2) and the nuts.
2. Install Tooling (H). Use a pry bar to hold bevel gear (5) and shaft (3). Tighten bolts (2) to a torque of 475 ± 60 N·m (350 ± 44 lb ft).
3. Raise bearing race (1) to a maximum temperature of 135°C (275°F). Install the bearing race (1) on the bevel gear shaft.
4. Use Tooling (A) and install retaining ring (4) on bevel gear shaft (3).
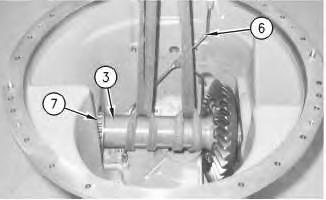
Illustration 2
g00504761
5. Install tube assemblies (6) in the bevel gear case.
6. Use a suitable lifting device to put the bevel gear and shaft (3) in position in the bevel gear case.
7. Put bearing cone (7) in position on the bevel gear shaft.
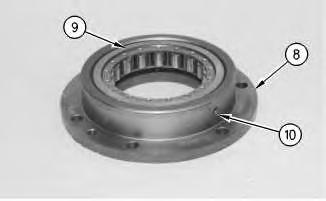
Illustration 3
8. Align the dowel hole in the race and the roller assembly (9) with the hole in cage (8) and install the bearing in the cage. Install dowel (10) in the cage that holds the bearing in place.
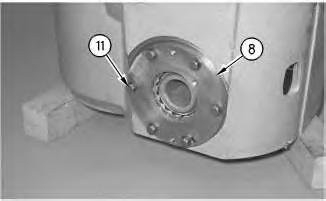
Illustration 4
g00504844
9. Position cage (8) on the bevel gear case and install bolts (11). Tighten the bolts to a torque of 135 ± 20 N·m (100 ± 15 lb ft).
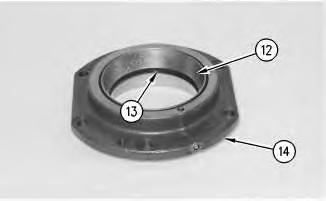
Illustration 5
g00504847
10. Lower the temperature of two bearing cups (12). Install the bearing cups with center ring (13) in cage (14).
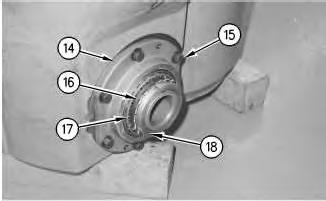
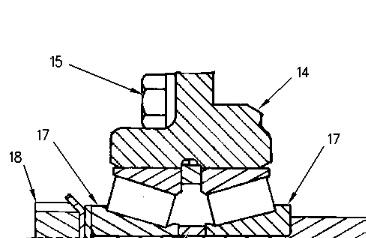
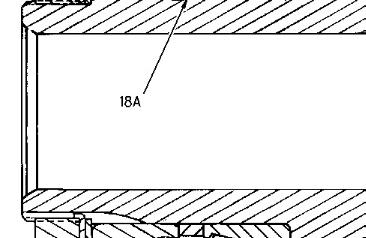
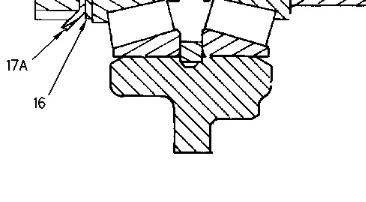
19. Raise bearing (21) to a maximum temperature of 135°C (275°F) and install the bearing on the pinion shaft. Use a 0.03 mm (0.001 inch) feeler gauge to make sure that the bearing is seated against shoulder (23) of the pinion.
10
g01206661
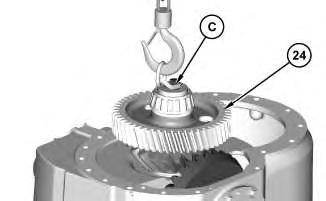
20. Install Tooling (C) on the pinion and attach a suitable lifting device. Lower the pinion and pinion gear assembly (24) into position in the bevel gear case.
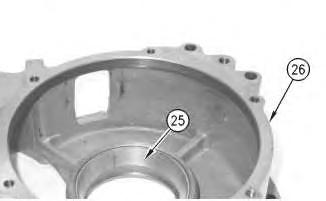
Illustration 11
g00504854
21. Lower the temperature of bearing cup (25) and install the bearing cup in transfer gear case (26).
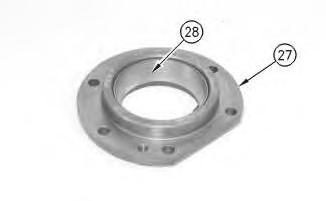
Illustration 12
g00504856
22. Lower the temperature of bearing cup (28) and install the bearing cup in cage (27).
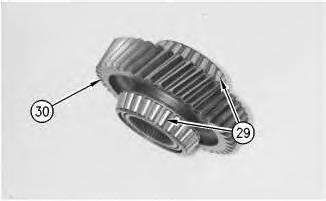
Illustration 13
g00504855
23. Raise bearing cones (29) to a maximum temperature of 135°C (275°F). Install the bearing cones on lower transfer gear (30). Use a 0.03 mm (0.001 inch) feeler gauge to make sure that the bearings are seated against shoulders on the transfer gear.
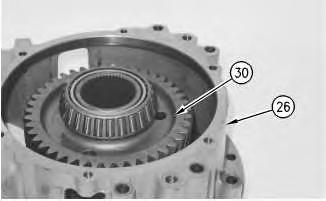
Illustration 14
g00504857
24. Put lower transfer gear (30) in position in transfer gear case (26).
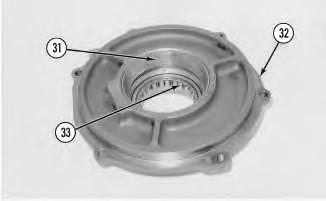
Illustration 15
g00504859
25. Use Tooling (D) and install bearing (33) in cage (32).
26. Lower the temperature of bearing cup (31) and install the bearing cup in cage (32).
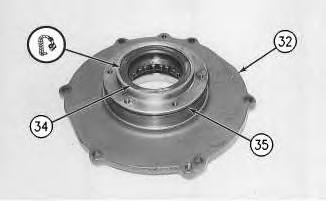
Illustration 16
g00830731
27. Put Tooling (M) in the seal bore of cage (32). Use Tooling (D) and install lip seal (34) in cage (32). Put clean oil on the lip of the seal.
28. Put glycerin on O-ring seal (35) and install the seal in the cage.
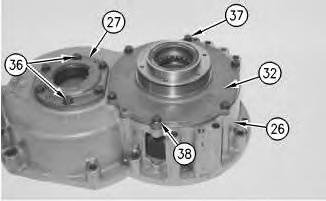
Illustration 17
g00504861
29. Leave out the shims and put cage (27) in position on transfer gear case (26). Install two bolts (36). Space the bolts at 180 degrees. Do not tighten the bolts.
30. Leave out the shims and put cage (32) in position on transfer gear case (26). Install bolts (37) and (38). Space the bolts at 180 degrees. Do not tighten the bolts.
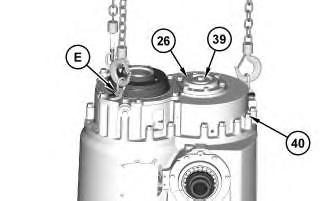
Illustration 18
g01206662
31. Install Tooling (E) on transfer gear case (26) and attach a suitable lifting device.
32. Install the retainer and bolt (39). Tighten bolt (39) to a torque of 270 ± 40 N·m (200 ± 30 lb ft).
NOTICE
Be sure that bolts (36), (37), and (38) that hold cages (27) and (32) in place on the transfer gear case are loose.
33. Put transfer gear case (26) in position on the bevel gear case. Install bolts (40) and washers. Tighten the bolts to a torque of 270 ± 40 N·m (200 ± 30 lb ft).
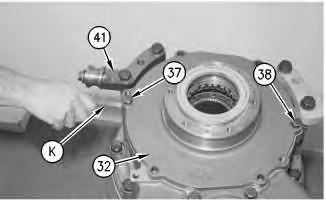
Illustration 19
g00843410
34. Use the following Steps to adjust the end play for the lower transfer gear:
a. In order to seat the bearings, rotate the transfer gear at least three revolutions. Then, tighten bolts (37) and (38) evenly to a torque of 2.25 N·m (20 lb in).
b. Then, rotate the transfer gear at least three revolutions. Tighten bolts (37) and (38) evenly to a torque of 4.5 N·m (40 lb in).
c. Use Tooling (K) to measure the gap between cage (32) and the transfer gear case. Make the measurement at the edge of the cage in line with the center of bolts (37) and (38). Average the two measurements.
d. Add 0.23 mm (0.009 inch) to the average figure that was obtained in Step 34.c. This figure will be the correct thickness for the shims that should be used.
35. Remove cage (32). Put the correct thickness of shims in position on the transfer gear case. Put cage (32) in position and install the bolts that hold the cage in place. Tighten the bolts to a torque of 135 ± 20 N·m (100 ± 15 lb ft). The bearing end play will be 0.10 ± 0.05 mm (0.004 ± 0.002 inch). It will not be necessary to check the bearing end play if this procedure for adjustment has been followed. If a measurement of the bearing end play is desired, refer to “Measurement of the Bearing End Play for the Bevel Pinion and Transfer Gears” in this section.
36. Put two roller bracket (41) in position and install the bolts that hold each one. Tighten the bolts to a torque of 270 ± 40 N·m (200 ± 30 lb ft).
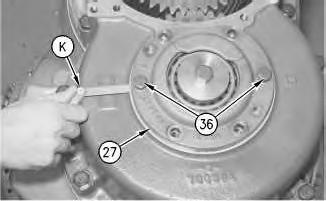
37. Use the following Steps to adjust the end play for the upper transfer and pinion gear:
a. In order to seat the bearings, rotate the transfer gear at least three revolutions. Then, tighten bolts (36) evenly to a torque of 4.5 N·m (40 lb in).
b. Then, rotate the transfer gear at least three revolutions. Tighten bolts (36) evenly to a torque of 9.0 N·m (80 lb in).
c. Use Tooling (K) to measure the gap between cage (27) and the transfer gear case. Make the measurement at the edge of the cage in line with the center of bolts (36). Average the two measurements.
d. Add 0.43 mm (0.017 inch) to the average figure that was obtained in Step 37.c. This figure will be the correct thickness for the shims that should be used.
38. Remove cage (27). Put the correct thickness of shims in position on the transfer gear case. Put cage (27) in position and install the bolts that hold the cage in place. Tighten the bolts to a torque of 135 ± 20 N·m (100 ± 15 lb ft). The bearing end play will be 0.10 ± 0.05 mm (0.004 ± 0.002 inch). It will not be necessary to check the bearing end play if this procedure for adjustment has been followed. If a measurement of the bearing end play is desired, refer
to “Measurement of the Bearing End Play for the Bevel Pinion and Transfer Gears” in this section.
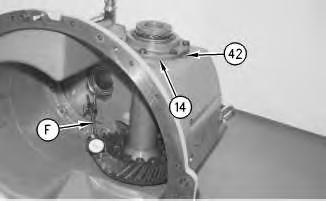
Illustration 21
g00504885
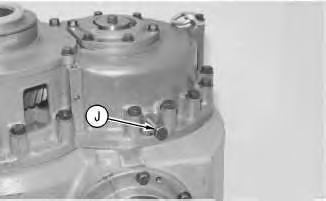
Illustration 22
g00839501
39. Put the bevel gear case on the side so that the bevel gear shaft is in a vertical position with the bevel gear at the bottom.
NOTICE
It is important for the bevel gear case to be in this position. The bevel gear must be held as far away from the pinion gear as possible when the gear clearance (backlash) is set.
40. Install Tooling (J) in the transfer gear case. Tighten Tooling (J) until there is no movement in the pinion gear. Be sure that Tooling (J) is between the teeth of the gear.
41. Put Tooling (F) in position and check the clearance (backlash) between the bevel gear and that are evenly spaced around the gear.
42. The difference between the high measurement and the low measurement must not be more than 0.15 mm (0.006 inch).
43. Install the correct amount of shims (42) under bearing cage (14). Install the six bolts in the cage and tighten the bolts to a torque of 135 ± 20 N·m (100 ± 15 lb ft).
44. Check the gear clearance (backlash) in order to be certain that the clearance is still correct. If the clearance is not correct, add or remove shims (42), as needed.
NOTICE
Tooling (J) must be removed.
45. Remove Tooling (J) from the transfer gear case.
End By:
a. Connect the transmission and the bevel gears.
Measurement of the Bearing End Play for the Bevel Pinion and Transfer Gears
2 Tooling Setup
The bearing end play for the bevel pinion and transfer gears should be adjusted according to the procedure that is given in “Bevel and Transfer Gears - Assemble”. If this procedure is used, the bearing end play (backlash) should be correctly set at 0.10 ± 0.05 mm (0.004 ± 0.002 inch).
NOTICE
It is very important to load the bearings vertically in both the upward direction and the downward direction when you make the measurements. Otherwise, false readings will result.
If a check of bearing end play is desired, the measurement must be made only while the bearings are being rotated and loaded with the Tooling that is shown.
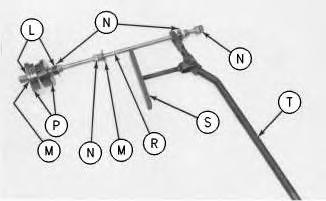
Illustration 23
g00843736
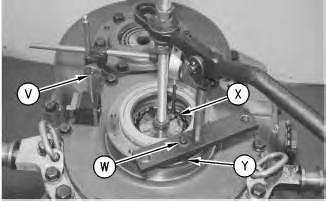
Illustration 24
g00843737
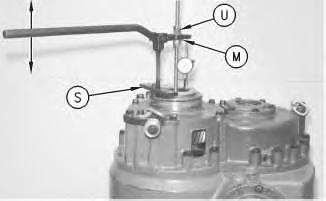
Illustration 25
g00843739
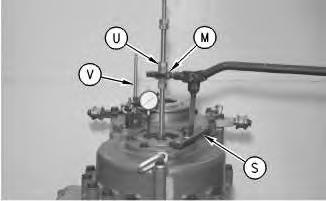
Illustration 26
g00843740
Tooling (S) requires an additional hole that is 16.00 mm (0.630 inch) (5/8 inch) in diameter. Tooling (s) is also a part of Tooling (T). Drill the hole for Tooling (W) 25 mm (1.0 inch) from the tapped center hole, as shown.
This is the Tooling that will be used to check the bearing clearance for the input transfer gear. The transfer gear is clamped to Tooling (P). Tooling (T) is used to force the gear to move. The gear can be moved upward or the gear can be moved downward with the lever. Tooling (L) fits in Tooling (P) to center Tooling (R) in the gear.
Note: Use the following Steps to measure the bearing clearance for the input transfer gear.
1. Install the Tooling in the transfer gear so that Tooling (R) and Tooling (P) are centered in the gear. Install Tooling (R) with the 5/8 by 11 thread on top.
2. Tighten Tooling (U) on top of the adapter in order to prevent movement of the gear. Tooling (N) can then be used to turn the gear.
3. Fasten Tooling (S) and Tooling (T) to the housing with Tooling (W), as shown. Use Tooling (Y) to support the plate.
4. Put the slotted end of the lever in a horizontal position on the threaded rod. Be sure that there is 1.0 mm (0.04 inch) clearance between Tooling (M) and the lever.
5. Lubricate the washers so that the assembly will turn smoothly.
6. Put Tooling (V) in position. Be sure that the indicator tip is vertical and that the indicator tip is in contact with the top adapter. Lubricate the surface of the adapter or lubricate the indicator tip.
7. Push the adapter downward and hold the adapter down while the lever is up. Use a ratchet wrench to turn the gear with Tooling (N). Rotate the gear for at least three revolutions. Watch the needle on the dial indicator. Watch the backward movement and the forward movement. Stop rotating the gear at the point of the maximum needle movement.
Note: The needle may move back and forth during rotation due to runout in the adapter. The reading should always be taken at the same location so that the measurement will be accurate and consistent.
8. Mark the location of Area (X). Mark the location at the point of maximum needle movement on the surface of the adapter. Set the dial indicator to zero as you force the gear downward.
9. Pull the gear upward by pulling the lever downward. Do this procedure as you turn the gear at least three revolutions. Record the maximum reading that is obtained when the indicator tip is returned to Area (X). This reading will be the actual bearing clearance. The reading should be 0.10 ± 0.05 mm (0.004 ± 0.002 inch).
10. Repeat the procedure. The result should be identical if the first procedure was correctly done.
Note: Use the following Steps to measure the bearing clearance for the pinion gear.
11. Screw the 5/8 - 11 NC end of Tooling (R) in the pinion shaft.
12. Put the lever assembly and Tooling (S) in position. Install Tooling (W) in the bearing retainer. Use Tooling (Y) to support the plate.
13. Adjust Tooling (U) so that the slotted end of the lever is horizontal.
14. Allow 1.0 mm (0.04 inch) clearance between the lever and Tooling (M). Lubricate both washers.
15. Put Tooling (V) in position, as shown. Be sure that the indicator tip is vertical and that the indicator tip is in contact with the flat end surface of the pinion gear. Lubricate the flat end surface of the pinion gear or lubricate the indicator tip.
16. Rotate the pinion for at least three revolutions as you force the pinion gear downward by lifting up on Tooling (T). Watch the backward movement and the forward movement of the needle on the dial indicator as the pinion gear is being rotated. Stop rotating the pinion gear at the point of the maximum needle movement. Mark the location at the point of maximum needle movement on the surface of the pinion gear. Set the dial indicator to zero as you force the pinion gear downward.
Note: The needle may move back and forth during rotation due to runout in the surface of the pinion gear. The reading should always be taken at the same location so that the measurement will be accurate and consistent.
17. Pull the pinion gear upward by pulling the lever downward. Do this procedure as you turn the pinion gear at least three revolutions. Record the maximum reading that is obtained
when the indicator tip is returned to the marked location. This reading will be the actual bearing clearance. The reading should be 0.10 ± 0.05 mm (0.004 ± 0.002 inch).
18. Repeat the procedure. The result should be identical if the first procedure was correctly done. Copyright 1993 - 2024 Caterpillar Inc. All Rights Reserved.
Network For SIS Licensees. Thu Jul 11 13:25:16 UTC+0530 2024
Product: TRACK-TYPE TRACTOR
Model: D6T TRACK-TYPE TRACTOR LAE
Configuration: D6T TRACK-TYPE TRACTOR
Disassembly and Assembly
D6T Track-Type Tractor Power Train
i06151275
Bevel and Transfer Gears - Disassemble SMCS - 3011-015
Disassembly Procedure Table 1 Required Tools
Start By:
A. Separate the transmission and bevel gears.
Note: Put identifying marks on all of the shims as the shims are removed. The identifying marks will ensure correct installation at assembly.
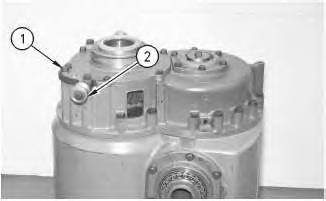
Illustration 1
g00504390
1. Remove bolts (1) and roller brackets (2) from each side of the transfer gear case.
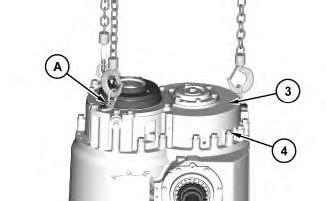
Illustration 2
g01206244
2. Remove and discard bolts (4) that hold transfer gear case (3) to the bevel gear case.
3. Install Tooling (A) and attach a suitable lifting device to Tooling (A) . Remove transfer gear case (3) from the bevel gear case. The weight of transfer gear case (3) is approximately 101 kg (223 lb).
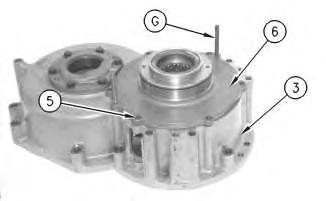
3
4. Remove bolts (5) that hold cage (6) to transfer gear case (3) .
5. Install Tooling (G) . Tighten Tooling (G) evenly. Remove the cage and the shims from the transfer gear case.
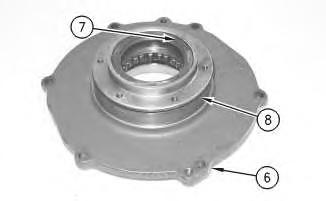
Illustration 4
g00830580
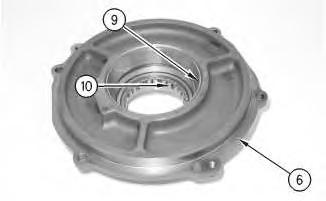
6. Remove lip seal (7) and O-ring seal (8) from cage (6) .
This is the sample of the manual click on the download link for complete manual
DOWNLOAD LINK
For some reason if link does not work download this pdf and then click