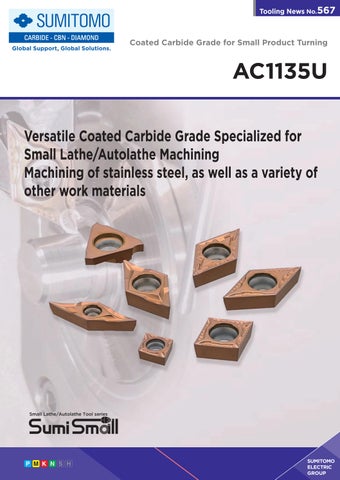
Coated Carbide Grade for Small Product Turning
Versatile Coated Carbide Grade Specialized for Small Lathe/Autolathe Machining
Machining of stainless steel, as well as a variety of other
work materials
Coated Carbide Grade for Small Product Turning
Application Range Features of AC1135U
Coated Carbide for Small Product Turning
AC1135U
Coated Carbide for Small Product Turning
AC1135U
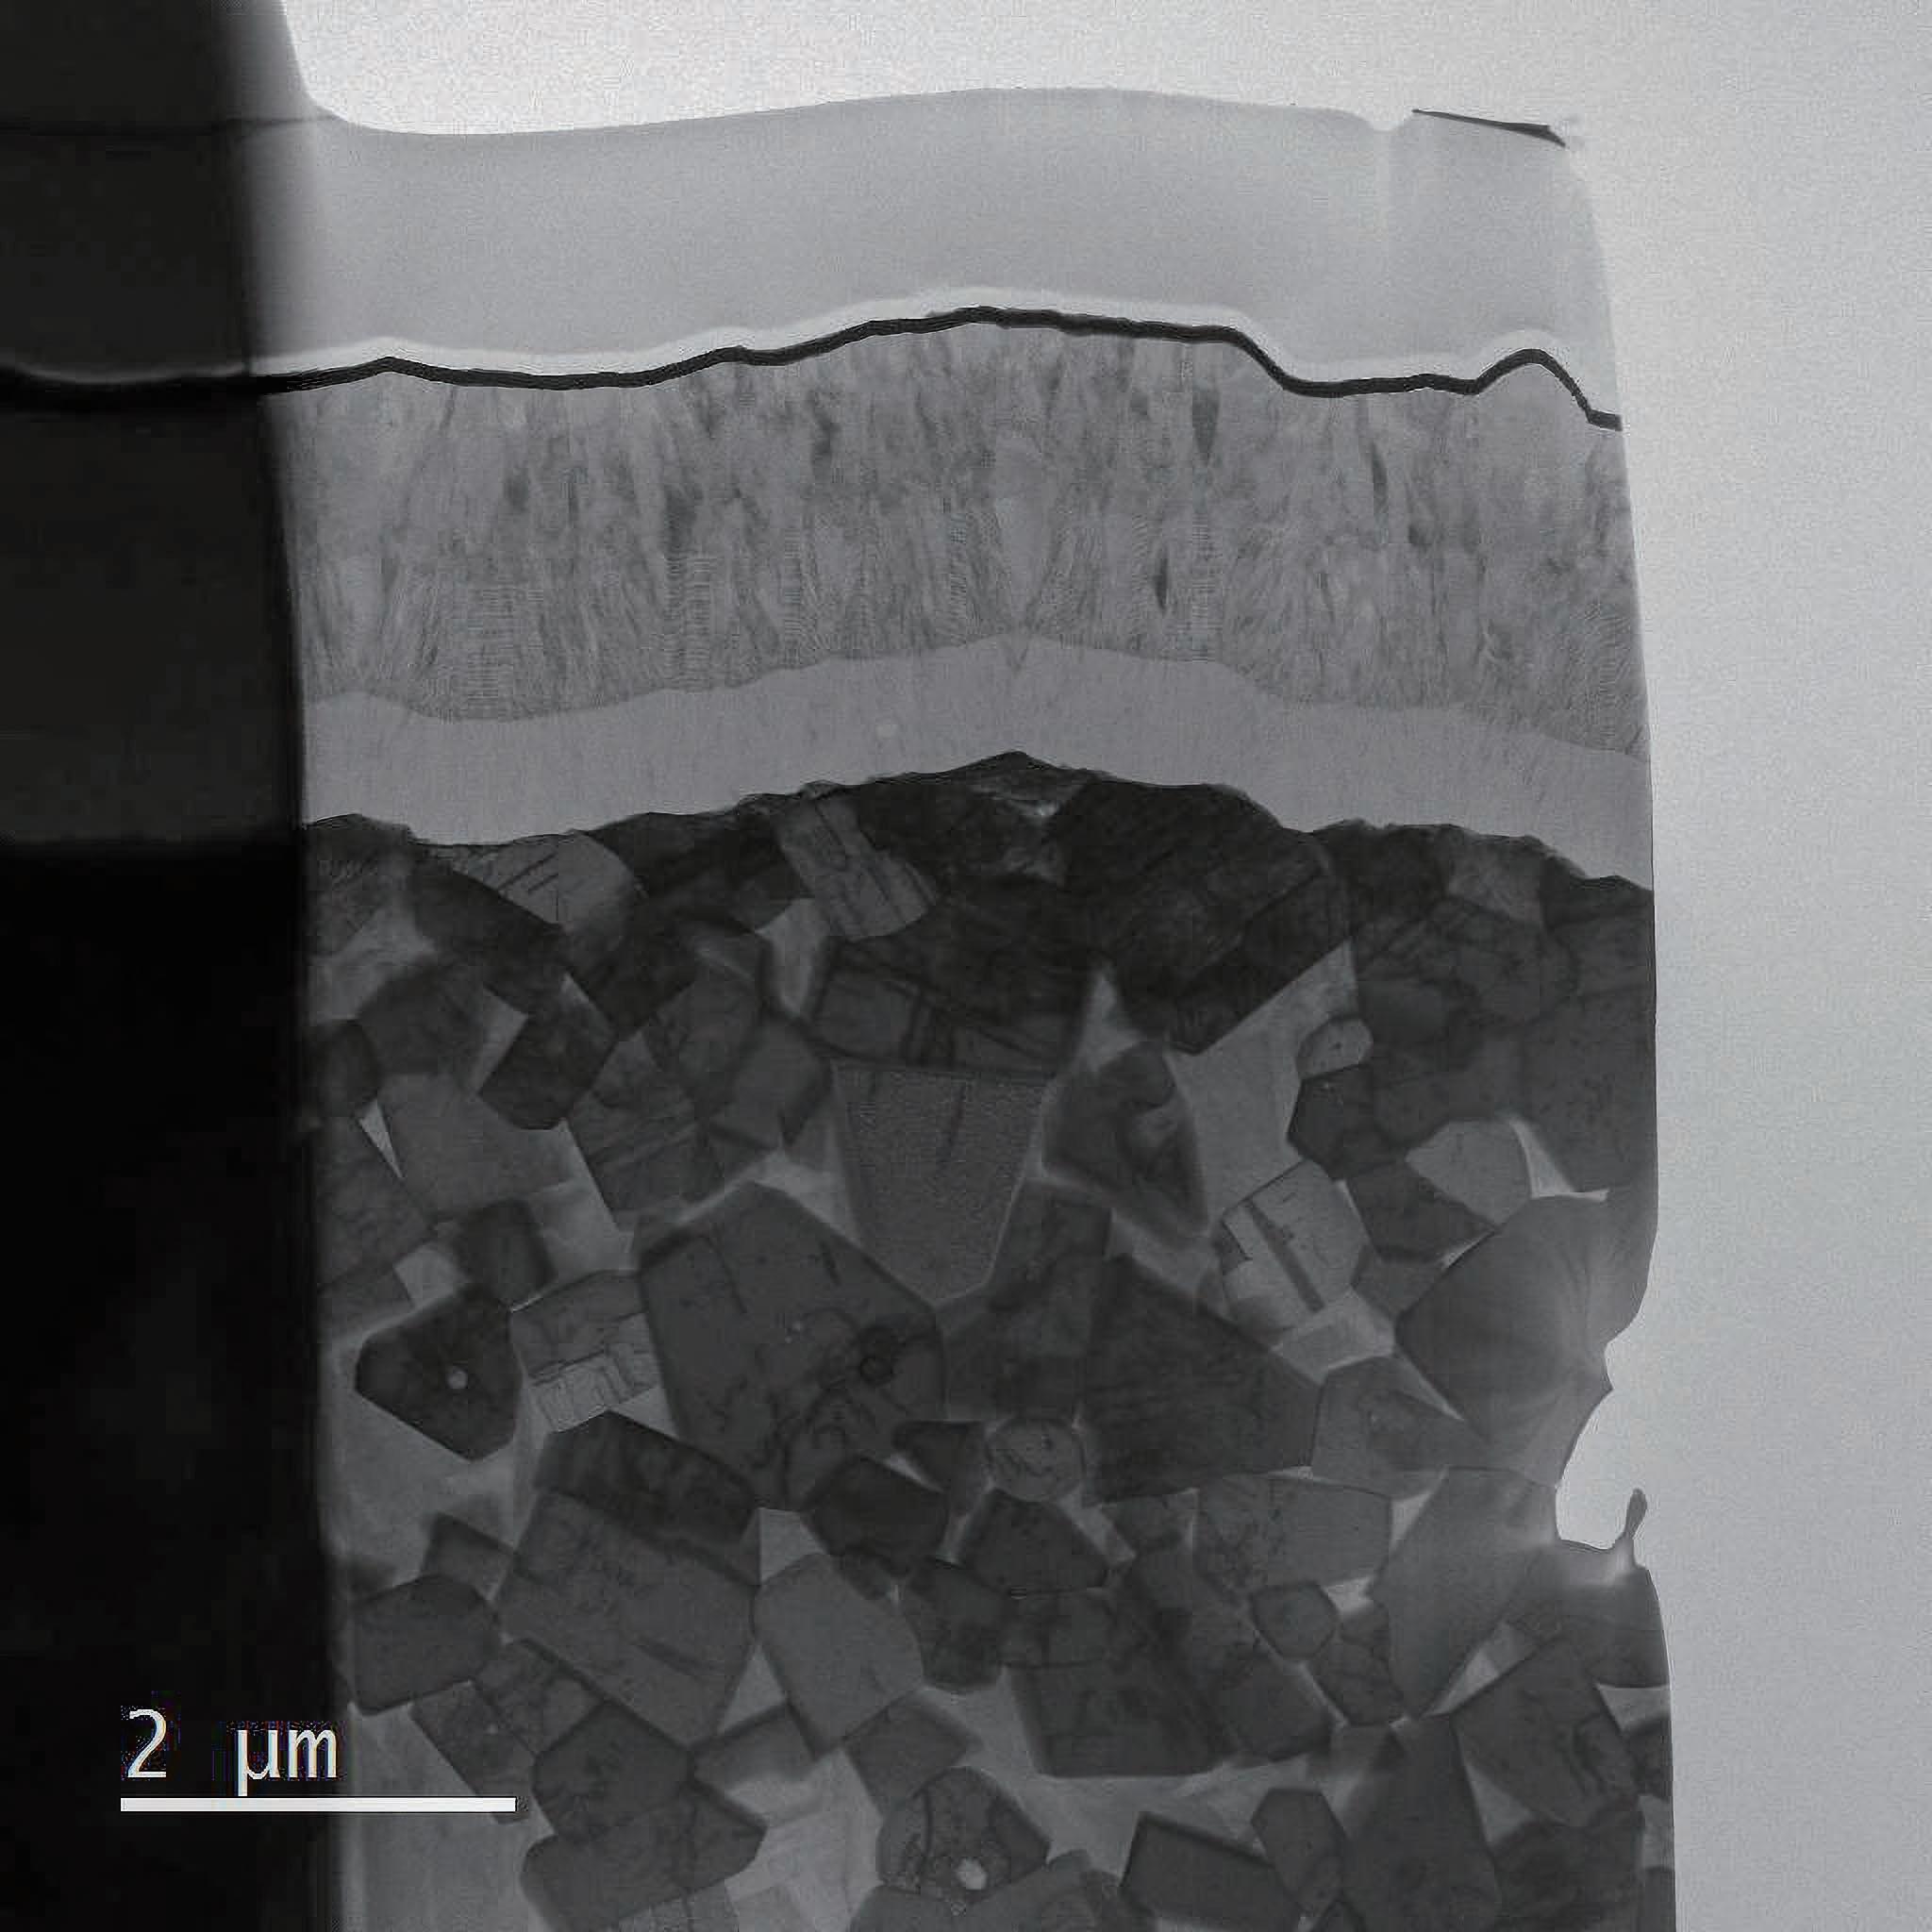
Carbide Substrate
Special Surface Treatment
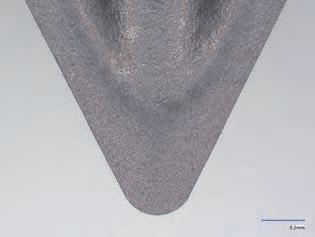
The smooth, glossy surface suppresses adhesion and reduces the occurrence of micro-chipping
Adhesion-resistant Layer (TiCN-based)
The use of a TiCN-based composition with excellent adhesion resistance reduces adhesion in fine cutting and low-speed conditions, maintaining high machined surface quality
Chipping-resistant Layer (TiAlBN-based)
The use of an ultra-fine grained TiAlBN-based composition with excellent toughness suppresses unexpected chipping and achieves high stability
High-adhesion Technology
Improved stability with special technology enhancing coating adhesion strength
Chipbreaker Selection (Main Chipbreakers)
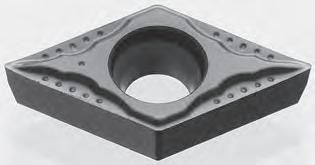
SI type
Excellent chip control performance over a wide range of cutting conditions
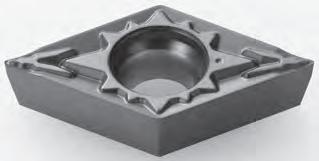
FF
type
Outstanding chip control in fine finishing applications
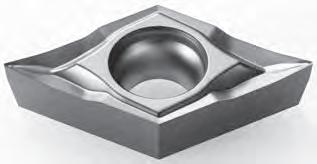
SL type
Exhibits excellent cutting edge sharpness over a wide range of cutting conditions. Emphasis on high machined surface quality
Chipbreaker Application Range
Selecting Chipbreakers
Recommended
Machined Surface Quality in Facing (Stainless Steel)
Excellent machined surface quality even at low speeds
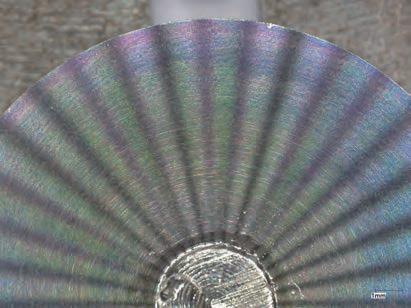
vc = 120m/min
vc = 60m/min
vc = 20m/min
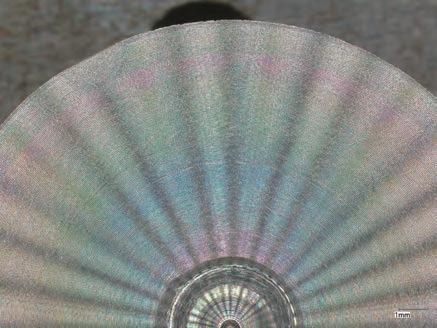
Work Material: SUS316L Continuous Cutting Insert: DCGT11T302
Cutting Conditions: n = 1,800min-1 f = 0.05mm/rev ap = 0.5mm Wet (oil-based)
Machined Surface Quality in External Grooving (Stainless Steel)
Machined surface quality superior to conventional grades
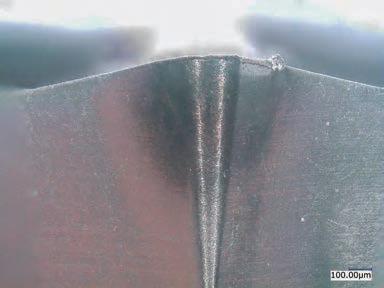
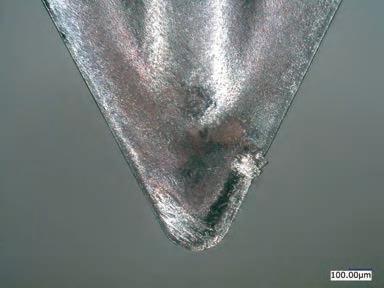
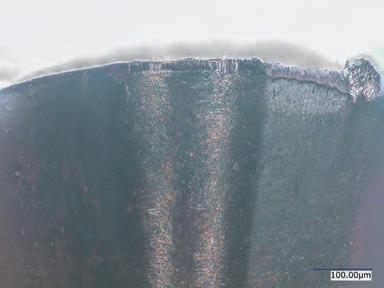
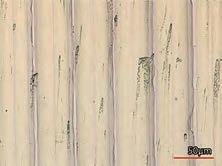
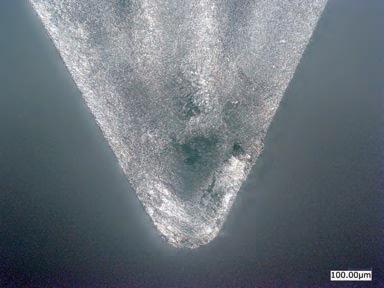
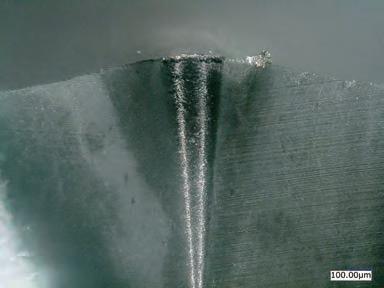
Work Material: SUS316L Continuous Cutting ø10mm Insert: DCGT11T302
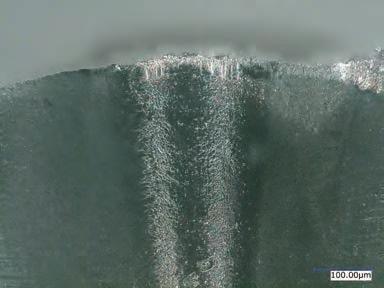
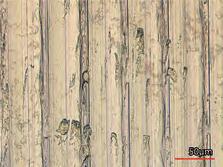
Cutting Conditions: vc = 120m/min f = 0.05mm/rev ap = 0.5mm Wet (oil-based)
Stability in External Grooving (Stainless Steel)
Machined surface quality and dimensional accuracy can be maintained over a longer period
Machined Surface RoughnessWork Material Dimensional Variation AC1135U
Competitor's Grade A
Conventional
Competitor's Grade A
Work Material: SUS316L Continuous Cutting ø10mm L = 14mm Insert: DCGT11T302
Cutting Conditions: vc = 120m/min f = 0.05mm/rev ap = 0.5mm Wet (oil-based)
Machined Surface Quality in Cut-o Machining (Stainless Steel)
Achieves 1.7x longer tool life than conventional grades and reduced tearing on machine surface
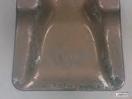
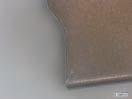
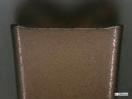
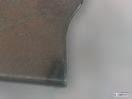
AC1135U
Reduced tearing, machining continued through 125 pieces
Conventional Grade Tearing, machining unable to continue at 75 pieces
Work Material: SUS316L Cut-off ø10mm Insert: GCMN2002-GF
Cutting Conditions: n = 3,000min-1 f = 0.05mm/rev Wet (oil-based)
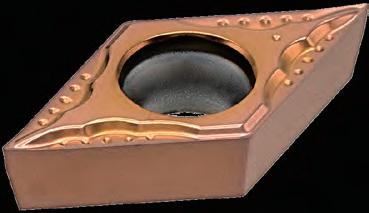
80° Diamond type Positive Inserts


55° Diamond type Positive Inserts


DCGT
DCGT 11T301MN-SL
Triangular type Positive Inserts


Right-handed (R) inserts are used with right-handed (part number suffix: -R3J) holders and heads.
Part Number Suffix Code (Chipbreakers)
Select holders and inserts with matching width of cut (CW). Not usable with GNDXL type / GNDIS type holders.
Select holders and inserts with matching width of
Suppresses cutting edge chipping to achieve 12.5x longer tool life
Suppresses wear to achieve 7.5x longer tool life
Tool: DCGT070201MN-SI (AC1135U) Continuous External Turning and Facing
Cutting Conditions: vc = 110m/min f = 0.04mm/rev ap = 0.05-0.20mm Wet (oil-based)
Minimal damage in comparison to machining the same number of workpieces with competitor’s grade
Tool: DCGT070202MN-SI (AC1135U) Continuous External Turning
Cutting Conditions: vc = 50m/min f = 0.03mm/rev ap = 0.2mm Wet (oil-based)
SUS304 Electrical Device Component
Suppresses chipping for good machined surface quality in comparison to machining the same number of workpieces with conventional grade
Tool: DCGT11T301MN-SI (AC1135U) Continuous External Turning and Facing Cutting Conditions: vc = 110m/min f = 0.04mm/rev ap = 0.15mm Wet (oil-based)
Good machined surface quality even when machining twice the number of workpieces as competitor’s grade
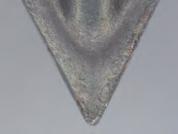
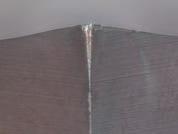
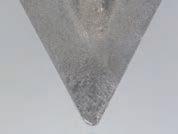
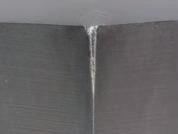
Tool: DCGT070201MN-SI (AC1135U) Continuous External Turning Cutting Conditions: vc = 40m/min f = 0.04mm/rev ap = 0.2mm Wet (oil-based) Low-frequency vibration cutting
Tool: VCGT110302MN-SI (AC1135U) Continuous External Turning Cutting
Application Examples
STKN Material Automotive Component Pure Iron Automotive Component
Suppresses rake face wear to achieve 1.5x longer tool life
Tool: DCGT11T301MN-SI (AC1135U) Continuous External Turning
Cutting Conditions: vc = 120m/min f = 0.05mm/rev ap = C0.2 Wet (oil-based)
Suppresses corner tip chipping to achieve 1.4x longer tool life
Tool: CCGT09T302MN-SI (AC1135U) External Turning and Interrupted Facing
Cutting Conditions: vc = 150m/min f = 1.0mm/rev ap = 0.2mm Wet (oil-based)