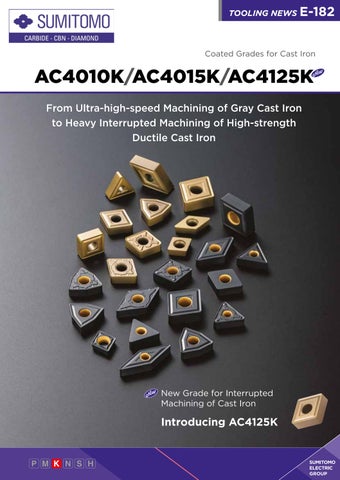
Coated Grades for Cast Iron
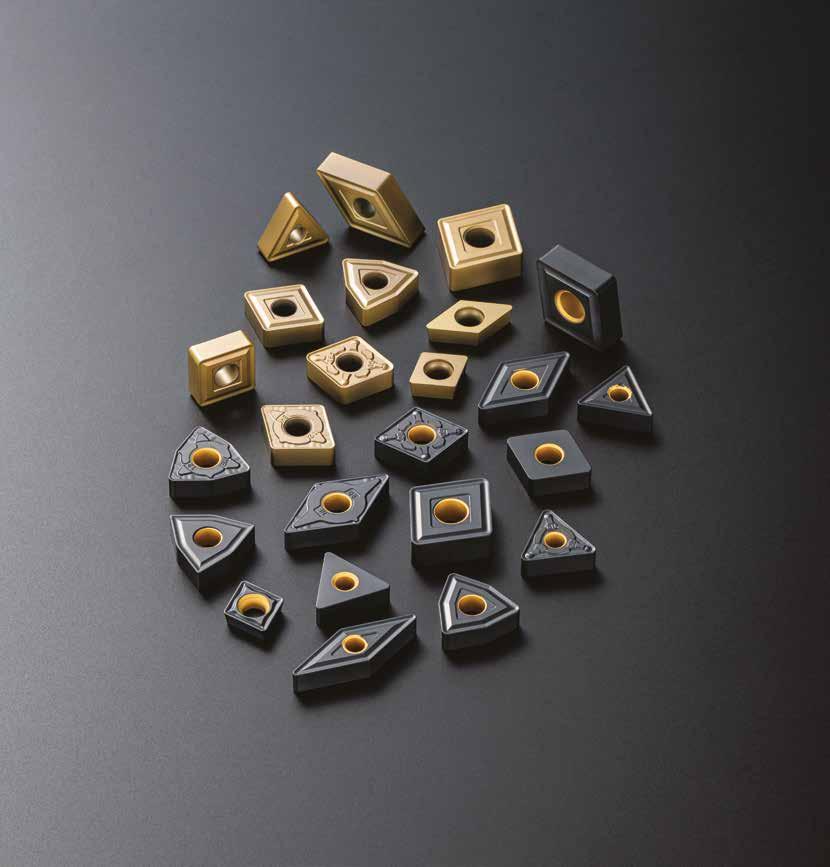
From Ultra-high-speed Machining of Gray Cast Iron to Heavy Interrupted Machining of High-strength
Ductile Cast Iron
New Grade for Interrupted Machining of Cast Iron Introducing AC4125K
Coated Grades
AC4010K/AC4015K/AC4125K
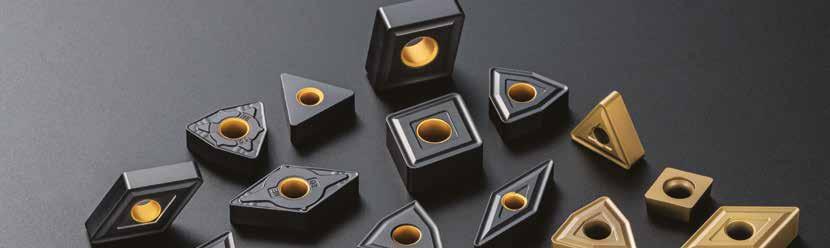
AC4010K
AC4015K
AC4125K
Features AC4010K / AC4015K
AC4010K
Our 1st recommended grade for machining gray cast iron.
Ultra-thick film coating enables ultra-high-speed machining at vc=700m/min.
AC4015K
Our 1st recommended grade for machining of ductile cast iron.
High-adhesion and high-strength coating enables stable and long tool life.
AC4125K
Our 1st recommended grade for interrupted machining of cast iron.Especially effective for stable long life in roughing of parts like differential cases and carriers.
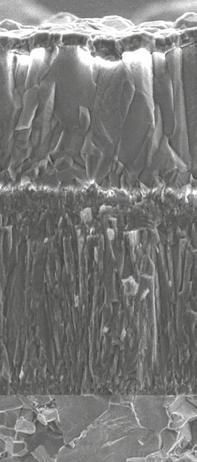
Technologies for high-adhesion, crystal orientation control and residual stress control realise stable tool life for various types of cast iron, from grey cast iron (GJL) to high-strength ductile cast iron (GJS).
Special Surface Treatment
Compressive stress more than twice as high as conventional stress Chipping resistance: Twice as much as conventional types
Crystal Orientation Control Alumina Layer
Crater wear resistance in high-speed machining: Twice as much as conventional types
C-rich Ultra-fine TiCN Layer
Flank wear resistance: Twice as much as conventional types
High Adhesion Technology
Smooth layer adhesion treatment (Rz0.15μm0.07μm) greatly improves peel-off resistance
Coated Grades for Cast Iron
AC4010K/AC4015K/AC4125K
Applications of AC4000K Series (Example)
SUMIBORON BN7125
For finishing of gray cast iron For High-speed Machining General-purpose For Interrupted Turning From finishing to machining of ductile cast iron.
SUMIBORON BNC500
Machining of gray cast iron 1st Recommendation for unstable machining Interrupted cutting for higher wear resistance for higher wear resistance for unstable machining Interrupted cutting
AC4010K AC4015K AC4125K
Our 1st recommended product for machining of ductile cast iron High-precision Machining
Features of AC4125K
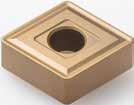
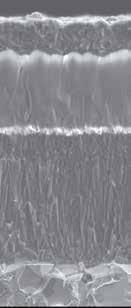
Carbide Substrate
Excellent chipping resistance is demonstrated by the evolution of high adhesion technology, fine crystal orientation control technology and residual stress control technology, and very stable machining is realized in heavy interrupted machining and unstable machining of cast iron. In addition, it adopts a gold color that makes used corners easily identifiable.
Special Surface Treatment
Significantly improves the compressive stress while maintaining the gold color Chipping resistance: Twice as much as conventional types
Crystal Orientation Control Ultra-fine Alumina Layer
Fine grain structure greatly improves the coating strength Chipping resistance: Twice as much as conventional types
C-rich Ultra-fine TiCN Layer
Flank wear resistance: 1.5x as much as conventional types
High Adhesion Technology
Smooth layer adhesion treatment (Rz0.15μm0.07μm) greatly improves peel-off resistance
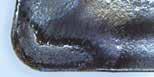
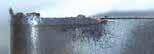
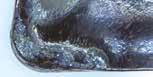
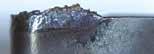
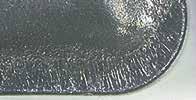
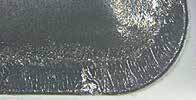
Work Material: GG25
Continuous
Insert: CNMG120408
Cutting Conditions: vc=600m/min
f=0.4mm/rev
ap=2.0mm
Dry
Work Material: GG25
Interrupted
Insert: CNMG120408
Cutting Conditions: vc=400m/min
f=0.3mm/rev
ap=2.0mm
Wet
Work Material: GGG70 Continuous
Insert: CNMG120408
Cutting Conditions: vc=140m/min
f=0.3mm/rev ap=1.5mm Wet
Work Material: GGG-40.3 Interrupted
Insert: CNMG12040
Cutting Conditions: vc=450m/min f=0.3mm/rev ap=1.5mm Wet