E-167_AC5005S-AC5015S-AC5025S

Page 1


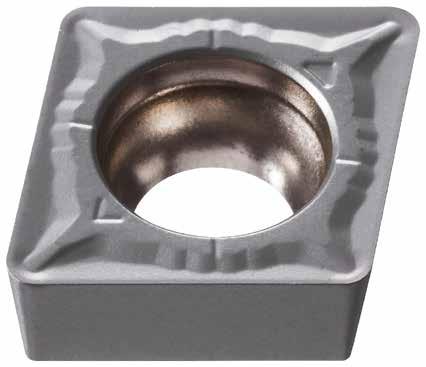
Coated Grades for Exotic Alloys

AC5005S/AC5015S/AC5025S

New Grades for Exotic Alloy Turning, Creating „Absolutely Stable Cutting“ Introducing

Application Range

AC5005S AC5005S

For high-efficiency machining

Excellent wear resistance, tool life 1,5 x conventional grade

Features of AC5000S Series

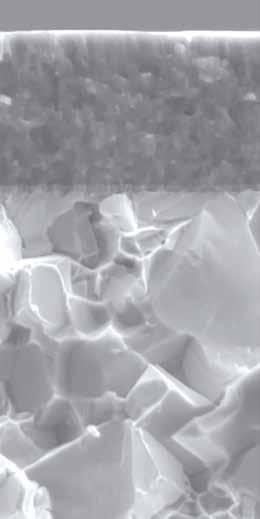
Newly developed heatresistant carbide substrate

PVD-coating technology ABSOTECHTM

Newly developed tough carbide substrate

1st recommendation

Excellent wear resistance, 2 x conventional grade

AC5015S AC5025S

For interrupted machining

Fracture resistance, 1,5 x conventional grade

Also suitable for work materials other than exotic alloys

Applicable work materials:

Try the following grades if even greater rigidity is required.

High efficiency with a newly developed dedicated substrate with excellent high-temperature hardness/strength. Realises excellent wear resistance and plastic deformation resistance during machining.

AC5005S

Excellent high-temperature strength

Conventional Carbide Substrate (High-temperature deformation evaluation 800°C)

Deformation at high temperatures 50% down from conventional grade

Highly heat-resistant ultra-multi-layer thin-film AlTiSiN structure realizes excellent crater wear resistance and flank wear resistance.

Introduction of a revolutionary new sintering process enables hardness to be maintained while greatly improving rigidity, whilst attaining a reduction in boundary defects and chipping resistant issues.

AC5005S Series

Excellent Cutting Edge Quality

Conventional

For Exotic Alloy Turning

Chipbreaker Selection Guide

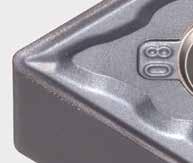
Finishing

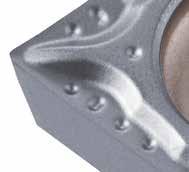
Main chipbreaker exhibits excellent chip evacuation performance even with small depth of cut.

Cutting edge designed with an emphasis on sharpness (20° rake angle) to suppress wear.

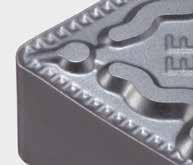
Medium to Rough Cutting

Grooved rake face suppresses heat generation and uneven contact.

Spherical protrusions exhibits excellent chip evacuation performance over a wide range of conditions.

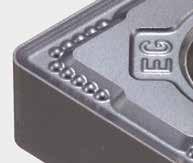
Rough Cutting

Cutting edge shape that retains its strength even after wear progresses.

Chipbreaker Cross-Section

Corner

Large convex rake face design keeps its cutting edge strength while suppressing crater wear.

_

Chipbreaker Cross-Section

Corner

Suppresses notch wear by eliminating the change of cutting points on the cutting edge.

Finishing to Light Cutting

Dimpled shape suppresses heat generation due to large depths of cut.

_

Chipbreaker Cross-Section

Corner

Cutting edge designed with an emphasis on sharpness (15° rake angle). Cutting edge shape intended to improve profiling and reduce cutting force.

Light to Medium Cutting

Suppresses chip build-up at high feed rates for ideal chip control.

Protrusion design controls chip flow.

CNMG1204_ _

Chipbreaker Cross-Section Corner Edge

CCGT09T3_ _

Chipbreaker Cross-Section Corner Edge

Rake face shape with excellent balance of sharpness and strength.

CCGT09T3_ _

For Exotic Alloy Turning

AC5005S/AC5015S/AC5025S

Cutting Performance of AC5005S

Comparison of Wear Resistance (High-speed)

Competitor‘s

Competitor‘s

Comparison of Wear Resistance (High-feed)

Competitor‘s

Competitor‘s

Tool Life (V-T Chart, High-feed)

Competitor‘s

C (S05 PVD)

Competitor‘s

D (S05 PVD)

Newly developed heat-resistant carbide substrate and PVD coating technology ABSOTECHTM suppress wear.

AC5005S/AC5015S/AC5025S

Cutting Performance of AC5015S

New PVD coating technology

ABSOTECHTM reduces wear.

AC5015S achieves 2x wear resistance compared to conventional grade.

Work Material: Insert:

Cutting Conditions:

Inconel 718 (44HRC) CNMG120408 vc = 40 m/min, f = 0,1 mm/rev, ap = 1,5 mm, wet

Newly developed hard base material suppresses boundary defects.

AC5015S achieves 1,5x fracture resistance compared to conventional grade.

Work Material: Insert:

Cutting Conditions:

Hastelloy (22HRC) CNMG120408

vc = 50 m/min, f = 0,1 mm/rev, ap = 1,5 mm, wet

Cutting Performance of AC5025S

New PVD coating technology

ABSOTECHTM suppresses wear.

AC2025S achieves 2,5x wear resistance compared to conventional grade.

Work Material: Insert:

Cutting Conditions:

Inconel 718 (44HRC)

CNMG120408

vc = 40 m/min, f = 0,1 mm/rev, ap = 1,5 mm, wet

Newly developed hard base material suppresses boundary defects.

AC2025S achieves 1,5x fracture resistance compared to conventional grade.

Work Material: Insert:

Cutting Conditions:

Hastelloy (22HRC)

CNMG120408

vc = 50 m/min, f = 0,1 mm/rev, ap = 1,5 mm, wet

Application Examples of AC5005S

Inconel 718, Aerospace Component

Good wear resistance for 2x longer tool life.

Competitor‘s product C (S05 CVD)

Insert:

Cutting Conditions:

CNMG 190616 NEG vc= 55 m/min, f = 0,3 mm/rev, ap = 3,0 mm, wet

Ni-Based Heat-Resistant Alloy, Industrial Machine Component

Good wear resistance for at least 5x longer tool life.

(16 passes/C)

Conventional (S10 PVD) (3 passes/C)

Insert: Cutting Conditions: TNMG 160408 NEF vc = 30m/min, f = 0,13 mm/rev, ap = 0,8 mm, wet

15-5 PH Stainless Steel, Industrial Machine Component

Good wear resistance for 1,4x longer tool life.

Insert:

Competitor‘s product F (M10 CVD)

Cutting Conditions: CNMG 120408 NEG vc = 100 m/min, f = 0,2 mm/rev, ap = 0,6 mm, wet

Inconel 718, Aerospace Component

Suppresses wear and extends tool life.

Comp‘s D (S05 PVD) (1 pass/C)

Insert: Cutting Conditions: CNMG 120408 NUP vc = 45 m/min, f = 0,15 mm/rev, ap = 3,2 mm, wet

Hardened Steel, Industrial Machine Component (50–55HRC)

Good wear resistance for 13% reduced machining time and extendable tool life.

pass/C)

Comp‘s E (S05 PVD) (1 pass/C)

Insert: Cutting Conditions: SNMG 120412 NGU vc= 51 m/min, f = 0,4 mm/rev, ap = 1,4 mm, wet

15-5 PH Stainless Steel, Aerospace Component

Good wear resistance for 66% reduced machining time and 1,5x longer tool life.

Insert:

Cutting Speed: 1,5x Feed Rate: 1,3x (1 pass/C)

Competitor‘s product G (S10 PVD)

Cutting Conditions: CNMG 120412 NME vc = 55 m/min, f = 0,36 mm/rev,ap = 2,5 mm, wet

For Exotic Alloy Turning Application Examples of AC5015S

Ni-Based Heat-Resistant Alloy, Automotive Component

Good wear resistance for 1,5 times longer tool life.

AC5015S NEX

Competitor‘s product A (S10 PVD)

Insert:

Cutting Conditions:

TNMG 160404 NEX vc = 82 m/min, f = 0,12 mm/rev, ap = 0,5 mm, wet

Inconel 713C, Automotive Component

Suppresses wear and shows 2,0 times longer tool life.

AC5015S NEX

Conventional

Insert:

Cutting Conditions:

CNMG 120408 NEX vc = 100 m/min, f = 0,12 mm/rev, ap = 0,3 mm, wet

Inconel 625, Aeronspace Component

Good wear resistance for 1,6 times longer tool life.

AC5015S NGU

Competitor‘s product C (S10 PVD9

Inconel, Automotive Component

Suppresses wear and extends tool life.

AC5015S NEF

pcs/C)

Conventional (21 pcs/C)

Insert:

Cutting Conditions: TNMG 160408 NEF vc = 30 m/min, f = 0,04 mm/rev, ap = 0,5 mm, wet

Inconel 718, Aeronautic Component

Good wear resistance for 2,0 times longer tool life.

AC5015S NEG

Competitor‘s product B (S10 PVD)

Insert:

Cutting Conditions: SNMG 120408 NEG vc = 50 m/min, f = 0,15 mm/rev, ap = 2,0 mm, wet

Insert:

Cutting Conditions: CNMG 120408 NGU vc = 50 m/min, f = 0,3 mm/rev, ap = 0,5 mm, wet

Inconel 718, Aerospace Component

Good wear resistance for 2,0 times longer tool life.

AC5015S NEG

Competitor‘s product D (S10 PVD)

Insert:

Cutting Conditions: CNMG 120408 NEG vc = 37 m/min, f = 0,2 mm/rev, ap = 1,4 mm, wet

For Exotic Alloy Turning

Application Examples of AC5015S

100Cr, Automotive Component

Suppresses wear for 2,0 times longer tool life.

Competitor‘s product E (P10 PVD)

Insert:

Cutting Conditions: TNGG 160402 RFY vc= 120 m/min, f = 0,1 mm/rev, ap = 0,3 mm, wet

GX10CrNi18-8 Stainless Cast Steel Valve Component

Suppresses wear for 2,2 times longer tool life.

0,23mm

(pcs)

Competitor‘s product G (S10 PVD)

Insert:

Cutting Conditions: CNMG 120408 NEM vc = 90m/min, f = 0,15 mm/rev, ap = 2,0 mm, wet

Hardened Steel Automotive Component (47 HRC)

Suppresses wear for 2,0 times longer tool life.

(pcs)

Insert:

Cutting Conditions: DCGT 070202 MNSI vc = 70 m/min, f = 0,03 mm/rev, ap = 0,80 mm, wet

Alloy Steel, Industrial Machine Component

Stable machining for 1,6 times longer tool life.

0,23mm

0,23mm

NEM

Insert:

Competitor‘s product F (S10 PVD)

Cutting Conditions: CNMG 120408 NEM vc = 120 m/min, f = 0,25 mm/rev, ap = 0,30 mm, wet

EN-GJS-450-10, Automotive Component

Suppresses wear for 2,0 times longer tool life.

Conventional

Insert:

Cutting Conditions: SPGT 090308 L/RSD vc= 210 m/min, f = 0,19 mm/rev, ap = 0,25 mm, wet

Sintered Ferrous Alloy, Automotive Component

Suppresses notch wear for 1,7 times longer tool life.

(pcs)

Insert:

Cutting Conditions: CNMG 120408 NGU vc = 170 m/min, f = 0,15 mm/rev,ap = 0,30 mm, wet

Application Examples of AC5025S

Inconel 718, Aerospace Component

Suppresses fracture for 1,7 times longer tool life.

Conventional (1,5 pcs/C)

Inconel 718, Aerospace Component

Suppresses wear for 1,5 times longer tool life.

(12 pcs/C)

Insert:

Cutting Conditions: DNMG 150608 NEG vc= 35 m/min, f = 0,1 mm/rev, ap = 1,6 mm, wet

Ni-Based Heat-Resistant Alloy, Automotive Component

Enables stable machining for 2,0 times longer tool life.

Competitor‘s product A (100 pcs/C)

Insert:

Cutting Conditions: TNGG 160402 NSU vc = 70m/min, f = 0,1 mm/rev, ap = 0,15 mm, wet

Hastelloy, Aerospace Component

Suppresses wear for 4 times longer tool life.

Output (pcs) (200 pcs/C) (200 pcs/C) (18pcs/C) (2,5 pcs/C)

Competitor‘s product B (S10 PVD)

Insert:

Cutting Conditions: CNMG 120412 NMU vc = 100 m/min, f = 0,3 mm/rev, ap = 3,0 mm, wet
Insert:

Cutting Conditions: TNGG 160402 RFY vc = 37 m/min, f = 0,1 mm/rev, ap = 0,1 mm, wet

Inconel, Automotive Component

Suppresses wear and extends tool life. Conventional (200 pcs/C)

Insert:

Cutting Conditions: DCMT 11T308 NSU vc= 49 m/min, f = 0,15 mm/rev, ap = 0,5 mm, wet

Fe-Based Heat-Resistant Alloy, Valve Component

Enables stable machining for 2 times longer tool life.

Output (pcs)

Conventional

Insert:

Cutting Conditions: WNMG 080408 NEM vc = 90 m/min, f = 0,15 mm/rev,ap = 1,5 mm, wet

AC5025S

Application Examples of AC5025S

100Cr6, Industrial Machine Component

Good wear resistance for 2,0 times longer tool life.

PVD)

Insert: Cutting Conditions: TNGG 160402 RFY vc= 110 m/min, f = 0,1 mm/rev, ap = 1,5 mm, wet

X5CrNiMo17-12-2, Industrial Machine Component

Suppresses wear for 1,5 times longer tool life.

Heat Resistant Stainless Steel, Automotive Component

Stable machining for 2,0 times longer tool life.

Vbmax: 0,23mm Vbmax: 0,23mm

Vbmax: 0,23mm AC5025S RFY AC5025S NEG

Insert: Cutting Conditions: CNMG 120408 NEG vc = 80 m/min, f = 0,3 mm/rev, ap = 2,0 mm, wet
Hardened Steel, Industrial Machine Component (49 HRC)

Same tool life even at 1,4 times higher cutting speed.

NMU

NEG

Insert: Cutting Conditions: CNMG 120408 NEG vc = 120m/min, f = 0,3 mm/rev, ap = 1,5 mm, wet
Insert: Cutting Conditions: CNMG 120412 NMU vc= 350 m/min, f = 0,16 mm/rev, ap = 1,50 mm, dry

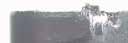
Negative Type Inserts Stock Items

Negative Type Inserts Stock Items

Positive Type Inserts Stock Items

Positive Type Inserts Stock Items

Positive Type Inserts Stock Items

Inserts for Grooving Tools GND Series (for Grooving / Cut-off)

Cut-off (Handed Edge)

GCMR: right-handed, GCML: left handed
External Profiling/External Radius Grooving

Grooving/Cut-off

Profiling/Radius Grooving/Necking

GCM

GCM

Note: The values in blue have been changed from the 2020-2021 General Cataloque.

Select holders and inserts with matching width of cut (CW). Not usable with GNDIS type holders.

Part Number Suffix Code (Chipbreakers)

Type Symbol Applications

Grooving/traverse cutting

Grooving/cut-off

Cut-off (Handed edge)

External profiling/external radius grooving

Profiling/radius grooving/necking

Multi-functional/general purpose

Multi-functional/low-feed

Grooving/general purpose

Grooving/low-feed

Grooving/Low cutting force

Cut-off/general purpose

Cut-off/low cutting force

Profiling/general purpose

Facing/necking/general purpose

For Exotic Alloy Turning

Recommended Cutting Conditions

Ni-based material

Fe-based material

Co-based material

AC5005S

AC5015S AC5025S

AC5005S AC5015S AC5025S

AC5005S

AC5015S AC5025S

AC5015S AC5025S

(Germany)

SUMITOMO ELECTRIC Hartmetall GmbH Konrad-Zuse-Straße 9, 47877 Willich

Tel. +49 2154 4992-0, Fax +49 2154 4992-161

Info@SumitomoTool.com www.SumitomoTool.com

(UK and Ireland)

SUMITOMO ELECTRIC Hardmetal Ltd. 3 Paper Mill Drive Redditch, B98 8QJ, UK

Tel. +44 1844 342081, Fax: +44 1844 342415 InfoUK@SumitomoTool.com www.SumitomoTool.com

Turn static files into dynamic content formats.

Create a flipbook
E-167_AC5005S-AC5015S-AC5025S by BTS Company d.o.o. - Issuu