The Future of Pharmaceutical Manufacturing
The pharmaceutical, biotechnology, healthcare, and life sciences industries are evolving rapidly, with increasing emphasis on contamination control, operational efficiency, and regulatory compliance. Modern cleanroom environments are no longer just controlled spaces they are intelligent ecosystems designed to ensure product quality, operator safety, and uninterrupted manufacturing processes.
As global GMP, WHO, FDA, and ISO standards continue to advance, manufacturers are adopting innovative cleanroom equipment that combines superior performance, energy efficiency, and smart technology.
We explore the latest trends in cleanroom equipment technology and how they are transforming pharmaceutical manufacturing.
Why Modern Cleanroom Technology Matters
Cleanrooms play a critical role in preventing contamination during pharmaceutical production. Even microscopic airborne particles can compromise product quality, resulting in production losses and regulatory issues.
Advanced cleanroom equipment helps organizations:
• Improve product quality.
• Reduce contamination risks.
• Increase operational efficiency.
• Protect personnel and products.
• Ensure GMP and ISO compliance.
• Lower maintenance and operating costs.
Investing in modern cleanroom technology is essential for companies looking to remain competitive in today’s pharmaceutical landscape.
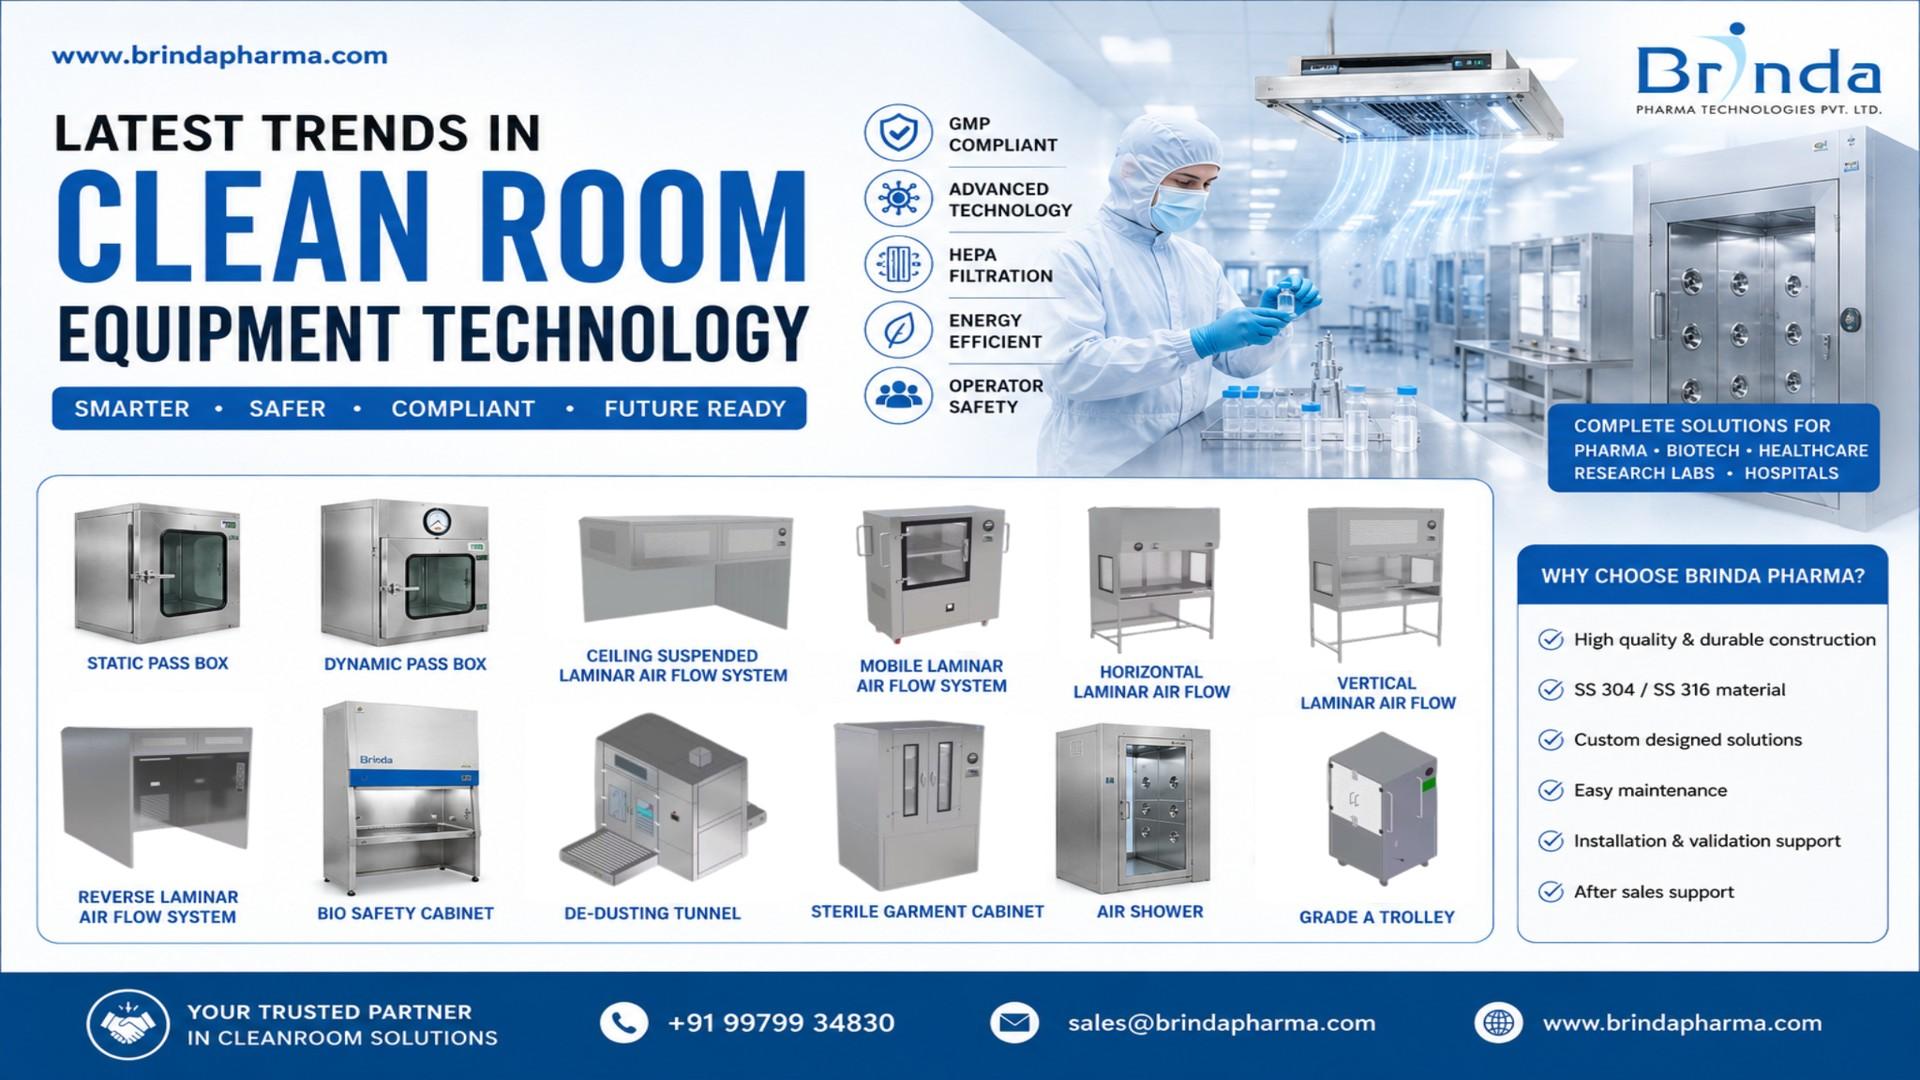
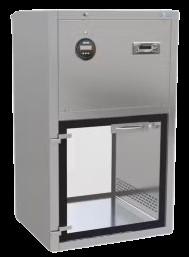
Smart Static & Dynamic Pass Boxes
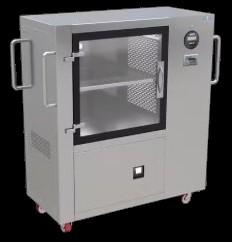
Material transfer is one of the most critical points where contamination can occur. Today’s Static Pass Boxes and Dynamic Pass Boxes incorporate advanced interlocking mechanisms, HEPA filtration, UV sterilization, and digital monitoring systems.
Latest Features:
• Electronic Door Interlocks.
• HEPA-filtered Airflow.
• UV Sterilization.
• Differential Pressure Monitoring.
• Touchscreen Controls.
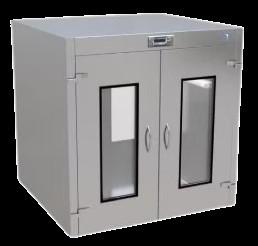
• Energy-efficient Operation.
Benefits:
• Prevent CrossContamination.
• Safe Material Transfer.
• Reduced Human Intervention.
• Improved GMP Compliance.
Complete Guide to Static & Dynamic Pass Boxes for Pharma Cleanrooms
Advanced Laminar Air Flow Systems
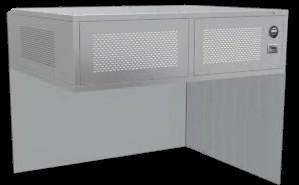
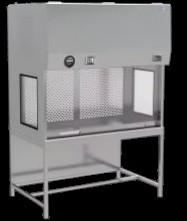
Laminar Air Flow systems continue to evolve with better airflow management and energysaving technologies.
Modern solutions include:
• Ceiling Suspended Laminar Air Flow Systems
• Mobile Laminar Air Flow Systems
• Horizontal Laminar Air Flow
• Vertical Laminar Air Flow These systems create ISO Class clean environments suitable for sterile manufacturing, sampling, filling, and laboratory applications.
Industry Trends:
• Uniform Airflow Distribution
• Smart Airflow Monitoring
• Low-noise EC Motors
• High-efficiency HEPA Filters
• Compact Modular Designs
• Easy Maintenance
Reverse Laminar Air Flow Systems
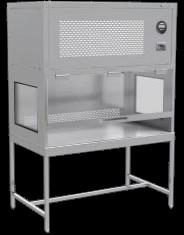
Reverse Laminar Air Flow (RLAF) systems are increasingly used for powder sampling and dispensing operations in pharmaceutical and API manufacturing.
New Technology Features:
• Negative pressure operation.
• Dust Containment.
• Enhanced Operator Protection.
• High-capacity HEPA Filtration.
• Ergonomic workstation Design.
Advantages:
• Reduces airborne Contamination.
• Protects operators.
• Prevents product loss.
• Improves Workplace Safety.
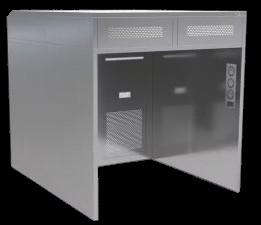
Complete Guide to Laminar Air Flow System for Pharma Cleanroom
Air Shower Cabinets with Enhanced Protection
Air Shower Systems remain one of the most effective contamination control solutions for cleanroom entry.
Latest Advancements:
• High-Velocity Air Nozzles.
• Automatic Operation.
• Motion Sensors.
• Energy-Saving Blowers.
• Digital Control Panels.
• Quick Cleaning Cycles.
Benefits:
• Removes Dust Particles.
• Prevents Contamination Entry.
• Improves Cleanroom Efficiency.
• Supports GMP Compliance.
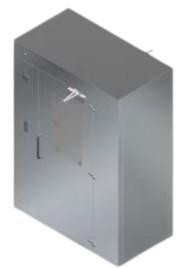
How to Choose the Right Air
Shower
Cabinet for Your Lab
Sterile Garment Cabinets
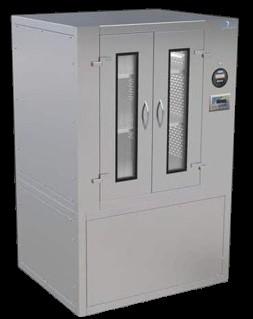
Proper storage of sterile garments is essential for maintaining cleanroom integrity.
Modern Sterile Garment Cabinets feature:
• HEPA-Filtered Airflow.
• Stainless Steel SS 304/316 Construction.
• UV Sterilization
• Humidity Control.
• Easy-clean Design.
These cabinets ensure garments remain contamination-free until use.
Complete Guide to Sterile Garment
Cabinets in Pharmaceutical Cleanrooms
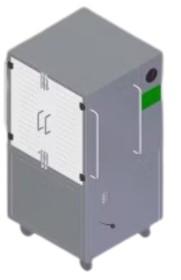
Grade A Trolleys for Sterile Material Handling
Material handling equipment has evolved to meet stringent cleanroom standards.
Today’s Grade A Trolleys Provide:
• Stainless Steel Construction.
• Smooth Hygienic Surfaces.
• Easy Maneuverability.
• Corrosion Resistance.
• Cleanroom-Compatible Design.
These trolleys ensure contamination-free transportation of sterile materials.