www.canplastics.com
NOVEMBER 2022
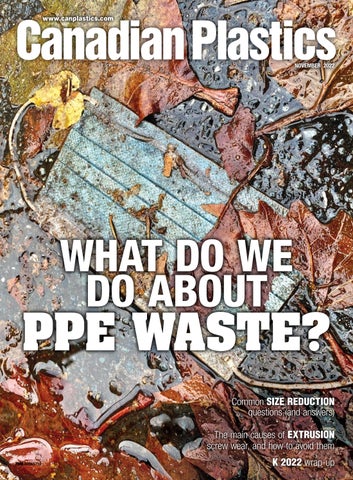
WHAT DO WE DO ABOUT PPE WASTE? Common SIZE REDUCTION questions (and answers) The main causes of EXTRUSION screw wear, and how to avoid them PM# 40065710
K 2022 wrap-up
contents NOVEMBER 2022 VOLUME 81 • NUMBER 5
FROM THE ARCHIVES
The December 1967 issue of Canadian Plastics reported on the largest-ever chemical tank constructed of reinforced plastics. The tank was filament-wound on-site for an unnamed chemical company in West Virginia, and held 250,000 gallons of hydrochloric acid. It had a diameter of 46 feet, a shell height of 20 feet, and an overall height of 26 feet. In the winding process, continuous glass-fibre filament was run through a polyester bath, then on to the rotating mandrel. About 22,000 pounds of glass-fibre laminate went into the tank, which replaced a rubber-lined steel tank that had been previously used.
10
Number of the month:
176,000*
* Approximate number of visitors to the K 2022 trade show in Düsseldorf, Germany. (See pg. 6)
17
19
Cover Photo Credit: © Igor / Adobe Stock
cover story 4
Editor’s View: Two big problems still linger
5
Ideas & Innovations: A new soft polymer material is capable of ‘thinking’
6
News: • K 2022 attendance slips 21 per cent from 2019 • New ownership for Barway Plastic Equipment • Wavin acquires Montreal’s Bow Plumbing Group • Supplier News and People
10 RECYCLING: What do we do about PPE waste?
The pandemic wasn’t just a healthcare crisis but also an environmental crisis. International organizations and countries purchased and used billions of masks and other PPEs in response to COVID-19, with little attention given to safe management of medical waste. But as mountains of disposable masks and other litter continue to pile up, some recyclers and government agencies are stepping up.
features
15 K 2022 WRAP-UP: Canadians show off at K
From throughout the Great White North all the way to Düsseldorf, Germany, these Canadian exhibitors came to promote their technologies.
19 EXTRUSION: The turn of the screw
The main causes of extrusion feedscrew wear and what to do about them.
24 SIZE REDUCTION: Size reduction FAQs 27 Technology Showcase 29 Advertising Index
We asked some shredder and granulator makers about the most common plastic size reduction questions they get from their customers, and how they answered. Here’s what they told us.
30 Technical Tips: Five questions to ask before instrumenting a mold
Visit us at www.canplastics.com November 2022 Canadian Plastics
3
Canadian Plastics magazine reports on and interprets developments in plastics markets and technologies worldwide for plastics processors, moldmakers and end-users based in Canada.
editor’s view
www.canplastics.com
Two big problems still linger
A
s we head into 2023, the pandemic is largely over, but like a massive storm finally moving off, it’s left behind a ravaged landscape. And the manufacturing sector is definitely showing signs of the hit, particularly with supply chain disruptions and skills/ labour shortages. The latter has been a problem for so long that by now it feels almost like part of the DNA of plastics manufacturing. After all, manufacturing hasn’t been the most attractive labour sector in Canada for a decade. According to Statistics Canada, the manufacturing labour market hit the peak of its last boom cycle between 2000 and 2003 but then plunged by half a million jobs from 2004 to 2008, and hasn’t experienced another boom cycle since. And the pandemic, characterized by forcibly lowered productivity, made the problem much worse. Between February and April 2020, Canada’s manufacturing sector lost over 280,000 jobs — a 17 per cent drop in employment compared to 16 per cent in the country’s general labour force. A study by the Excellence in Manufacturing Consortium found that, as of May 2020, the lack of available candidates with the right skills inhibited manufacturing output by more than 20 per cent, representing $98.4 billion in unfilled orders. Manufacturers had to turn down new orders because they were unable to fill them. Since the beginning of this year, however, Canada’s manufacturing sector has continued to grow, with increases in output, new orders, purchases, and employment. But not necessarily skilled employment. To close the skills gap, companies are investing in the current workforce through upskilling and increasing wages, but they’ve been doing that for years now and still haven’t replaced the retiring baby boomers. For some shops, automation is a permanent solution, but for most others the prob-
4 Canadian Plastics November 2022
lem remains unsolved. The supply chain problem is far newer, of course, and definitely brought on by the pandemic. China is still shutting down huge sectors of its society to stop the spread of the virus, thereby slowing the manufacturing of all sorts of goods upon which worldwide industry relies. But that’s not the whole story. In retrospect, the entire global supply chain was a Jenga-block tower poised to come crashing down. A decades-long focus on supply chain optimization to minimize costs, reduce inventories, and drive up asset utilization has removed buffers and flexibility to absorb disruptions – COVID-19 simply illustrated that many companies weren’t fully aware of the vulnerability of their supply chain relationships to global shocks. A recent survey of North American supply chain executives found that more than half don’t expect a return to a “normal” supply chain until the first half of 2024 or beyond, while 22 per cent expect disruptions to continue until the second half of 2023. When asked what “magic levers” could bring supply chain costs under control and help mitigate uncertainty, the leading responses were: an end to the war in Ukraine, cited by 32 per cent; lowering fuel costs, 31 per cent; outlawing supply chain profiteering/corruption, 21 per cent; and raising interest rates quickly and significantly to halt inflation, 10 per cent. One conclusion we can draw from the experts is that there are no silver bullets or flip-a-switch solutions due to the complexity and dynamics of the situation. Coming out of it will take time, and we can hope to see incremental improvements over several months. But for now, again, it remains ongoing and unsolved. On the plus side, there’s no doubt our industry will eventually solve both these issues – solving problems is, after all, what we do best.
Reader Service Print and digital subscription inquiries or changes, please contact Angelita Potal Tel: 416-510-5113 Fax: 416-510-6875 email: apotal@annexbusinessmedia.com Mail: 111 Gordon Baker Rd., Suite 400 Toronto, ON M2H 3R1 EDITOR Mark Stephen 416-510-5110 Fax: 416-442-2230 mstephen@canplastics.com ASSOCIATE PUBLISHER Stephen Kranabetter C: 416-561-5362 W: 416-510-6791 skranabetter@annexbusinessmedia.com MEDIA DESIGNER Lisa Zambri lzambri@annexbusinessmedia.com ACCOUNT COORDINATOR Cheryl Fisher 416-510-5194 cfisher@annexbusinessmedia.com AUDIENCE DEVELOPMENT MANAGER Serina Dingeldein 416-510-5124 sdingeldein@annexbusinessmedia.com GROUP PUBLISHER/VP SALES Martin McAnulty mmcanulty@annexbusinessmedia.com COO Scott Jamieson sjamieson@annexbusinessmedia.com PRINTED IN CANADA ISSN 008-4778 (Print) ISSN 1923-3671 (Online) Publication Mail Agreement #40065710 2022 SUBSCRIPTION RATES 5 issues Canadian Plastics, plus Dec. 2022 Buyers’ Guide: CANADA: 1 Year $77.50 plus applicable taxes; 2 Years $123.50+ taxes USA: $176.00 (CAD) / year FOREIGN: $201.00 (CAD) / year
Occasionally, Canadian Plastics will mail information on behalf of industry related groups whose products and services we believe could be of interest to you. If you prefer not to receive this information, please contact our audience development department in any of the four ways listed above. Annex Privacy Officer privacy@annexbusinessmedia.com • Tel: 800-668-2374 No part of the editorial content of this publication can be reprinted without the publisher’s written permission ©2022 Annex Business Media. All rights reserved. Opinions expressed in this magazine are not necessarily those of the editor or the publisher. No liability is assumed for errors or omissions. All advertising is subject to the publisher’s approval. Such approval does not imply any endorsement of the products or services advertised. Publisher reserves the right to refuse advertising that does not meet the standards of the publication. MEMBER: Magazines Canada, Canadian Plastics Industry Association.
Mark Stephen, editor
mstephen@canplastics.com www.canplastics.com
ideas & innovations
A new soft polymer material is capable of ‘thinking’
Photo Credit: Kelby Hochreither/Penn State. All Rights Reserved.
R
esearchers in the U.S. have developed a soft polymer material that can “think” about what’s happening around it by sensing and responding to mechanical stress without – as is usual – requiring additional circuits to process such signals. Developed by collaborators from Penn State University in State College, Pa., and the U.S. Air Force, the technology hinges on a novel, reconfigurable alternative to integrated circuits. For the layperson, integrated circuits are science’s current best approximation of information processing similar to the brain’s role in the human body. Integrated circuits are typically composed of multiple electronic components housed on a single semiconductor material, usually silicon, and they run all types of modern electronics, including phones, cars, and robots. According to principal investigator Ryan Harne of Penn State, integrated circuits are the core constituent needed for scalable computing of signals and information, but have never before been realized by scientists in any composition other than silicon semiconductors. Until now. Harne’s team has now used integrated circuits in a soft polymer material that acts like a brain that can receive and process digital strings of information, resulting in new sequences of digital information that can control reactions: when the material receives external stimuli, it translates the input into electrical information that is then processed to create output signals. “We’ve created the first example of an engineering material that can simultaneously sense, think, and act upon mechanical stress without requiring additional circuits to process such signals,” Harne said. The technology builds upon previous work to develop the novel material that stretches back over decades, including using information from a 1938 paper that described a way to create an integrated circuit by constructing mechanicalelectrical switching networks. Harne and his team had already developed a soft, mechanical metamaterial that could “think” about how forces are applied to it and respond using programmed materials, which was outlined last year in a paper published in Nature Communications. That material, however, could only operate on binary input-output signals, not compute high-level logical operations, Harne said; the new material goes much further in functionality thanks to the inclusion of reconfigurable circuits, and can use mechanical force to compute complex arithmetic, detect radio frequencies to communicate specific light signals, and even realize combinational logic. The researchers are now evolving the material to process visual information in the same way that it does physical signals. “We’re currently translating this into a means of ‘seeing’ to augment the sense of ‘touching’ that we’ve presently created,” Harne said. “Our goal is to develop a material that dem-
Penn State researchers have created mechanical integrated circuit materials from conductive and non-conductive rubber materials that sense and react to tactile input, such as force.
onstrates autonomous navigation through an environment by seeing signs, following them, and maneuvering out of the way of adverse mechanical force, such as something stepping on it.” According to Harne, the material has potential applications in autonomous search and rescue systems; infrastructure repairs; and even bio-hybrid materials that can identify, isolate, and neutralize airborne pathogens. CPL
PCS_MinLube_CP_QtrPg_101722.indd 1 CPL_PCS_Nov22.indd 1
November 2022 Canadian Plastics
5
10/17/22 12:50 PM 2022-10-18 2:06 PM
news
Photo Credit: Messe Düsseldorf
K 2022 attendance slips 21 per cent from 2019
A
pproximately 176,000 visitors came to K 2022 in Düsseldorf, Germany from Oct. 19-26 – the first major international plastics show since the start of the COVID-19 pandemic – which was a drop of about 21 per cent compared with the last show in 2019. Next to Germany, most European visitors came from the Netherlands, Italy, Turkey, France, Belgium, Poland, and Spain. The number of visitors from the East Asian region, China in particular, was down due to quarantine regulations in those nations. About 42 per cent of visitors came from overseas, show organizers said, which is nearly identical to the percentage in 2019. According to polling taken of attendees, around twothirds of all visitors ranked machinery and plant construction first in terms of interest. Fifty-seven per cent said they were interested in raw and auxiliary materials, with recyclates and bioplastics being particularly popular. For 28 per cent, semifinished products and technical parts made of plastics and rubber were the main reason for coming. And over 70 per cent of all visitors came from top and middle management.
For K 2022, the amount of exhibition space actually increased compared with 2019 even though the total number of exhibitors fell slightly. A total of 3,037 exhibitors – including about 20 Canadian companies – took 178,965 square meters, or 1,926,363 square feet, in 2022. That compares with 3,327 exhibitors that used 177,035 square meters, or 1,905,589 square feet, in 2019, organizers said. The big change from 2019 on the exhibitor front is that there were no Russian exhibitors at this year’s show due to the invasion of Ukraine. K is held every three years, and the 2022 show marked the 70th anniversary. The next K is scheduled for Oct. 8-15, 2025. CPL
A
well-known machinery and equipment sales firm in Canada’s plastics sector is now under new ownership. Barway Plastic Equipment Inc., headquartered in Vaudreuil-Dorion, Quebec, has been supplying the plastics industry for almost 30 years, since its founding in 1993 by industry veteran Wayne Hart. Barway serves plastics processers in Eastern Ontario, Quebec, and the Maritimes by representing Haitian Corp. and Zhafir Plastics Machinery, and also addresses processor needs with access to other major equipment suppliers such as Advantage Engineering, BinMaster, Kongskilde, Lorenz Conveying Products, Maguire Products, Munchy, Novatec Inc., Rotogran International Inc., Star Automation, and TEC. And Barway also offers a full line of its own silos. Hart sold the company in July of this year to machinery installation specialist Marc Viau and his sons Alex and Antoine. Marc Viau now serves as Barway’s president, and Alex and
6 Canadian Plastics November 2022
Barway’s new owners also operate a machinery installation and servicing company.
Antoine are both vice presidents. The Viau family had worked with Barway for years as a contractor for the installation of equipment and silos through Saint Zotique, Que.-based Mecanique Industrielle M.M.V. Inc., a machinery installation and servicing company founded by Marc Viau over 25 years ago. “We had developed a good relationship with Wayne through our installation business, and when he announced his plans to sell, he offered me the chance to buy Barway and I
accepted,” Marc Viau said. “My sons now run Barway with me, so it’s completely family-owned. My sons started working at Barway in October 2021 in order to become more familiar with the business before we bought it, and they’re now totally up to speed.” Barway will continue to represent all of the existing machinery lines, Marc Viau said, but will also add installation services courtesy of M.M.V. “Barway customers can now have both the new equipment and the installation,” he said. And the new Barway is also offering modification and fabrication of custom metal parts for all industries in its fabrication location in Saint Zotique, he added. So, it’s not quite the same Barway as you might remember. “I handle all of the on-road sales, Peter Booth handles our inside sales, and we’re looking to add another salesperson for the road,” Marc Viau said. “The Barway name is well established, but we’re a young company again and we’re looking to grow as quickly as possible.” CPL www.canplastics.com
Photo Credit: Mecanique Industrielle M.M.V. Inc.
New ownership for Barway Plastic Equipment
Wavin acquires Montreal’s Bow Plumbing Group
Conduit extruder Dura-Line building new plant in Alberta
I
C
n a move that gives it a presence in the North American residential and commercial construction industry, Netherlands-based building products maker Wavin BV has bought Bow Plumbing Group, a manufacturer of plastic pipes and fittings headquartered in Montreal. The financial terms of the deal have not been disclosed. Founded in 1939, Bow produces full product lines of drainage and pressure plumbing for commercial and residential applications in a range of plastic materials, including crosslinked polyethylene (PEX), chlorinated polyvinyl chloride (CPVC), ABS, and PVC. The firm has local manufacturing in Quebec, and warehouses and commercial reach across Canada and the U.S. “[Our] investment in the Bow Plumbing Group strengthens and extends [our] presence in this important market,” Wavin officials said in a Sept. 1 statement. “Bow’s reputation for excellence in plastic pipes and fittings will complement [our] full spectrum of offerings for drinking water, wastewater, and rainwater management.” As part of the acquisition, Gilles Cyr, the former CEO of Bow, has been named as the general manager of Wavin’s new business in Canada. CPL
onduit extruder DuraLine Ltd. is building a 150, 0 0 0 -squa re-foot manufacturing plant in St. Albert, Alta., a suburb of Edmonton. The Knoxville, Tenn.-based company, which is a business unit of Orbia Advance The front of the new St. Albert Corp. SAB de CV Mexico, facility. has already begun construction on the new facility, which is scheduled to be fully operational by spring of 2023. The firm plans to hire as many as 90 new full-time employees. Founded in 1971, Dura-Line makes HDPE conduit with smooth, ribbed, and corrugated walls; microducts with outer diameters from 5 to 22 millimeters; and bundled microducts with an oversheath. The products provide protective pathways for wires and cables that resist extreme temperatures, chemicals, and corrosion. The company has 17 manufacturing facilities employing 1,700 people in the U.S., Canada, India, Oman, and Europe, as well as a global sales and distribution network. CPL
MANUFACTURING AGILITY WITH THE ZERES III SERIES
Photo Credit: Dura-Line Ltd.
news
www.absolutehaitian.com
The Zhafir Zeres III electric injection molding machine from Haitian advances plant floor flexibility and productivity. • Electric precision where you need it • Integrated hydraulics for core pull, ejectors, carriage movement, optional valve gates • No need for hydraulic power pack • Quiet with up to 80% energy savings • 10% lower cost on average than full electric machines • 44 to 1,551 U.S. tons and a wide range of injection units Looking for higher productivity per square foot? Talk to our sales engineers to learn more at 216-452-1000 or 508-459-5372.
FLEXIBILITY WITH TECHNOLOGY TO THE POINT November 2022 Canadian Plastics CPL_Absolute_Nov22.indd 1
7
2022-10-20 3:29 PM
news
Canadian Plastics golf
SUPPLIER NEWS – Cranberry Township, Pa.based auxiliary equipment maker Conair Group has appointed Auxiplast Inc. as its new sales representative for Quebec and Atlantic Canada. Founded in 1994, Auxiplast is headquartered in Varennes, Quebec, and is headed by Jean-François Continelli and David Marois.
A
pproximately 75 golfers turned out for the first Canadian Plastics fall golf tournament at Royal Stouffville Golf Course in Stouffville, Ont., on Sept. 29. The Texas Scramble event kicked off at 11:00 am followed by dinner and trophy presentations and prize draws. Prizes included low team gross, closest to the pin, and longest drive. Despite some close shots, the $10,000 hole-in-one prize on the 18th hole went unclaimed. Canadian Plastics would like to thank tournament sponsors Absolute Haitian, AceTronic Industrial Controls, Chillers Inc., Hasco Canada, Nylene, PCS Co., Pounds of Plastic, Stäubli, and Wittmann Battenfeld Canada. CPL
From left: Dave Carter (M.B.C. Rotomould Inc.), Dave Taylor (Techstar Plastics), Adam Carter (M.B.C. Rotomould), Kim Thiara (AceTronic Industrial Controls) and Ron Keilhauer (M.B.C. Rotomould) on the hole-in-one 18th hole.
PEOPLE
Tasos Pourloukakis
Jonatas Melo
Robert Bunting
Clayton Tyler
Brian Larkin
Raje Dwaraka
Travis Smith
Vanessa Malena
Rolfe Olsen
Mike Gunner
Rebecca Liebert
Alfredo Santa
Danny Dweik
Dan Gallo
Gary Riley
Simon Medley
– McDonough, Ga.-based packaging supplier Alpla Group has named Tasos Pourloukakis as regional managing director for North America. - Material supplier Borealis AG has named Jonatas Melo as vice president of performance materials. - Newton, Kan.-based Bunting, which designs and manufactures magnetic separation, detection, and materials handling equipment, has named Robert Bunting as president and CEO. - McHenry, Ill.-based additives maker Chroma Color Corp. has named Clayton Tyler as sales director. - Medical device and packaging supplier Comar, headquartered in Voorhees, N.J., has named Brian Larkin as president and CEO. - Pawcatuck, Conn.-based extrusion machinery maker Davis-Standard LLC has named Raje Dwaraka as chief financial officer. - Kingsport, Tenn.-based Eastman Chemical Co. has named Travis Smith as senior vice president, additives and functional products. - York, Pa.-based Engel Machinery Inc., the North American subsidiary of Austrian injection molding machine builder Engel Holding GmbH, has named Vanessa Malena as president.
8 Canadian Plastics November 2022
- Blow molder Graham Packaging Co. Inc., based in Lancaster, Pa., has named Rolfe Olsen as president of beverages. - Machinery maker KraussMaffei Corp., headquartered in Florence, Ky., has named Mike Gunner as automation vice president. - Specialty chemical maker Lubrizol Corp., headquartered in Wickliffe, Ohio, has appointed Rebecca Liebert as president and CEO. - Film and sheet extrusion systems supplier Macro Engineering & Technology Inc., based in Mississauga, Ont., has named Alfredo Santa as area sales manager for Canada and Latin America. - Calgary-based materials maker Nova Chemicals Corp. has appointed Danny Dweik as interim CEO. - St. Louis, Mo.-based Spartech, a manufacturer of engineered thermoplastics and custom packaging solutions, has appointed Dan Gallo as chief operating officer. - Tecumseh, Mich.-based Uniloy Inc., a manufacturer of blow molding equipment, parts, and tooling, has appointed Gary Riley as CEO. - Independence, Ohio-based material supplier Valtris Specialty Chemicals has named Simon Medley as CEO.
www.canplastics.com
DECEMBER BUYERS’ GUIDE Canadian Plastics 2023 Annual Buyers’ Guide will be published and mailed in December. The Guide is your essential resource for Canada’s Plastics Industry. Access information on companies and contacts within the following categories: Mold, Tool and Die Makers Machinery Manufacturers Raw Material Suppliers Moldmaking Components, Equipment, Supplies & Services Processors & Products Services Associations If you are not currently part of our Buyers’ Guide and would like to be added, please contact Stephen Kranabetter at skranabetter@canplastics.com
FEBRUARY 2023 ISSUE Here’s an early look at what’s inside the upcoming February 2023 issue of Canadian Plastics magazine: The cover story will be on injection molding. The K 2022 trade show may be over, but it’s not forgotten. The key themes in new injection molding at K were digitization, climate protection, and the circular economy. Here’s what the IMM makers unveiled to help close the loop. In addition, we’ll also feature articles on • The latest hot runner innovations • How to purge extrusion machinery • Quebec rotational molder Manunor turns 30
recycling
WHAT DO WE DO ABOUT PPE WASTE?
The pandemic wasn’t just a healthcare crisis but also an environmental crisis. International organizations and countries purchased and used billions of masks and other PPEs in response to COVID-19, with little attention given to safe management of medical waste. But as mountains of disposable masks and other litter continue to pile up, some recyclers and government agencies are stepping up. By Mark Stephen, editor
S
ometimes the solution to a problem can cause other problems down the road. To date, the COVID-19 pandemic has claimed some 6.5 million lives, a number that would probably have been higher but for the personal protective equipment (PPE) worn by billions of people that helped slow the spread of the virus. But these PPEs have produced a crisis of a different sort: all the surgical masks, N95 masks, gloves, and other single-use items that have been thrown away.
10 Canadian Plastics November 2022
Since the onset of the crisis in early 2020, demand for PPEs both within and beyond the health sector has skyrocketed. Each month from March 2020 to March 2022, an estimated 129 billion face masks – three million a minute, or 50,000 every second – and 65 billion gloves were used worldwide by healthcare workers and the general public. Other PPEs include surgical gowns, hair and beard nets, shoe covers, plastic wrap, shields, sheeting, sanitizing equipment, garments, test kits, and more.
All of this translates into an almost unbelievable amount of waste, virtually all of it containing plastic. One study shows that more than eight million tons of pandemic-associated plastic waste has been generated globally, with more than 25,000 tons entering the global ocean. In Canada, meanwhile, an estimated 63,000 tons of PPE waste ended up in our landfills between June 2020 and June 2021, with a smaller portion being incinerated due to biomedical contamination. Most disposable PPE is designed for single-use applications and consists of petroleum-based, nonbiodegradable polymers. Disposable masks, for instance, may feel like soft cotton, but they’re almost all made from non-biodegradable material such as polypropylene (PP). PPE waste like masks escapes waste streams to become litter in a variety of ways, mainly either by being flushed down the toilet or simply discarded on the street. From there, it gets washed into storm drains, many of which empty straight into streams, lakes or the ocean, adding to the already serious problem of microplastics and other plastic litter found in oceans and on land. Which is why the scientists behind the statistics predict that almost all pandemic-associated plastic litter escaping from the waste stream will eventually end up on the seabed or beaches. Even when PPE waste is disposed of properly within the waste stream, the results aren’t ideal. In most jurisdictions, the stream coming from hospitals and long-term care facilities is deemed Category B waste – tainted by infectious substances – which means it can’t be sent through municipal recycling facilities. Nor can PPEs be recycled through mainstream or curbside recycling programs because the recycling process is so complex; in most municipal systems – which combine physical and biological processes – there’s no way to separate the mixture of polymers contained in these products. Instead, the vast majority of PPE disposed in the Canadian healthcare system, and most other systems, is treated as non-dangerous general solid www.canplastics.com
Photo Credit: © Igor / Adobe Stock
MOUNTAINS OF GARBAGE
recycling waste, and ultimately landfilled. The remainder is treated as biomedical solid waste and is either disinfected and landfilled or incinerated. But these methods have their own drawbacks. Landfill sites have existed for decades all over the world, of course, but the rubbish buried in them decomposes very slowly, making them a problem for future generations; and landfills produce secondary side effects as well, including methane emissions, unpleasant views, and rat and seagull infestations which create their own waste problems. And many countries – Canada and the U.S. included – do not handle all of their recycling and waste domestically, instead shipping tonnes of waste overseas. Incineration, meanwhile, produces climate-warming carbon emissions, and also releases toxic air pollutants such as dioxins, furans, mercury, and polychlorinated biphenyls into the atmosphere. There’s also just too much of the litter – hospitals in
Wuhan, China alone burned through 240 tons of single-use PPE every day at the height of the pandemic and barely made a dent in that city’s influx.
A LOW PRIORITY
Unlike the outbreak of the pandemic, the accumulation of PPE waste was predictable. Even as they mandated maskwearing, governments all over the world were aware that the discarded masks and other PPE waste would accumulate very quickly, but at the outset of the pandemic, as institutions scrambled to carry out measures to protect overwhelmed healthcare systems from collapse, initiatives to deal with this waste weren’t prioritized. Now, however, enough time has gone by – and enough discarded masks have been seen blowing around parks and city streets and floating in rivers and seas by enough people – for the problem to gain prominence, with growing calls to develop policies, programs, and innovations to safely reduce these
primarily plastic items. But there are difficulties. First, even before the pandemic, the treatment of plastic waste wasn’t keeping up with the increased demand for plastic products, and postpandemic PPE litter has added immeasurably to the problem – waste management and handling systems have limited capacity designed primarily based on pre-COVID-19 patterns of biomedical waste generation. Pandemic epicentres in particular struggle to process the waste. And second, because of its multimaterial structure and potential contamination by biohazards, waste PPE isn’t currently recycled using such conventional mechanical recycling technologies as grinding, washing, separating, drying, re-granulating, and compounding. So, two years after the WHO officially labeled COVID-19 a pandemic in March 2020, and countless tons of accumulated PPE pollution later, what do we
November 2022 Canadian Plastics CPL_Struktol_Sept21.indd 11 CPL_Struktol_Nov22.indd
11
2021-08-19 3:31 2022-08-09 2:47 PM
Photo Credit: Vitacore Industries Inc.
recycling
Vitacore Industries provides PPE recycling bins at long-term care and urgent care facilities at no cost.
do with all of this waste? We start with the realization that, while posing some challenges, reusing PPE is actually a huge area for growth. In Canada as elsewhere, government agencies, universities, and private sector firms are collaborating on an array of projects aimed at implementing recycling initiatives and developing reusable options for PPE.
FIRST OUT OF THE GATE
In February 2021, Canada’s first recycling program for singleuse masks and respirators was launched in long-term care and urgent care facilities across Vancouver. The program was created through a partnership between Vancouver-based medical supply maker Vitacore Industries Inc., McMaster University in Hamilton, Ont., and the University of British Columbia, and provides PPE recycling bins at long-term care and urgent care facilities at no cost. Once collected, the PPEs are sterilized by Vitacore before being sent to McMaster to be broken down and repelletized into PP for use as construction materials to reinforce concrete or as siding for buildings. And McMaster researchers are looking into ways to expand the possible uses for the repelletized materials. “The PP used in most masks and respirators is of very high quality, so it’s worth trying to recapture, and we’ve been able to divert a significant number of PPEs from landfill or incineration,” said Vitacore president Mikhail Moore. “One challenge to recycling PPEs is separating the various materials, such as aluminum from PP in masks, and we’ve created an automated process to do that.” A second recycling challenge, Moore continued, is to remove pathogens. “We know what type of PPE and what type of plastic we’re receiving in collected PPEs from hospitals, but we
12 Canadian Plastics November 2022
don’t know what kinds of pathogens or other biological contaminants there might be,” he said. “Going through a sanitation protocol to remove those pathogens is a very important part of PPE recycling. The catch at this point is that the sanitization process degrades the polymers slightly, but that step is being refined and we’re getting to the point where our endproduct is comparable to other recycled polymers that are suitable for non-medical, non-food contact applications.” Also in 2021, Brantford, Ont.-based chemical recycling firm GreenMantra Technologies Ltd. received $300,000 from the federal government to develop solutions for efficient and cost-effective recycling of disposable PPE waste. GreenMantra said it will take single-use PPE from Canadian hospitals as a feedstock and use a proprietary process to heat the material in the presence of a catalyst to produce waxes and specialty polymers. The company said its process produces specialty polymers that can be used as additives in construction materials like asphalt, roofing shingles, drainage pipes, and plastic lumber, replacing fossil fuel-based additives. “The goal is to develop a stream of feedstock that can be used within our existing and future commercial-scale advanced recycling facilities,” said Domenic Di Mondo, GreenMantra’s chief commercial officer. “This will be on the scale of millions of pounds per year of diverted PPE with the potential to increase to tens of millions of pounds.” The grant is part of a federal program, called Innovative Solutions Canada, to invest in solutions to challenges from the pandemic, in this case large amounts of hard-to-recycle PPE such as medical masks, surgical gowns, and respirators made with plastics.
TERRACYCLE TUNES IN
Waste management company TerraCycle, headquartered in Trenton, N.J., has been involved in recycling PPEs since long before the pandemic, and has been offering its Zero Waste Box recycling solution – where people can drop off single-use PPE items such as gloves and face masks – since the early days of the crisis. The boxes can be found in numerous public spaces and shops throughout North America and the UK; and in Canada, authorities in the Quebec cities of Vaudreuil-Dorion and Pointe-Claire have set up boxes at various locations, as has Humber College at its North and Lakeshore campuses in Ontario. When full, the boxes are returned to TerraCycle for processing and the collected PPE waste is first aggregated before being cleaned and melted into pellets. The resulting recycled pellet material can then be used by third-parties to manufacture a variety of new products, including outdoor furniture, plastic shipping pallets, outdoor decking, watering cans, storage containers, bins, and tubes for construction applications. According to TerraCyle president and CEO Tom Szaky, different programs are in place to sort different types of PPEs into different waste streams for different recycling processes for different end-products. “The face masks, which are primarily PP, can be reduced to a material that can be used for extrusion products, plastic decking, for example,” he said. “Elastomers, meanwhile, are ground down and then mixed with recycled plastics as an additive to provide a flexibility in www.canplastics.com
recycling
an end-product. With plastic latex gloves, we separate the latex and nitrile – because those two materials are hard to mix together – and the end materials can go into flooring applications. The metals in the nose strips, which require magnets for separation, are used in barstock or metal sheeting.” According to Szaky, approximately 90 per cent of TerraCycle’s PPE recycling uses mechanical recycling – which is the process of reducing plastic waste into secondary raw material or products without significantly changing the chemical structure of the material – with the rest being chemically recycled, which does change the chemical structure by turning plastic polymers back into individual monomers for repolymerization. Some regulations dictate what the Zero Waste Box program can and cannot collect, he continued, but otherwise the company works out its protocols on its own with its clients.
“Mainly, we’re not allowed to collect PPE from a hospital environment because of contamination issues,” Szaky said. “Other types of contamination aren’t related to COVID-19 but are facility-related instead, and in these cases we work with the facilities to understand what those contaminants are – for example, paint from a body shop – and then we put protocols in place for that particular situation and that type of contamination.”
ALL ABOUT PYROLYSIS
TerraCycle’s reliance on mechanical recycling for PPE is common among PPE recyclers, but there is some momentum growing behind a type of chemical recycling called pyrolysis, which is a waste-to-energy temperature reaction that reduces PPE to chemicals, resins, oil, propane, ethylene, and other fuels, and which involves no incineration or landfill use. Researchers at Cornell Uni-
versity in Ithaca, N.Y., for example, are initiating a pilot project in New York state that will collect waste PPE from hospitals and medical centres and then send it to decontamination facilities in New York or Suffolk counties. There, it will be shredded, sterilized, and dehydrated to become small particles, and then brought to an integrated pyrolysis plant, like one contemplated for Rockland County, north of New York City. According to the researchers, the medium-temperature pyrolysis – about 650°C or 1,200°F – can deconstruct the plasticized gowns and gloves, which are derived from petroleum, into chemicals such as ethylene, butane, gasoline, bauxite, propane, diesel, light naphtha, and sulfur. Using a different principle, meanwhile, a team from Swansea University in Wales has developed a process that breaks down the plastic in PPEs into hydrogen using only sunlight. Photore-
Fiberglass Cooling Towers are Economical & Built to Last
Advantage Engineering’s Newest Non-rusting Fiberglass Evaporative Cooling Towers provide one of the lowest costs of cooling per ton compared with other cooling systems such as chillers & fluid coolers. Cooling towers and systems by Advantage Engineering are economical, easy to install and simple to operate. • 45 – 270 ton cooling capacity • • All fiberglass construction for long life • • Low maintenance direct drive fan • • 10 year shell & 5 year mechanical warranty •
525 East Stop 18 Road Greenwood IN USA
317-887-0729
Chillers Inc of Newmarket Ontario is the exclusive representative of Advantage products in Canada.
Learn more
Solely focused on process water cooling systems November 2022 Canadian Plastics CPL_Chillers_Nov22.indd 1
13
2022-10-31 3:11 PM
recycling
STRUCTURAL CHANGES
As of the fall of 2022, the worst of the pandemic is hopefully behind us and it seems clear already that COVID-19 is a primary catalyst for both short- and long-term changes in plastic waste management systems and technologies. In some cases, the jury is still out on these changes. “In Europe and North America, new recycling players are getting into the PPE business, but the important question is, how consistent is the supply and can you build a stable business from it?” said Tom Szaky. “TerraCyle had a facility and process in place before the pandemic, and the pandemic doubled our supply, but we don’t know how long this boost is going to last. I think the levels of PPE being available for recycling will come down as overall demand for PPE falls, but probably not to a pre-pandemic level – we had baseline growth before the pandemic anyway, and going forward a certain percentage of people will decide they feel more comfortable wearing masks in public for good.” And while PPE usage might decline, there still remains a massive amount of waste products going unrecycled, even now. “It’s estimated that about 99 per cent of PPE waste is still going to either landfill or incineration,” Mikhail Moore said. “It’s a very big problem – our program was able to recover 33,000 kilograms last year, which is the equivalent of 8.8 million masks. This is a good start, but the scale of the problem is immense, both in Canada and globally.” In the bigger picture, even before the pandemic, an estimated 77 million tonnes of plastic waste were being mismanaged annually; by contributing further to the challenge of managing municipal waste properly – especially in developing countries where resources and infrastructure are largely lacking – COVID-19 has forced the world to reckon with the gaps and neglected aspects of the waste stream and how we produce, use, and discard our healthcare resources from cradle to grave. But this is why another legacy of the pandemic might be a more efficient plastics recycling sector, resulting from both large-scale government investment in recycling infrastructure contained in recovery packages and recycling companies’ own streamlining. “What PPE related to COVID-19 shows us is that certain waste streams will index up and down, as opposed to traditional plastics recycling, which is good at creating baseline infrastructure but not very good at being malleable to ebbs and flows,” Tom Szaky said. “So, I hope that one of the muscles that gets developed is the ability to grow a supply CPL chain and then reduce it when necessary.”
14 Canadian Plastics November 2022
PUSHING THE ENVELOPE WITH WASTE PPE The range of what recycled PPE polymers can be used for is being expanded rapidly. Here’s a look at what some innovators have done to recapture the plastic from discarded face masks. • Researchers from RMIT University in Australia have proposed using the material from three million disposable face masks to make one kilometre of a two-lane road, preventing 93 tonnes of waste from going to landfill. The new road-making material is a mix of shredded single-use masks and processed building rubble designed to meet civil engineering safety standards, and studies found shredded PPE can increase the strength of the pavement by up to 22 per cent and improve resistance to cracking. • France-based startup Plaxtil collected 70,000 masks last year, melding them into a new type of plastic called “Plaxtil” that can be made into visors, textile products, and even school supplies like protractors, rulers, and triangles for geometry kits. • A team of scientists from the National University of Science and Technology in Russia along with “Plaxtil” plastic. colleagues from the U.S. and Mexico has come up with a novel method of turning used masks into low-cost, flexible, disposable, and efficient batteries, with the masks being compressed and heated up to 140°C, or 285°F, to form pellets to work as the electrodes of the battery. The new batteries can be used in household appliances from clocks to lamps. • In India, a project developed by a company called Shayya – meaning “bed” in Sanskrit – turned scraps of waste PPE into cheap, lightweight mattresses for use in COVID-19 care centres. • Specialized thermal heating machines which convert used PPE into reusable plastic blocks within one hour have been installed inside five National Health Service hospitals in the UK. Developed by Welsh company Thermal Compaction Group, the machines thermally compact the polypropylene in PPEs at 350°C, or 660°F, into one-metre rectangular blocks on-site; the blocks are then collected, processed, and reengineered into items like chairs, garbage bins, and bottle caps.
Photo Credit: Plaxtil
forming uses nanostructured semiconductors and light to degrade the plastic and any virus attached to it. The byproducts are hydrogen and chemical feedstocks, which can be reused by the chemical industry. No greenhouse gases are produced, the researchers say, and the process is cheap and easy enough to be used by rich and poor countries alike. Research is still at an early stage, but the researchers see the technology as a way to tackle disposable face masks and other hospital waste.
k 2022 wrap-up
CANADIANS SHOW OFF AT
From throughout the Great White North all the way to Düsseldorf, Germany, these Canadian exhibitors came to promote their technologies. By Mark Stephen, editor
Checking out the GN800 thermoformer at the BMG booth.
W
hen K 2022 opened on Oct. 19 in Düsseldorf, Germany, it was the first global plastics trade show held since the COVID-19 pandemic began. Other than that, it was business as usual in most ways – which is a good thing. And as usual, Canadian exhibi-
tors and attendees numbered among the tens of thousands of sector members who attended the world’s largest trade fair for the plastics and rubber industry. The completely sold out, eight-day marathon show featured about 3,030 exhibitors from 63 nations, including
about 20 standalone Canadian booths. Not an overwhelming number, perhaps, but it included both well-known heavy hitters and up-and-comers, and others that fell in between. But whether large, mid-size or small, they made their presence felt. Here’s a look, in alphabetical order, at some of the made-in-Canada machineries and technologies presented at the show.
A NEW THERMOFORMER
Thermoforming and packaging equipment maker BMG, which acquired Chester, N.S.-based GN Thermoforming last year, highlighted both its flagship GN800 and its new GN915 highspeed, plug-assist, form-cut-stack thermoformers; its Manti robotic trim press handling system, aimed at handling lids, cups, bowls, and clamshells; and its new NextGen controls, described as an intuitive, easy-to-use HMI platform that simplifies operations and reduces training requirements for new employees. According to BMG vice president of marketing and sales operations Paul Phillips, the new GN915 is well-suited for a variety of product packaging possibilities for the medical, food, and consumer packaged goods industries; is flexible enough to use all thermoformable materials, including those with 100 per cent recycled content and various biodegradable materials like polylactic acid (PLA); and can accommodate tooling designed for other thermoforming machines of its size. BMG ran live demonstrations of both the GN800 and the NextGen controls throughout the show. Brampton. Ont.-based blown film extrusion equipment maker Brampton Engineering Inc. (BE) showcased its AquaFrost water-quenched blown film technology. Designed for 5- to 11-layer blown film systems, AquaFrost offers improved clarity and thermoformability, balance orientation, and increased flexibility with less resins, BE officials said. The company also displayed its FlexWIN bi-directional gap winder that features tapeless transfer with zero foldover. It includes gearless direct-drive servo motors to drive its spindles for precise torque control and energy savNovember 2022 Canadian Plastics
15
k 2022 wrap-up
A section of large-diameter pipe on display at the Corma booth.
Photo Credit : Deacro Industries Ltd.
ings, is able to isolate the winding tension from the upstream web tension, and includes improved precision and range-of-tension control and lay-on pressure. Lachine, Que.-based CDS – Custom Downstream Systems Inc. touted the full range of its downstream plastic extrusion machinery, including complete turnkey systems; die tooling, line control, and automation that monitors and adjusts vacuum levels, temperatures, and speeds; cooling and sizing, including air-cooling tables, cooling tanks, and vacuum calibration tables; pulling machines, including belt and horizontal haul-offs and cleat haul-offs; cutting, including travelling cut-off saws, crosscut saws, and travelling guil-
lotine cutters; combination units with puller and cutter combination unit options; collection machines, including run-off tables, automatic coil winders, and takeaway conveyors; texturizing machines, including embossing and brush scouring; and auxiliary equipment, including lube tanks, strip feeders, preheaters, and pay-offs. Corma Inc., a Torontobased maker of corrugated plastic pipe production systems, presented information about its model 3030 corrugator, which uses vacuum forming technology and accepts vacuum formable materials including PVC, polyethylene, and polypropylene. The machine produces single-wall corrugated pipe; double-wall pipe with corrugated outer walls and smooth inner walls; and triple-wall pipe, produced as a corrugated middle layer between a smooth inner and outer wall. Corma also showcased its model 830 corrugator for pipe sizes between 50 and 300 millimeters.
AN IMPROVEMENT OVER STANDARD SLITTERS
Deacro Industries Ltd., headquartered in Mississauga, Ont., promoted its T610 twin-turret duplex slitter rewinder, which, by allowing the operator to set cores up on the outer rewind mandrels during the slitter run time, is said to give significantly reduced downtime compared to standard slitters. A differential
Deacro’s T610 twin-turret duplex slitter rewinder.
16 Canadian Plastics November 2022
rewind system compensates for web gauge variation, allowing the T610 to rewind non-uniform web constructions. The company also promoted its RS1300 shaftless salvage rewinder, which has a reversible option that Deacro officials described as particularly well-suited for printed web converters since the print direction can be maintained without removing the roll. Drader Manufacturing Industries Ltd., headquartered in Edmonton, showed its Injectiweld handheld plastic welding fabrication kit and repair system. The Injectiweld has interchangeable tips and an automatic feed system that enables a person to use the welder with one hand, and uses radiant heat to thermally bond most types of plastics without the use of hot air or gas. The welding rod is automatically drawn into the gun by a set of rod driver wheels and fed into the connecting tube, where it’s nipped off, packed into the barrel, and melted. The company also promoted its new Drader Injectiweld 425, which booth staff described as extremely compact, lightweight, tough, and reasonably priced. Eagle Vizion Ltd., an optical sorting system maker from Sherbrooke, Que., showcased its Flake Analyzer, which is designed to analyze and control the stream quality of presorted recycled plastics through continuous real-time resin and colour analysis. In lab mode, the Flake Analyzer will help increase accuracy, efficiency, and reliability of sample testings, Eagle staff said; and installed in-line in an industrial recycling process, the unit will validate purity in real-time with continuous sample analysis, customerdefined contaminant thresholds, and automated reaction to purity changes. Kitchener, Ont.-based startup LabsCubed, which manufactures automated testing equipment, displayed its CubeOne automated polymer testing system. The tabletop machine accommodates various sample shapes and sizes, and tests tensile and tear strength. “Compared with vertical universal testing machines, where the technician runs a test, waits, and runs the next test, the CubeOne automates the process,” www.canplastics.com
k 2022 wrap-up
LabsCubed chief technical officer and company co-founder Ammar Jafar with the CubeOne system.
said Ammar Jafar, chief technical officer and co-founder of the company. “The technician loads the tray with samples, loads the tray in the machine, presses start, and can walk away and perform a value-added task rather than wait around.” Once the testing is complete, Jafar continued, the results are uploaded to the cloud, where they can be accessed from anywhere. “And because the process is automated, it’s more consistent and gives you a common base that lets you compare results,” he added. In 2019, the CubeOne system took the top prize at the first Startup Stadium competition at Plast-Ex and the Advanced Design & Manufacturing Expo in Toronto; and in 2020 it won a European Product Design Award.
THE LATEST IN BLOWN FILM
Film and sheet extrusion system maker Macro Engineering & Technology Inc., of Mississauga, promoted its barrier blown film lines – available up to 13 layers, each line is capable of producing a variety of structures using different combinations of resins and layer configurations, and all models are equipped with a patented extrusion die and air ring technology that Macro officials
®
November 2022 Canadian Plastics CPL_Davis_Nov22.indd 1
17
2022-10-04 1:24 PM
said ensures an exceptionally flat film that’s free of gels. The company also promoted its Automax-S surface winders, which are available with a variety of standard features to accommodate a range of winding and roll changing needs; and the revamped MacroPack-TP co-extrusion dies, aimed at smaller diameter multilayer dies, especially for double-bubble/third-bubble technology and wire and coating applications. MMC Packaging Equipment Ltd., of Laval, Que., demonstrated the threein-one Cameleon LM-270Lx lining machine, which features three interchangeable liner insertion technologies for maximum flexibility. The Cameleon combines pre-cut wads, rotary die, and punch and die technologies with beforeand-after peripherals for optimal autonomy, MMC officials said, and also has a proprietary vision system for closure and liner inspection with OCR capabilities for quality assurance and process diagnostics. Mold-Masters, of Georgetown, Ont., showcased a slew of new hot runner systems, controllers, and auxiliary injection units, including the Fusion series G3 nozzles, which feature more compact nozzle bore cut-outs to help minimize tooling requirements and are available in customizable lengths up to 1,000 millimeters; the PET series twostage hot runner system, which is said to be compatible with any major brand of PET-preform mold; the PET series nozzle, with improved thermal profile, field replaceable heater sleeve, and an industry-standard gate design; the EM5 allelectric, servo-driven auxiliary injection unit that offers an expanded shot range of 550 to 1,237 grams (18 to 42 ounces); the Axiom (TG) hot runner system for single-stage PET molders; the Symfill system, designed to minimize core shift to improve part quality (straightness) of cylindrical, centreinjected components having an aggressive L/D ratio; the TempMaster M3 temperature controller, with a “TCConnect” technology that eliminates the need for traditional T/C control cables altogether; and the TempMasterME hot runner temperature controller,
18 Canadian Plastics November 2022
Mold-Masters Fusion series G3 hot runner nozzles.
an easy-to-operate unit aimed at lowcavitation molds of 12 zones maximum. Vancouver-based for-profit social enterprise Plastic Bank made a splash by committing to stop 50 ocean-bound plastic bottles for every K 2022 attendee who pledged to become an “Ocean Steward.” Plastic Bank works with local entrepreneurs in coastal areas to establish plastic collection branches, with community members being paid to collect plastic garbage, which is then processed into Social Plastic feedstock, a recycled plastic material that can be reintegrated into the global manufacturing supply chain. At its booth, Plastic Bank also showcased products and packaging made from this feedstock by global partners such as SC Johnson, Henkel, ScanCom, CartonPack, IVC Group, Promoland-Recycool, Advansa, and Bloem Living.
CUTTING-EDGE RECYCLING
Montreal-based recycler Polystyvert Inc. promoted its polystyrene (PS) recycling technology, which takes plastic waste in its solid form and dissolves it in a solvent. Once dissolved, the process can mechanically and chemically separate contaminants and additives – including a wide range of hard-toremove contaminants such as pigments and brominated flame-retardants –
before separating the original polymer from the solvent. Finally, a PA paste is obtained, which is then devolatized into pellets. The process is effective on all types of PS, from industrial waste to post-consumer streams, and the endproduct is a high-purity polymer that can be used as new raw material resin again, including for food-grade applications. Tooling solutions provider StackTeck Systems Ltd., of Brampton, promoted its collapsing core closure mold technology, which enables the molding of creative packaging solutions, including 360 degrees of internal threads or undercuts as well as containers or closures with smaller neck diameters than the core or body, such as cosmetic jars. According to StackTeck officials, these capabilities enable the injection molding of part designs that would traditionally have been molded via injectionblow or extrusion-blow methods. The company also promoted its new FastTrack program that gives the customer between 8 to 10 weeks delivery by using automated design capabilities that work with a preset, optimized set of mold design rules to reduce the engineering phase of every project from weeks to just a few days. And Top Grade Molds Ltd., of Mississauga, showcased its newest developments in mold technologies, specifically high-performance industrial packaging for pails and buckets, as well as co-injection technology to address post-consumer recycling (PCR) content. Regarding pails and buckets, Top Grade officials said the company is establishing new industry cycle time benchmarks for heavy-wall containers; while for co-injection technology for PCR, the company is working with molders to help satisfy or exceed legislation requirements now or in the near future to utilize recycled material in new products. Top Grade also promoted its X-Tri Seal design, which uses three seals to provide superior barrier protection, has a replaceable nozzle seal for easy maintenance, and replaceable seals available with extra stock for CPL easy gate insert repairs. www.canplastics.com
Photo Credit: Mold-Masters
k 2022 wrap-up
THE TURN OF THE SCREW
extrusion
The main causes of extrusion feedscrew wear and what to do about them.
By Mark Stephen, editor
Photo Credits: All photos courtesy of CPM Extrusion Group
S
ometimes big problems take a long time to develop. Coastal erosion is one; on a much lesser scale, extruder feedscrew wear is another. Along with the barrel, the screw is the main moving part in an extruder, and it must withstand many different wear and corrosion environments depending on the end user. But in many cases, feedscrew wear is generally a slow process that can go unnoticed since minor wear will have little effect on overall performance, as machine parameters can be adjusted to maintain productivity. But when the wear can no longer be ignored – when it reduces the machine’s performance by causing spiking scrap rates, soaring energy consumption, and even catastrophic failure results – it goes from being a minor nuisance into a serious matter for maintenance and engineering departments, and rightfully so. Excessive wear in a plasticating unit poses a litany of serious performance issues, naturally affecting cost and overall quality. The slowness of the wear process aside, a second reason that screw wear can sneak up on an extrusion shop is that many extrusion plants rarely, if ever, pull screws that are performing at the expected performance level in order to record wear. Which means that when melt quality declines to the point that a screw is finally pulled for inspection, it may not be salvageable, forcing longer downtime waiting for new equipment. In too many shops, enormous amounts of repair cost and machine
downtime are often wasted by not understanding the causes of the wear and by not taking steps early on to prevent it before it becomes critical.
THE BIG THREE
Screw wear is serious, but it’s not complicated. The majority of the wear occurs in predictable places: specific areas of high pressure, in particular the transition section and last few turns of metering. And while there are many factors that can cause the screw to wear, all of them relate to three main wear phenomena: abrasive, corrosive, and adhesive. Of the three, abrasive wear is by far the most common, caused by friction between the compound and the screw/barrel surfaces, not unlike tire wear or brake wear on your automobile. “Abrasive wear happens over an extended period of time, not instantaneously,” said Adam Dreiblatt, director, process technology with CPM Extrusion Group. “The nature of the compound formulation – the percentage of pigments, fillers, and reinforcing fibres – and the metallurgy of the screws will determine the time scale for abrasive wear to manifest itself. In some cases, this will occur in a matter of months, and in other cases it can take years.” The root of the problem is the fact the screw doesn’t remain perfectly centred in the barrel over its full length – instead, it moves constantly in that clearance due to varying pressure and torque, which causes continuously moving contact of the screw flights with the barrel liner.
Corrosive wear of screws occurs as a result of chemical interaction between the base metal and the compounded materials, usually observed as surface pitting.
As a result, very tiny particles that are harder than the screw flights will cause microabrasions by being trapped between the rotating screw flight and barrel liner. Abrasive wear occurs locally at specific locations along the length of the extruder, the OEMs say, and is manifested as smooth, rounded, polished screw and barrel surfaces caused by the hard material rubbing against the metal surfaces. Corrosive wear happens, not surprisingly, when corrosive materials attack the surface metal. “The feedscrew and barrel are destroyed through an unintentional chemical or electrochemical action,” said John Christiano, vice president of extrusion with Davis-Standard LLC. “Some PVCs, corrosive flameretardants, and fluorocarbons are common culprits.” Others point out that processing virgin corrosive materials with barrels and screws not designed for them will prematurely wear the screws. “Fluoropolymers are a prime example, as I have seen many processors use standard equipment to process ETFE and other fluoropolymers that, while not as corrosive as FEP or PFA, will decrease the life of the hardware,” said Larry Alpert, medical extrusion technology manager with Graham Engineering. “As for fillers, in the medical field many polymers are filled with tantalum and/or tungsten fill and will wear the feedscrews even when the screws have been adequately November 2022 Canadian Plastics
19
extrusion
Severe abrasive wear on kneading elements.
designed for use. I’ve had processes where the CPM90V screws were replaced every two months.” The dividing line is between virgin and non-abrasive polymers – which are passive against any corrosive wear – on the one side, and abrasive materials on the other. Exclusively using the former, along with proper alignment of the screw within the barrel, can ensure continuous operation of the extruder for years with almost no screw wear, some OEMs say, while adding other items or fillers to the mix – anything with different shapes, sizes, hardness, and chemical structures that behave differently than virgin polymers under load, temperature, and pressure – can trigger corrosion. And according to most OEMs, the largest portion of corrosive wear usually occurs in the metering zone where temperatures are higher and the material remains for longer, increasing the possibility of product degradation, and is manifested as pitting and surface roughness. The third phenomenon, adhesive wear, is caused by the metal-to-metal contact of screws rubbing against each other or against the barrel sections. “Depending on the design of the screw, a top screw flight can be thrust against the barrel with high pressure, causing a momentarily localized weld, and the weld separates with subsequent screw rotations and is carried away,” said Kanti Das, Graham Engineering’s senior applications engineer. “The adhesive wear is severe with sliding contact with similar material.” But unlike abrasive and corrosive wear, adhesive wear – which usually results in rolled flight edges, galling, and other evidence of
20 Canadian Plastics November 2022
metal-to-metal contact – isn’t just a typical byproduct of running an extruder. “Metal contacting metal is not considered a normal condition associated with twin-screw compounding extruders,” said Adam Dreiblatt. “Any sign of adhesive wear is an immediate indication that something is wrong.” Adhesive wear, along with some other factors, also helps to explain why feedscrew wear can be somewhat less severe, and different, in single-screw extruders than in co-rotating twins. “In the first place, single-screw units don’t generate screw-to-screw adhesive wear,” said Tammy Straw, marketing and business development manager with Entek. “Also, single-screw units typically turn at much lower screw speeds than corotating twins, and typically aren’t used as much in high-wear environments for compounding as twin-screws are.” Finally, the wearing pattern of twinscrews may be different from that of a single-screw.
LOCATION, LOCATION, LOCATION
Feedscrew wear in an extruder will always happen, even if only very slowly – the diameter of the feedscrew will decrease and the diameter of the barrel will increase as the screw wears. But some OEMs note that if the rate of wear changes, it’s an early warning of a problem – that something in the process itself may have changed. “If the wear rate suddenly speeds up, the hardness of a mineral filler may have changed, a different screw or barrel metallurgy may have mistakenly been installed, the screw geometry may have been altered, or there could be an increase in pressure at the die because of a different size die hole or filtration screens,” said Tammy Straw. The location of the wear on the screw also reveals a lot about where the problem is in the extruder. “If the screw flight wear pattern is on one side, it indicates some misalignment between the screw and barrel, or that the screw is bent,” said Kanti Das. “Excessive wear in the transition section area of a singleflight screw may indicate high compression and short transition.” Wear that occurs in the melting zone, meanwhile, can be a sign of abrasion
from resin pellets or contamination in recycled feedstock, pigments, and any filler introduced into the main feed port. “The first kneading element on the extruder screw design is subject to the highest mechanical stress and is the highest wear-point in most compounding extruders,” Adam Dreiblatt said. “The conveying elements feeding into this first kneading element also experience abrasion since there’s no melt present at this point in the extruder to act as a lubricant for the remaining screw elements.” Abrasive wear in downstream mixing zones can be caused by abrasive fillers being compounded, Dreiblatt continued, while abrasive wear in the die pressurization zone – which begins at the end elements and moves upstream as wear progresses – is a sign that the diameter of the conveying screw elements has decreased, with the enlarged clearances reducing the conveying efficiency. “This is the second-highest wear point in most compounding extruders,” he said. Whatever the cause, usually the first consequence of screw wear that can be observed is the reduction of the maximum flow rate that can be processed by the extruder. “The clearance between the barrel and screw will increase as the wear advances, which results in increased leakage flow over the screw flights, leading to a decrease in pumping capacity and lower melting rate,” said John Christiano. “The specific output rate of the extruder will decrease and the melt temperature will increase. Process stability will decline as the wear becomes excessive, leading to output and melt temperature fluctuations. You’ll definitely notice a difference in output rate as well as extrudate quality.”
A GOOD COATING
Winding back the clock on the problem, there are early steps that can be taken to dramatically reduce screw wear. The first is proper design of the screw – it should be designed so that melt begins to form before compression starts, the OEMs say, and with enough melt present throughout the remainder of the screw to prevent complete solids plugging. The right design also includes having the screw made from the right materials. www.canplastics.com
extrusion “Selecting the correct materials of construction is the best way to combat feedscrew wear, especially corrosive wear,” said John Christiano. “Using corrosiveresistant materials beginning with Ph stainless steel alloys is a good choice for moderately corrosive materials; and for very corrosive applications, high-nickel alloys are required.” For a screw that hasn’t been ideally designed for a specific extrusion process – in a unit bought at auction, for example, or being used to extrude newer, more exotic and abrasive materials – the OEMs suggest increasing the hardness of the base material of the screw with various coatings or surface treatments. “The most common coating practices in the industry are hard chrome plating, which offers some improvement of abrasive wear in the feed section; and electroless nickel plating, which offers protection against corrosive and abrasive wear due to uniform and denser coating than chrome plating,” said Kanti Das. “Also, the abrasive resistance of some substrates of the screw can be enhanced by surface treating like nitriding, nitrocarburizing, and age-hardening.” Additionally, a variety of coatings are available in today’s market, depending on the application – different types of PVD, CVD, and TDC coatings, for example, as well as Poly-Ond. “The choice of the right coating depends on the application of the process, and it’s best determined in a conversation with an OEM,” said Tammy Straw. The big limitation to coatings is that they’re best-suited for single-screw units. “The screws of co-rotating twinscrew extruders are operating at very high screw speeds – typically between 500 and 1,000 rpm – and are subject to very high mechanical stresses, which precludes the use of coatings, as they’ll generally fail under these conditions,” Adam Dreiblatt said.
still makes the extrusion process economically viable, the OEMs say. Ultimately, however, the clearance between the barrel and the screw will grow to exceed tolerable limits, at which point there are two options available: rebuilding or replacing the screw. Every extrusion system is unique in its own way, but there are some general rules of thumb that can be followed. First, there’s a divi-
LEADERS IN PLASTICS SHREDDING
TECHNOLOGY
STAND-ALONE SHREDDERS TO COMPLETE RECYCLING SYSTEMS FOR ALL TYPES OF PLASTICS & POLYMERS
TO REBUILD OR NOT TO REBUILD?
In the short term, depending on the severity, a processor with a worn screw might be able to buy some extra time by increasing the speed of rotation to maintain the original design flow rate and discharge pressure. The maximum acceptable amount of wear is that which
sion between the options available for single- and twin-screw extruders. “For co-rotating twin-screw extruders, repair or rebuilding of worn parts isn’t feasible, since the screws are small individual segments versus a solid one-piece screw,” said Adam Dreiblatt. “When the screws are disassembled to replace worn parts, the majority of the screws can be reused in a different position. The screw
vecoplanllc.com
info.us@vecoplan.com
(336) 447-3573
November 2022 Canadian Plastics CPL_Vecoplan_June22.indd 1
21
2022-05-19 10:23 AM
extrusion
parts that are worn beyond specified limits are discarded.” In most other situations, rebuilding an existing screw can be an attractive option provided the amount of wear isn’t excessive. “Generally, we can engineer an existing screw back to its original performance characteristics and surface treatments, and this is the most costeffective option,” John Christiano said. “But if the screw wear is so extreme that it’s difficult or even impossible to repair reliably then it’s probably time to replace the screw, especially if your processing parameters have changed.” Either way, it’s not ideal to make this call on your own: An experienced screw manufacturer can inspect worn equipment and processing performance to determine if the current design is worth salvaging. Good rebuilding practices – which include high-quality welding, careful consideration of the metallurgical aspects of screw manufacturing, and proper flight-profile reconditioning – should allow for screws to be salvaged several times, OEMs say, although exactly how many times is up for debate. Officials at Glycon Corp., for example, caution customers against rebuilding a feedscrew more than twice, since each time the rebuild process is completed the original geometry of the screw is slightly altered. “After two rebuild operations, the flights of the screw have been side-grinded to a point that has altered channel volume and flight width, both of which can affect processing characteristics,” the company said. However, others cite examples of screws being rebuilt between six to eight times. Whatever the number, since the cost of rebuilding tends to be a fraction of the cost of a new screw, most OEMs recommend replacing the screw only as a last resort. “A new screw replacement takes time and money since extrusion screws should be custom-made for the resin and process, not bought off the shelf,” said Kanti Das. “The exceptions are, I wouldn’t recommend trying to rebuild any screws that are below 1.25-inches in diameter or made with tool steel.” An old rule of thumb says that a flight clearance four times the original tolerance is the cut-off point for screw replacement,
22 Canadian Plastics November 2022
but it’s important to consider the viscosity of the resin processed – a resin with higher viscosity will provide less loss of output than will lower viscosity resins with the same radial clearance.
GET DEFENSIVE
To modify the old saying, an ounce of preventative maintenance with an extrusion screw is worth several pounds of repair. “We recommend regular inspection of screw sets and barrels at set intervals to prevent reactive maintenance, and there are several ways to do this,” said Tammy Straw. “Some customers track the number of pounds run through an extruder, some track the length of time the screws are run in production hours, and others run strictly on a calendar basis.” Sometimes on larger machines, taking a machine out of production, removing the screw, cleaning and measuring both the screw and barrel, then reassembling the machine can take two or three days, which has always been tolerated as the price of doing business. Recently, however, preventive wear diagnostics technologies have caught up: On Coperion’s ZSK and STS extruders, diagnostics can be done by simply pulling the extruder screws out – dismantling the process section isn’t necessary. And Glycon recently introduced the latest version of its electronic measurement and tracking (EMT) system to measure screw and barrel wear at the source: inside the plasticating unit. Enhancements include the company’s new specialized SmartBarrels, which feature strategically placed ports called SmartPorts. The ports allow access to the inside of the barrel for instruments that measure the gap between the inner diameter of the barrel and the outer edge of the screw flights. The measurements can be used to determine the rate of wear and predict when screws and barrels will need to be replaced. Other monitoring tools include a borescope inspection to confirm correct barrel and screw alignment, which is now available from some suppliers as an articulating video borescope. “It’s critically important to borescope your equipment during the initial installation and
Corrosive wear of elements and barrels that’s not observed can lead to component failure; corrosion between screw elements and shafts can lead to a screw shaft failure.
also after any major repair of the barrel and screw,” John Christiano said. “It’s best to consult with your OEM on best practices based on your process.” But whatever the interval of inspection is, the goal should be to perform periodic inspection of the screw even when it’s performing at the expected level. “A well-performing screw can still develop minor issues like depleted patches of chrome plating or other small defects in flights, but these can be repaired easily if they’re discovered early,” Kanti Das said. In the end, with proper baseline data and wear-monitoring procedures in place, and an understanding of what’s happening to the screw, extrusion shops can develop the robust maintenance program that’s necessary to keep on top of screw wear – and in the bigger picture, greatly reduce downtime and increase CPL profitability.
RESOURCE LIST Coperion Corp. (Sewell, N.J.); www.coperion.com; 856-256-3175 CPM Extrusion Group (Traverse City, Mich.); www.cpmextrusiongroup.com; 231-947-6400 Davis-Standard LLC (Pawcatuck, Conn.); www.davis-standard.com; 860-650-4992 Auxiplast Inc. (Varennes, Que.); www.auxiplast.com; 450-922-0282 Entek Extruders/Entek Manufacturing Inc. (Lebanon, Ore.); www.entek.com; 541-259-1068 Glycon Corp. (Tecumseh Mich.); www.glycon.com; 800-255-9969 Graham Engineering (York, Pa.); www.grahamengineering.com; 717-848-3755 www.canplastics.com
size reduction
SIZE REDUCTION FAQs
We asked some shredder and granulator makers about the most common plastic size reduction questions they get from their customers. Here’s what they told us. By Mark Stephen, editor
“DO I NEED A SHREDDER OR A GRANULATOR?”
It helps, first, to understand the distinction, since shredders and granulators perform similar but different functions. A shredder is a high-torque, low-speed machine designed to process large and heavy items, as well as being capable of handling bulk-fed parts such as entire Gaylords of material at one time. Shredders are designed for centralized, high-volume work, and are built with either single- or dual-shaft designs. Granulators are high-speed, low-torque machines designed to reduce parts to small particle sizes for reuse, and can be processed in downstream molding equipment. Available in large central and smaller beside-the-press models, they depend on high-horsepower motors and inertia generated from heavy flywheels for cutting power.
24 Canadian Plastics November 2022
In deciding between the two, the OEMs say, four key considerations will usually provide the answer: volume/throughput, density, feeding method, and material size/condition requirements. “Granulators are often used by manufacturers for their sprues and runners and scrap parts as long as they’re of a size and weight that’s appropriate for a granulator to process,” said Greg Parent, the Canadian sales agent for Vecoplan LLC. “But as part size and part weight go up, a shredder becomes more useful, since it has the muscle to process large, heavy, and thick parts.” Granulators don’t have a minimum throughput limit, and when properly sized they can handle hundreds or even thousands of pounds of scrap as easily as a few pounds. “A granulator’s principal capacity limitation is the size and shape of the feed opening – if the scrap fits in and doesn’t jam the granulator, then it can probably be size-reduced,” said Dave Miller, general manager, size reduction with Conair Group. “But if you need to process high-volumes of heavy, dense scrap and you want to avoid the labour-intensive prep work needed to use a granulator, a shredder is likely your best choice.”
“CAN I GET A QUOTE ON A 50-HP GRANULATOR?”
With this type of question, the OEMs say, the customer is mistakenly trying to choose a size reduction machine based solely on a unit’s horsepower as opposed to the needs of the application. “This is especially true with new customers – they want to select the granulator themselves, according to horsepower, based on information they’ve sourced from a website,” said www.canplastics.com
Photo credit © digitalstock / Adobe Stock
W
hen it comes to size reduction in plastics, there are no stupid questions. You could go even further and say that the most basic questions are actually the smartest, since getting the fundamentals right eliminates much of what can go wrong with the process. For plastics processors – as opposed to recyclers – the primary goal of size reduction is to convert plastic scrap back into a size that matches the new or virgin material being processed. And it’s a more important step than ever, due to the higher cost of materials combined with increased demands from customers to include reground and/or recycled materials in the mix. Sounds simple, but there’s a lot more to it than that. And according to many shredder and granulator manufacturers, processing customers all across the board tend to ask the same few questions. So, here are the most common plastic size reduction FAQs and the OEMs’ answers.
size reduction “IS IT FOREIGN-MADE OR DOMESTIC?”
This is a question that’s become much more common lately, as supply chain problems that emerged during COVID-19 lockdowns continue. “This is actually one of the biggest questions I hear,” Mike Cyr said. “Customers want domestically-made size reduction equipment if possible – equipment that’s truly manufactured in North America, as opposed to only assembled in North America.” The reason, obviously, relates to parts and service. “They want easy access to components, aside from the consumables like blades, which can be obtained easily,” Cyr said. “Nobody wants to pay as much for shipping from overseas as for the replacement part itself.”
Jim Hoffman, president of Rapid Granulator Inc. “Other factors are far more important than horsepower: the type of process – injection, extrusion, or blow molding; the evacuation system; the part dimensions; the number of parts being processed per hour; the materials the parts are made from; the screen size; and whether the customer has automation giving a uniform rate of feed or an operator dumping large quantities in periodically. We can provide a quote based solely on horsepower, but the right way is to start with the application and work back from that.” Whether or not this particular question gets asked in the first place usually depends on who’s asking. “Production staff ask different questions than people in the purchasing department,” said Mike Cyr, president of Rotogran International Inc. “Buyers only tend to ask about the cost and the delivery time; because they’re too far removed from production, they usually don’t understand that it’s a system discussion based around the application, which is the key to everything. That’s why we need to talk to either the application engineer, plant manager, or someone else in a comparable position – there has to be a way to convey the application information directly to the manufacturer, because that information can get diluted going through the purchasing or accounting department.” Similarly, some OEMs report taking a lot of calls from customers with questions about throughput. “Some involve potential customers who have identified equipment they want to purchase for a new application based on its size/ throughput, while many others involve throughput changes when an existing granulator moves to a new application,” said Dave Miller. “In the case of a new machine, someone might say, ‘I’m thinking of this machine because I need 400 pounds per hour,’ but as we talk about the application, I often make a different recommendation and tell them, ‘If you need to granulate 400 pounds per hour of that particular material, this machine won’t do it – you’re going to need to look at this model instead.’ They might say, ‘Your website said the throughput rating was 400 pounds an hour,’ and I have to point out that 400 pounds of this material isn’t the same as 400 pounds of that one.”
“WHEN SHOULD I USE A STACKED SHREDDER/ GRANULATOR SYSTEM?”
By stacking the system – putting a shredder on top of a granulator – a processor can reach and maintain the maximum throughput capacity of an existing granulator while minimizing both the footprint and the cost, since there’s no conveyor between the machines. Most OEMs say that a stacked system can be a good option depending on how the customer wants to feed it. “If they want to be able to dump a Gaylord at once – the
Minutes MAtter Are changeovers keeping you off your pace? Dyna-Purge cleans on the first pass, minimizing machine downtime to maximize your productivity! Plus, only Dyna-Purge provides product and technical support built on over 30 years of innovation. Our customers enjoy the industry’s most effective commercial purging compounds, outstanding customer service and reliable results. Start saving time and increasing profits today. Request a free sample of Dyna-Purge and see for yourself.
Discover the Difference. 866-607-8743 www.dynapurge.com DYNA-PURGE is a registered trademark of ShUmAN PlASticS, iNc.
November 2022 Canadian Plastics CPL_Shuman_Nov22.indd 1 CP_MinutesMatter_Resize.indd 1
25
2022-10-31 2017-02-22 3:23 3:11 PM PM
Photo Credit: Wittmann Group
size reduction
New granulator knives.
‘dump-and-run’ – as opposed to feeding one piece at a time or using a conveyor, we might recommend a stacked system,” said Jim Hoffman. A stacked system can be ideal for saving space in a plant with sufficient ceiling height in applications where both shredding and granulating are required. But gravity is the enemy. “There’s no real opportunity to remove metal from the shredder’s material stream prior to entering the granulator, and this metal can completely destroy a set of granulator blades,” Greg Parent said. “Typically, metal detection and/or separation is included after the shredder and before the granulator for this reason. With a stacked system, a plate magnet can be put in between the two pieces of equipment, but it’s not highly effective.” Which is why a non-stacked layout, with a conveyor picking up the shredded material and conveying to the granulator, is a popular option. “You can more economically put a metal detector or magnet system to pull ferrous materials out on the smallish conveyor feeding the granulator,” said Bob Harrison, product manager, size reduction group with Universal Dynamics Inc. “Also, you can bypass the shedder if not needed and just load onto the conveyor feeding the granulator; and it’s easier to clean and maintain a non-stacked system.”
“HOW OFTEN DO I NEED TO SHARPEN OR CHANGE THE BLADES?”
We saved this for last, but it may be the most commonly asked size reduction question of all. And the answer is, it depends. “How fast a granulator’s blades will become dull depends on how much the granulator is processing high volumes of materials, the geometry of the basic part going into the granulator, as well as the material type,” said Denis Metral, international granulators sales manager with Wittmann Group. “However it happens, dull blades are far and away the most common granulator problem, and causes non-uniform and dusty regrind, lower throughput rates, increased energy consumption, and premature failure of connected devices.” The commonness of the problem is due to the fact that blades are the highest wearing items on granulators and shredders, and in many cases the most expensive maintenance item. And perhaps also the most neglected part of a
26 Canadian Plastics November 2022
granulator or shredder. “The percentage of processors that change their knives on a regular and scheduled basis is very small,” Bob Harrison said. “It’s the single most important thing that they can do to have quality regrind that can be used, or used in higher percentages.” Granulating requires precision blades, and the material matters – both the material being granulated and the material of the knives. It’s a fact that some materials are a lot harder to granulate than others. “Granulating glass-filled nylon means the knives have to be changed up to five times more often than granulating polystyrene, which is the easiest material in the world to granulate; and with post-consumer material that has the potential to be highly contaminated, the knives may need to be changed as frequently as every 24 hours,” said Jim Hoffman. “The most common material used in granulator knives is D2 tool steel, which seems to give the best balance of hardness versus malleability – for glass-filled materials, you can do tungsten carbide impregnation or different coatings to help extend the knife life, but you will never wear-proof it.” Unless the processor is running abrasive or glass-filled materials, OEMs say, they might be able to get away with as few as two or three sharpenings a year. “And knife sharpening/replacement doesn’t involve a lot of downtime – just a couple of hours or less, or perhaps a maximum of four to five hours on a large machine,” said Dave Miller. The OEMs also stress the importance of following the sharpening instructions of the operation manual, of course. “And having a spare set of blades available on the shelf for each granulator prevents downtime while waiting for the blades to be sharpCPL ened,” said Denis Metral. RESOURCE LIST Conair Group (Cranberry Township, Pa.); www.conairgroup.com; 724-584-5500 Auxiplast Inc. (Varennes, Que.); www.auxiplast.com; 450-922-0282 Dier International Plastics Inc. (Unionville, Ont.); www.dierinternational.com; 416-219-0509 Turner Group Inc. (Seattle, Wash.); www.turnergroup.net; 206-769-3707 Rapid Granulator Inc. (Leetsdale, Pa.); www.rapidgranulator.com; 724-584-5220 DCube (Montreal); www.dcube.ca; 514-272-0500 Rotogran International Inc. (Toronto); www.rotogran.com; 905-738-0101 Universal Dynamics Inc./Piovan Canada (Mississauga, Ont.); www.piovan.com; 905-629-8822 Vecoplan LLC (Archdale, N.C.); www.vecoplanllc.com; 336-447-3573 Greg Parent; 416-678-0154 Wittmann Battenfeld Canada Inc. (Richmond Hill, Ont.); www.wittmann-group.com; 905-887-5355 www.canplastics.com
technology showcase
AUXILIARY EQUIPMENT Air channeling system reduces heat loss The new SoftBoost air channeling system from Piovan Group allows the granule to be heated to the core in just 40 minutes in order to quickly bring it from 120° to 180°C, or 250° to 355°F. Completing the dehumidification directly or close to the injection molding machine allows the main dehumidification hoppers to be used at temperatures between 120° and 140°C, or 250° and 285°F, thus limiting heat loss. At the same time, this makes it possible to work along the plasticising screw of the press at lower temperatures, reducing further thermal stress during molding and limiting the production of scrap. The reduced residence time of the material in the SoftBoost hopper, at the required working temperature, avoids unnecessary stress on the rPET and allows its mechanical, chemical, and optical characteristics to be preserved. Piovan Canada Ltd. (Mississauga, Ont.); www.piovan.com; 905-629-8822
Dryer for high-throughput requirements
With a maximum capacity of 2,200 pounds, or 1,000 kilograms, per hour, Maguire’s new Ultra 2200 dryer is designed to meet the higher throughput requirements of central drying, sheet extrusion, preform, and fibre markets, while also offering much faster drying than conventional methods while using significantly less energy. Each chamber can self-load, heat, vacuum, and dispense – this design allows for a compact arrangement with a relatively low ceiling height requirement. The Ultra 2200 incorporates load cell technology, which provides the operator with the ability to monitor and control each step of the drying process, allowing for process optimization throughout the entire drying cycle. By digitalizing the process, every granule within the drying system is actively monitored and controlled. And the data can easily be viewed on the touchscreen, and is also available for export for integration with any ERP or other process control system. Maguire Products Canada Inc. (Vaughan, Ont.); www.maguireproducts.com; 905-879-1100
New material loader with dedusting function The new Feedmax CL (CLean) material loader from Wittmann Group is designed to meet the increasingly stringent requirements of the circular economy and the resulting increase in plastic granulate containing dust. The Feedmax CL can achieve a separation rate of dust and fines of up to 80 per cent (for particles < 1.000 μm) in one conventional material loading cycle. The separation screens are available in different sizes for varying degrees of fine particles and dust removal. The Feedmax CL also comes with an inflow chamber and a vortex cleaning chamber separated from each other by a self-fixating, removable cone. Another feature is the removal of dust from the entire feed quantity, over the whole material feed time. Where necessary, the particle separation result can be improved still further by lengthening the cycle time. Wittmann Battenfeld Canada Inc. (Richmond Hill, Ont.); www.wittmann-group.com; 905-887-5355
INJECTION MOLDING Multi-component versions of hybrid IMMs
Absolute Haitian, which last year began offering multi-component versions of its all-electric Zhafir injection molding machines, has now introduced the same capability for its Mars III Multi and Jupiter III Multi servo-hydraulic machines. The new Multi versions range from 135 to 596 tons for the Mars III line, and from 843 to 2,709 tons for the Jupiter III line, a series of twoplaten machines. Shot sizes range from 0.67 to 45.7 ounces on Mars III Multi machines, and from 43.3 to 89.8 ounces on the Jupiter III Multi machines. The Mars III Multi and Jupiter III Multi machines can be configured in a variety of ways, with the second injection unit in parallel, vertical, horizontal or piggyback positions, or switched off or removed for single-shot applications. The new units have Keba controls featuring a user-friendly arrangement of key buttons for the injection process of the additional unit. Absolute Haitian Corp. (Worcester, Mass.); www.absolutehaitian.com; 508-459-5372 Shadow Automation (Uxbridge, Ont.); 416-464-2070 Belplas Inc. (Toronto); 905-715-0529 Barway Plastic Equipment Inc. (Vaudreuil-Dorion, Que); www.barway.ca; 450-455-1396 November 2022 Canadian Plastics
27
technology showcase
SIZE REDUCTION Six-machine series includes electrics and hybrids Tederic’s new Neo family of six machines – the Neo.T (pictured), Neo.E, Neo.Ec, Neo.H, Neo.Mv, and Neo.Ms – are designed to use 30 to 80 per cent less energy than conventional hydraulic machines. The machines, with clamping forces from 60 to 4,400 tons, are equipped with a new generation of energy-efficient servo pumps that enable ultra-high response speeds; have advanced Keba controls and touchscreen control monitors available in a range of sizes, from 12 to 21 inches, depending on the model; and machine guarding that’s been fully designed to be safer, more practical, and more user-friendly. The controllers offer support for OPC, UA, and Modbus data protocols, and feature free programming capabilities to accommodate a variety of process requirements. Tederic North America Machinery Inc. (Palmetto, Fla.); www.teceric-na.com; 941-323-9081
EXTRUSION Roll stand for greater automation and process control The XP Express AGT roll stand for both sheet and cast extrusion, the latest addition to Davis-Standard’s XP Express roll stand portfolio, features greater automation and process control for the full range of sheet applications. Features include an inverteddown, multi-roll design, which facilitates improved die nip management and handling; efficient web cooling and conditioning capabilities; precision roll drive control; and high-performance web path options. In addition, the XP Express AGT addresses low melt strength resin delivery from die slot to nip, and expands the processing of thin-gauge sheet. The XP Express AGT is currently available in widths from 36 to 80 inches (900 to 2,000 millimeters) and with process rates up to 5,500 pounds per hour. Davis-Standard LLC (Pawcatuck, Conn.); www.davis-standard.com; 860-599-1010 Auxiplast Inc. (Varennes, Que.); www.auxiplast.com; 450-922-0282
28
Canadian Plastics November 2022
Revised universal shredder Weima has upgraded its W5.18 single-shaft plastic shredder to be more powerful, maintenance-friendly, and versatile, with an output of up to 280 kW. With its 1,800-millimeter-long and 500-millimeter-diameter rotor, the shredder easily shreds both hard plastics and tear-resistant fibres and films. The swing ram offers aggressive but controlled material feed, and the generously dimensioned inspection flap provides direct access to the rotor during service work. For demanding applications such as heavily contaminated material, Weima offers special options for wear and corrosion protection, including a Vautid shell or hard facing using weld seams for the rotors, and additional wear plates in the cutting chamber or wear-resistant screens. And cutting blades are available in 60- and 80-millimeter edge lengths, significantly extending the service life of the components. Weima America Inc. (Fort Mill, S.C.); www.weima.com; 803-802-7170
ADDITIVE MANUFACTURING Plastics machinery manufacturer enters 3D printing space With the launch of two new 3D printing technologies, KraussMaffei Technologies is entering into the additive manufacturing space. Targeted at large-format industrial additive manufacturing, the room-sized powerPrint is an extruder-based system that processes thermoplastic granulate, and can handle objects up to 10 cubic meters in size. And designed for industrial scale automated production, the smaller precisionPrint machine (pictured) is an automated, stereolithographybased solution that uses printing resins to produce parts with high surface quality and detail resolution that are cured by laser. Beta testing will first be conducted next year, after which both printers will be available on the market. KraussMaffei Corp. (Florence, Ky.); www.kraussmaffei.com; 859-283-0200
www.canplastics.com
technology showcase
MATERIALS
Photo credit: © ronstik / Adobe Stock
Capstock compounds offer ‘soft feel’ surface Struktol has expanded its TPW series of specialty additives with new capstock compounds that provide a “soft feel” surface. With excellent scratch resistance, adhesion to substrate, processability, and low gloss surface, these soft touch compounds are designed to offer superior anti-slip properties with greatly increased coefficient of friction. The focus of these new compounds will be wood-plastic composite handrails, poolside decking, stairs, ramps, and any other applications where a softer surface with better grip and feel are required. These products can all be supplied with or without a unique stabilization package. Additionally, Struktol’s capstock compounds can be tailor-made to address the customer’s needs. Struktol Canada Ltd. (Newmarket, Ont.); www.struktol.com; 416-286-4040
JOB POSTING: Regional Sales Manager, Piovan Canada The Regional Sales Manager is responsible for the procurement and maintenance of key and target accounts in the regional portfolio. Developing and executing upon strategic goal-oriented actions that will result in opportunities for sales of company equipment and services that deliver sustainable top & bottom-line growth within the assigned region(s). Full details here: www.canplastics.com/jobposting
advertising index Advertiser Page Absolute Haitian 7 Annex Business Media 9 Canadian Standards Association 23 CCC Plastics 29 Chillers Inc. 13 Davis-Standard LLC 17 Dyna-Purge Div./Shuman Plastics Inc. 25 Novatec Inc. OBC PCS Co. 5 Plastic Process Equipment IBC Struktol Canada 11 Vecoplan LLC 21 Weima IFC
Website www.absolutehaitian.com www.canplastics.com www.csagroup.org www.ccc-group.com www.chillersinc.com www.davis-standard.com www.dynapurge.com www.novatec.com www.pcs-company.com www.ppe.com www.struktol.com www.vecoplanllc.com www.weima.com
CREATE FORMULATIONS THAT GO BEYOND EXPECTATIONS When you’re looking for a customizable solution that enhances physical properties without compromising performance, Honeywell’s range of performance additives deliver on point. From lubricity to productivity to better filler and pigment dispersion, enhance a range of properties of your plastic formulations with Honeywell’s customizable high-performance additives offering. Let’s develop a solution that’s ideal for you. Contact our experts today!
LEARN MORE
Proudly distributed by CCC Plastics
November 2022 Canadian Plastics CPL_CCC_Nov22.indd 1
29
2022-10-27 3:44 PM
technical tips
Five questions to ask before instrumenting a mold By Brad Harvey, RJG Inc.
1. WHAT DO YOU WANT THE SENSOR TO DO?
This is the most important question to ask before installing sensors in your mold, and most people run into problems right here. Some want to try out process control software, while others are curious about the ability to collect data, track a part to a molding cycle, resolve ongoing challenges, or create a template to maintain or transfer processes. Whatever the answer, once you know what you want the sensor to do, we can begin to explore the many different functions sensors can serve if used correctly, including monitoring pressure at a specific area in the cavity, transferring the injection portion of the cycle to hold via pressure, detecting mold defection, sequencing valves gates, and automatically sorting bad parts.
2. WHERE DO YOU WANT THE SENSOR INSTALLED?
Conventional installation locations include post-gate, mid-cavity, and endof-fill, but there are others. Post-gate sensors allow you to know the moment plastic enters the cavity and at what pressure, and with this information you can perform various studies, including pressure loss (from nozzle to gate), pack rate, and gate seal (pressure lost when the hold pressure is released); in addition, post-gate sensors are often the location of choice when using Decoupled III to transfer from pack to hold using cavity pressure, but other locations can work as well, depending on your machine and percentage of barrel usage. Mid-cavity sensors can aid in performing calculations like determining pressure loss through the cavity and cavity deflection; they can help with timing the firing pattern of valve gates on larger parts, like car panels, where manifolds are being implemented,
30 Canadian Plastics November 2022
especially when located near each gate; and they’re also a good option for very small parts, as they can typically represent an average pressure in the cavity and may be the only location available if moving ejector pins are not available at the last point to fill. End-of-fill sensors are the most common location used for automatically sorting bad parts, like short shots, using cavity pressure data; they can also monitor the pressure required to fill your part when used in conjunction with a post-gate sensor. By subtracting the end-of-cavity pressure from the post-gate pressure, you can see the pressure loss through the cavity and observe the cooling behavior of the plastic, which is critical in semi-crystalline polymers. Cavity-temperature sensors can be used to detect the time at which the flow front passes over a particular area in the cavity, because the temperature rises rapidly as plastic flows over them, which can be useful in timing the opening of sequential valve gates when the sensors are located close to each gate; and they can also measure the surface temperature of the steel, and even the relative melt temperature of the plastic that’s passing over the sensor.
3. HOW SHOULD THE SENSOR BE INSTALLED?
The most common installation styles for pressure sensors are flush-mount and button-style. Flush-mount sensors are mounted in the cavity block so the sensing surface is in contact with the plastic. Button-style sensors are mounted away from the cavity, and the pressure is transferred to the sensor via ejector pin, transfer pin, static pin, or ejector sleeve. The choice of sensor style depends on many factors, including the availability of ejector pins in the desired cavity location, the space available for the sensor, and the temperature
of the mold, among others.
4. WHAT TYPE OF SENSOR TECHNOLOGY DO YOU NEED?
Two common sensor technologies are strain gage and piezoelectric. Strain gage sensors generally are more costeffective, require less maintenance, have more rugged cables, and are less susceptible to signal errors if water or other contaminants enter the connectors. Piezoelectric sensors are generally used in flush-mount applications and in certain applications where ultra-miniature sensors are required.
5. WHAT LOAD CAPACITY DO YOU NEED?
For button-style sensors, we need to determine the load capacity of the sensor used, which is determined by the predicted force that will be exerted on the sensor. To do this, we need to know the projected area of the sensing pin and the pressure you expect to see in the sensing location. Multiplying pressure by the area gives you the expected force. The sensor you choose must have a load capacity higher than the expected force, but not so high that the sensor signal gets “lost in the mud.” The preferred method for determining the expected pressure is to use flow simulation with predictions of the pressure in your chosen area. If this isn’t available, you can resort to the material datasheet, which often gives a pressure or tonnage factor. The key is to not make too many assumptions without supporting your decisions with actual data. CPL Brad Harvey is an engineering lab technician at RJG Inc., a Traverse City, Mich.-based training and consulting company that specializes in the injection molding industry. Visit www.rjginc.com for more. www.canplastics.com
Tired of Delays & Excuses? We Have Stock Ready to Ship In Canada!
Huge Inventory of Loaders Guaranteed to Ship within 72 hours! Not next week. NOT next month. NOT next year…Simply NOW!
Novatec.com NovatecNow.com •
© Copyright 2022 NOVATEC, Inc.
In Canada, contact us at Maguire Canada info@maguirecanada.com
905-879-1100