In 1914 Stuart A. Cogsdill set up shop in Detroit as a cutting tool regrinding and repair service. He soon began designing and manufacturing special tools for early automotive pioneers such as Henry Ford and the Dodge brothers, who relied on Cogsdill to develop innovative tooling solutions for tough manufacturing problems.
Currently owned and operated by the second and third generation of Stuart Cogsdill’s descendants, Cogsdill offers its 21st century customers the same commitment that inspired its founder.
“We will develop and build innovative tooling solutions for your tough manufacturing problems.”
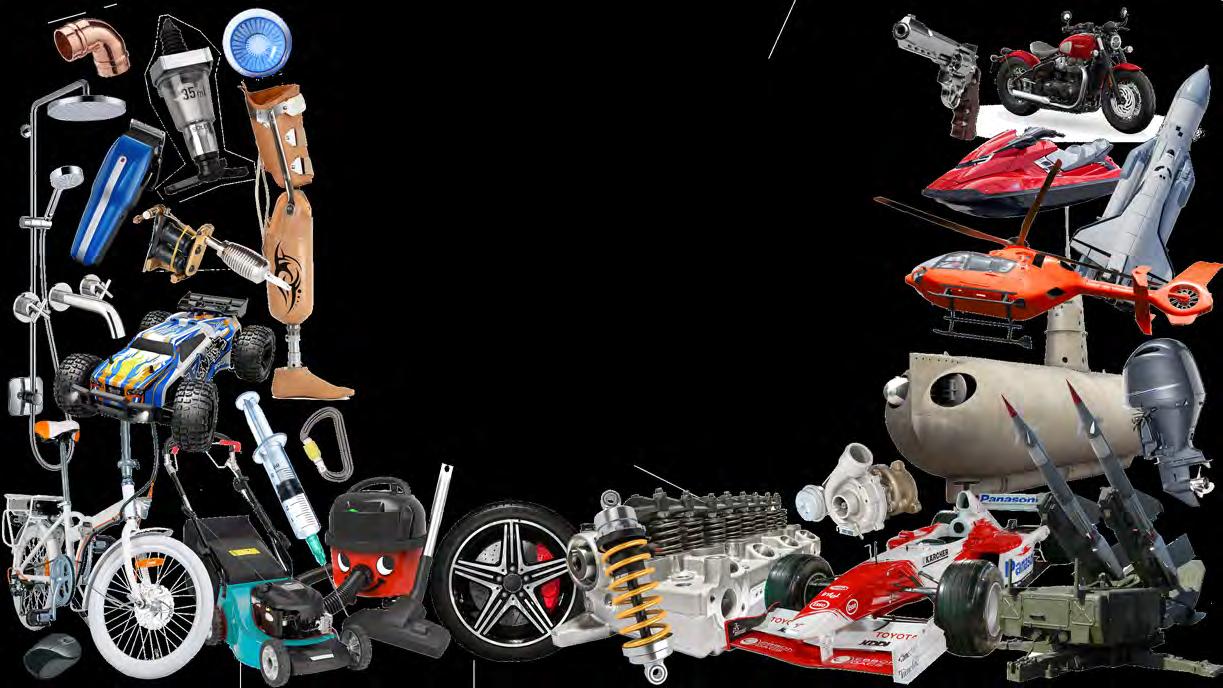
Our precision tools are used in the creation of every day items that touch every person on the planet.
From hypodermic needles and artificial hips to formula one engines and space rockets. The clothes you wear, the building you are in, the car you drive – planes, trains, and automobiles – whether sub-sea or the outer stratosphere – the list of applications is absolutely endless!
Cogsdill Today
“Our mission is to be the global leader in the precision tooling industry. Helping customers exceed their expectations through our enviable global experience, industry-defining products and an exceptionally friendly and stellar service.”
To achieve this aim, Cogsdill has two key operating units; one in the United States and one in the United Kingdom:
Cogsdill Tool Products, Inc.
Camden, South Carolina, USA – corporate headquarters
Cogsdill-Nuneaton Ltd.
Nuneaton, England – subsidiary of Cogsdill Tool Products
Cogsdill Austria GmbH
Same Passion
Commitment
Burnishing Tools
Deburring Tools
A fast, clean, and economical method of sizing, finishing and work hardening metal parts to exacting specifications. A better way to get rid of those troublesome burrs of drilled holes – front, back or both sides in one pass.
ZX Tooling System
Perform multiple operations on large parts, in one set-up or a minimum number of tool changes, with the ZX System.
Reaming Tools
Designed to produce accurately sized, extremely straight and round bores with fine surface finishes.
Recessing Tools
Ready to roll
Cogsdill Roll-a-Finish tools offer you a fast, clean, and economical method of sizing, finishing and work hardening metal parts to exacting specifications.
The tools can be operated on any spindle. Parts of virtually any configuration and material are accurately sized within “microns,” with surface finishes as fine as 2 µin (0.05 µm)… in seconds!
Accurate sizing. In one pass.
In process manufacture, no other operations required.
Standard Roll-a-Finish tools are available from stock for inside diameters from .156 to 4.000 inches, and for outside diameters from .062 to 2.000 inches. The tools are easily adjustable to suit application needs.. Special designs are available for larger and smaller diameters.
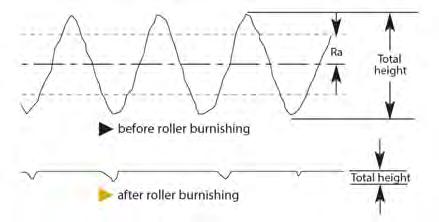
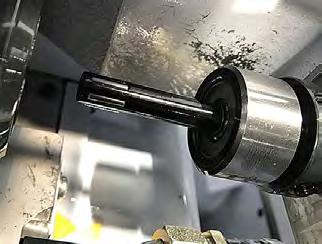
Roller burnishing is a surface finishing technique in which hardened, highly polished steel rollers are brought into pressure contact with a softer piece part. As the pressure generated through the rollers exceeds the yield point of the piece-part material, the surface is plastically deformed by cold flowing of sub-surface material.
The result is a mirror-like finish and a tough, workhardened surface with load-carrying characteristics that are superior to finishes obtained by abrasive metalremoval methods.
Burnishing Tools
Superior surface finishes without secondary operations ELIMINATE HONING
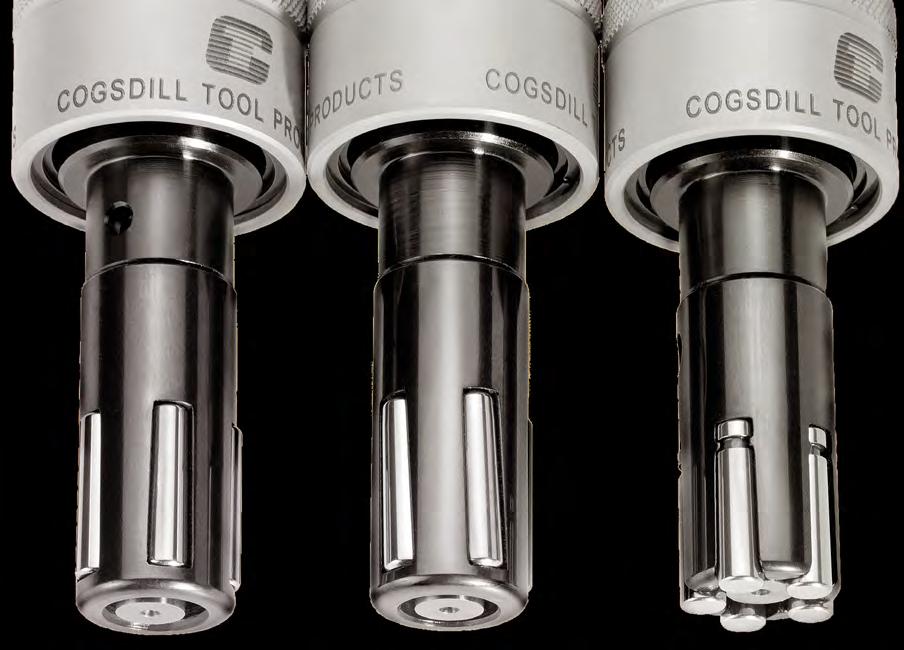
Standard internal range is offered in three styles:
• SR: Through-hole style (machine-feeding)
• SRH: Through-hole style with helix cage (self-feeding)
• SRB: Bottoming-style for blind hole (machine-feeding)
The Roller Burnishing Range
SR Series
Our premier line of internal burnishing tools, designed to suit all applications. Ideal for applications where tool length is restricted by tool changers, turrets, etc.
AEX Series
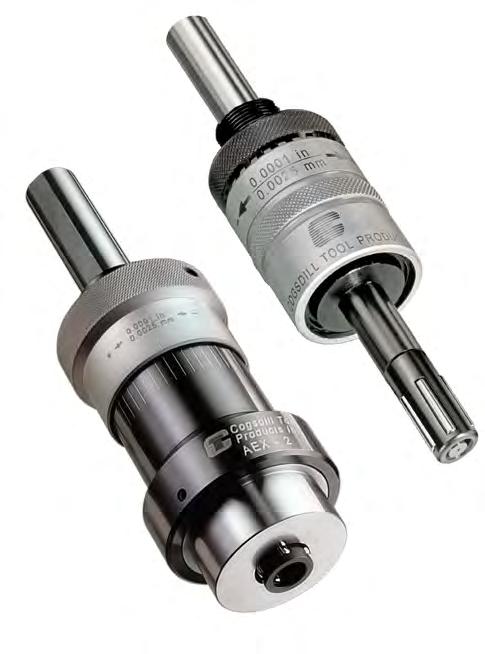
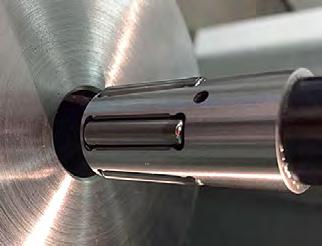
For burnishing the outside diameter of cylindrical parts, such as shafts rotating in bushings or bearings. Provides an ideal surface for grease and oil seals.
.156 to 4.000 inches internal tools for most sizes in stock for next
Micro Series
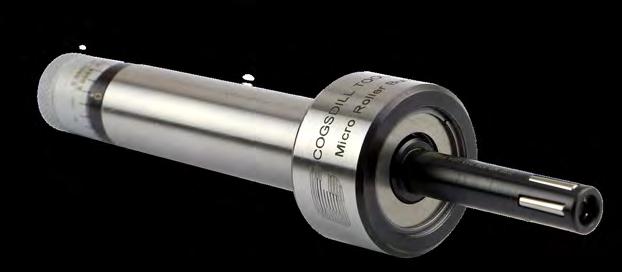
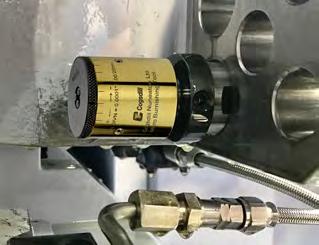
Micro Roller Burnishing series offers a compact design for use where limited space is available on multispindle automatic and screw type machines.
Peak/Valley surface condition
We hold the largest range of burnishing tools and spares in the US. Standard sizes available for immediate shipping!
Ask our engineers Compact and clever
Cogsdill Roller Burnishing tools can be applied to a wide variety of part configurations, including:
• Inside diameters (bores)
• Outside diameters (shafts)
• Flat surfaces
• Tapers
• Spherical and contours
• Fillets (radii at shoulders)
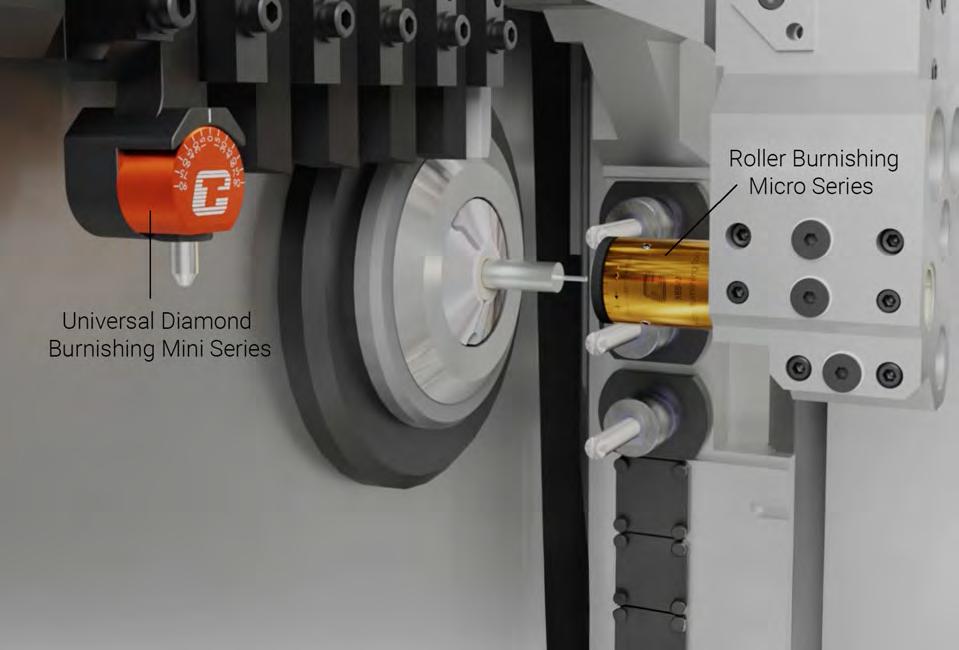
Micro Roller Burnishing series offers a compact design for use where limited space is available on multi-spindle automatic and screw-type machines.
• MR/B –Internal tools from 0.187 to 0.501 inch (4.75 to 12.73mm) in through style, and bottoming style larger than 0.246 inch (6.25mm)
• XBB-M –External tools from 0.059 to 0.393 inch (1.5mm to 10mm ) in bottoming style with two shank sizes available 16mm and 20mm.
Universal Burnishing Tools (UBT)
Versatile Burnishing
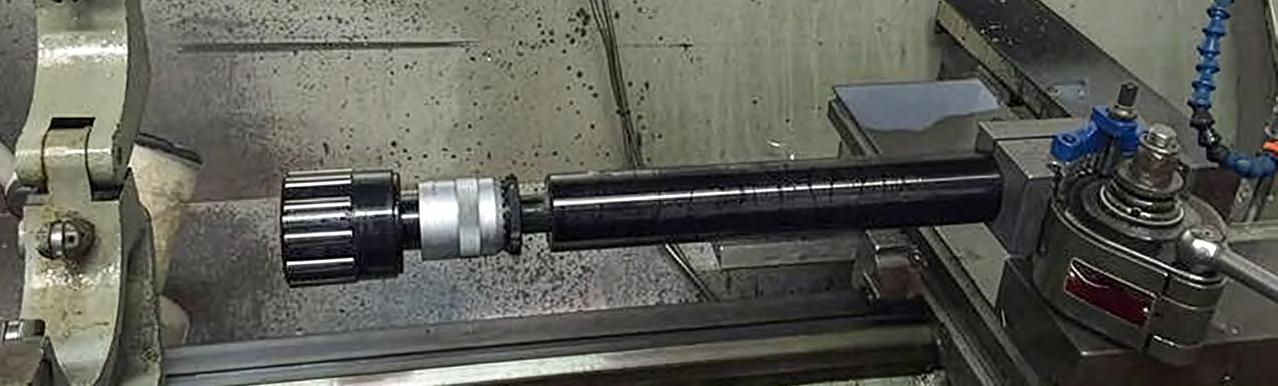
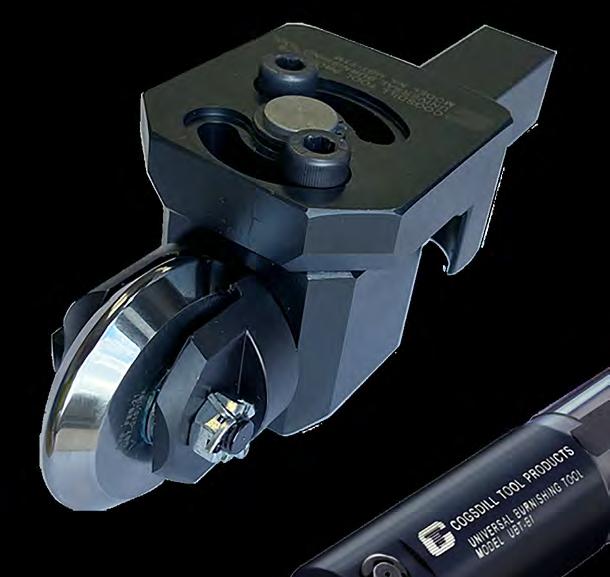
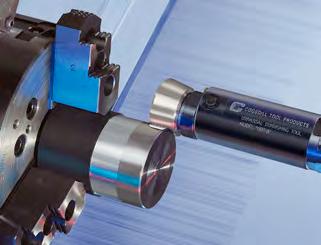
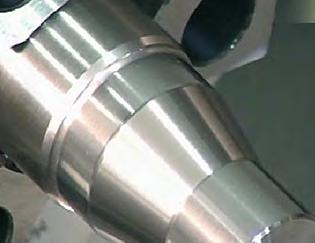
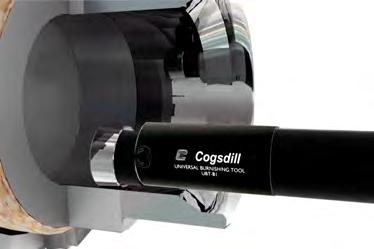
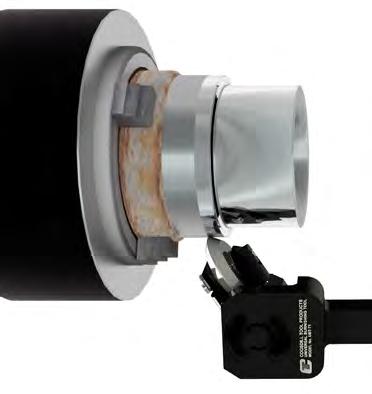
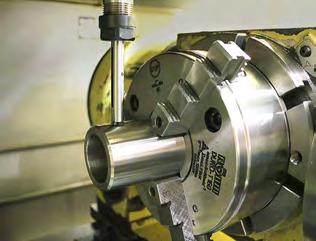
Cogsdill Universal Burnishing Tools are designed for burnishing shafts, faces, tapers, contours, and relatively large IDs (greater than 2.750 inches/69.85mm).
• Boring-Bar style and Indexable turning-holder style designs
• Tool designs to suit any part size or configuration, or any turning machine
• Low surface finishes
• Standard, available off-the-shelf
• Adjustable for optimum burnishing pressure
• Hardened steel or carbide rollers
Any size. Any configuration. On any turning machine.
We hold a range of tools and spare Carbide and HSS rolls in stock – in the US and UK.
Two styles are available:
Boring-Bar Style
The Cogsdill UBT-B series are designed for use in a machine turret configuration on a CNC lathe, where differing diameters are required from a single tool set-up.
Turning-Holder Style
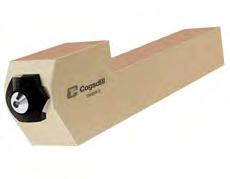
The Cogsdill UBT-T series are designed for use in an indexable turning holder configuration, mounted to a machine turret on a lathe.
This tool can be used in both leftand right-hand configurations.
• UBT-B1 – For large diameters, tapers & faces (Hardened steel and carbide roll)
• UBT-B2 – For smaller diameters, tapers & faces. (Hardened steel and carbide roll)
• UBT-B3 – For smaller diameters where facing is not required. (Hardened steel only)
• UBT-T1 – For outside diameters, faces, tapers and contours (Carbide roll)
• UBT-T2 – For outside diameters only (Carbide roll)
• UBT-T3 – For large outside diameters only (Hardened steel)
• UBT-T4 – For outside diameters where limited space is available. (Hardened steel only)
Gun Chamber Burnishing Tools (CBT)
Adjustable stop for chamber length
Redefining convention
One for the Chamber
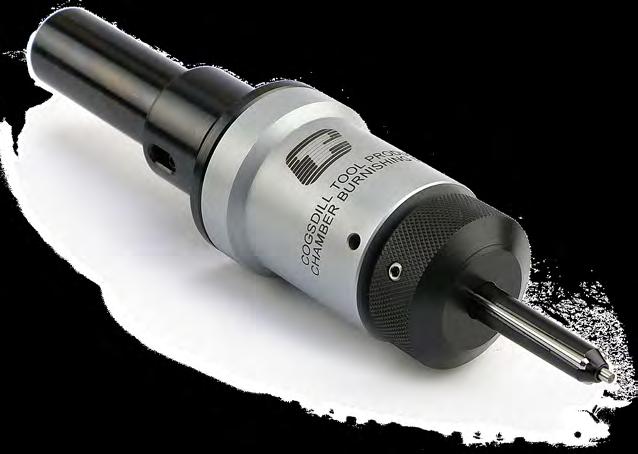
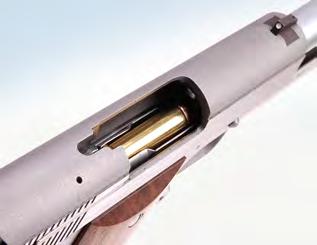
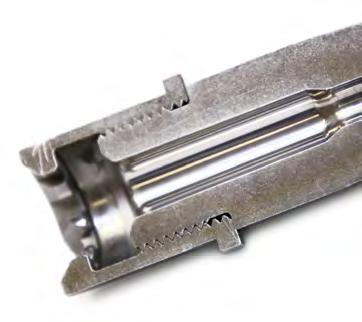
Ensure trouble-free shell casing ejection with the Cogsdill Gun Chamber Burnishing Tools (CBT).
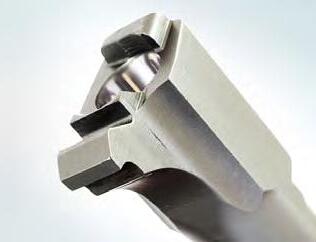
The chamber burnishing tools have been designed to the Sporting Arms and Ammunitions Manufacturers Institute (SAAMI) standard for Handgun and Rifle Chamber geometries. Our selection of chamber burnishing tools cover standard calibers from leading manufacturers.
Improved quality. In one pass. In seconds.
The conventional manufacturing process for armament shell chambers is reaming with a profiled reamer. Our expanding chamber roller burnishing tools enhance the reamed bore by producing an extremely fine surface finish (15 micro inches or less), which produces improved performance, repeatable shell ejection and prevents jams. Due to the fact that no metal is removed in the process, the surface finish depends on the existence of a uniform and tear-free reamed finish which will be caused to flow under the force exerted through the rolls.
CBT are versatile
• Create an ultra-smooth chamber finish in one pass in seconds.
• Offers a simple burnishing process for use after chamber reaming.
• Fast, easy tool set-up and operation. No special skills required.
• Use in any spindle from drill press to CNC machine.
• Easy to maintain, high quality tooling made by toolmakers.
TROUBLE-FREE EJECTION
Our standard CBT are available from stock with many other chamber configurations available upon request.
An ultra-smooth gun chamber finish. Enhance performance, spent shell ejection and loading speed.
Universal Diamond Burnishing Tools (UDBT)
Universally speaking
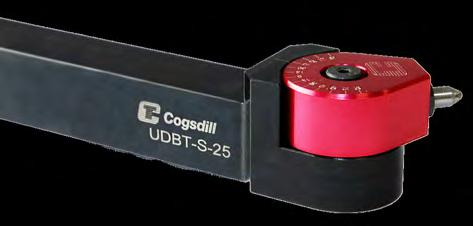
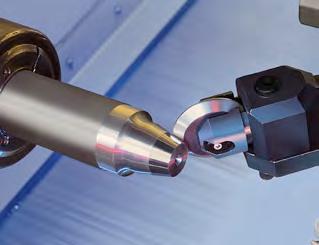
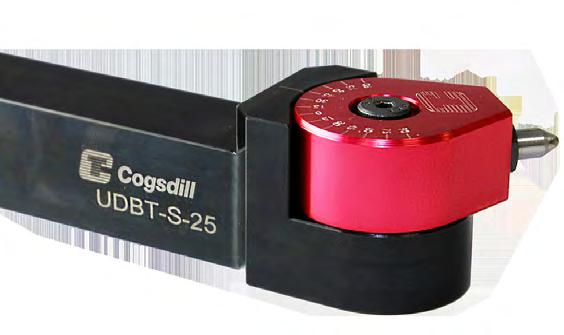
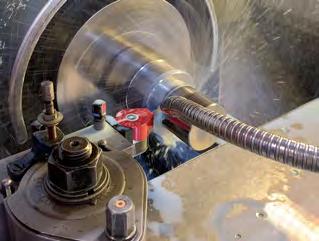
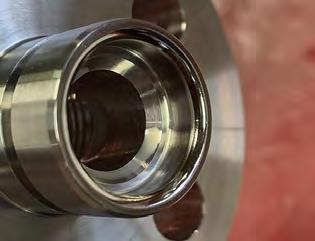
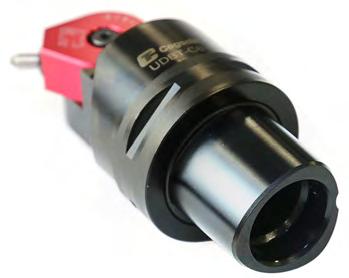
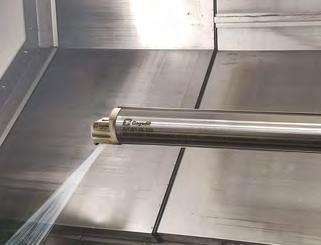
The latest addition to the Cogsdill Burnishing portfolio is the Universal Diamond Burnishing Tool Series (UDBT). UDBT are designed to produce mirror-like finishes on any surface; from carbon steels to tool steels, cast iron to alloys, and most ferrous and non-ferrous metals up to 55 HRC.
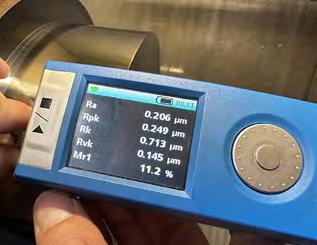
With most metals, a turned or ground part with a prepared 1.02–1.54 µm (40–60 µin) finish can be burnished to a 0.10–0.20 µm (4–8 µin) finish in seconds. Cast iron can be burnished to an 0.20–0.38 µm (8–15 µin) finish.
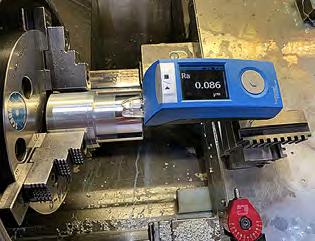
Using Cogsdill’s proven diamond insert geometry, our premium range of burnishing tools can achieve low Ra surface finishes in one pass – achieving results not attainable from any other metal removal process.
Standard model ranges available from stock:
• UDBT-S-25 (Straight Shank with 25mm square section)
• UDBT-S-0750 (Straight Shank with 3/4” square section)
• UDBT-S-1.00 (Straight Shank with 1” square section)
• UDBT-C4, UDBT-C5 and UDBT-C6 – integrated Capto Shank supplied with through coolant capability
Other shanks available upon request:
• KM50 and KM63 – integrated KM with through coolant capability
Simple and Efficient
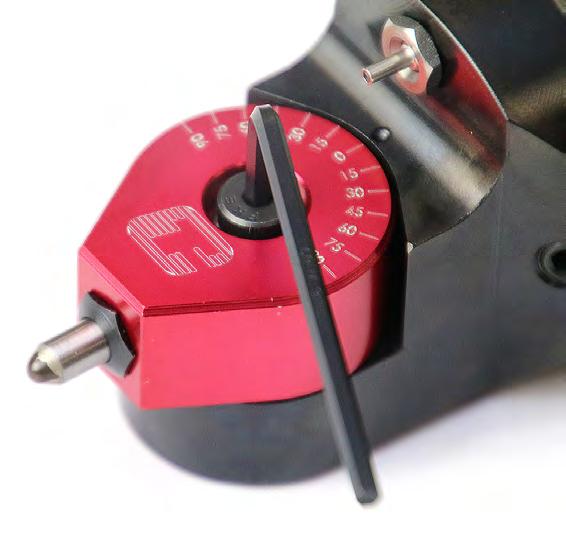
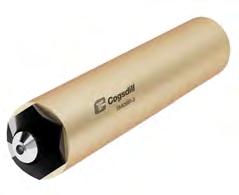
UDBT are designed to be adjustable through 180 degrees, which makes them the ideal choice tool for lower volume batch components where a designated orientated tool is not required.
This single tool streamlines operations significantly as it can be utilized in either left or right-handed machine configurations – eliminating the need for multiple tools in specific environments.
Further more, set up and operation is relatively simple, no special operator skills are required.
As a result, Cogsdill UDBT offers incredible production efficiencies and cost effectiveness.
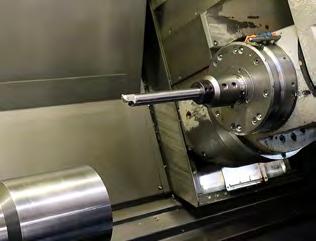
UDBT offers flexibility for burnishing large bores, outside diameters, tapers and faces to achieve superior surface finishes not possible by turning alone.
Mini Series (UDBTM)
For when size matters
ACTUAL SIZE
The range has just got bigger (actually, it’s just got smaller!)
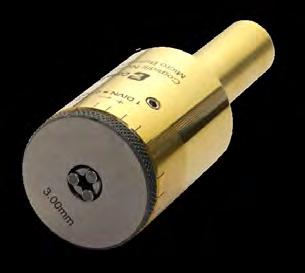
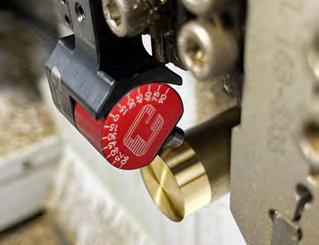
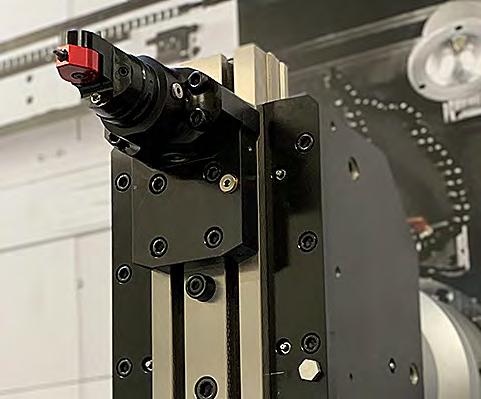
Following on from the success of the original UDBT, we are pleased to introduce a smaller sibling designed specifically for CNC sliding head lathes (Swiss-type).
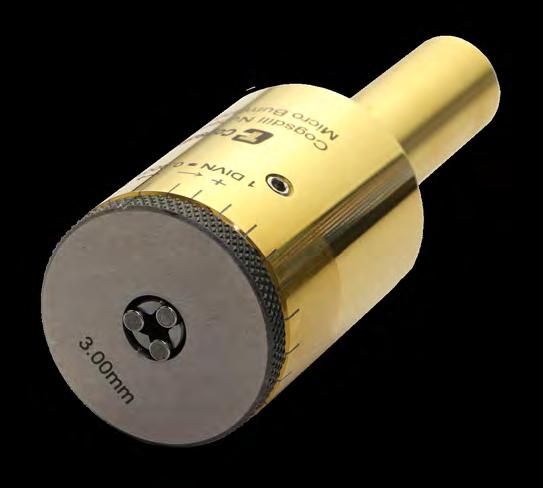
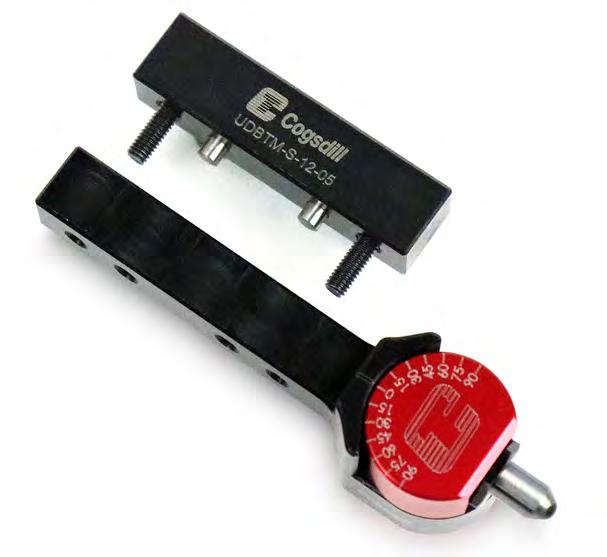
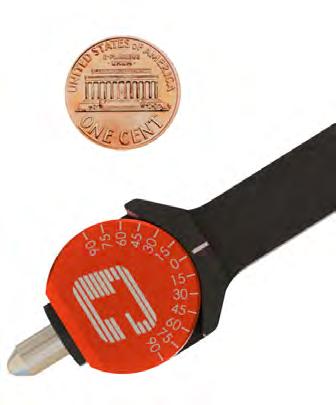
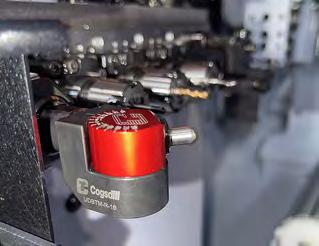
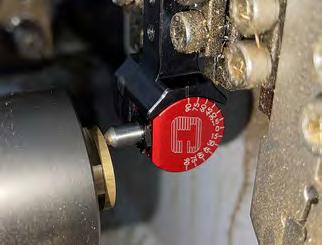
Cogsdill Universal Diamond Burnishing Tool Mini Series (UDBTM) is a compact burnishing solution, with the adjustment head not much bigger than a penny (as shown in the illustration). But don’t let it’s small size fool you, this tool offers huge return on investment.
There are currently two different models available from stock:
• UDBTM-S-12 (Square Shank with 12mm section + included clamp plate assembly)
• UDBTM-R-16 (Round Shank with 16mm diameter)
Did you know?
By combining Cogsdill’s premium range of burnishing tools with the ZX facing heads, you can now achieve low Ra surface finishes in one pass from a single set-up.
Machine tool requirements
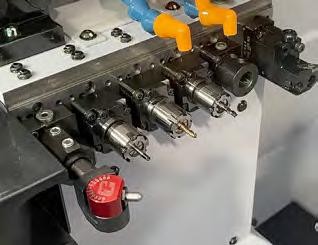
Developed as a solution for burnishing on CNC Swiss-type sliding head machines, this single tool streamlines operations significantly as it can be utilized in either left or righthanded machine configurations, with either round or square shanks to suit tool post or collet installation.
Compatible with most CNC sliding head lathes.
The quick and simple castellated adjustment makes this the most versatile diamond burnishing tool on the market.
Diamond Burnishing (DB) Diamond Burnish Face Mill (DBFM) Flat on your face
Diamond Hard
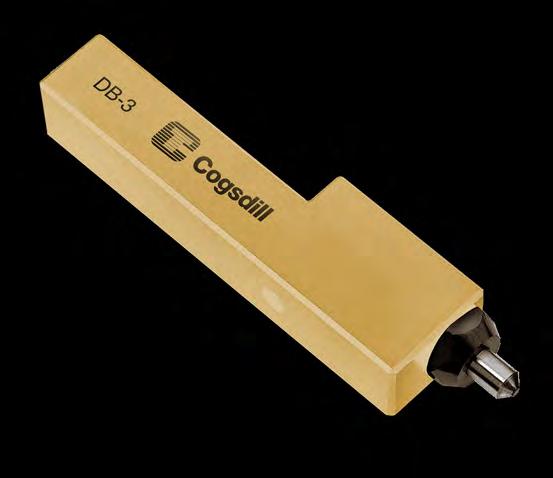
The Cogsdill Diamond Burnishing Tools are designed to produce high quality, low micro-inch burnished finishes on shafts, large bores, and faces. With most metals, a turned or ground part with a properly prepared 40 to 60 micro-inch (1.02 to 1.54 µm) finish can be burnished to a 4 to 8 micro-inch (0.10 to 0.20 µm) finish in seconds. Cast iron can usually be burnished to an 8 to 15 micro-inch (0.20 to 0.38 µm) finish.
• Multiple designs for use on most turning and Swiss-type machines – manual or CNC
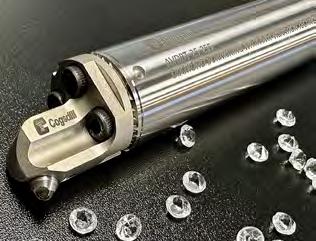
• All tools have include a premium quality, replaceable and polished diamond insert
• Easily adjustable for optimum burnishing pressure
Simple and efficient, Cogsdill Diamond Burnishing Tools are designed to produce mirror-like finishes on any size stock; from carbon steels to tool steels, cast iron to alloys, and most ferrous and non-ferrous metals.
For conventional slide adapters
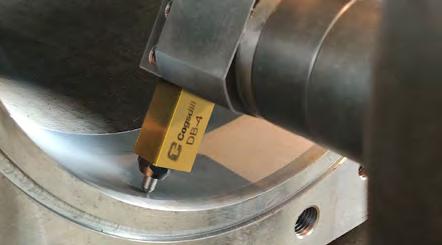
The DB Series offers enhanced flexibility for high-volume applications or when adjustable spring pressure is required.
Utilizing our unique and proven diamond geometry, but designed for use in conventional open-ended square shank slide adapters.
For high volume applications, there are a multitude of dedicated tools specific to your machine configuration.
style, designed for use in a tool-post in either a manual or a CNC machine.
in CNC machines.
Mini round Boring-Bar style, designed for use in turrets in Swiss-Type CNC machines.
All diamonds that Cogsdill use in their tool manufacturing are sourced via De Beers and adhere to their Code of Origin to provide assurance that it is natural, conflict free and meets industry-leading ethical standards.
CNC machines.
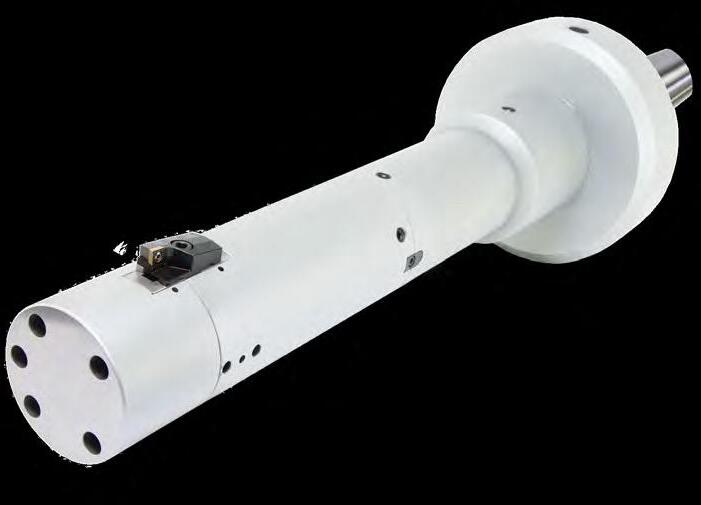
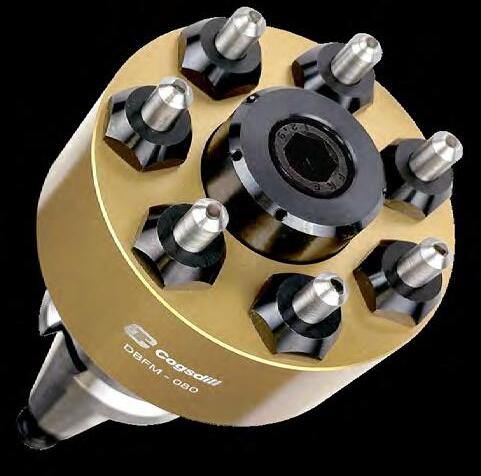
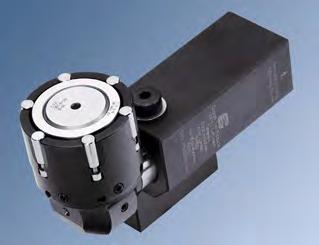
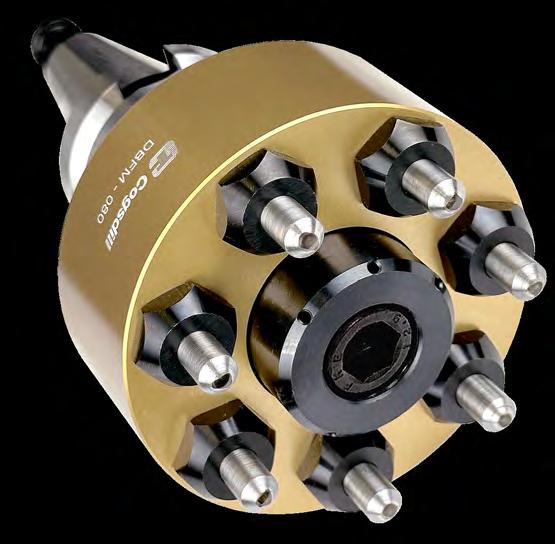
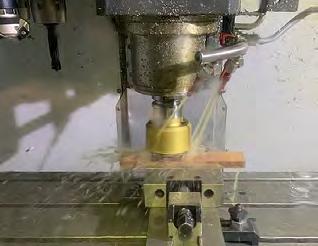
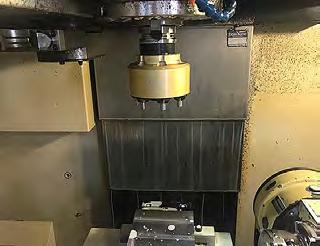
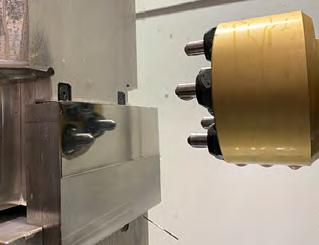
The Cogsdill Diamond Burnish Face Mill Tool (DBFM) for burnishing flat faces achieves superior surface finishes.
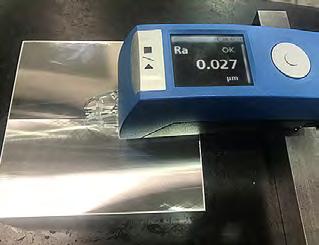
Using Cogsdill proven diamond insert geometry, our premium range of burnishing tools can achieve low RA surface finishes, by cold flowing the peaks into the valleys in one pass –achieving results not attainable from any other metal removal process.
Simple and efficient, Cogsdill DBFM tools are designed to produce mirror-like finishes on any surface; from carbon steels to tool steels, cast iron to alloys, and most ferrous and non-ferrous metals.
Set up and operation is relatively simple, no special operator skills are required.
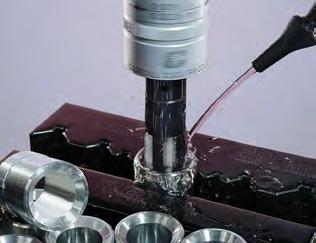
All tools are supplied with through coolant capability but while the tool must be used with coolant, no special coolant is required. Straight oils, soluble oils, and synthetic coolants can be used to provide the necessary lubrication.
FLAT OUT
MIRROR FINISH
Work harden to a superior finish in one pass. Burnish flat surfaces effortlessly.
• Designed to fit in your CNC machining center, with a common interface to suit industry-standard milling arbors.
• The tools can be used on both large and small areas, and are ideal for short production runs. The Diamond Burnish Face Mill Tool can produce quality finishes on interrupted surfaces, such as a face of a flange having a series of bolt holes or a keyway.
• The tools are supplied pre-loaded, but the spring pressure can be adjusted to ensure consistent pressure on the face of the component, assuring repeatability from part to part.
Spare diamond inserts are easily replaced and available from stock. Diamond nibs are interchangeable between all sizes and styles.
The premium quality and replaceable diamond burnishing insert is polished and contoured to provide superior finishes and long tool life. Although the diamond nibs are qualified, Cogsdill recommended replacing nibs as a set.
DB Series Turning-Holder
Round Boring-Bar style, designed for use in turrets
Mini Turning-Holder style, designed for use in a tool-post in Swiss-Type
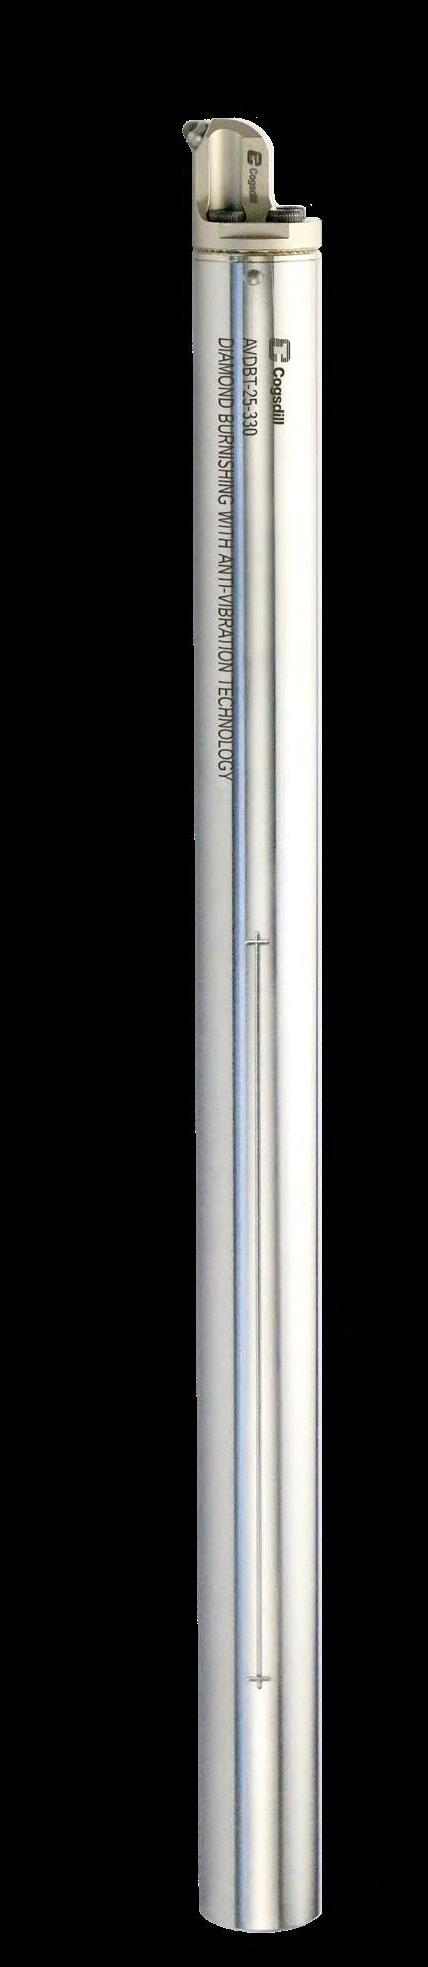
Standard Series (AVDBT)
Cogsdill are the premium manufacturer of burnishing tools. . Diamond tools available for immediate shipping!
Introducing the most anticipated addition to the Cogsdill’s burnishing portfolio
Anti-Vibration Diamond Burnishing Tools (AVDBT)
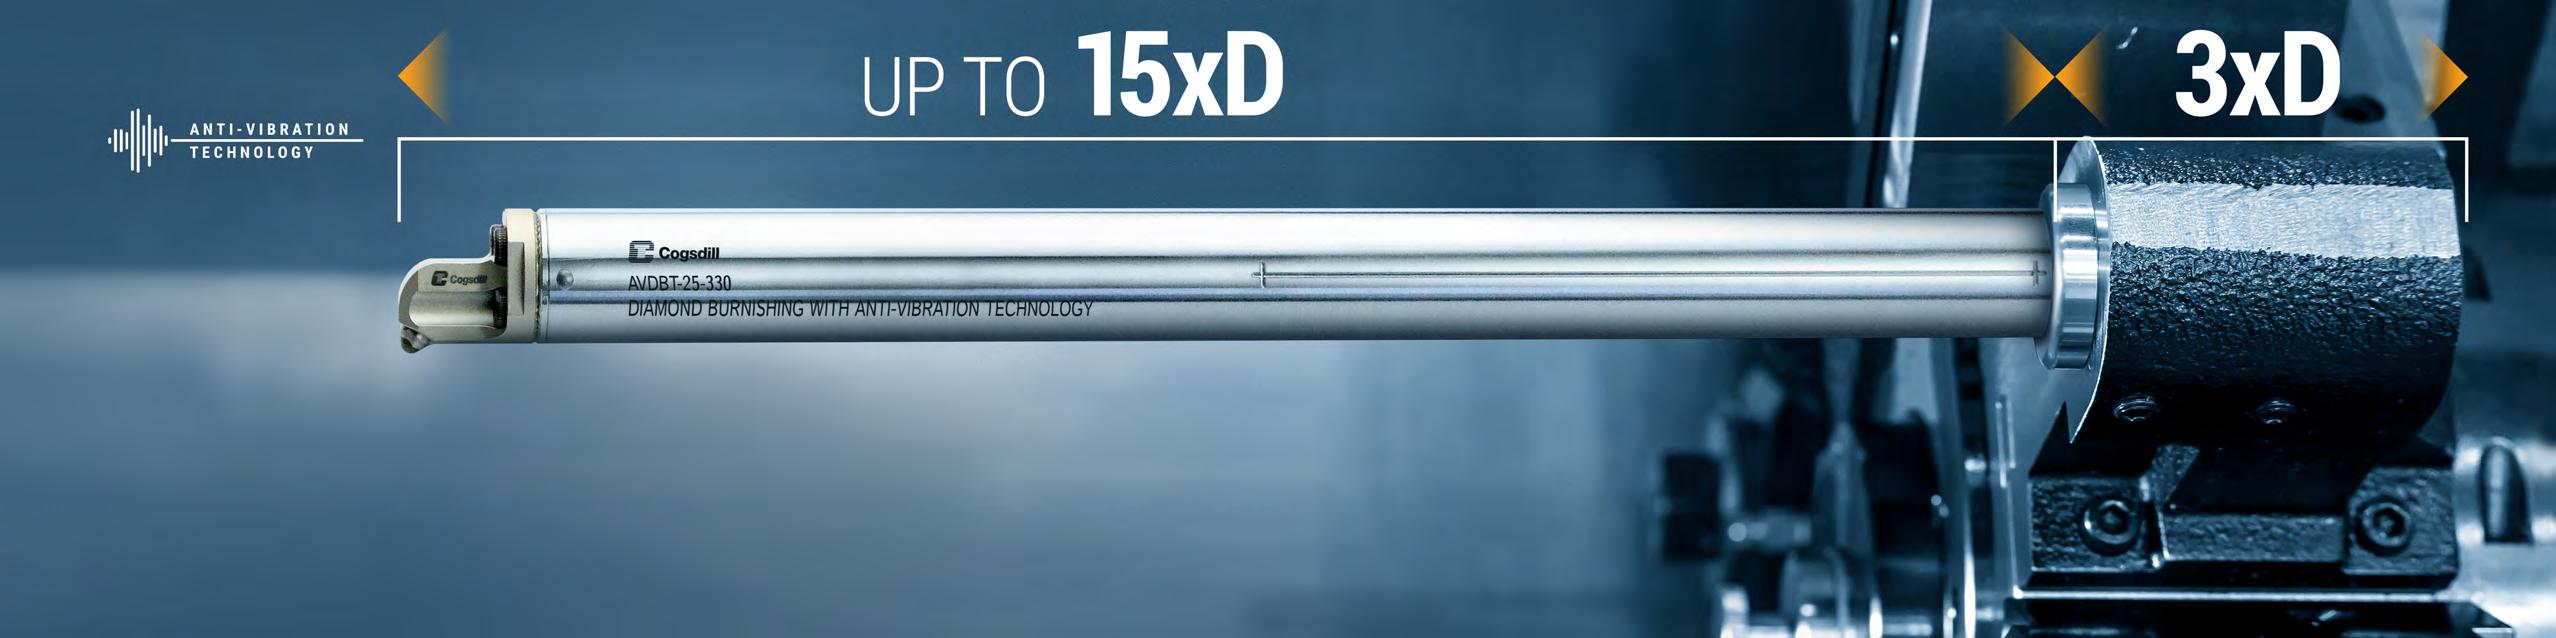
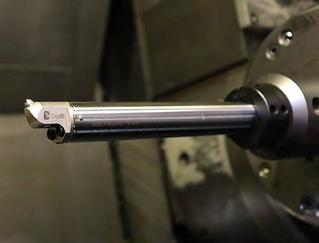
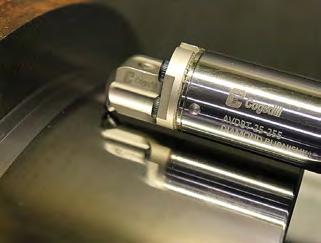
Combining Cogsdill’s proven diamond insert geometry with the latest auto-tuning, mass dampening, anti-vibration technology – AVDBT offers incredibly low Ra surface finishing for both external diameters and internal bores at depths up to a staggering 15xD!
Good(bye) Vibrations
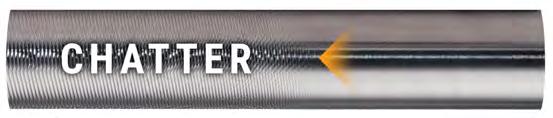
Typically, with conventional single point boring and burnishing, sur face finish deterioration can arise when machining applications over 4xD due to increased vibration and regenerative tool chatter. This becomes more problematic when working with even higher overhangs.
Trying to stabilize the surface finish usually involves a lower cutting speed, reduced depth of cut, or increased feed per revolution. All adding to higher production costs or compromising on quality.
Our Anti-Vibration technology starts with the auto-tuning mass damper.
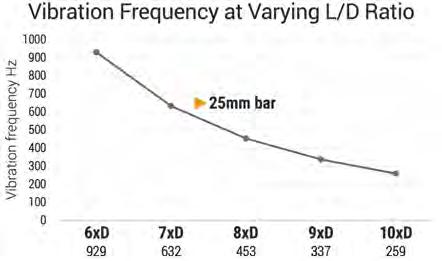
Cogsdill’s tooling is unique due to the complex polymers that surround a tungsten mass within the boring bar. Vibration frequencies differ significantly over varying lengths. The polymers in turn respond by changing their form, adjusting to the cutting frequency which counteracts vibration – automatically and consistently – effectively auto-tuning the “sweet spot” with no manual adjustment required.
Turning a complex technology into a simple plug-and-play solution.
ACTUAL SIZE
QUICK CHANGE
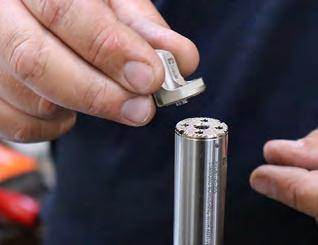
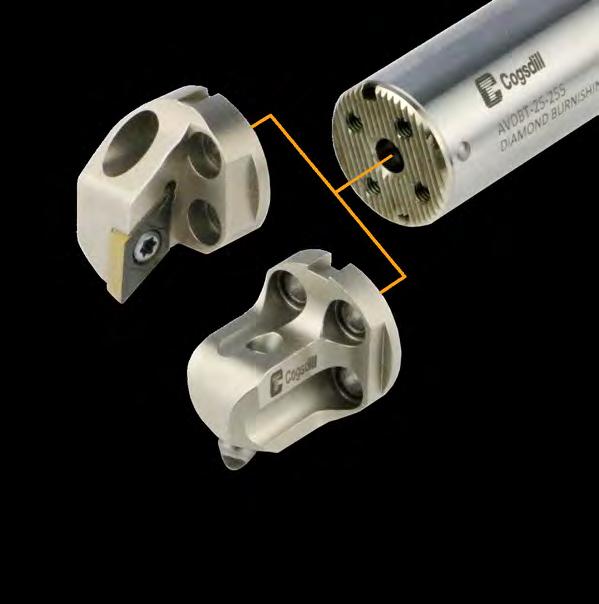
Designed with a quick-change interface that incorporates a serrated coupling for alignment and secure tightening. With our exchangeable heads, you can switch from turning/boring to burnishing in seconds with repeatable results time after time.
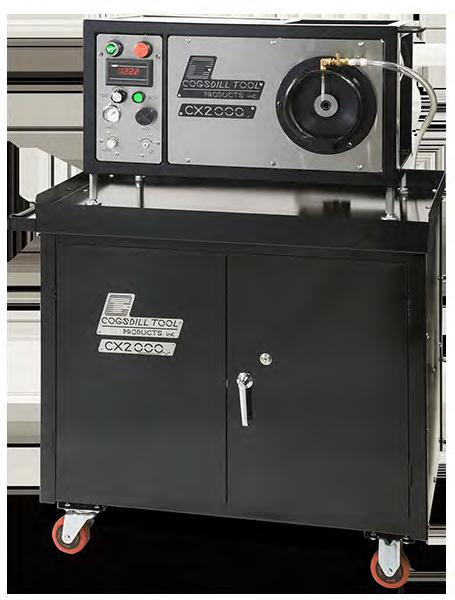
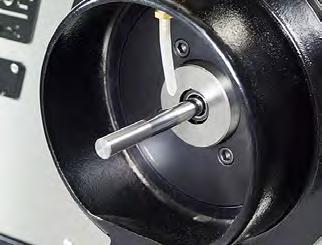
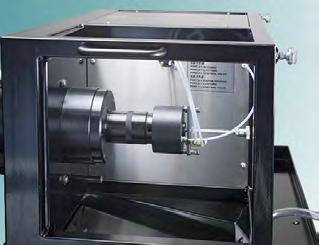
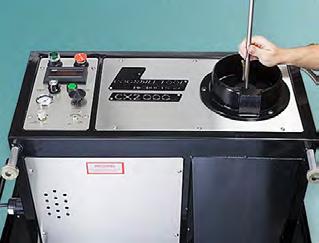
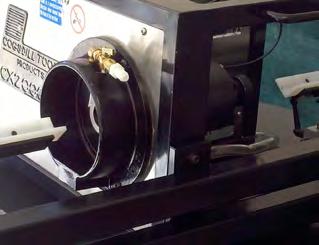
Cogsdill’s CX machines roller burnish cylindrical diameters of any length in seconds.
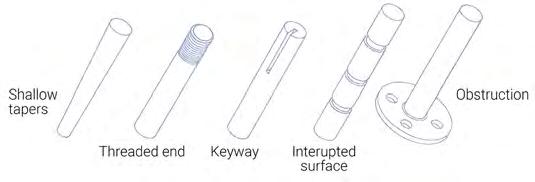
Parts are sized, finished and work hardened by highly polished, precision rollers in one quick pass. Fatigue life, corrosion resistance and appearance are enhanced as your parts are accurately sized and finished. Various model options are designed to meet your manufacturing requirements. Equipment options are available to accommodate through-feed applications, parts with obstructions, and part-to-part size variations.
Cylindrical parts of any length, bars, tubing, wire and stranded cable may all be processed with Cogsdill’s self-contained, selffeeding roller burnishing machines.
IN ONE QUICK PASS
Better quality parts with improved surface finishing – produced in less time at a lower cost.
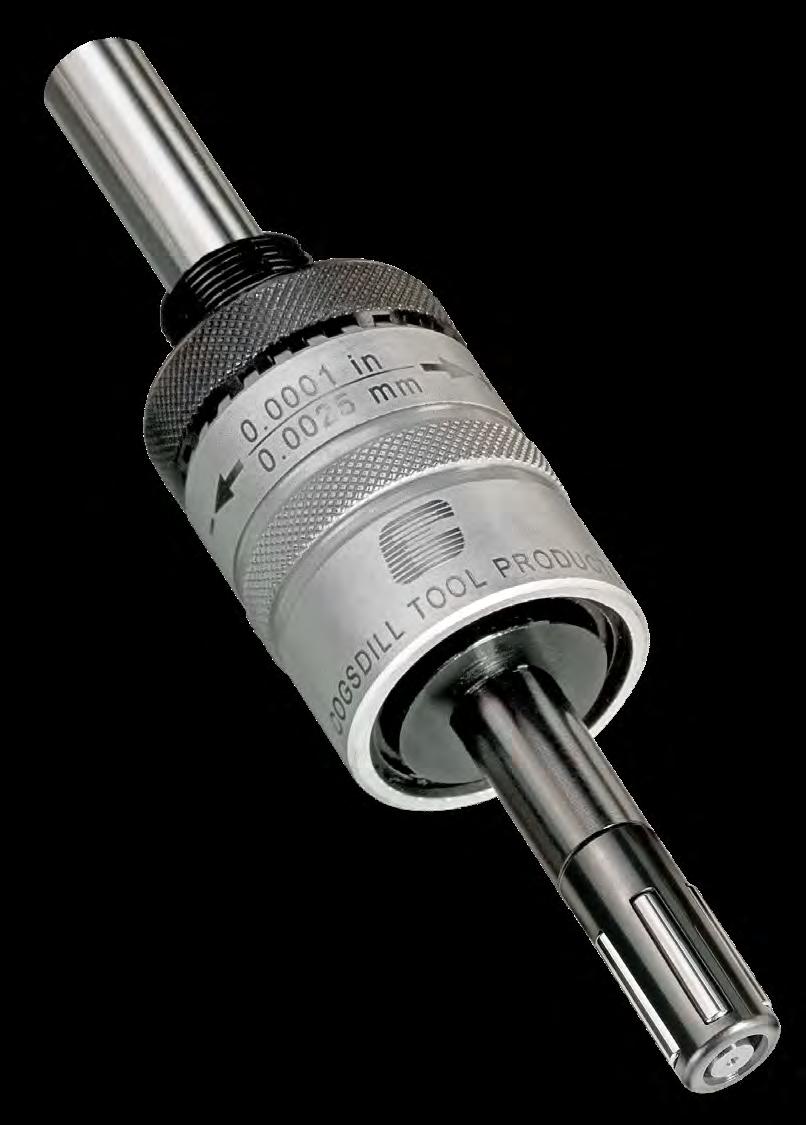
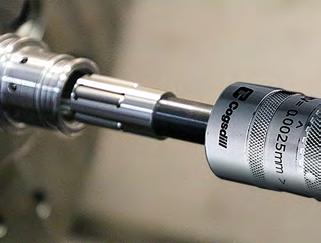
Accurate sizing – Tolerances within .0001 inch (.0025mm) are attainable, depending on variables. A prepared tolerance of .002 inch (.05mm) can usually be reduced by 50 % (.001 inch /.02mm).
Low micro finishing – One pass through a Cogsdill CX machine can quickly reduce a 20-40 microinch Ra (0.5 to 1.0 micrometer) ground surface or an 80-120 microinch (2-3 micrometers) Ra turned surface to a mirror like 5 microinch (.125 micrometer) Ra finish or lower.
Work hardening – With certain materials, increases in surface hardness of up to 3 points on the Rockwell “C” scale are attainable.
Appearance improvement – Machined parts (turned or ground) can be roller burnished to lustrous, mirror like finishes.
Fast processing – Cylindrical parts of any length are processed at speeds up to 30 feet/min (9.14 m/min).
Examples of various types of parts which are processed by CX external roller burnishing
Coolant systems are designed and recommended to supply the necessary part lubrication for burnishing.
ROLLING IN THE DEEP
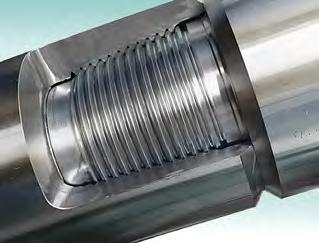
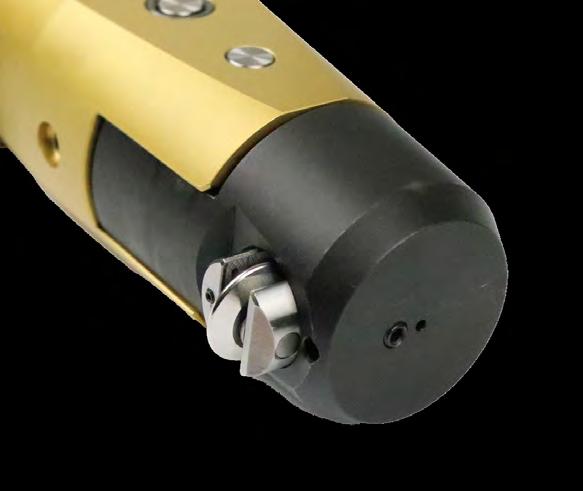
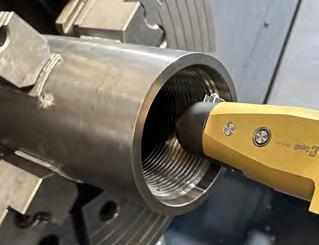
Thread Root Rolling Tools (TRR), also known as cold root rolling, significantly increase the fatigue strength of highly stressed components whilst also producing a superior surface finish.
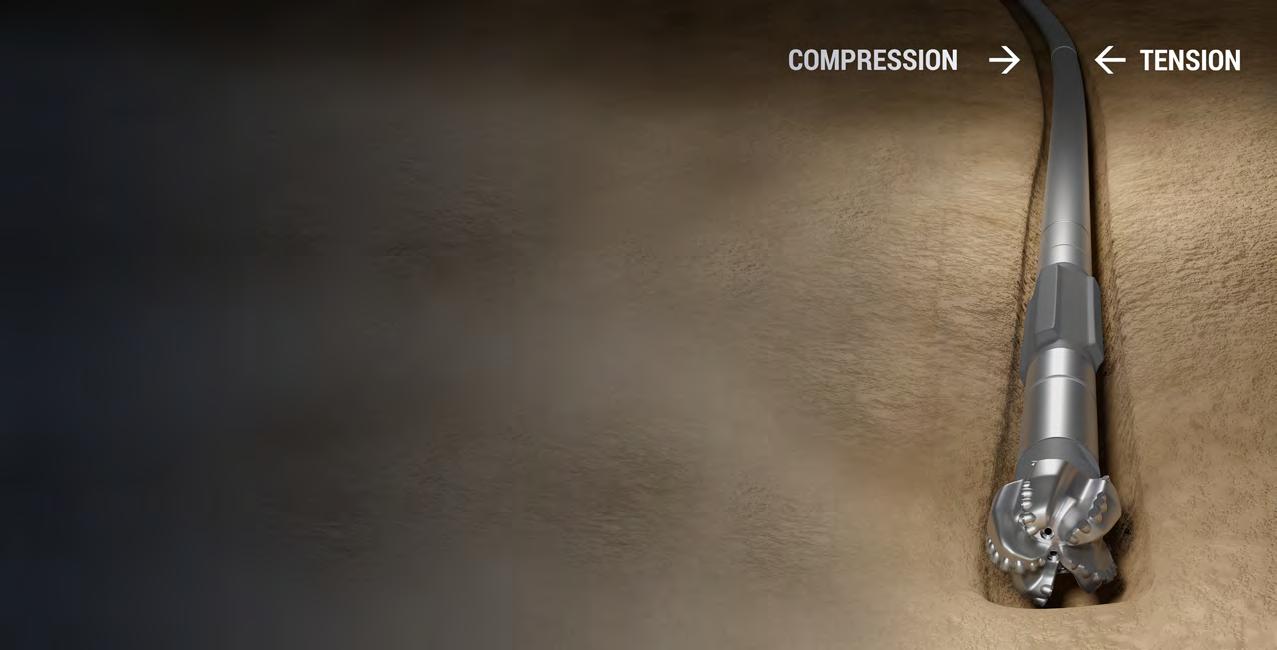
Cold Root Rolling is an advanced method of roller burnishing that uses controlled pressure to cold-form the material at the root of newly machined or previously cut threads.
This process introduces a compressive residual stress that cancels out the tensile stress that the component is subjected to during use.
Reduce the chance of corrosion and dramatically extend the life of threaded connections.
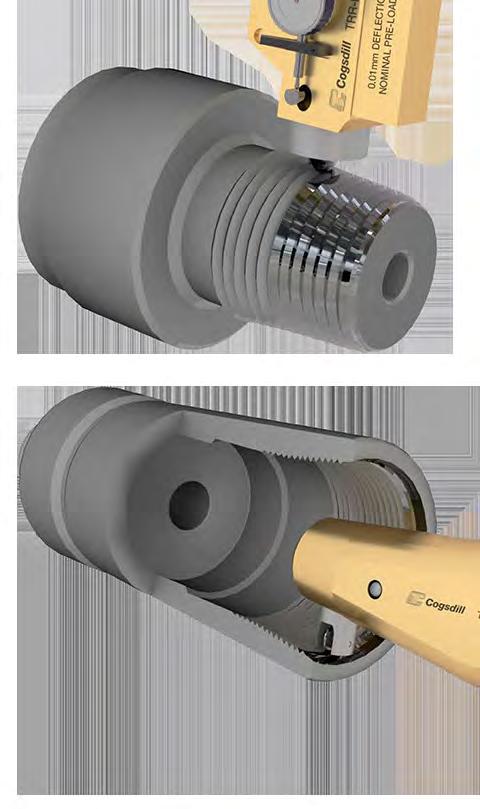
• TRR-IN (Box) for internal (female) threads
• TRR-EX (Pin) for external (male) threads
Available with various roll radii options
IN SECONDS!
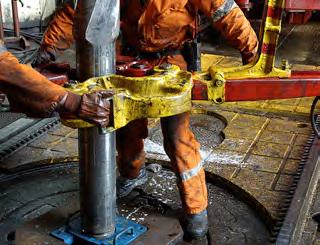
Oil & Gas
Cold Root Rolling ensures extended wear life to the pipe thread connection by altering the materials substructure and improving the surface finish to diminish corrosion that occurs in harsh environments.
Using a hardened formed HSS roll that matches both the profile and designated radius of the tapered thread, pressure is applied in order to deeply penetrate the root radius, which displaces and deforms the thread material.
DRILL STRING CONNECTORS
® We hold a range of metric and imperial tools plus assortment of blades. Available from stock for immediate shipping!
Taking the edge off
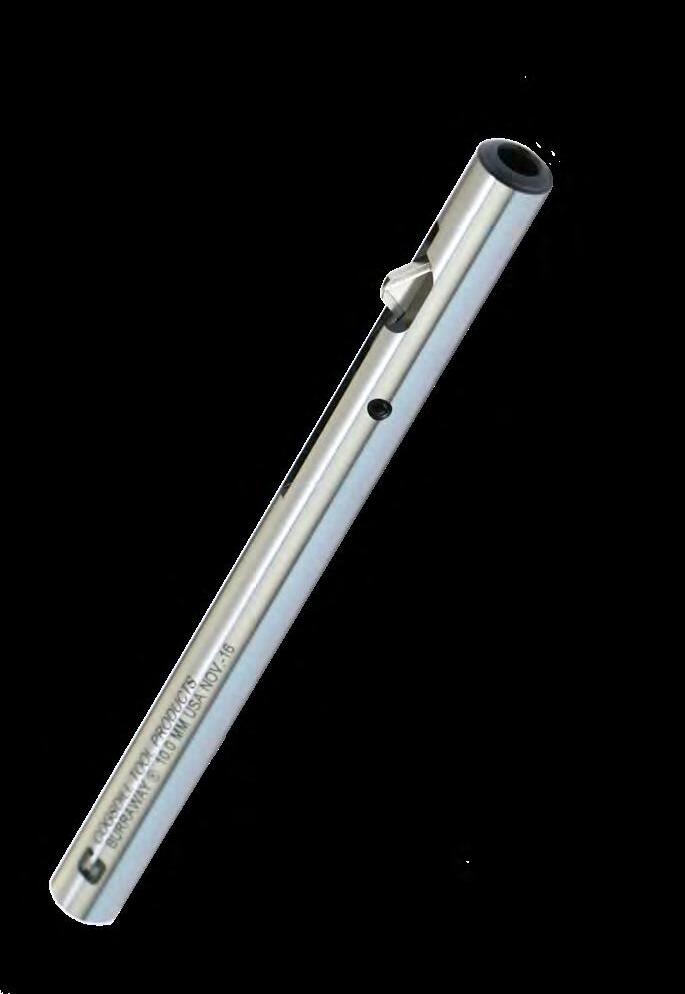
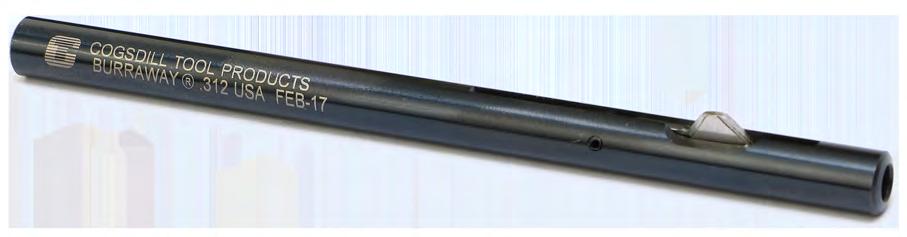
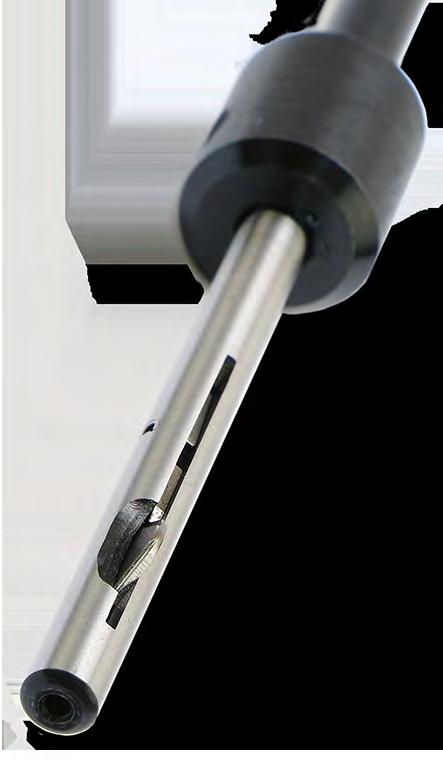
Burraway tools suit a variety of machines from manual to CNC – and can even be used in a hand-drill with excellent results.
Polished blades are designed not to damage the bore.
They are available in an assortment of metric and imperial sizes ranging from 2mm to 50mm / 0.093” (3/32”) to 2 inches, with a range of standard size tools and blades always held in stock.
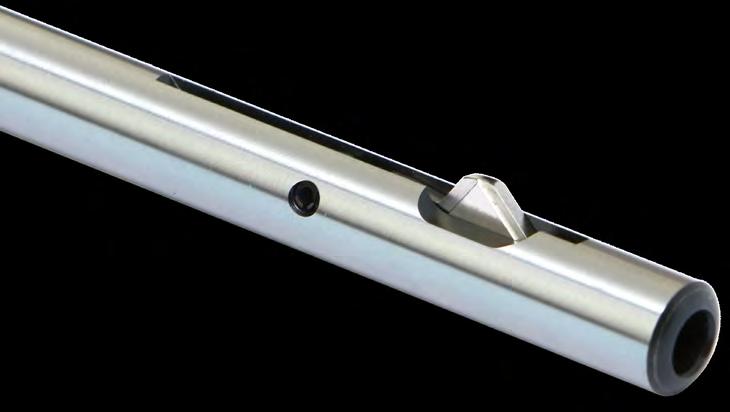
The Burraway tools feature an inexpensive, replaceable cutting blade which adjusts to control the amount of edge break and can be easily replaced within a few seconds.
A range of cutting-edge geometry options to suit different materials are offered, and as standard, tools are supplied already fitted with a double acting blade. The crowned and polished top surface of the blade will not mar the inside surface of the hole.
All Burraway tools support a simple method for easily adjusting cutting pressure and chamfer size via a tension adjustment screw.
Both Sides in One Pass
How Burraway
tools work:
1 Upon entry, spring tension holds the cutting blade in the extended position as it removes the burr on the front of the hole.
2 As the feed load increases, the pre-set spring tension is exceeded and the blade retracts automatically as the tool passes through the workpiece.
3 Spring tension again causes the blade to extend as it emerges from the ID of the part; the burr is removed on the back side of the hole on the return stroke.
Design features
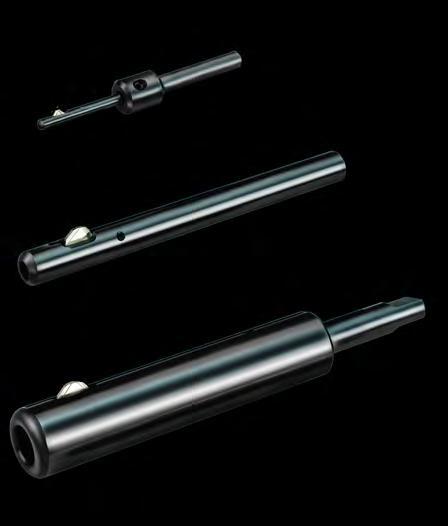
There are three types of Burraway tools – Types
A, B & C – that correspond to differing diameters.
Type A tools
Two-piece construction (arbor assembly and adapter).
• Imperial: hole sizes from .093 through .203 in.
• Metric: hole sizes from 2 to 5mm
Type B tools
A single-piece construction.
• Imperial: hole sizes from .218 through .750 in.
• Metric: hole sizes from 5.5 through 19mm
Type C tools
A single-piece construction.
• Imperial: hole sizes from .750 through 2 in.
• Metric: hole sizes from 20 through 50mm
A variety of tool designs to meet your needs
Burraway tools are available for both metric and imperial hole sizes. Standard drill sizes are available from stock.
Custom tools – larger sizes, altered standards, or special designs – can also be supplied to suit your particular requirements.
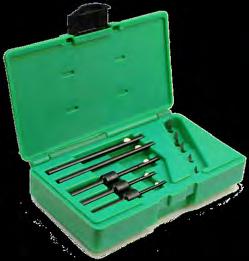
Burraway Kit
A durable box containing five deburring tools with replacement blades in popular imperial hole sizes: 1/8 in. • 5/32 in. • 3/16 in. • 7/32 in. • 1/4 in.
SMALLEST JUST GOT SMALLER
Micro-Burraway for your small hole applications from Ø 1mm
Blade information
Various blade rake angles and spring tension options are available and recommended for deburring specific material types.
• Positive rake – Ideal for steels and stainless steels
• Negative rake – Ideal for softer materials such as brass or hard plastics
• Neutral rake – Ideal for aluminum
Double-Acting (DA) For deburring both front and back of holes
Back-Acting (BA) For deburring back of hole only
Front-Acting (FA)
For deburring front of hole only
We hold a range of metric and imperial tools. . Available from stock for immediate shipping!
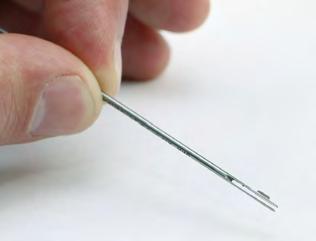
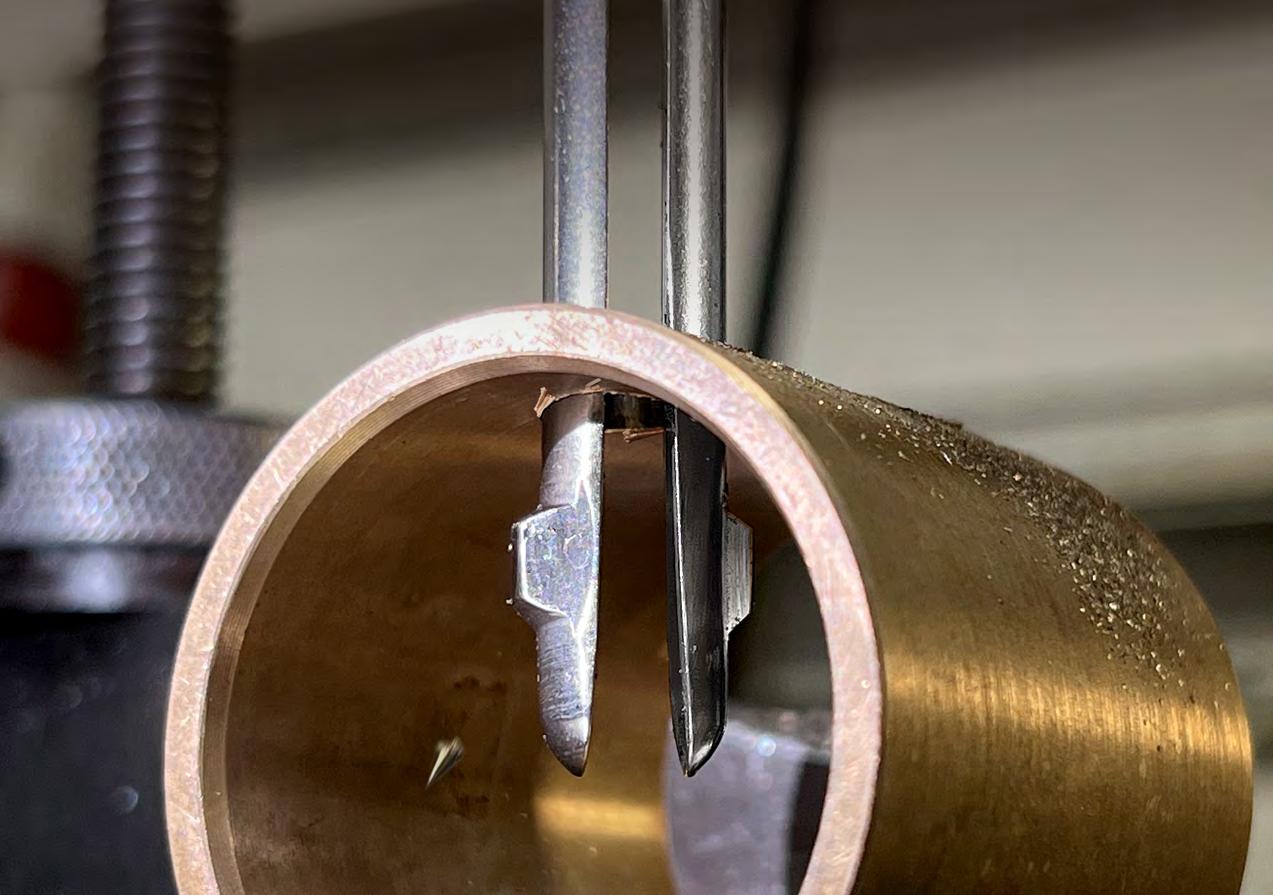
The original “Clothes Pin” tool
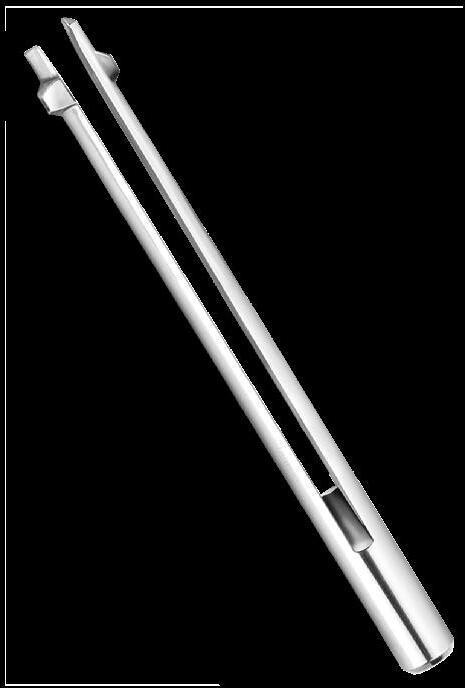
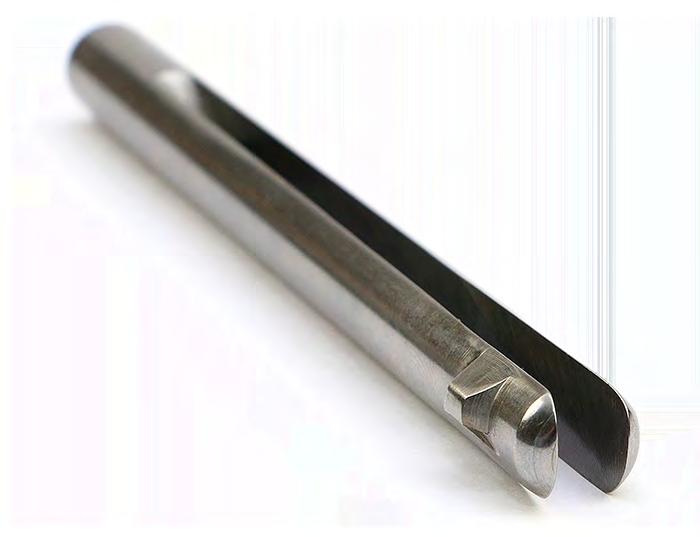
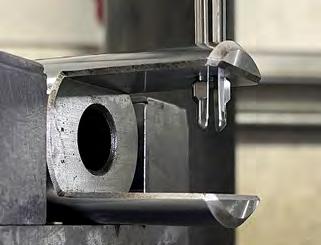
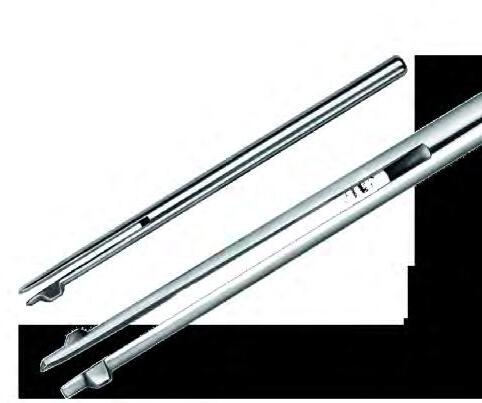
Often copied but never beaten, Burr-Off is one of the most efficient and economical hole de-burring tools ever made for mass production.
Burr-Off tools
CP-04 through CP-13 are for hole sizes from 1.57mm (.062 inch) through 5.56mm (.219 inch) and have a single cutting edge. Larger tools feature two cutting edges.
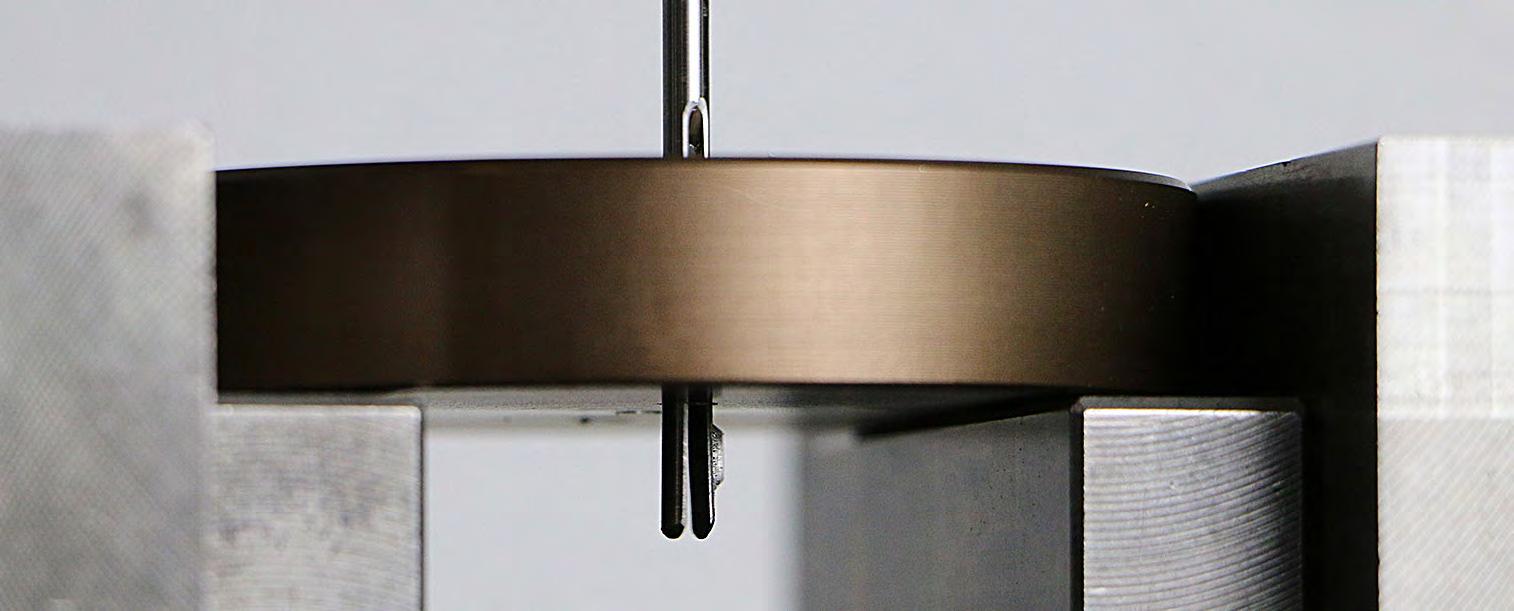
Cogsdill originated the “Clothes Pin” tool over half a century ago. The Burr-Off is a simple one-piece construction. Delivering super efficient hole deburring in a wide range of sizes. The Burr-Off operates on the same basic principle as the Burraway, but is designed for high-production, automated deburring operations, where hole alignment can not be guaranteed – and primarily for ferrous materials. The open-slot design of the “clothes pin” tool allows chips to clear easily, which makes the tool ideal for automatic equipment and multi-spindle machines. Just like the Burraway, the Burr-Off deburrs the front, back, or both sides of holes in one fast pass.
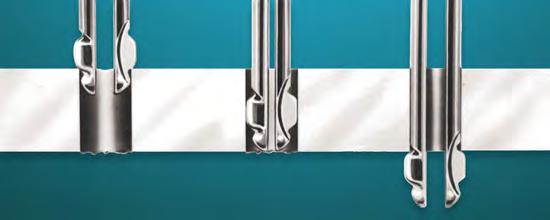
How Burr-Off tools work:
1 Integral cutting edges remove the burr from the front of the hole as the tool enters the hole.
2 The slotted design allows the tool to “collapse” under load as the tool feeds through the workpiece. The crowned and polished top surface of the cutting edges will not mar the inside surface of the hole.
3 The back of the hole is deburred on the return stroke.
High volume. No adjustment.
For mass production hole de-burring with no tool adjustment necessary.
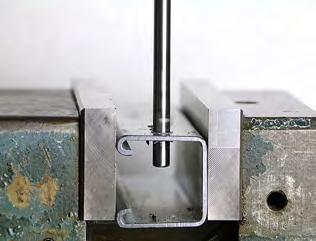
Ideal for where access is restricted, Burr-Off tools are perfect for interrupted or interference cuts, holes close to shoulders, bosses, back folded sections, multi-layer or multi-sectional parts – pipes, tubes, liners housings, flanges – whether cast, stamped, extruded or machined.
CROSS-HOLE DEBURRING IDEAL FOR FERROUS
Variety of tools
Burr-Off tools are available for both metric and imperial hole sizes. Standard drill sizes are available from stock.
The integral cutting edges can be altered upon request for front or back-cutting only.
Custom tools – larger sizes, altered standards, or special designs –can also be supplied to suit your particular requirements.
Micro stop. Piloted countersink.
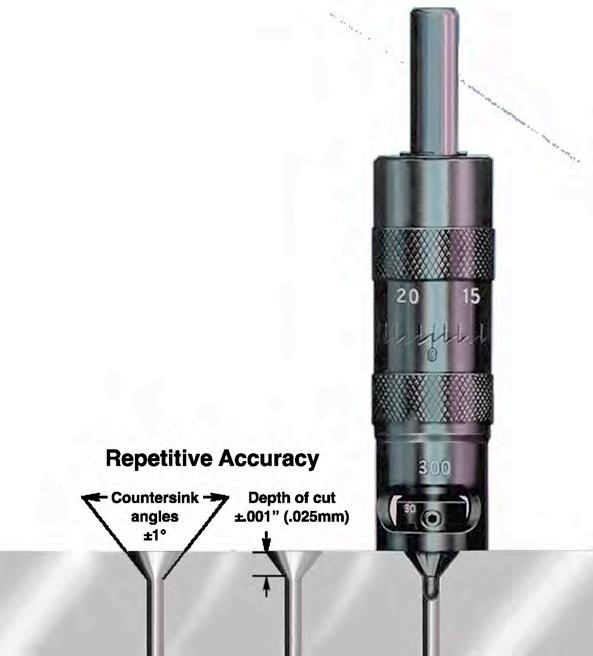
Precision depth control with accuracy and consistency.
IDEAL FOR AIRCRAFT
Countersink with precision
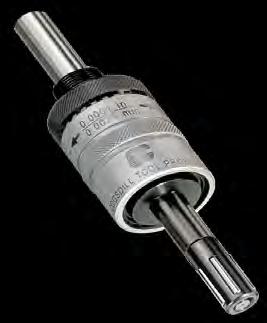
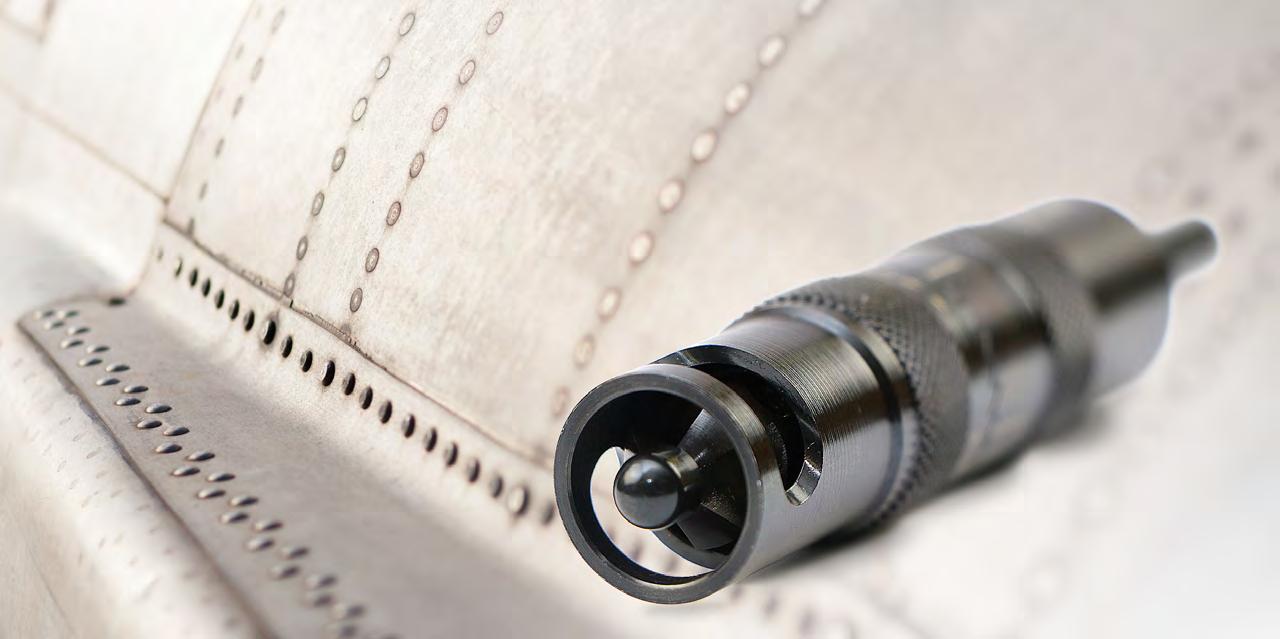
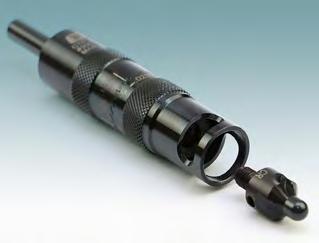
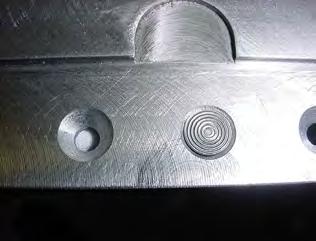
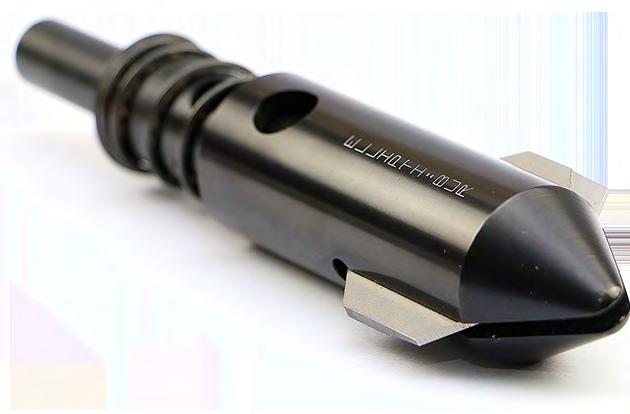
The Micro-Limit is a precision depth-control countersinking tool. Consisting of a drive with a piloted countersink and a depth control adjustment feature, suitable for hand held power tools or machine tools.
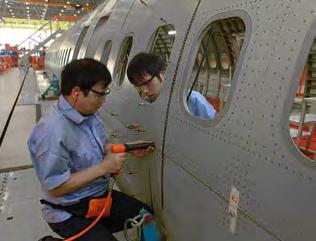
The Micro-Limit drive is designed and built for rugged production work with repetitive accuracy. The thrust load is taken up on ball bearings through a hardened steel stop collar. The drive shaft rides on needle bearings. This design makes our drive the most durable in the industry and why it is the preferred countersinking tool for high-production requirements, such as rivet hole preparation in aircraft manufacturing.
Three drive models cover a wide range of hole sizes. Adjustment is in increments of .025mm (.001 inch).
An array of interchangeable countersinks and pilots are available as standard.
The Micro-Limit is also offered with an overtravel unit built into the standard drive.
Elliptical Illusion
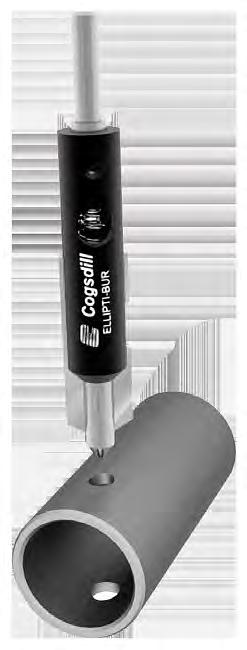
The Ellipti-Bur® is designed for deburring irregular hole surfaces, such as those which are generated by drilling into curved surfaces, or by drilling at an angle. Enabling the user to perform these difficult deburring operations quickly and accurately, and without jigs, fixtures, or special operator skills.
This automatic self guiding feature produces a relatively uniform break on the edge of the hole.
Design Features
The Ellipti-Bur features a spring-loaded and self-centering conical pilot to locate and seat the tool for consistent results. Upon contact with the part, the HSS blade disengages and floats, remaining free to oscillate and follow the irregular surface geometry of the hole. This ensures both radial displacement resulting from the elliptical shape of angular drilled holes and axial displacement (“rise and fall”) from the saddle shaped configuration of holes drilled in cylindrical surfaces.
All essential tool parts are hardened and ground for durability.
Three models cover a range of hole sizes from 3.96 to 25.4mm (5/32 to one inch).
Curved surfaces. Simply deburred.
IDEAL FOR OIL HOLES
Turn your boring machine into a lathe
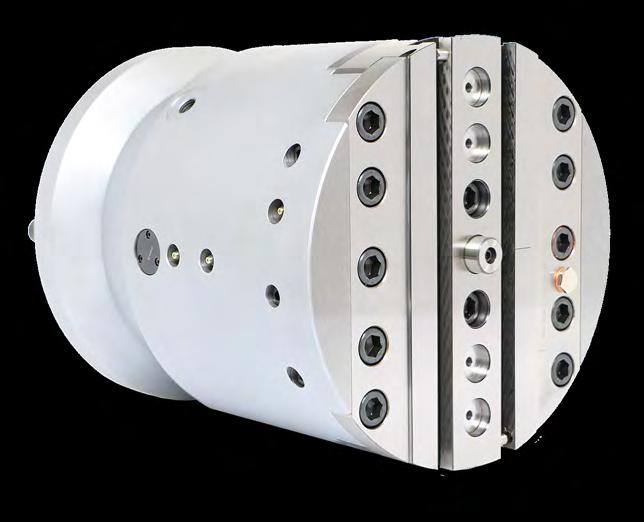
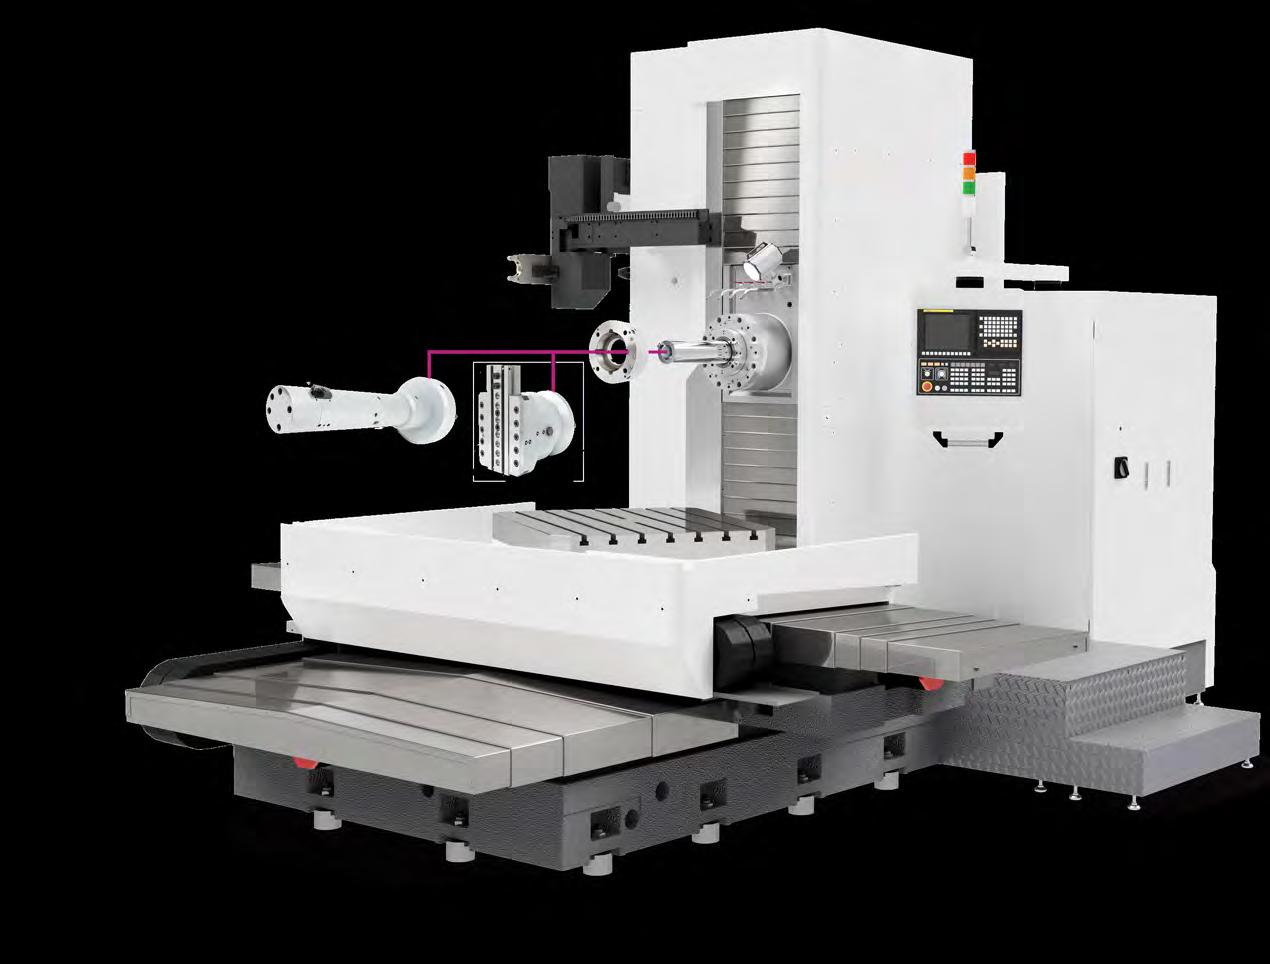
The Cogsdill ZX range of Facing / Contouring Heads and Modular Boring tools allow relatively simple 2-axis CNC programs to perform a variety of machining operations by converting linear motion into radial slide movement by mechanical actuation.
No need for an additional electronic interface, expensive software or hardware.
Part changes can be accommodated quickly and easily with program changes. Operations that were previously performed manually can be converted to CNC Control, thus improving productivity, accuracy, part to part repeatability and improved surface finish.